B2B Activewear Manufacturing & Quality Engineering

Private Label Activewear Manufacturer: Seamless & Cut-and-Sew with Strict Quality Control

MOVEVOX provides end-to-end activewear development and scalable manufacturing for established apparel brands, fast-growing DTC labels, and professional importers. Operating 28 Italian Santoni seamless knitting machines alongside dedicated cut-and-sew production lines, we eliminate sample-to-bulk quality drift through strict specification freezing, in-house technical review, and multi-stage QC inspections.

  • Dual Manufacturing Systems: 100 pcs MOQ for seamless activewear, 150 pcs for cut-and-sew garments.
  • 5–10 Working Days: Fast turnaround for confirmed sample development.
  • 5-Stage QC Gate System: In-house inspection led by an 8-year quality assurance manager.
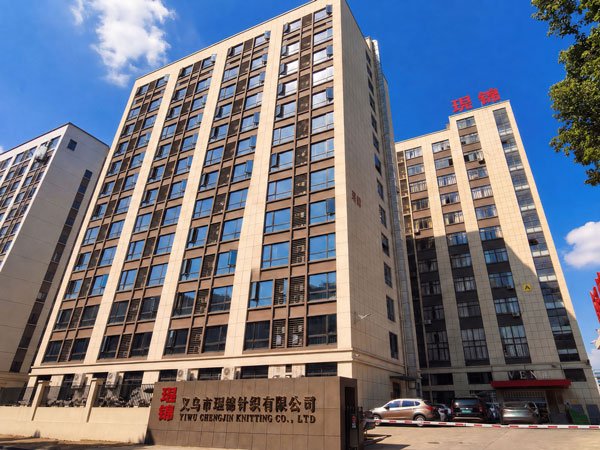
Santoni seamless knitting workshop and activewear quality inspection at MOVEVOX manufacturing base
150K–200K Managed monthly delivery capacity across core & satellite network.
Target Buyer Fit

Tailored Sourcing Solutions for Growing and Established Activewear Brands

MOVEVOX designs its production systems for B2B buyers who prioritize product consistency, specification discipline, and scalable capacity over cut-rate, unverified trading brokerages.

Established Brands

Built for brands requiring complete Tech Pack execution, strict POM tolerance management, and verified factory audit compliance. We ensure bulk orders replicate approved physical benchmarks across continuous quarterly collections.

  • Strict adherence to measurement charts
  • Support for third-party audits (SGS/ITS)
  • Controlled capacity scaling without unapproved transfer

DTC Apparel Labels

Designed for DTC brands scaling fast across multiple seasonal drops, requiring flexible trial order MOQs combined with rapid replenishment capabilities. We combine seamless and cut-and-sew under one unified window to simplify collection launches.

  • 100 pcs seamless / 150 pcs cut-and-sew MOQ
  • Multi-SKU development sharing fabric platforms
  • Fast sample turnaround within 5 to 10 days

Importers & Distributors

Engineered for commercial buyers managing high-volume, multi-container programs across international markets. We provide centralized procurement for core yarns, unified AQL inspection protocols, consolidated carton packing, and seamless forwarder handover.

  • Predictable scheduling via centralized PMC
  • Complete export and carton breakdown docs
  • Stable pricing structures for annual repeat POs

Marketplace Operators

Structured for brand sellers requiring flawless packaging execution, exact SKU barcode labeling, individual warning-printed polybags, and reliable FBA warehouse delivery compliance without packaging errors.

  • 100% SKU label and FNSKU scanning accuracy
  • Squat-proof testing to minimize return rates
  • Rapid replenishment for winning ASINs
Operational Metrics

MOVEVOX Manufacturing Facts & Operational Capacity at a Glance

All figures reflect our core owned facility and controlled satellite manufacturing operations, verified through real factory records and active capacity planning.

28 Santoni Machines

Italian electronic seamless knitting circular machines installed in our core base.

6,000 m² Production Base

Multi-floor technical operations space located in Fotang, Yiwu, Zhejiang Province.

5 QC In-House Quality

Full-time QC personnel led by an 8-year activewear quality assurance manager.

5–10 Days Sample Lead Time

Standard development turnaround from confirmed Tech Pack to completed physical samples.

150K–200K Monthly Capacity

Managed stable monthly delivery volume across core manufacturing and 8 satellite plants.

Data reflects verified baseline manufacturing capacity as of 2026; single-order execution ranges typically between 300 and 50,000 pieces across customized activewear programs. Explore our full manufacturing infrastructure for technical details.

Risk Mitigation

Eliminating the Four Critical Risks in Custom Activewear Sourcing

Most apparel sourcing failures occur because suppliers separate prototype sampling from industrial mass manufacturing. Here is how MOVEVOX protects your brand integrity.

Risk 01: Quality Drift

Sample-to-Bulk Quality Drift

Problem: Prototype fits perfectly, but mass production suffers from seam bursts, tight waistbands, or loose ankles.

Impact: High consumer return rates, negative reviews, and damaged brand reputation on major sales channels.

MOVEVOX Control: We enforce Specification Freezing and physical PP Sample locking before issuing any bulk cutting authorization.

Zero Drift Protocol
Risk 02: Material Variance

Fabric Batch & Color Inconsistency

Problem: Repeat orders arrive with different hand-feel, shade variations, or sheer fabric that fails squat tests.

Impact: Sets cannot be sold together, customer dissatisfaction rises, and reorder predictability is completely lost.

MOVEVOX Control: All custom fabric lots undergo mandatory GSM weighing, 4-way stretch testing, Lab Dip approval, and opacity verification.

Verified Dye Lots
Risk 03: Fragmentation

Multi-Vendor Management Chaos

Problem: Managing separate vendors for seamless, cut-and-sew, logos, labels, and packaging leads to communication breakdowns.

Impact: Misaligned delivery dates, mismatched brand trims, and nobody taking accountability when defects occur.

MOVEVOX Control: One single project manager coordinates design conversion, trim procurement, dual-system production, and final QC.

Single Accountability
Risk 04: Subcontracting

Uncontrolled Subcontracting Risks

Problem: Audited factories secretly pass purchase orders to unvetted home workshops to meet compressed peak deadlines.

Impact: Massive quality variations, failed social compliance standards, and serious brand ethical liabilities.

MOVEVOX Control: We manage production exclusively through our owned facility and 8 contractually bound, auditable satellite plants.

100% Traceable
Engineering Framework

How Does MOVEVOX Engineer Consistent Quality in Activewear Manufacturing?

MOVEVOX controls activewear manufacturing through an integrated engineering framework that bridges technical product development with industrial production. By combining owned Italian Santoni knitting technology, precision cut-and-sew lines, and centralized raw material management, we transform customer Tech Packs into stable, repeatable bulk production standards.

1. Pre-Production DFM & Tolerance Alignment

Every style undergoes manufacturability review, POM cross-checks, and fabric elasticity calculations before cutting or programming begins. Read our manufacturing guides for details.

2. Physical Benchmark Locking

Approved pre-production samples (PP Samples) serve as the legal quality benchmark across all manufacturing cells and inspection checkpoints.

3. Multi-Stage Gate Inspections

5 dedicated QC staff conduct incoming fabric tests, first-article checks, in-line audits, and AQL 2.5 final inspections before cartoning.

4. Closed-Loop Traceability & CAPA

Every production batch is linked to material lots, machine logs, and QC records, ensuring immediate root-cause correction if deviations arise.

Why It Matters: Consistent activewear production requires engineering discipline at the yarn and pattern level, not just sorting defects at the packing stage.
Core Capabilities

Six Core Manufacturing Capabilities Under One Managed Supply Chain

We provide comprehensive private-label execution capabilities, ensuring every phase from yarn selection to final packaging remains strictly controlled under unified technical standards.

⚙

Santoni Seamless Knitting

Operating 28 Italian Santoni seamless circular machines in our core production base. Specializing in engineered body-mapping, zoned compression, ribbed structures, and breathable mesh zones with low-barrier sampling starting from 100 pcs/style.

✂

Precision Cut-and-Sew Assembly

Equipped with 24 specialized sewing machines including 4-needle 6-thread Flatlock, overlock, and coverstitch. Expert handling of high-stretch synthetic fabrics, multi-panel stitching, and ergonomic waistbands starting from 150 pcs/style.

📏

Pattern & Fit Engineering

Professional pattern-makers converting customer Tech Packs, reference samples, or sketches into production-ready patterns. Strict measurement chart review, grade rule validation, and dynamic fit testing for international sizing.

🧶

Raw Material & Dyeing Sourcing

Unified procurement of premium Nylon/Spandex, Polyester/Spandex, recycled fibers, and buttery-soft fabrics. In-house testing for GSM weight, 4-way stretch recovery, shrinkage, opacity, and custom Pantone dyeing.

🏷

Branding & Trim Customization

Complete private-label execution covering heat transfer, high-density silicone print, screen printing, embroidery, woven main labels, compliant care labels, hangtags, barcodes, and custom polybags.

🏭

Scalable Capacity Network

Combining our owned core factory with 8 audited satellite facilities across Yiwu and Guangzhou. Centralized PMC scheduling and quality dispatch ensuring prototype precision scales smoothly to 50,000+ pieces.

Quality Protocol

Five Mandatory Quality Inspection Gates Across Every Production Batch

Our QC department operates independently from production management, with full authority to halt lines, mandate reworks, or reject materials that fail approved specifications.

Gate 01

Raw Material IQC

Every incoming roll of fabric and yarn lot is tested before entering cutting or seamless knitting.

  • GSM tolerance ±5%
  • 4-way stretch recovery
  • Colorfastness check
Gate 02

Pre-Production Freeze

Technical review locking final measurement charts, BOM details, trim placements, and PP Sample benchmarks.

  • Tech Pack confirmed
  • PP Sample sealed
  • Marker shrinkage checked
Gate 03

First Article Check

The first completed garment off each active line undergoes full dimensional measurement and construction audit.

  • 100% critical POM verified
  • Stitch density (SPI) check
  • Logo coordinate audit
Gate 04

In-Line Inspection

Continuous roaming patrols checking active workstations, seamless machines, and sewing units for process deviations.

  • Skip stitch & tension audit
  • Seamless knitting holes
  • Symmetry balance check
Gate 05

Final AQL Release

100% visual finishing inspection followed by random sampling audits under customer-designated AQL standards prior to cartoning.

  • AQL 2.5/4.0 measurement
  • Barcode & SKU scan audit
  • Carton mark verification
Defect Containment & CAPA: Defective items are immediately quarantined. When non-conformance exceeds acceptable thresholds, our Quality Lead initiates a formal Root Cause Analysis and Corrective Action Plan (CAPA) before goods can be released for shipment. Review our detailed Quality Guides for inspection checklists.
Consistency Benchmark

How We Guarantee Mass Production Matches Your Approved Sample

An approved prototype is not just a showcase garment; it represents the binding technical baseline for our entire cutting, knitting, sewing, and inspection workflow.

Sealed pre-production sample compared directly with mass production activewear garment on measurement table

Physical Sample Retention & Workshop Locking

We retain duplicate physical sealed PP Samples in our quality assurance room and directly at line workstation boards. Operators, technicians, and QC personnel reference the exact physical garment throughout all manufacturing stages.

Six Consistency Control Criteria

  • Dimensional Tolerances: Bulk measurements follow strict POM tolerances (Seamless ±2.0 cm, Cut & Sew ±1.5 cm) aligned with your approved sample.
  • Fabric Hand-Feel: Sourced from verified yarn suppliers and cross-checked against the sealed reference swatch for softness and weight.
  • Logo Position Coordinates: Governed by laser-marked placement templates matching exact X/Y coordinates from approved artwork.
  • Seam Strength: Flatlock and overlock tensions are calibrated to match the stretch elasticity and tensile durability of the prototype.
  • Color Accuracy: Custom-dyed fabrics and trims are verified under standard D65 lighting to eliminate multi-panel shading variances.
  • Packaging Precision: Custom labels, size tags, barcodes, and polybags follow the exact physical package approved during sampling.
Workmanship Standards

Precision Workmanship Standards for High-Stress Activewear Zones

Activewear requires specialized sewing and knitting engineering to endure repetitive high-intensity movements without chafing, twisting, or seam blowouts.
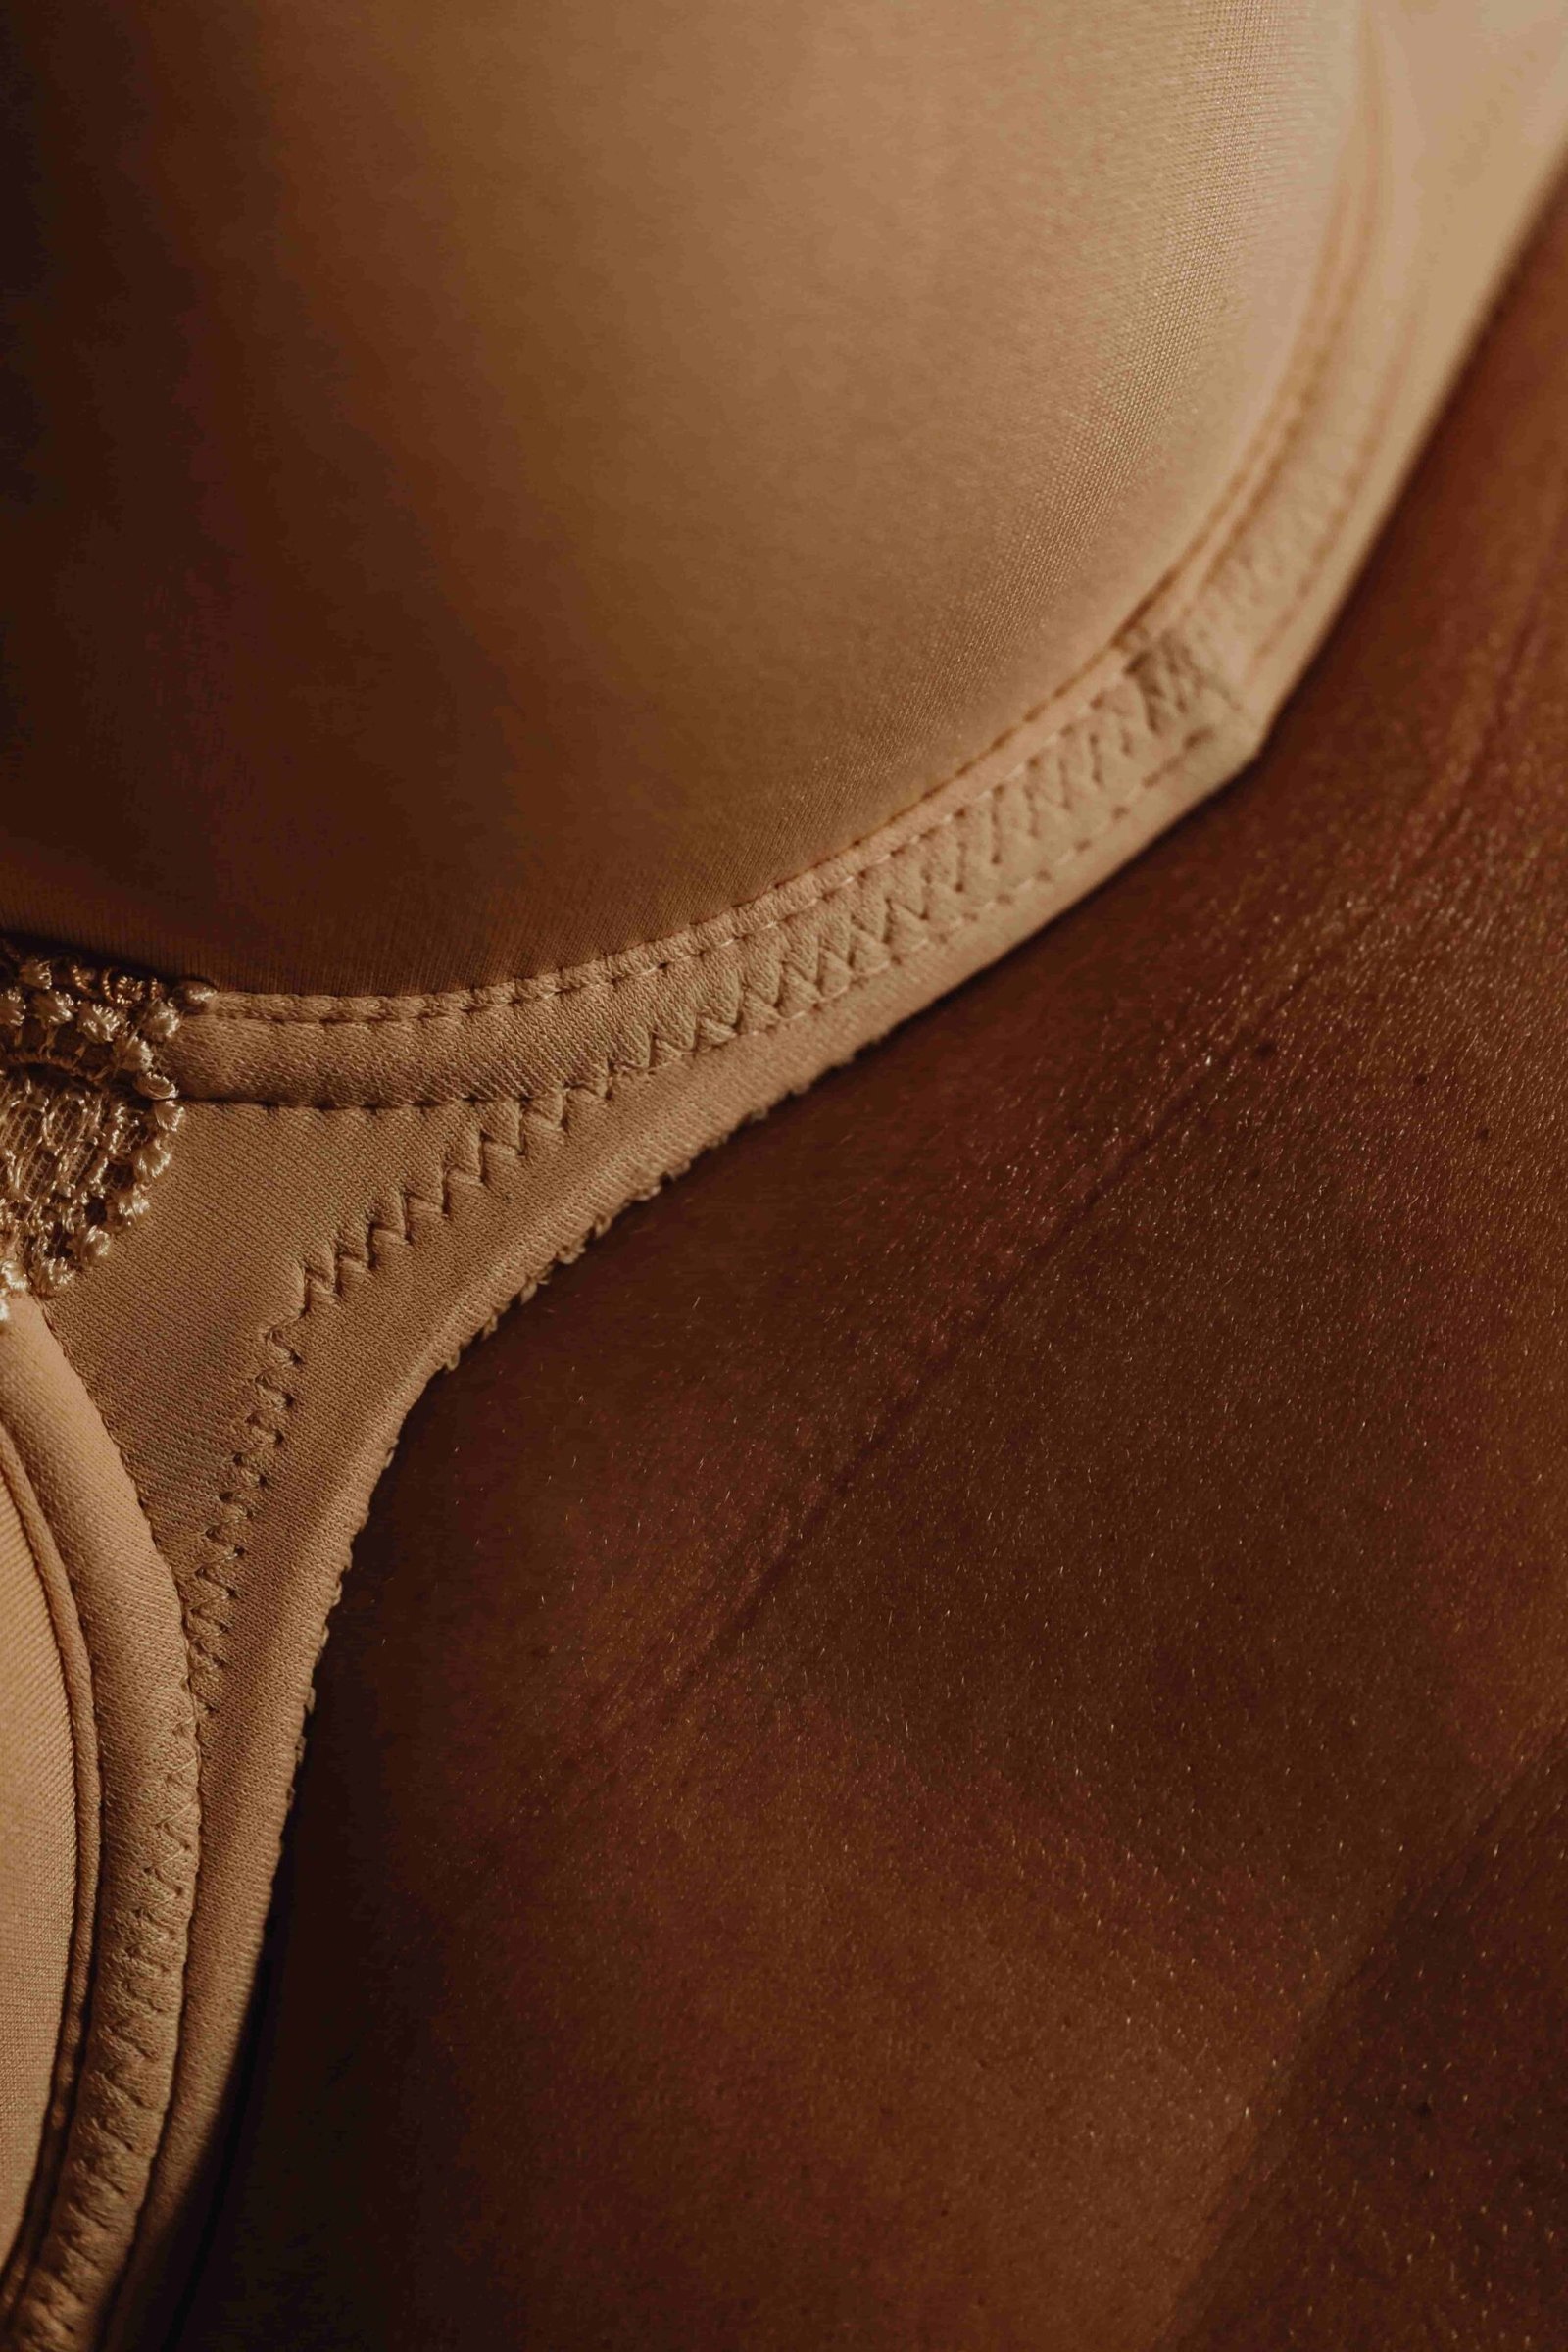
Macro close-up of 4-needle 6-thread Flatlock stitching on high-stretch yoga leggings inseam

4-Needle 6-Thread Flatlock

Ultra-flat, low-profile seam construction with high tensile stretch, minimizing skin friction during deep stretches and workouts.

Inseams & Underbands
Overlock seaming on synthetic activewear panels showing balanced tension and edge encasement

Elastic Overlock Seaming

High-elasticity multi-thread overedging that expands naturally with high-spandex synthetic fabrics without snapping stitches.

Side Panels & Sleeve Joins
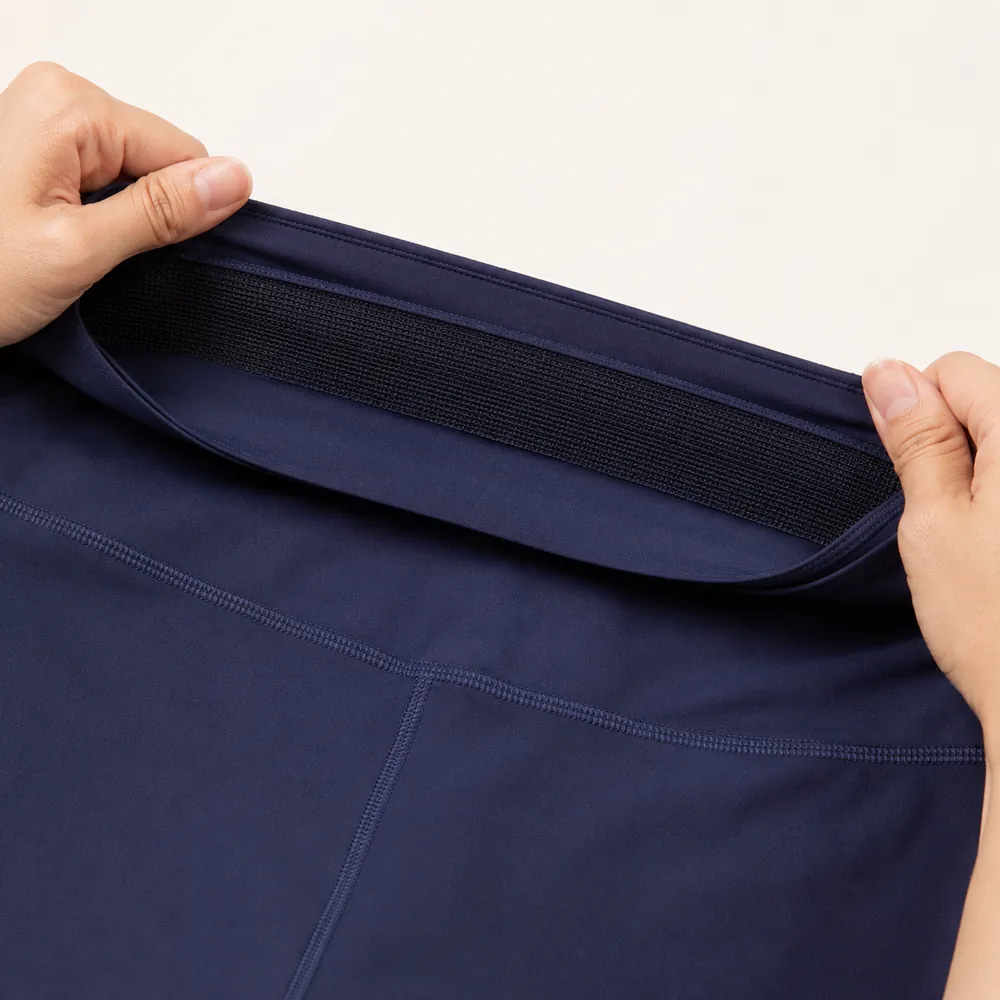
Double-layer yoga leggings waistband construction with interior stabilization support

Double-Layer Bonded Waistband

Ergonomic high-waisted construction utilizing inner stabilization mesh or bonded edges to eliminate rolling and slippage.

Yoga Leggings Waistbands
Reinforced diamond crotch gusset stitching on athletic shorts to distribute movement stress

Reinforced Diamond Gusset

Precision-sewn triangular or diamond crotch inserts distributing dynamic multidirectional stress during squats and lunges.

Active Shorts & Tights
Engineered seamless knitting density transition from supportive ribbing to breathable mesh

Engineered Seamless Density

Computer-programmed stitch density transitions moving smoothly from compressive ribbing to micro-ventilation mesh without seams.

Seamless Bra & Tops
Coverstitch hem finishing on activewear training t-shirt showing flexible exterior lines

Clean Coverstitch Hemming

Flexible double-needle hem finishing providing clean exterior lines while allowing total opening expansion during wear.

Active Tops & Hems
Laboratory Testing

Verifiable Physical & Chemical Testing Protocols for Export Markets

MOVEVOX aligns raw material selection and garment performance with recognized international testing protocols to ensure target market safety, durability, and retail compliance.

4-Way Stretch & Recovery

Purpose: Verify fabric elongation and return recovery under continuous movement.

Standard: ASTM D2594 / D3107 testing cross-grain and length-grain elasticity cycles.

Target: ≥90% Recovery

Opacity & Squat-Proof Test

Purpose: Ensure zero fabric transparency and white-out under extreme body stretching.

Standard: AATCC TM203 light blocking evaluation combined with physical squat strain checks.

Verified Non-Sheer

Colorfastness Validation

Purpose: Prevent color bleeding, migration, and staining during intense sweat and laundry.

Standard: AATCC TM61 (washing), AATCC TM8 (crocking), and AATCC TM15 (perspiration).

Grade 4.0+ Fastness

Dimensional Stability

Purpose: Control length and width shrinkage across multiple home wash and dry cycles.

Standard: AATCC TM135 fabric shrinkage and AATCC TM150 garment stability testing.

Tolerance: ±3% to ±5%

Pilling & Abrasion Resistance

Purpose: Evaluate surface fuzzing resistance against gym equipment and thigh friction.

Standard: ASTM D4970 Martindale pilling tester operated under specified cycle loads.

Grade 3.5–4.0 Standard

Chemical Compliance (RoHS/REACH)

Purpose: Verify restricted substance compliance for European and North American customs.

Standard: Tested under RoHS 2.0 Directive (EU) 2015/863 and REACH Annex XVII phthalates limits.

Reports TST20250405148E / 150E
Product Architecture

Custom Activewear Product Range Engineered for Private Label Brands

Explore our core production categories across seamless knitting and cut-and-sew manufacturing, built with verified 4-way stretch fabrics and durable activewear constructions.
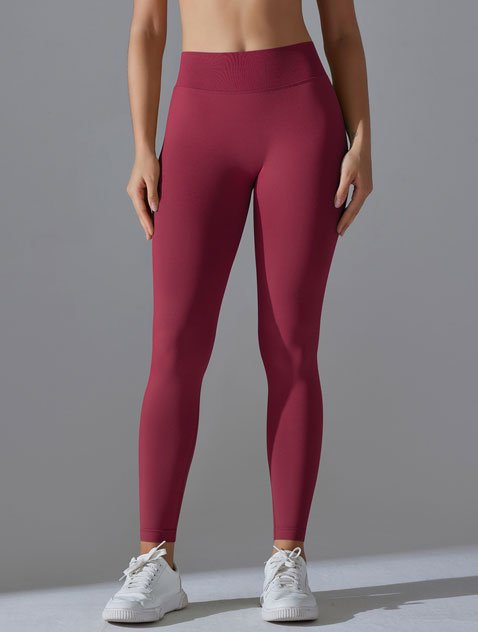
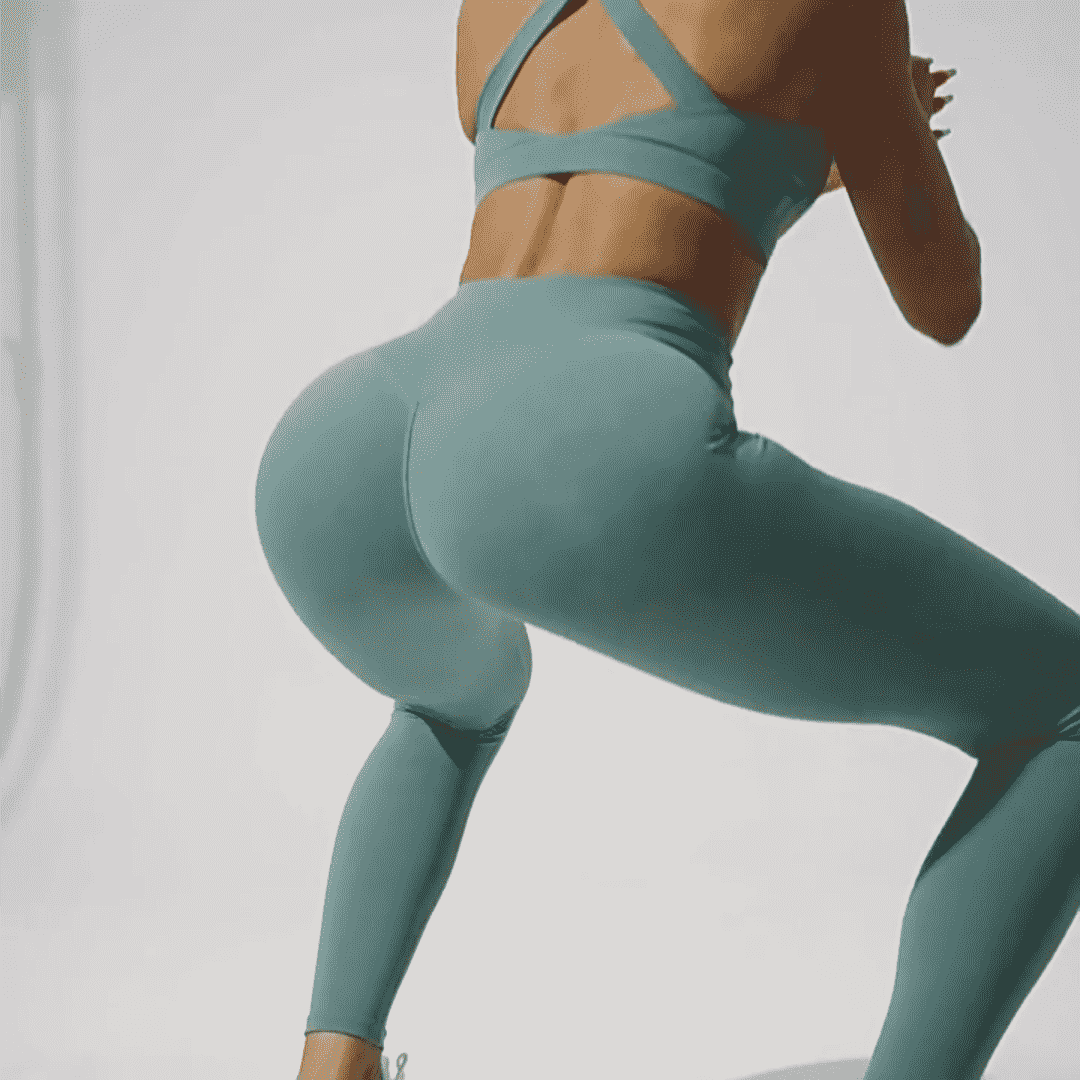
High-waisted private label yoga leggings with seamless waistband and 4-way stretch fabric

Yoga Leggings

No-front-seam waistbands, diamond gussets, and squat-proof 4-way stretch Nylon/Spandex.

MOQ: 100/150 pcs
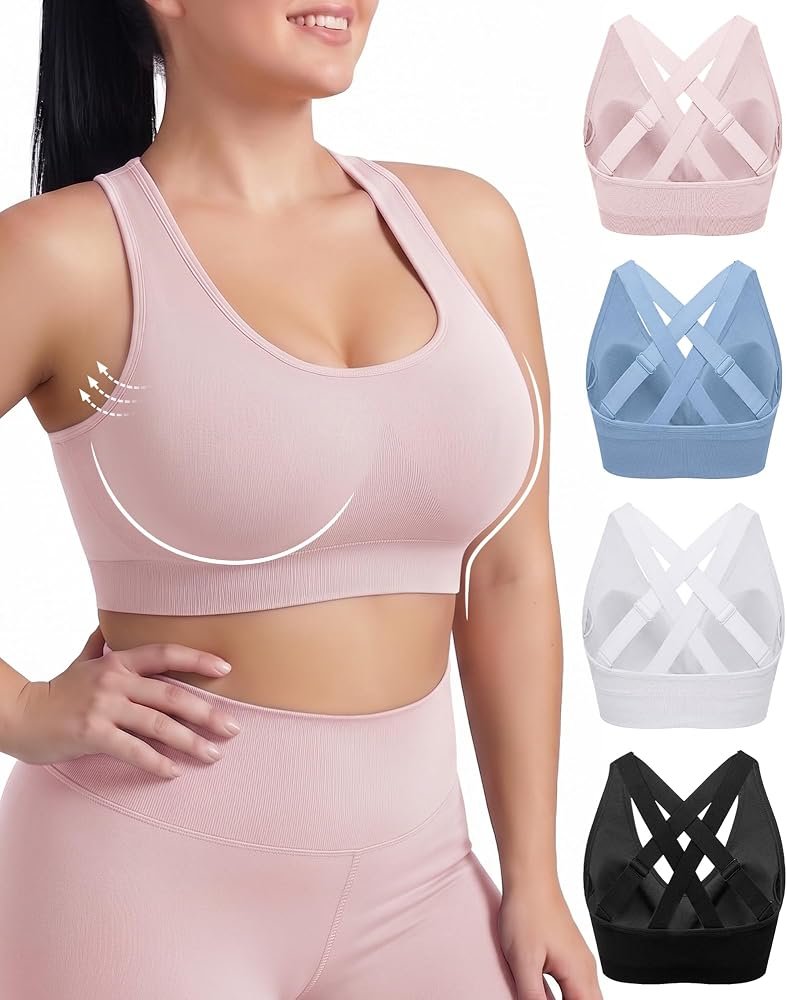
Medium to high support custom sports bra with racerback design and removable pads

Sports Bras

Custom supportive structures featuring racerback, cross-back, and removable padding systems.

Med-High Support
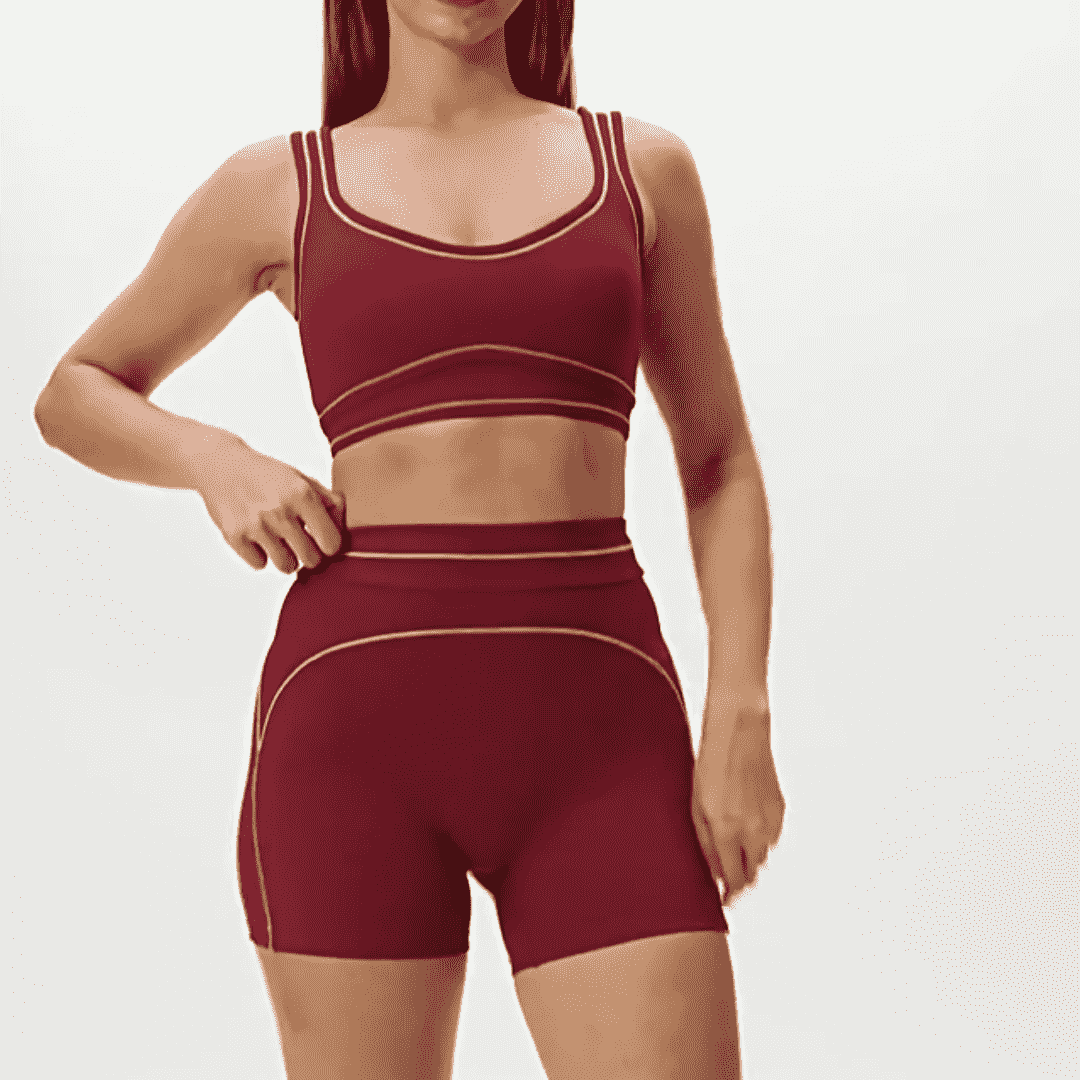
Matching seamless gym workout set with zoned ribbing and dyed-to-match fabric

Seamless Sets

Matching bra and legging combinations sharing identical dyelots, compression, and rib textures.

Santoni Seamless
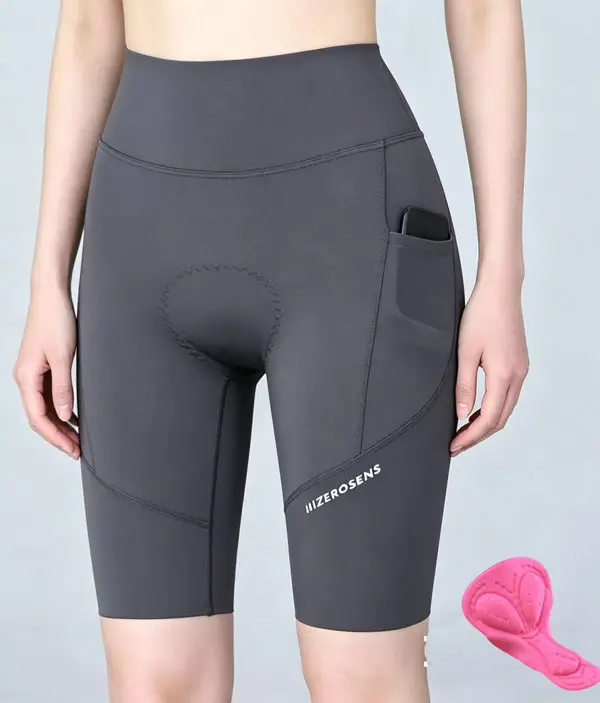
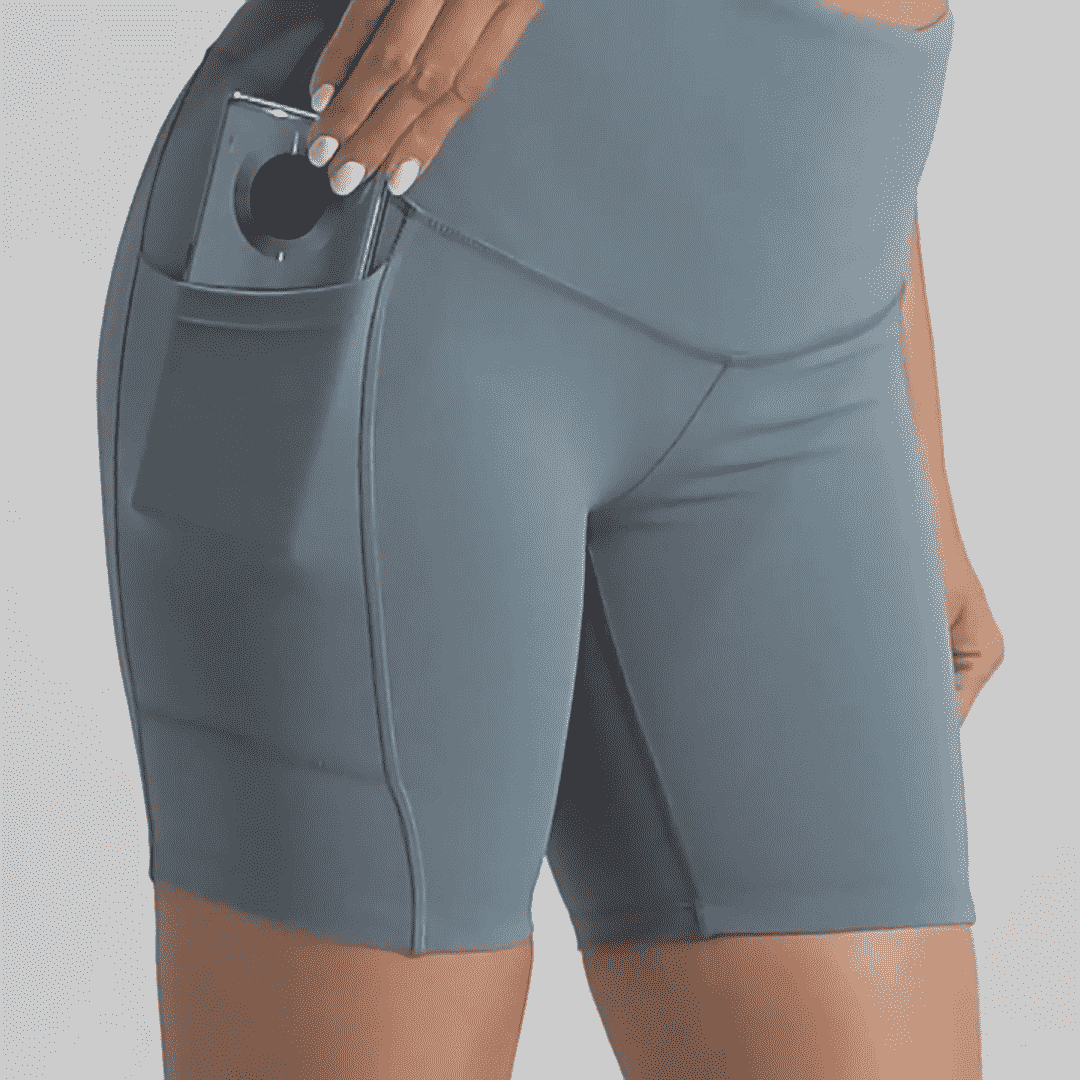
Custom biker and yoga shorts with high-elasticity leg bands to prevent ride-up

Active Shorts

High-elasticity 4" to 8" inseam active shorts engineered to prevent leg-band ride-up and rolling.

Anti-Chafing Inseam
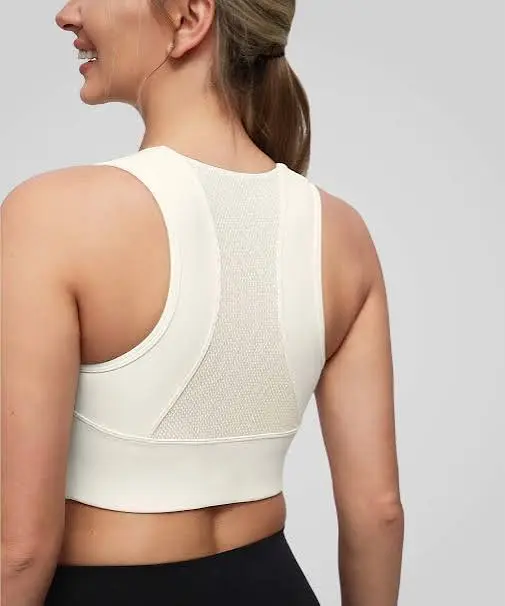
Fitted lightweight active tank top with breathable moisture-wicking synthetic fabric

Active Tank Tops

Breathable crop and regular length tanks with optional built-in shelf bra support.

Buttery-Soft Feel
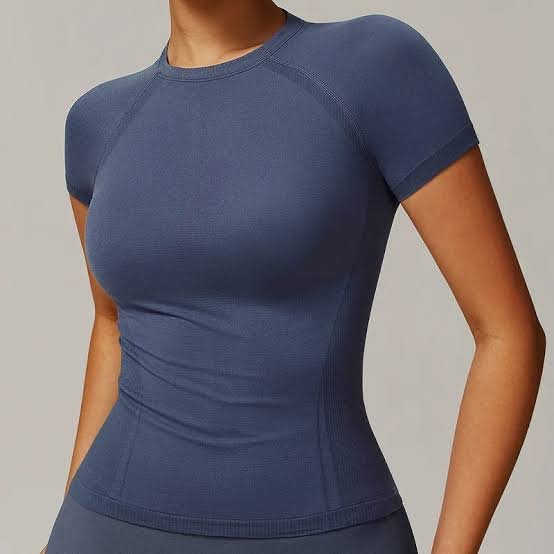
Ergonomic training workout t-shirt with Flatlock stitching and quick-dry technology

Training T-Shirts

Ergonomic workout tees constructed with Flatlock seaming and engineered body-cooling mesh panels.

Quick-Dry Poly/Span
Fitted long sleeve activewear workout top with thumbhole cuffs and half-zip collar

Long Sleeve Tops

Fitted training tops with thumbhole cuffs, half-zip closures, and strategic ventilation mapping.

Thumbhole Cuffs
Lightweight active jacket with full-zip closure and stretch side panels for layering

Active Jackets

Lightweight full-zip training jackets and studio cover-ups with stretch panels and secure pockets.

Cut & Sew Line
Technical Pattern Engineering

Pattern Making, Negative Ease Engineering and Sizing Tolerances

Activewear pattern development requires advanced understanding of synthetic fabric elongation, recovery, and dynamic body movement across multi-dimensional stretch axes.

Base Size Calibration & Negative Ease Engineering

Activewear fits cannot be engineered using static woven garment formulas. High-stretch synthetic fabrics (typically 18%–30% Spandex) require calculated negative ease to provide core compression without constricting circulation or causing sheer white-out.

  • Body Data Mapping: Establishing baseline waist, hip, inseam, and bust coordinates aligned with target market demographic profiles (US, EU, UK, AU).
  • Fabric Stretch Calculation: Factoring in cross-grain and length-grain modulus to establish proportional negative ease for each specific fabric lot.
  • Dynamic Fit Validation: Testing physical fit samples through dynamic squat, lunge, and arm-raise motions to eliminate waistband rolling and front crotch pulling.
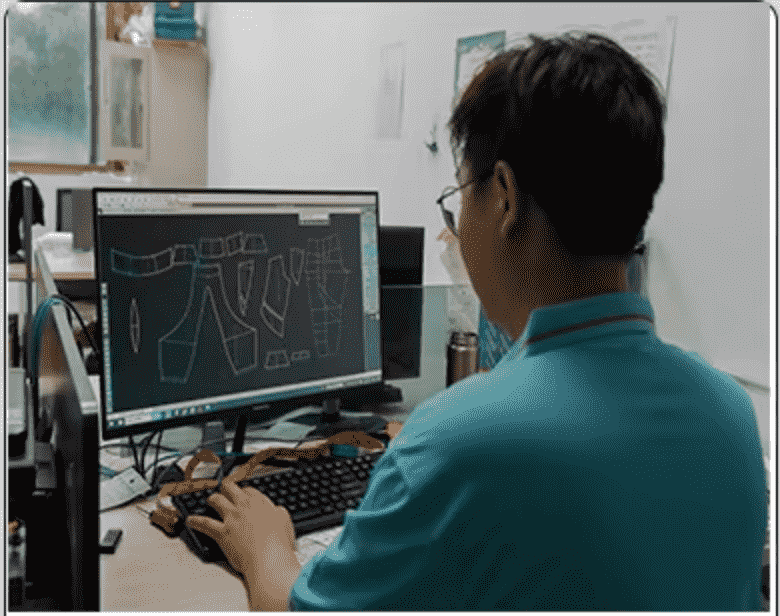
Technical pattern maker adjusting activewear CAD marker and measuring negative ease on sample table

Grade Rule Proportions & Manufacturing Tolerance Control

Extending a base size into a commercial size set (XS to 2XL) requires non-linear grade rule algorithms. Increasing garment dimensions proportionally ensures that larger sizes retain core support while smaller sizes do not lose structural compression.

  • Standard Measurement Tolerances: Enforcing strict manufacturing tolerances (Seamless controlled within ±2.0 cm, Cut & Sew within ±1.5 cm).
  • Size Set Sample Audits: Verifying multi-size sets physically before mass cutting to ensure strap width, rise depth, and pocket locations scale correctly.
  • Master Spec Freezing: Uploading finalized pattern CAD files and verified measurement charts directly into production workstations.
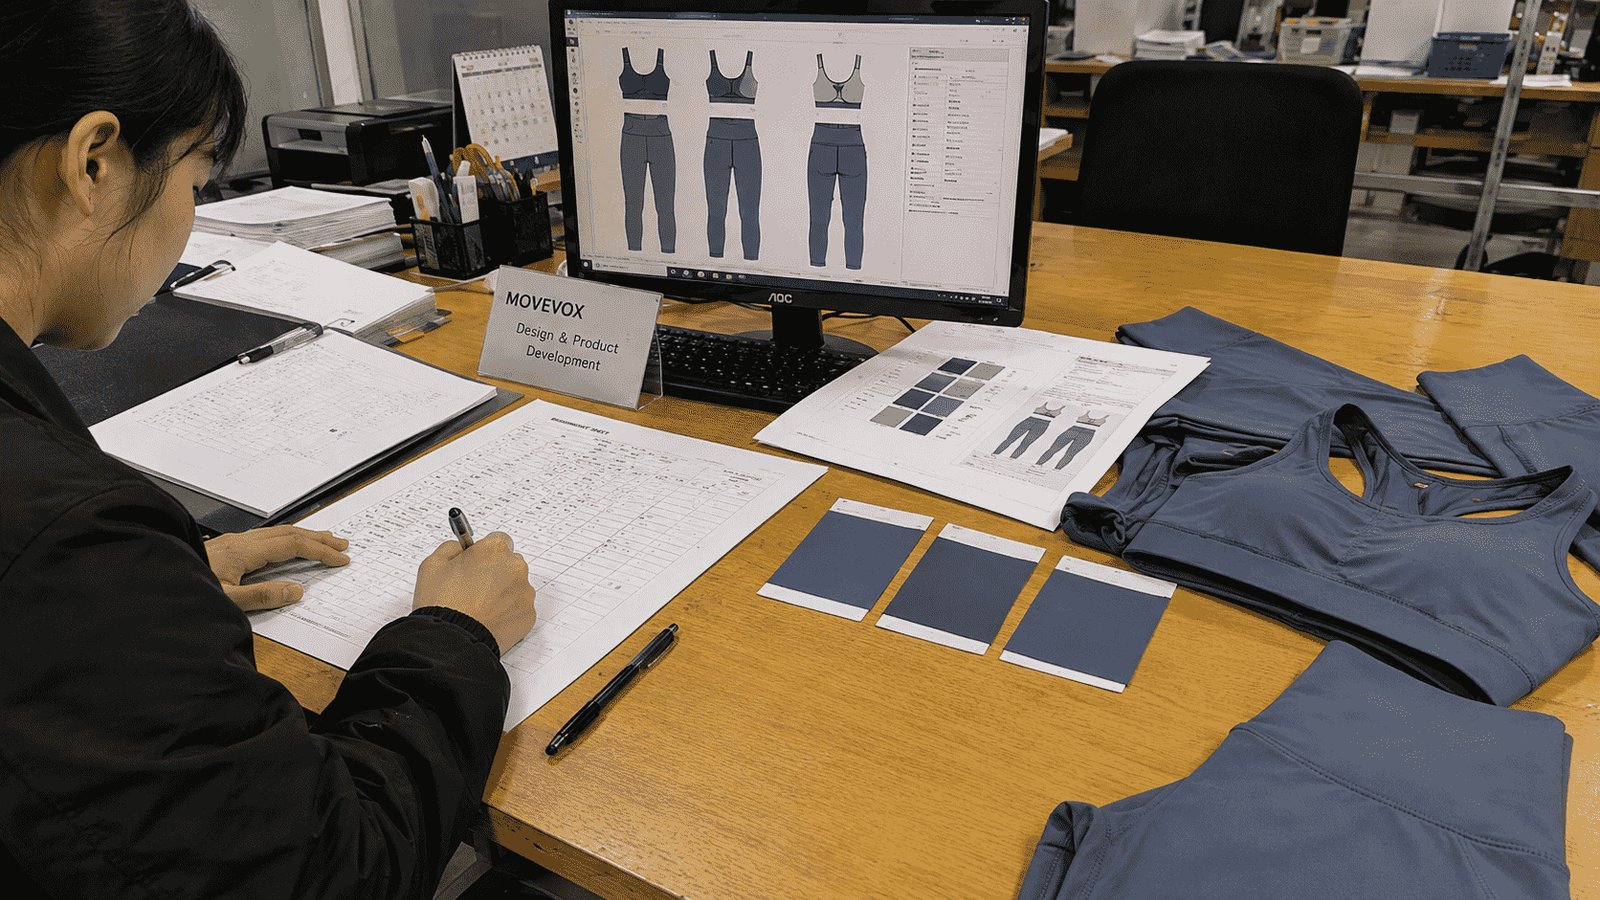
Multi-size activewear size set graded from XS to XXL layered to demonstrate proportional grade rules
Audit Readiness

Complete Transparency for Brand Vendor Qualification and Audits

We provide international sourcing teams and compliance officers with fully verifiable operational facts, official entity documentation, and open audit access.

Verified Legal & Facility Facts

Legal Entity

Yiwu Chenjin Import And Export Co., Ltd.
Credit Code: 91330782MA2HWGPQ6N

Facility Address

Fotang Base, Yiwu
No. 97 Xiazhang Village, Fotang Town, Yiwu, Zhejiang

Facility Size

6 Floors, ~6,000 m²
Dedicated seamless knitting, sewing, and QC zones

Management

Jerry (General Manager)
8+ Years international activewear supply chain experience

Audit & Testing Support Protocols

MOVEVOX welcomes scheduled factory visits and live video tours for technical and social compliance evaluations. We accommodate third-party pre-shipment inspections from SGS, Intertek, Bureau Veritas, and QIMA, ensuring full commercial alignment with your internal vendor compliance manual.

  • RoHS 2.0 Directive (EU) 2015/863 tested compliant (Report TST20250405148E)
  • REACH Annex XVII Phthalates tested compliant (Report TST20250405150E)
  • Live video factory audits supported via Zoom / Google Meet
Supply Chain Architecture

Our Controlled Supply Chain: Core Manufacturing Hub & Satellite Network

MOVEVOX eliminates the risks of unmanaged subcontracting through a transparent hybrid production model that combines owned core manufacturing with audited satellite workshops.

Core Central Hub

MOVEVOX Production Hub (Yiwu)

Handles 100% of product development, Tech Pack translation, prototype sampling, Santoni seamless knitting, pilot orders, first-article locking, and final AQL quality inspection.

Seamless Satellites

6 Yiwu Satellite Facilities

Dedicated seamless knitting partner plants providing controlled overflow capacity under unified yarn and program specs.

Cut & Sew Satellites

2 Guangzhou Satellite Facilities

Specialized cut-and-sew garment facilities handling complex multi-panel stitching, jackets, and specialized synthetic knits.

Material Partners

Yarn & Fabric Mills

Direct supply partners providing verified Nylon/Spandex, Polyester/Spandex, and GRS-certified recycled material options.

Branding Partners

Logo & Trim Specialists

Dedicated facilities for high-density silicone molding, heat transfer printing, woven labels, and elastic tape production.

Fulfillment

Packaging & Logistics Hub

Centralized barcode scanning, SKU labeling, custom polybag packing, 7-layer export cartoning, and forwarder handover.

Unified Accountability Rule: Regardless of whether a specific process occurs at our core base or a dedicated satellite line, MOVEVOX manages all Technical Packs, BOM inputs, raw material purchases, production schedules, and final QC releases under a single point of commercial and legal accountability.

Commercial Terms

Transparent MOQ Tiers, Sample Lead Times & Production Calendars

We maintain clear, realistic minimum order quantities and development milestones, allowing brands to validate new designs without excessive inventory exposure.

Manufacturing Program Standard MOQ Specification Sample & Bulk Lead Time Commercial Terms & Policies
Seamless Activewear
(Leggings, Bras, Shorts)
100 pcs per style
(50 pcs/color, min 20 pcs/size)
Sample: 5–10 working days
Bulk: 20–35 days
Sample fee: $100/pc (100% credited against bulk order invoice upon reaching 500 pcs).
Cut-and-Sew Apparel
(Tops, Tights, Jackets)
150 pcs per style
(50 pcs/color, min 10 pcs/size)
Sample: 5–10 working days
Bulk: 20–35 days
Sample fee: $120–$150/pc (100% credited against bulk order invoice upon reaching 1,000 pcs).
Custom Pantone Dyeing
(Custom Fabric Lots)
~400–600 pcs equivalent
(Based on dye vat minimums)
Lab Dip: 3–5 working days
Bulk Dye: 15–20 days
Dye lot approved via physical lab dip swatches under standard D65 light box before bulk dye.
Private Label Trims & Packs
(Bags, Tags, Silicone Logos)
500–1,000 pcs per trim
(Follows trim supplier MOQ)
Trim Sample: 3–7 working days
Bulk: Runs parallel
Excess custom packaging inventory stored securely in our warehouse for repeat orders.
Proven Case Study

Case Study: Rapid Sample Approval to 3x Surge Production for a European DTC Brand

How MOVEVOX supported a Spanish activewear brand from a 1,200-piece initial trial order to bi-monthly repeat orders and an urgent 3x seasonal surge delivery without quality compromise.

Client Profile & Operational Challenge

Client Profile: A direct-to-consumer activewear brand based in Spain, expanding across European online channels and local trade shows, requiring high-density silicone logo branding and custom frosted zip polybags.

The Challenge: The brand required 1,200 custom pieces completed and shipped within 15 days via split air and sea freight. High initial demand led them to place a second 1,200-piece repeat order in week two before first shipment arrival.

MOVEVOX Engineering Solution

We finalized sample details via video conferences and 5–7 day DHL express sampling, locked silicone heat-transfer parameters, organized double-line dedicated production, and maintained a dedicated buffer inventory of 1,500 pieces per core color to support rapid reorder cycles.

  • 100% in-line garment inspection and 7-layer export cartoning
  • Split air/sea freight logistics arriving 2–3 days ahead of deadline
  • Activated satellite capacity during a May surge that tripled normal volume
Timeline 15 Days

Initial 1,200-piece custom batch completed on schedule.

Delivery 2–3 Days

Goods arrived early ahead of promotional launch date.

Surge Capacity 3x Volume

Seamlessly handled 3x promotional volume spike without delay.

Partnership 2 POs/Mo

Ongoing bi-monthly replenishment and new style releases.

“MOVEVOX delivered exactly what they promised on the prototype. Even when our May promotional demand tripled, their buffer fabric stock and dedicated production lines met our delivery timeline flawlessly.”

Cost Architecture

Total Cost of Sourcing: Calculating True Supply Chain Risk vs. Initial Unit Price

A unit quote that is $0.30 cheaper often results in significantly higher landed costs once defective batch reworks, air-freight emergency penalties, and customer return rates are factored in.

Cost & Risk Factor Low-Tier Unvetted Suppliers MOVEVOX Controlled Manufacturing System
Initial Quoted Price Appears 5%–10% lower upfront; frequently adds hidden surcharges post-PO. Itemized, transparent quotation tied to exact fabric, trim, and packaging specs.
Sampling Iterations 3 to 5 sample rounds due to weak Tech Pack comprehension; delays launch by months. Disciplined DFM review achieving approved prototypes within 1 to 2 iterations.
Fabric Batch Variations Uncontrolled dye lots causing multi-panel shading and sheer non-squat-proof fabric. Mandatory lab dips, GSM verification, and 4-way stretch recovery testing.
Defect & Rework Costs High AQL failure rates (burst seams, uneven waistbands) discovered upon delivery. 5-stage QC gates with pre-shipment AQL 2.5 inspection ensuring zero bulk drift.
Emergency Air Freight Production delays force expensive air-shipping to avoid missing retail launch dates. Centralized PMC milestone tracking achieving ≥95% on-time factory handover.
Customer Return Rates Negative e-commerce reviews and high return rates caused by sizing inconsistency. Calibrated negative ease and strict POM tolerance control protecting brand equity.
The Bottom Line on Sourcing Cost: MOVEVOX minimizes your Total Cost of Sourcing through front-end DFM reviews, verified raw materials, dedicated in-house QC gates, and single-window accountability. By ensuring first-time right production, we protect your channel profit margins.
Industry Clarity

Six Common Myths in Activewear Manufacturing vs. Technical Production Realities

Technical clarity prevents commercial misunderstandings. We believe in educating our brand partners on the physical and industrial realities of activewear production.

Myth 01: Seamless Assembly

"Seamless means 100% zero sewing."

Production Fact: Circular Santoni machines knit tubular bodies; crotch gussets, waistbands, hems, and straps still require precision Flatlock and overlock assembly.

Technical Reality: Seamless reduces seam lines by ~70%, but relies on expert sewing for final finishing.

Myth 02: Fabric Weight

"Higher GSM automatically guarantees squat-proof."

Production Fact: Opacity is determined by yarn fineness, knit density, and Spandex elongation; a loose heavy knit can still shear out during deep squats.

Technical Reality: AATCC TM203 light-blocking and physical stretch tests are required per color.

Myth 03: Color Matching

"A Pantone code looks identical on all fabrics."

Production Fact: Nylon, Polyester, and Spandex absorb dyes differently; physical Lab Dip approvals under D65 lighting are mandatory for each specific fabric base.

Technical Reality: Digital screen color codes must be physically matched on actual production swatches.

Myth 04: Zero Tolerance

"Apparel factories can achieve 0 mm variance."

Production Fact: High-stretch knitted fabrics naturally fluctuate; professional brands operate within realistic POM tolerances (±1.5 cm for cut & sew, ±2.0 cm for seamless).

Technical Reality: Quality control measures relaxed garments against calibrated POM standards.

Myth 05: Market Sizing

"A US Medium directly converts to European Medium."

Production Fact: Demographic body shapes differ in rise depth, torso length, and hip-to-waist ratios; market-specific grading rules must be engineered.

Technical Reality: Custom base patterns and grade rules must be built for your target market.

Myth 06: Mill Certificates

"A mill's certificate covers the garment factory."

Production Fact: Raw material certificates only apply to yarn or fabric; finished garment factory audits and chemical tests require explicit entity scope.

Technical Reality: MOVEVOX provides authentic finished product testing (RoHS/REACH) per product line.

FAQ

Frequently Asked Questions on Activewear Manufacturing & Quality Control

Get direct answers to common commercial, technical, and operational questions regarding custom activewear production with MOVEVOX.

Are you a direct manufacturing factory or a trading company?

MOVEVOX is an integrated manufacturing and supply-chain company. We own and operate our core manufacturing facility in Fotang, Yiwu, equipped with 28 Santoni seamless machines and 24 specialized sewing units, while coordinating 8 long-term satellite factories for scalable bulk capacity. Formal contracts and commercial operations are executed directly under our legal entity, Yiwu Chenjin Import And Export Co., Ltd.

How do you protect our proprietary designs and Tech Pack IP?

We execute bilateral Non-Disclosure Agreements (NDAs) prior to receiving proprietary files. Your Tech Packs, custom prints, unreleased prototypes, and order quantities are kept strictly confidential and never shared with other clients, displayed at public trade shows, or sold as stock goods.

Can we conduct third-party quality inspections before shipment?

Yes, we fully accommodate third-party pre-shipment inspections (PSI) conducted by agencies such as SGS, Intertek, Bureau Veritas, or QIMA, as well as your designated internal QC auditors. Production is released for export handover upon passing agreed inspection standards.

What happens if mass production deviates from our approved PP sample?

MOVEVOX operates under single-window accountability. If mass production deviates from agreed POM tolerances or confirmed physical standards, we initiate immediate root-cause containment, providing rework, replacement, or commercial resolution at our own responsibility.

Is the sample development fee refundable or deductible?

Yes. Standard sampling fees ($100 for seamless, $120–$150 for cut-and-sew) are 100% credited against your bulk invoice once the mass production order reaches agreed volume thresholds (500 pcs for seamless, 1,000 pcs for cut-and-sew).

Why is custom Pantone dyeing MOQ higher than garment MOQ?

Fabric dye vats and seamless yarn dye lots operate on physical minimum liquid volume constraints (typically ~400–600 pcs equivalent). For smaller trial orders below dye-vat thresholds, we provide in-stock factory color swatches matching your target palette.

How is your 20 to 35-day bulk lead time calculated?

Lead time begins once all Tech Pack specifications are frozen, the physical Pre-Production (PP) Sample is formally approved, bulk fabric arrives, and initial deposit payment is confirmed. Specialized custom-milled fabrics or complex trims may require dedicated timeline alignment.

Can we use our own nominated freight forwarder for export delivery?

Yes. We routinely handle FOB, EXW, and CIF terms, coordinating directly with your designated international freight forwarder and providing accurate Packing Lists, carton breakdowns, and shipping marks for customs clearance.

Can you develop activewear if we only have sketches or a physical sample?

Yes. Our product development team can reverse-engineer physical reference samples or translate sketches into complete production Tech Packs, grading rules, and physical prototypes.

What are your standard business communication hours and response times?

Our international project management team operates daily from 07:00 to 24:00 China Standard Time (CST, UTC+8), providing direct English communication and guaranteed 2-hour response windows during business hours.

Direct Contact

Connect Directly with MOVEVOX Project & Technical Leads

Connect directly with dedicated project managers and technical leads to discuss your activewear specifications, commercial terms, and development schedule.

✉

Official RFQ Email

Best for sending complete Tech Packs, formal RFQs, BOM sheets, and commercial contract inquiries.

Email: lzmwwx@gmail.com

Guaranteed 2h Response
💬

Direct WhatsApp Chat

Ideal for rapid project clarification, sampling photo updates, quick fabric inquiries, and technical messaging.

WhatsApp: +86 151 0555 8361

Daily 07:00–24:00 CST
📹

Live Video Factory Tour

Schedule a live video walk-through via Zoom or Google Meet to view our Santoni seamless machines and QC tables.

🏢

On-Site Factory Visit

Visit our multi-floor production facility in Fotang, Yiwu, for on-site technical reviews and physical audits.

Request MOQ & Sample Details

START YOUR PROJECT

Ready to Develop Your Private Label Activewear Line?

Tell us what you want to develop, your estimated quantity and customization needs. We will review the details and suggest the next practical step for sampling, quotation or production.

Helpful details to include:

Request MOQ & Sample Details