Protecting Global Activewear Brands with Disciplined Quality Architecture
MOVEVOX implements an engineering-driven quality management system across our 6,000㎡ Yiwu facility. Backed by 5 full-time QC specialists, an in-house performance testing lab, and verified RoHS, REACH, and GRS compliance, we eliminate bulk defects and ensure complete international regulatory conformance under strict AQL 1.5/2.5 benchmarks.
- Disciplined 4-stage inspection workflow covering raw yarns, inline sewing, and export cartons
- In-house physical testing laboratory verifying wash shrinkage, 4-way stretch recovery, and opacity
- 100% dual-head conveyor metal detection combined with batch-level ERP barcode traceability
5 Dedicated QC Specialists, in-house physical lab, and certified RoHS 2.0 / REACH compliance.
What Defines Authentic Activewear Quality Assurance and Regulatory Compliance?
Understanding why technical activewear manufacturing requires rigorous mechanical testing and chemical auditing rather than simple end-of-line garment packing checks.
Authentic activewear quality assurance is an end-to-end preventative discipline encompassing raw fiber analysis, inline kinetic stitch monitoring, stress-to-failure mechanical testing, and batch-level traceability. At MOVEVOX, quality is engineered before cutting rather than inspected after packaging. Our 5-member QA team verifies raw fiber modulus, stitch SPI density, wash shrinkage, and restricted chemical thresholds across all OEM activewear and ODM activewear programs.
Preventative Raw Fiber Auditing
Inspecting incoming yarn and knit fabric rolls under the ASTM 4-Point System to arrest defects before cutting.
Inline Kinetic Tension Monitoring
Calibrating stitch tensions and differential feeds every 2 hours on flatlock and Santoni circular knitting floors.
Stress-to-Failure Physical Testing
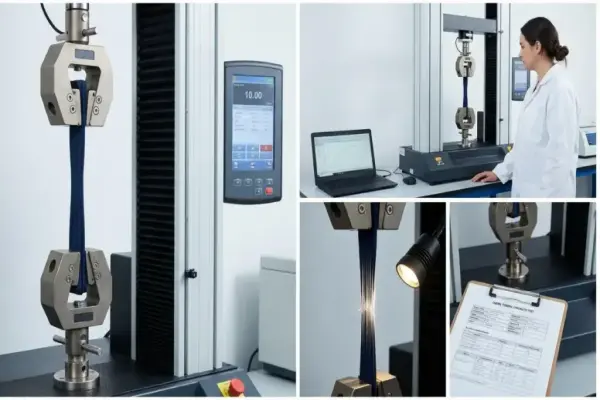
Verifying four-way stretch recovery modulus, seam tensile strength (>180N), and squat-proof opacity in our lab.
100% Foreign Contaminant Screening
Passing every packed garment through dual-probe conveyor metal detectors calibrated to 0.8mm ferrous spheres.
Verified Factory Data Powering Activewear Quality Assurance
Our quality performance is substantiated by dedicated personnel, standardized inspection thresholds, and independent chemical certifications across our Yiwu operations.
Full-time inspectors led by Quality Director Nacy Wu covering IQC, IPQC, FQC, and OQC.
Strict sampling thresholds for major functional and minor aesthetic defects.
Dual-head conveyor metal detection for all garments prior to export carton packing.
Verified compliant under EU RoHS 2.0 and REACH Annex XVII phthalate testing.
Maximum allowable dimensional change after 5 commercial wash and dry cycles.
All quality records, batch inspection logs, and lab reports are archived digitally and retrievable by order number for up to 24 months.
Four Costly Activewear Quality Hazards—And How We Eliminate Them
Sourcing performance activewear presents severe legal, mechanical, and commercial liabilities. Here is how our preventative quality control protocols protect your brand.
Chemical Non-Compliance & Customs Seizure
Risk: Toxic phthalates, banned azo dyes, or excessive heavy metals trigger European or US customs confiscation and heavy regulatory fines.
Our Control: Every batch complies strictly with EU RoHS 2.0 and REACH Annex XVII; suppliers submit verifiable chemical COAs prior to cutting.
Crotch Bursting & Seam Ruptures
Risk: Standard overlock stitching snapping along crotch curves during heavy squats causes viral 1-star reviews on e-commerce storefronts.
Our Control: Enforcing 4-needle 6-thread flatlock assembly, diamond crotch gussets, and computer bartack reinforcements across all performance leggings.
Squat-Through Sheerness & Grin-Through
Risk: Light or pastel yoga tights stretching transparent across glute zones triggers mass product returns and false advertising allegations.
Our Control: Mandatory dual-axis stretch opacity inspection on our backlit testing fixture, holding opacity strictly above 99.5% under tension.
Color Bleeding & Wet Rub Contamination
Risk: Low-grade disperse dyes migrating from dark leggings onto skin or workout equipment leads to severe retail chargebacks.
Our Control: Rigorous laboratory auditing under AATCC 15 and AATCC 61, requiring Grade 4.0 or above for perspiration and wash fastness.
Three-Tier Defect Classification & Production Interception Matrix
We classify defects across three rigorous operational tiers to eliminate ambiguity and prevent substandard garments from reaching packing lines.
Level Red: Critical Defects (Zero Tolerance / 0 Acceptance)
Criteria: Any foreign metal residue (broken needle fragment), presence of restricted RSL substances, fabric holes or laddering, open unstitched seams >5mm, or base POM dimension variance >3.5cm.
Action Protocol: Instant production line stoppage; 100% quarantine of the affected lot; mandatory 8D root-cause investigation before line restart.
Level Yellow: Major Defects (AQL 1.5 Threshold)
Criteria: Skipped stitches on flatlock seams, uneven stitch tension causing fabric puckering, visible shading variance between panels (below Grade 4.0), or logo placement shift >10mm.
Action Protocol: Lot isolated by IPQC; 100% screening of current shift output; technician recalibrates machine tensions and replaces dull needles immediately.
Level Green: Minor Defects (AQL 2.5 Threshold)
Criteria: Removable superficial dust or chalk marks, untrimmed loose thread ends >5mm, minor hangtag placement shift within 5mm, or minor fold crease.
Action Protocol: Defect resolved online at trimming and iron stations; documented in daily shift log to prevent cumulative drift.
The 4-Stage Closed-Loop Quality Control SOP: IQC to OQC
Our quality assurance architecture operates on a 4-gate closed loop. No garment advances to subsequent manufacturing phases without passing designated verification criteria.
Incoming Quality Control (IQC)
10%–20% roll inspection under ASTM 4-point standards; validating yarn lot numbers, fabric GSM weight, four-way stretch modulus, and color lab dips.
Raw MaterialsIn-Process Quality Control (IPQC)
Hourly roving audits across 28 Santoni seamless circular knitting machines and ~24 sewing stations, checking stitch tension and 10–12 SPI densities.
Inline AssemblyFinal Quality Control (FQC)
100% full-piece flat inspection of all finished garments. Checking 8 primary POM dimensions, trimming thread ends, and 100% metal detector screening.
100% Unit AuditOutgoing Quality Control (OQC)
Pre-shipment statistical audit according to AQL 2.5 standards, verifying barcode readability, polybag warning texts, and export carton drop integrity.
AQL 2.5 DispatchIQC Stage: Raw Fiber, Performance Fabric & Trim Verification
Quality begins with rigorous raw material qualification. Every roll of performance knit fabric and spool of synthetic filament is validated before cutting in our custom fabric warehouse.
ASTM 4-Point Roll Audit
We inspect 10%–20% of incoming rolls on motorized inspection machines. Penalty points are assigned per ASTM D5430; rolls exceeding 40 points per 100 square yards are rejected.
Fabric Weight & Width Audit
Circular swatches extracted across edge-to-edge positions are weighed on calibrated analytical balances, enforcing strict ±3.0% GSM tolerance across dye lots.
Elastic Modulus Screening
Fabric test strips are subjected to mechanical extension cycles to verify instantaneous elasticity and 30-minute recovery modulus before markers are created.
Trim & Hardware Testing
Zippers are checked for slide resistance, elastics audited for anti-roll recovery after 5,000 extension cycles, and heat-seal adhesion tested for silicone logos.
IPQC Stage: Inline Knitting & High-Stress Assembly Surveillance
Our In-Process Quality Control operates on rigorous hourly patrol cycles, catching machine drift and operator deviation directly at the workstation.
Seamless Circular Knitting Surveillance
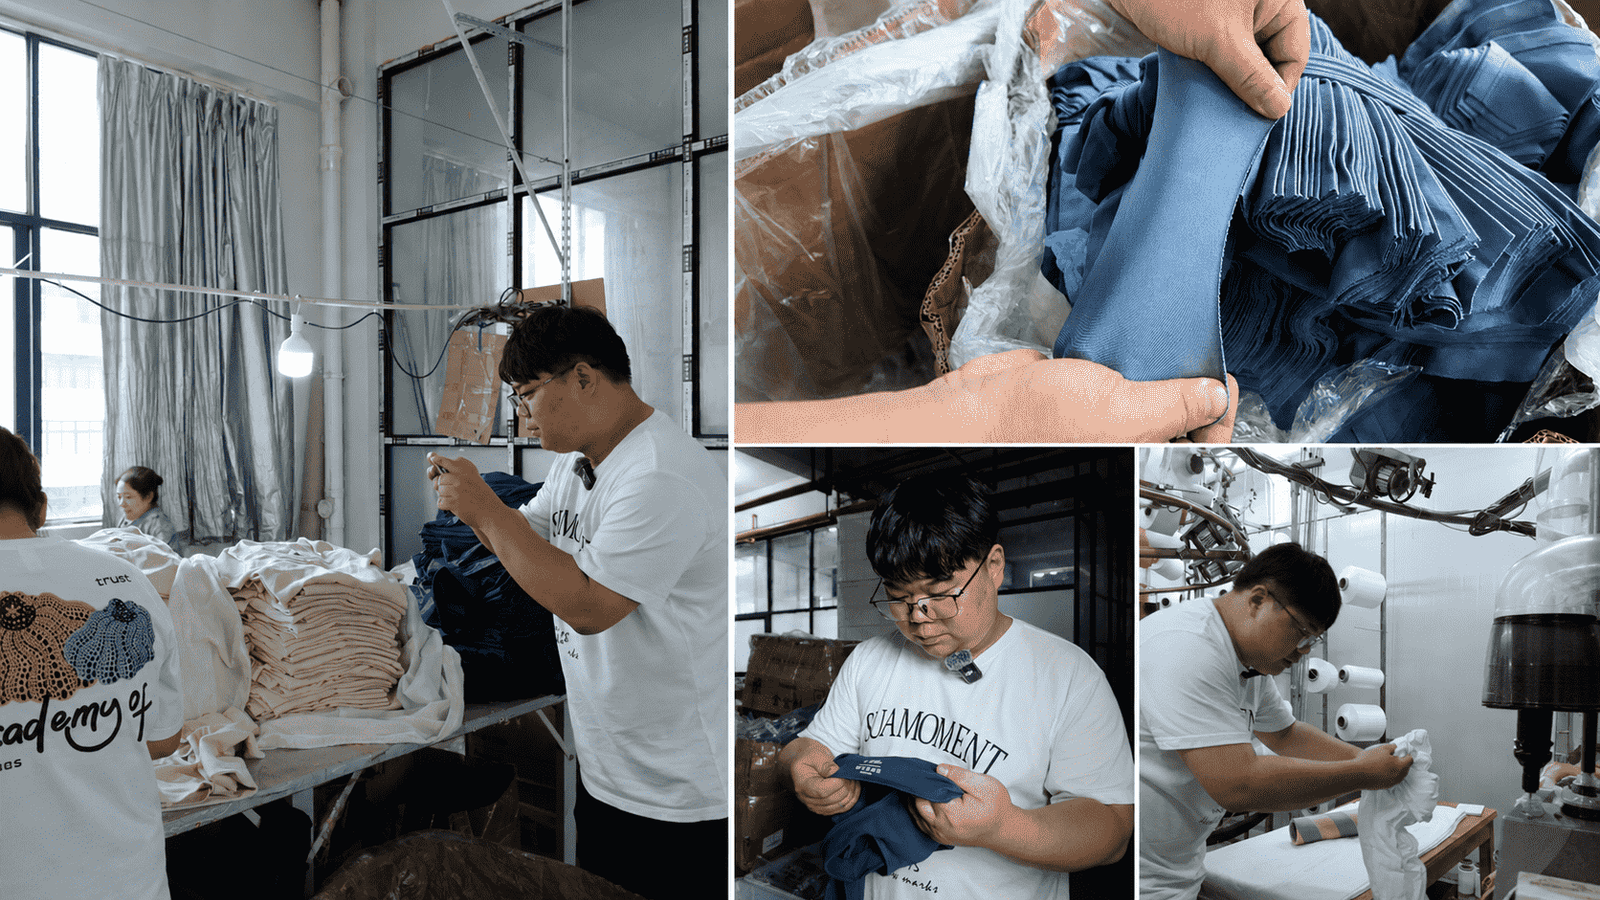
Operating 28 Italian Santoni circular knitting machines, inspectors check the first tubular body piece of every production shift. Tubes are measured for tubular width, tube weight (GSM), and examined under oblique lighting for broken filaments, needle lines, or elastane tension dropouts.
Electronic multi-feed tension controllers are logged every 4 hours to eliminate barre lines and ensure identical left-and-right leg tube compression on seamless activewear collections.
Precision Sewing Line & Stress Point Auditing
Across our ~24 specialized sewing stations (flatlock, 4-thread overlock, and coverstitch), roving inspectors sample completed sub-assemblies every 2 hours. Stitch density is verified with optical magnifying gauges, maintaining 10–12 SPI.
High-stress terminations—including pocket mouths, crotch seam intersections, and waistband joins—are audited for computer bartack reinforcement and pull-tested to ensure seams withstand dynamic athletic loads without cracking.
FQC & OQC Stage: 100% Finished Garment Inspection & Pre-Shipment Audit
Every activewear piece passes through dual independent quality gateways before leaving our Yiwu manufacturing facility.
Flat POM Dimension Audit
Every garment is laid flat on standardized inspection tables under 1,000-lux neutral daylight lighting, verifying 8 critical POM dimensions against approved tech pack tolerances.
Aesthetic & Trimming Review
Operators audit garments for cosmetic flaws—clearing loose threads over 3mm, checking for fabric spots, and confirming thermal silicone logos are free of bubbles or peeling.
Pre-Shipment Statistical Audit
Before dispatch, our Chief Quality Officer conducts a secondary statistical audit according to ANSI/ASQ Z1.4 (ISO 2859-1) Level II, enforcing strict AQL 1.5 Major and AQL 2.5 Minor limits.
Packaging & Barcode Audit
Auditing outer carton burst strength, polybag suffocation warning text compliance, silica gel placement, and 100% barcode scanning readability for rapid client warehouse intake.
In-House Physical Testing Laboratory: Four Core Mechanical Protocols
We maintain a dedicated in-house performance testing laboratory, testing sample swatches and bulk production cut-offs against global athletic wear benchmarks.
Dimensional Stability (AATCC 135)
Method: 5 consecutive commercial laundering and tumble-dry cycles at 40°C.
Benchmark: Dimensional change held strictly within ±3.0% along length and width, preventing customer shrinkage complaints post-purchase.
Perspiration Fastness (AATCC 15)
Method: Immersion in synthetic acidic and alkaline sweat solutions under 37°C incubation for 4 hours.
Benchmark: Evaluated under standardized grayscale; requires Grade 4.0 or above for shade alteration and multi-fiber staining.
4-Way Recovery (ASTM D2594)
Method: Constant-rate tensile extension measuring instant stretch and residual growth after 30-minute relaxation.
Benchmark: Minimum ≥92% elastic recovery rate, eliminating knee bagging, waistband sagging, and fit distortion over time.
Pilling Resistance (ISO 12945-2)
Method: Multi-directional mechanical abrasion testing using standard wool abradant under 9kPa pressure.
Benchmark: Grade 4.0 or above after 2,000 rubs, ensuring fabric surfaces resist pilling from barbell knurling and rough floor contact.
Activewear Quality Benchmark Index: Multi-Dimensional Performance Radar
We quantify the mechanical performance of our core activewear fabric formulations across 6 objective engineering dimensions, providing transparent benchmarks for brand developers.
Elastic Recovery: 94 / 100
ASTM D2594 verified; demonstrates less than 8% residual growth after 500 cyclic stretch pulls, preserving contour memory.
Abrasion Durability: 92 / 100
ISO 12945-2 Martindale surface durability rated at Grade 4.0+, preventing fiber fuzzing against athletic equipment.
Wash Colorfastness: 95 / 100
AATCC 15/61 validated; maintains Grade 4.0–4.5 against domestic wash agitation and synthetic perspiration immersion.
Moisture Dispersion: 90 / 100
AATCC 79 wetting absorption under 2.5 seconds, pulling perspiration across exterior surfaces for rapid evaporation.
Squat-Proof Opacity: 98 / 100
Tested on backlit fixtures under 40% elongation, guaranteeing >99.5% visible light blockage across all stretch zones.
Seam Tensile Strength: 96 / 100
ASTM D1683 flatlock tensile resistance exceeding 180N, providing double the bursting load of conventional overlock joints.
100% Squat-Proof & High-Extension Opacity Testing Protocol
Light or pastel activewear often turns transparent when stretched across glute curves. MOVEVOX implements a dedicated optical testing protocol to guarantee complete modesty across yoga sets and tights.
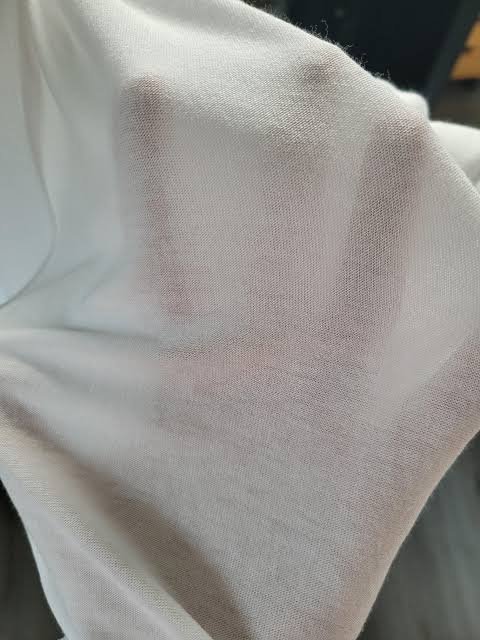
The Sheerness Challenge
When knit fabrics stretch beyond 35% elongation, micro-gaps appear between yarns, allowing skin tones to show through.
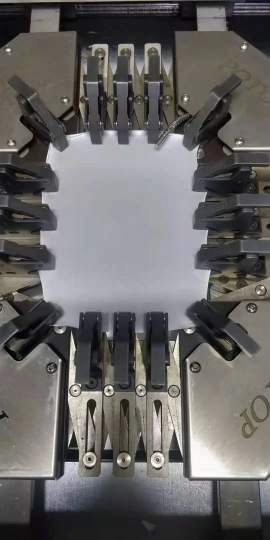
2-Axis Biaxial Extension
Our lab utilizes a mechanical fixture clamping samples under simultaneous 40% crosswise and 30% lengthwise elongation.
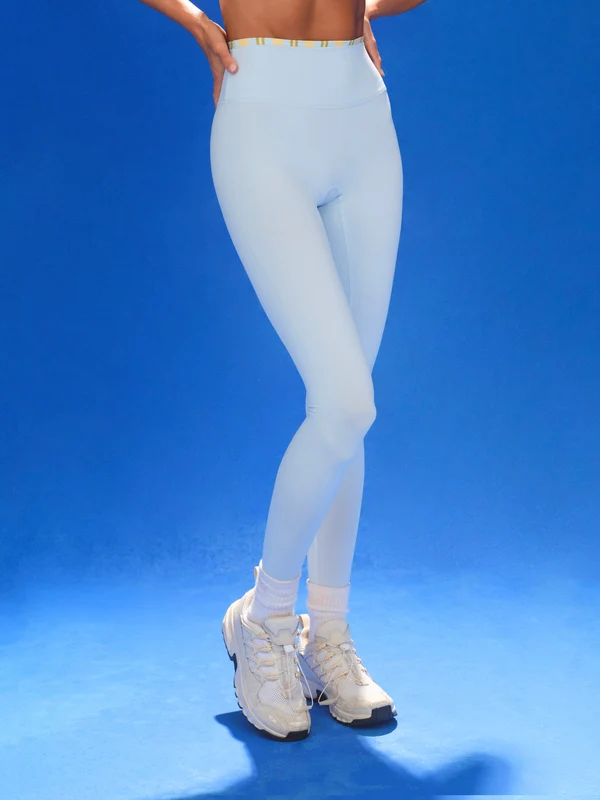
Backlight Lux Audit
Stretched swatches are placed over a 1,500-lux illuminated surface; optical sensors require ≥99.5% total light blockage.
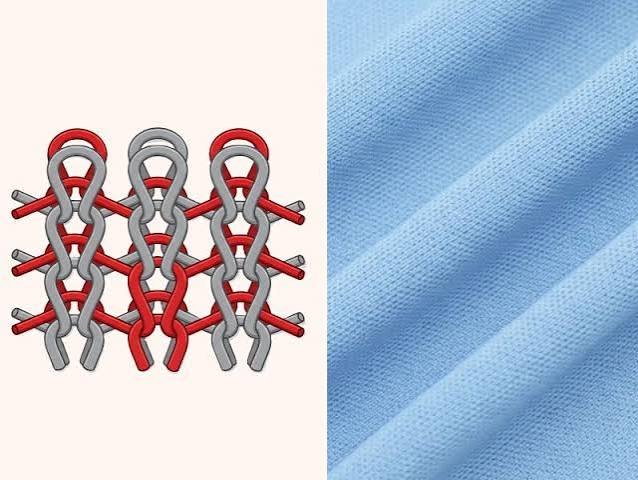
High-Gauge Interlock Solution
We engineer 36-gauge double-knit interlock structures with dope-dyed black elastane cores to block light at the yarn level.
Seam Tensile Load & Anti-Burst Bursting Strength Standards
Activewear seam failures are unacceptable. We engineer our stitch structures to withstand explosive athletic extensions without thread breakage or seam slippage.
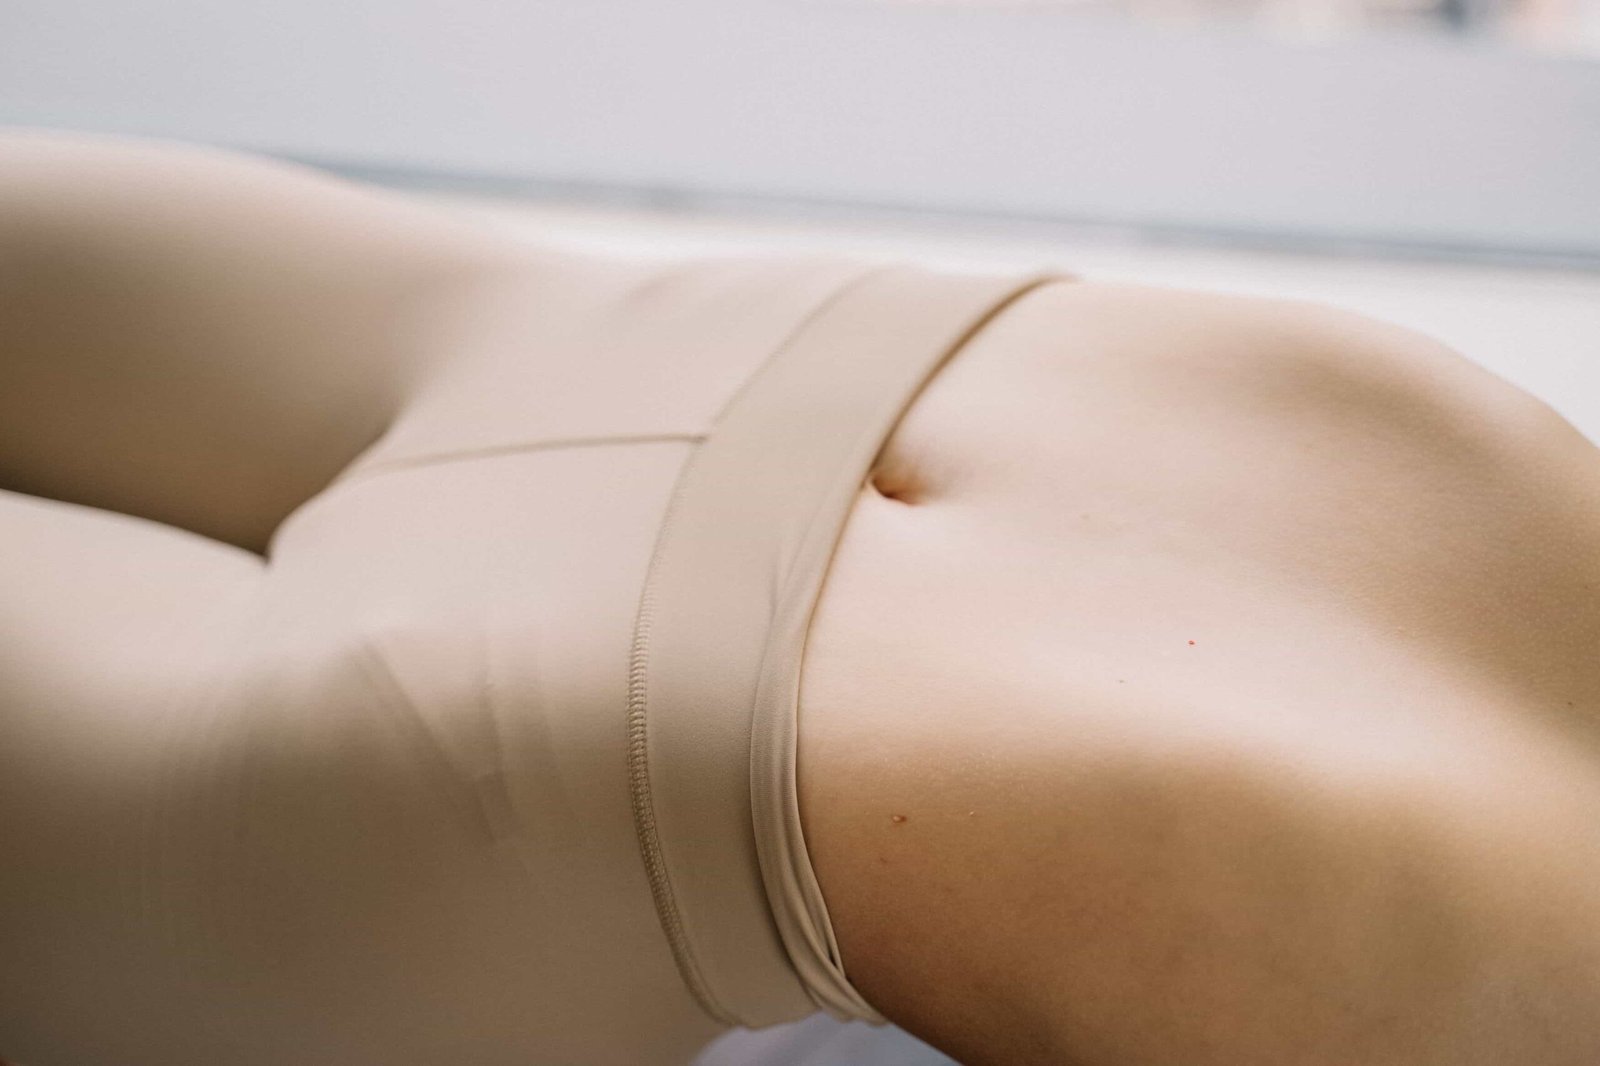
4-Needle 6-Thread Flatlock
Executed at 10–12 SPI to form an ultra-flat, high-elastic seam lying flush against skin, distributing tension across 6 separate thread paths.
Tensile Load Testing (>180N)
Tested under ASTM D1683; our flatlock seams withstand perpendicular tensile forces exceeding 180N, more than double the 80N apparel baseline.
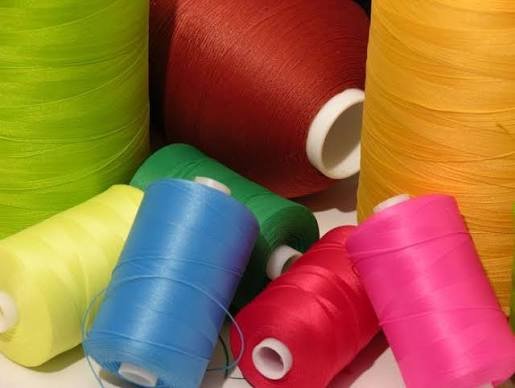
High-Elongation Woolly Nylon
We utilize texturized micro-filament nylon in looper channels, providing over 120% seam elongation that mirrors high-spandex fabric movement.
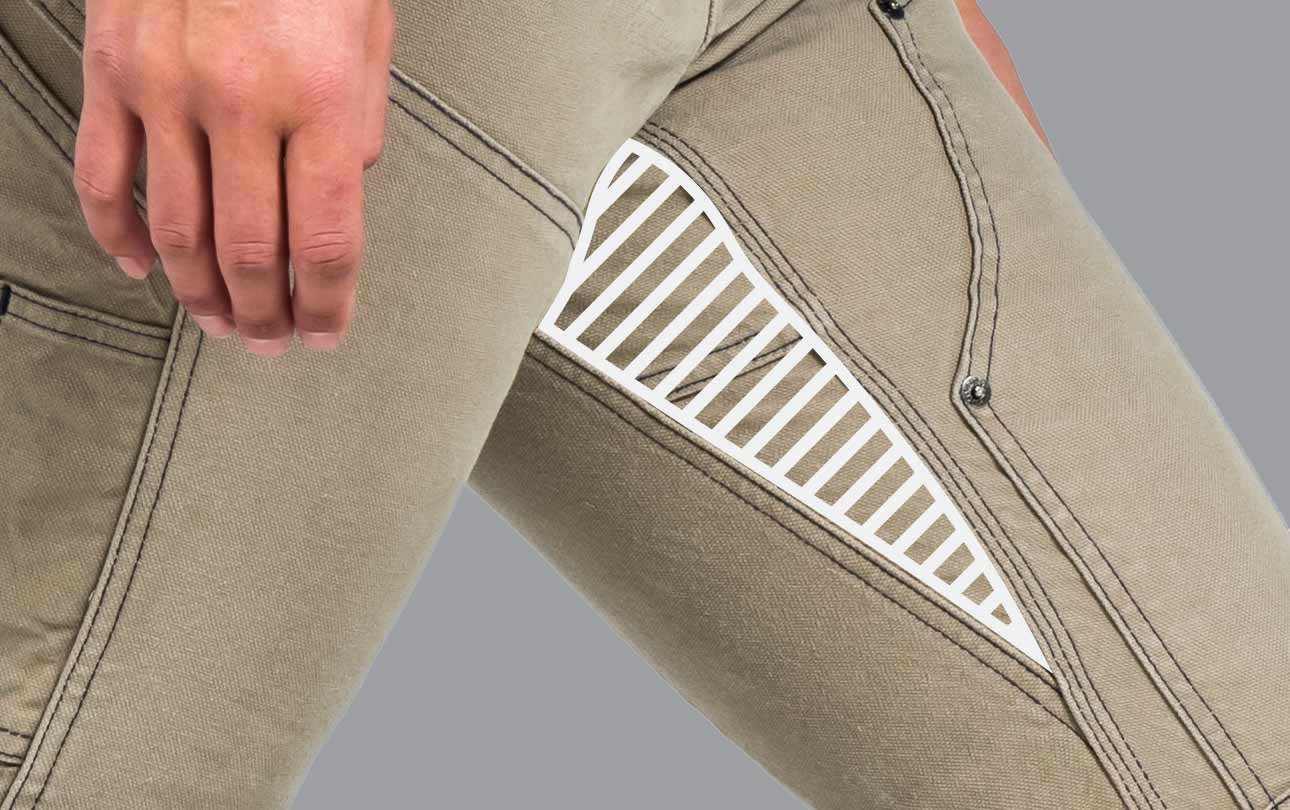
Diamond Gusset Dispersion
Eliminating 4-way cross junctions by inserting an anatomical diamond gusset, redirecting vertical squat loads away from vulnerable groin junctions.
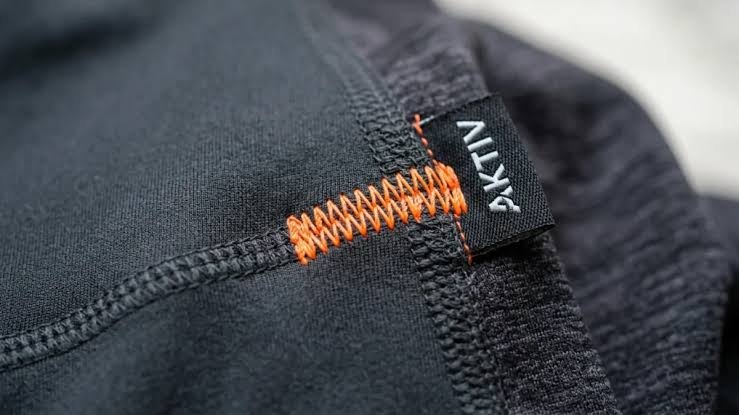
Programmable Bartack Anchors
Heavy-density programmable bartacks applied at pocket corners, side splits, and zipper terminations arrest seam unraveling under shear loads.
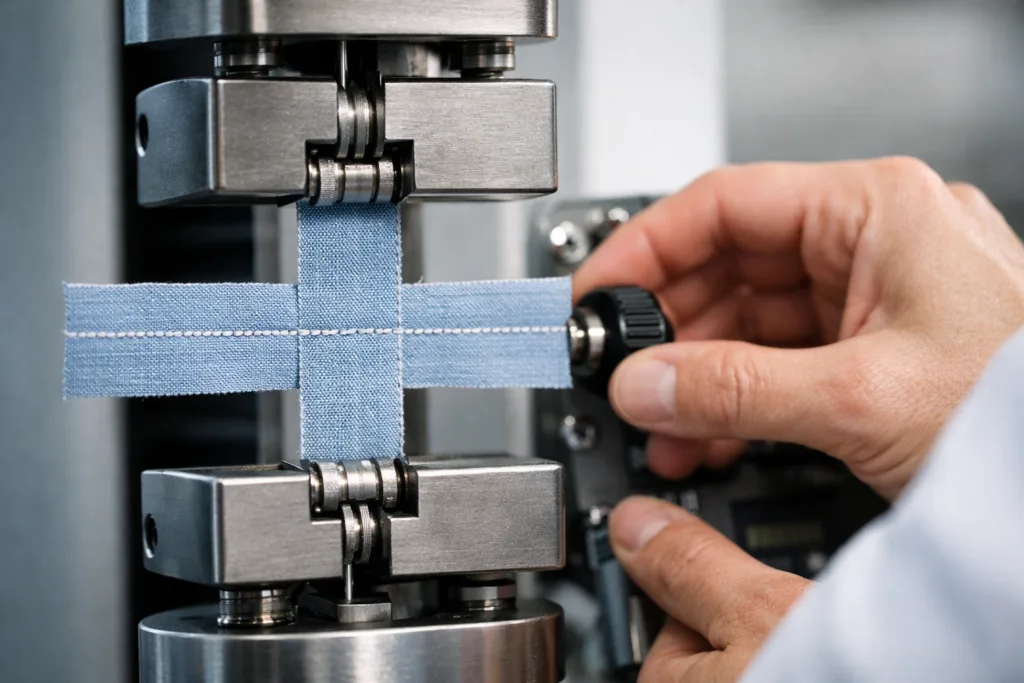
Pneumatic Seam Fatigue Audit
Submitting finished assemblies to cyclic pneumatic expansion chambers to verify zero thread loosening after 1,000 consecutive inflation cycles.
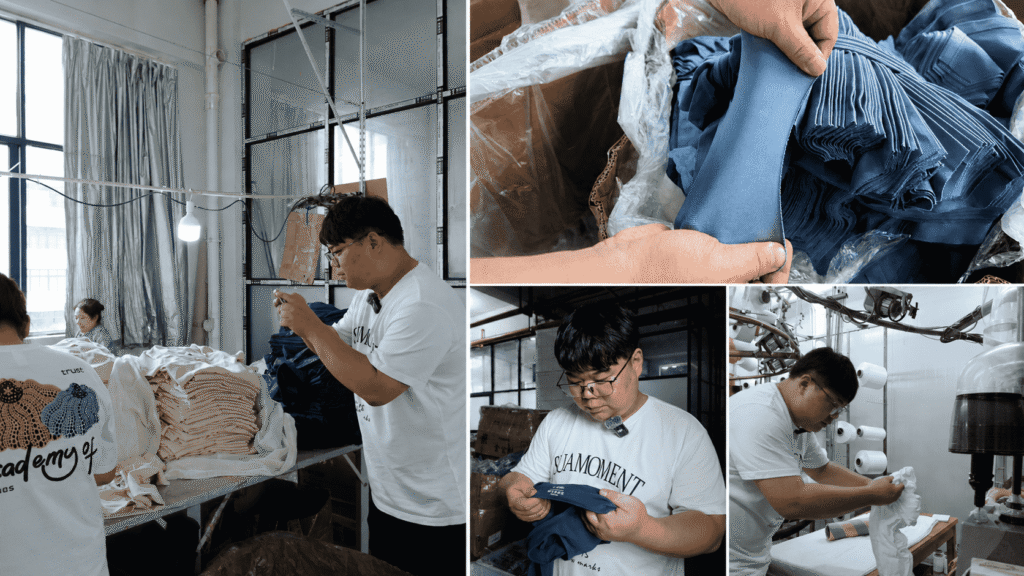
Verified International Chemical & Environmental Compliance Portfolio
We substantiate compliance through independent third-party laboratory test reports, guaranteeing your activewear lines comply with EU and US restricted chemical legislation.
RoHS 2.0 Heavy Metals Safety
Report: TST Report No. TST20250405148E
Certified free of restricted heavy metals (lead, cadmium, mercury, hexavalent chromium) and toxic flame retardants (PBB, PBDE) across synthetic fabrics.
REACH Annex XVII Phthalates
Report: TST Report No. TST20250405150E
Formulated with zero banned phthalate plasticizers (DEHP, DBP, BBP, DINP, DIDP, DNOP), ensuring complete chemical safety for next-to-skin activewear.
Global Recycled Standard
Scope: Certified Post-Consumer Polyamide
Sourced through certified recycled yarn spinning partners, supporting official Transaction Certificates (TCs) for recycled nylon and polyester lines.
OEKO-TEX Standard 100 Aligned
Scope: Class I / II Dyeing & Trims
Core performance dyeing mills and auxiliary trim partners operate certified dye facilities compliant with OEKO-TEX Standard 100 with zero carcinogenic azo dyes.
Zero-Tolerance Restricted Substance List (RSL) Control Thresholds
MOVEVOX maintains a strict Restricted Substance List (RSL) governing every chemical auxiliary, pigment, and polymer entering our production chain.
| Restricted Chemical Group | Test Standard | Regulatory Limit (EU/US) | MOVEVOX Factory Standard | Scope of Application |
|---|---|---|---|---|
| Carcinogenic Azo Dyes | EN 14362-1 / ISO 24362-1 | <30 ppm (EU REACH) | <20 ppm (Undetected) | All dyed yarns, fabrics, and prints |
| Phthalate Plasticizers | CPSC-CH-C1001-09.4 | <1,000 ppm (0.1%) | <100 ppm (Compliant) | Silicone heat transfers, elastic coatings |
| Total Heavy Metals (Pb, Cd, Hg, Cr) | EPA 3052 / EN 16711-1 | <100 ppm combined | <20 ppm (Undetected) | Metallic aglets, zipper pulls, snaps |
| Polyfluoroalkyl Substances (PFAS) | CEN/TS 15968 | <100 ppb total | 100% Fluorine-Free DWR | Water-repellent coatings on shorts |
| Free & Hydrolyzed Formaldehyde | ISO 14184-1 | <75 ppm (Skin contact) | <16 ppm (Undetected) | Anti-crease finishes, fixing agents |
Ethical Labor Practices, Workplace Safety & Social Compliance
We manage our 6,000㎡ Yiwu manufacturing facility with transparent, humane, and legally compliant labor standards, protecting our brand partners against supply chain ethical risks.
Fair Wages & Voluntary Labor
Zero tolerance for child labor, forced labor, or prison labor. All employees are paid fair wages meeting or exceeding statutory benchmarks, with regulated working hours and paid overtime.
Workplace Health & Safety
Our facility is equipped with automated fire sprinkler networks, illuminated emergency exit corridors, continuous ventilation exchanges, and fully stocked first-aid medical stations.
Non-Discrimination & Welfare
We cultivate an inclusive workplace free of harassment or discrimination based on gender, ethnicity, or age. Continuous safety drills and machine ergonomics training are provided.
Social Audit Readiness
Our facility is structured to welcome client-commissioned ethical audits conducted by recognized bodies such as Intertek, SGS, or Bureau Veritas according to BSCI and SMETA pillars.
Sustainable Activewear Manufacturing & GRS Chain of Custody
We provide verified sustainable production infrastructure for activewear brands targeting circularity, backed by chain-of-custody documentation and eco-friendly trims.
Post-Consumer Recycled Feedstock
Sourcing GRS-certified recycled nylon derived from ocean-bound fishing nets and post-consumer polyamide waste, alongside certified rPET recycled polyester.
Transaction Certificate (TC) Matching
Every commercial production run of recycled activewear is backed by official GRS Transaction Certificates linking your purchase order to genuine recycled feedstocks.
Dope-Dyed Clean Technologies
Offering solution-dyed yarns where pigments are integrated during melt spinning, reducing water consumption by up to 80% and eliminating toxic dye effluent.
Biodegradable & Recycled Packaging
Packaging finished apparel in 100% compostable PLA+PBAT cornstarch polybags or GRS-certified recycled ziplock bags via our custom packaging center.
100% Needle & Foreign Metal Detection Safety Protocol
A broken needle fragment inside an activewear seam can cause consumer injury and catastrophic product liability lawsuits. MOVEVOX enforces a non-negotiable 100% screening policy.
100% Conveyor Metal Detection
Every finished activewear garment—without exception—passes through an automated dual-probe conveyor metal detector immediately prior to final carton packing.
0.8mm Ferrous Sensitivity
Our metal detection equipment is calibrated to detect ferrous metal spheres down to 0.8mm–1.0mm in diameter, easily capturing microscopic sewing needle points.
Strict 2-Hour Calibration Records
Certified operators test the conveyor using standardized 9-point calibration test cards every 2 hours, logging detector sensitivity in permanent audit records.
Broken Needle Exchange Policy
When a needle breaks during sewing, the operator must locate all broken fragments and reconstruct the complete needle on an audit board before receiving a replacement.
Batch-Level ERP Barcode Traceability: From Yarn Lot to Export Carton
Complete end-to-end digital traceability ensures that any quality irregularity can be isolated instantly back to the specific machine, operator, and raw material batch.
Step 01: Raw Yarn Lot Barcoding
Incoming yarn spools and fabric rolls are assigned unique warehouse QR codes recording supplier origin, lot dye date, and IQC lab clearance data in our system.
Step 02: Inline Production Bundle QR Tagging
Cut panels and Santoni tubular knit batches travel through assembly accompanied by digital traveler cards, tracking operator ID, workstation, and sewing timestamp.
Step 03: QC Defect Cloud Logging
Quality inspectors log all measurement deviations and cosmetic flaws via mobile handheld terminals, updating real-time factory yield dashboards in our ERP.
Step 04: Master Carton QR Code Traceability
Outer export cartons are printed with scannable batch codes linking packed garments to specific production shifts, allowing full retrospective audit for up to 24 months.
Hold Your Activewear Sourcing to Uncompromising Quality Standards
Request our comprehensive 38-page Quality Assurance Manual, sample AQL inspection reports, and official RoHS/REACH compliance files today. Our quality engineering team is available to review your brand's technical specifications.
AQL 1.5/2.5 Standard | 100% Metal Detection | Third-Party Audit Supported | In-House Testing Lab
CAPA System: 8D Root-Cause Analysis & Continuous Improvement
We manage manufacturing deviations through a disciplined Corrective and Preventive Action (CAPA) framework, eliminating defect recurrence through systemic engineering.
Crotch flatlock seam unraveling during initial wearer fit testing.
Sewing machine looper thread tension was set too high, causing texturized nylon looper thread to snap under high mechanical extension.
Adjusted looper thread tension gauge, installed electronic tension sensors, and amended stitch parameter to 11 SPI in the production work order.
Minor waistband curl-over observed on high-compression legging samples.
Inner elastic band lacked sufficient recovery modulus, failing to counter the negative ease tension of the outer body fabric.
Replaced elastic band with high-recovery cross-woven webbing; increased top-edge understitch allowance to anchor elastic permanently.
Heat-transfer silicone brand logo flaking off after 10 high-temperature laundry cycles.
Heat-press dwell time was insufficient (10 seconds instead of required 15 seconds), resulting in incomplete polyurethane adhesive melting.
Installed automated pneumatic heat-press timers locked at 160°C and 15 seconds; mandated 20-wash pre-release tests for all logo lots via our custom logo line.
Case Study: Eliminating Seam Failures & Slashing Return Rates for an EU Brand
How MOVEVOX engineered anti-burst seam architecture, overhauled QC protocols, and reduced bulk return rates from 7.8% to under 0.08% for an expanding European athletic label.
The Quality Crisis
An established European fitness apparel brand distributing across Germany, France, and the UK faced a critical quality emergency with their flagship high-compression leggings. Their prior manufacturer suffered severe stitch quality degradation during bulk scaling. Inseams and crotch junctions ruptured during deep squats, resulting in a disastrous 7.8% customer return rate and imminent retailer chargebacks.
The MOVEVOX Engineering Solution
MOVEVOX took over manufacturing with an immediate technical overhaul. Our pattern team eliminated 4-way cross junctions, inserting a double-layer diamond crotch gusset. We transitioned all joining operations to our specialized 4-needle 6-thread flatlock machines calibrated at 11 SPI with high-elongation woolly nylon looper threads. In our lab, seam samples achieved ASTM D1683 tensile strength over 190N, while Quality Director Nacy Wu instituted 100% flatbed audits for bulk runs.
"MOVEVOX's quality assurance team caught seam vulnerabilities our previous vendor missed for years. Their disciplined in-house testing and strict AQL inspection gave us back our customer trust."
— VP of Sourcing & Quality, European Athletic Apparel LabelActivewear Quality Assurance Benchmark: MOVEVOX vs. Industry Alternatives
Evaluate how our dedicated QA workforce, in-house laboratory testing, and certified chemical compliance compare against typical apparel sourcing models.
| Quality & Compliance Dimension | MOVEVOX | Sourcing Brokers / Traders | Small Cut & Sew Shops | Massive Conglomerates |
|---|---|---|---|---|
| In-House Testing Lab | Comprehensive lab (AATCC 135, ASTM D2594, ISO 12945-2) | No in-house lab equipment | Visual hand-feel check only | Certified lab with rigid bureaucracy & high fees |
| Chemical Safety Certifications | Verified RoHS 2.0 & REACH reports on file | Relies on unverified factory claims | No formal chemical testing | Fully certified with enterprise price premiums |
| Dedicated QC Workforce | 5 full-time inspectors covering IQC, IPQC, FQC, OQC | Third-party inspectors hired per diem | 1–2 sewing supervisors self-inspecting | Large QC teams with inflexible scheduling |
| 100% Needle & Metal Detection | 100% dual-head conveyor screening for all units | Unmonitored or omitted | Manual handheld wand or zero detection | Mandatory 100% screening |
| Batch ERP Barcode Traceability | Digital QR tracking from yarn roll to export carton | Paper packing lists easily lost | Manual whiteboard scheduling | Enterprise SAP/ERP systems |
| Third-Party Audit Support | Welcomes BSCI, SMETA, and brand QA audits | Often obscures actual factory locations | Frequently fails basic labor audits | Standardized audit readiness |
| Defect Compensation Guarantee | Clear contractual redo and refund liability | Protracted dispute resolution | Disclaims liability post-shipping | Strict standard legal procedures |
Quality, Compliance & Factory Audit Technical FAQ
Direct technical answers addressing AQL sampling limits, third-party audits, chemical test reports, and defect compensation policies.
What AQL inspection standard do you enforce for bulk production?
By default, we enforce ANSI/ASQ Z1.4 (ISO 2859-1) Normal Single Sampling Level II, maintaining AQL 1.5 for Major functional defects and AQL 2.5 for Minor cosmetic points. We can accommodate custom client AQL protocols or provide 100% full inspection services upon contractual agreement.
Are your activewear fabrics certified under EU RoHS 2.0 and REACH Annex XVII?
Yes. Our production materials have undergone accredited testing by TST, certified under Test Report No. TST20250405148E (RoHS 2.0 heavy metals and flame retardants) and Test Report No. TST20250405150E (REACH Annex XVII phthalates), ensuring full legal compliance for the EU market.
Can our third-party inspection agency (e.g., SGS, Intertek, QIMA) inspect goods before shipping?
Absolutely. We welcome third-party inspectors commissioned by our clients. We provide dedicated inspection tables, calibrated lighting fixtures, and full factory access for random box selection and measurement auditing prior to container release.
How do you prevent broken sewing needles from contaminating finished activewear?
We enforce a 100% dual-head conveyor metal detection protocol for every packed garment, calibrated to 0.8mm ferrous spheres. Additionally, sewing workstations operate a strict broken needle reconstruction policy where new needles are issued only when all fractured pieces are accounted for.
What is your contractual policy if defective goods exceed the agreed AQL threshold?
If a pre-shipment audit reveals defects exceeding agreed AQL limits, the entire lot is quarantined for 100% re-inspection at factory expense. In the rare event that defective units pass to destination due to factory error, we provide free prioritized re-makes or immediate financial credit.
Can you supply official GRS Transaction Certificates for our sustainable activewear lines?
Yes. For orders specifying GRS-certified recycled nylon or recycled polyester, we coordinate directly with certified yarn and fabric mills to provide official Transaction Certificates (TCs) linking your purchase order to legitimate recycled feedstocks.
How do you ensure color shade consistency between separate production batches?
We lock physical master color swatches under D65, TL84, and UV light boxes during initial lab dip approvals. Furthermore, matching top-and-bottom fabrics are dyed in synchronized lots, guaranteeing zero shade mismatch between bras and leggings.
Do you allow client-commissioned ethical and social compliance audits like BSCI?
Yes. Our 6,000㎡ Yiwu facility complies with legal labor, wage, and occupational health standards. We routinely host scheduled on-site audits from international inspection agencies auditing labor rights, fire safety, and environmental standards.
Secure Your Brand's Activewear Supply Chain with Verified Quality
Partner with an activewear manufacturer that treats quality control and regulatory compliance as an exact engineering science. Download our documentation, schedule an audit, or submit your brand QA manual for engineering review within 24 business hours.
Request QA Audit Packet
Access our 38-page Quality Assurance Manual, standard SOP checklists, defect matrixes, and certified RoHS/REACH laboratory reports.
Book On-Site / Virtual Audit
Schedule a comprehensive live video walkthrough with Quality Director Nacy Wu or arrange an on-site visit to inspect our Yiwu testing center.
Submit Brand QA Manual
Upload your brand's technical measurement manual, acceptable tolerance limits, and Restricted Substance List for 24-hour engineering clearance.
Submit Your Quality & Compliance Specifications
Provide your technical requirements below. All project files, technical packets, and proprietary designs are protected under formal mutual Non-Disclosure Agreements.
Commercial & Legal Credentials: Legal Entity: Yiwu Chenjin Import And Export Co., Ltd. | Official Email: lzmwwx@gmail.com | Official WhatsApp: +86 151 0555 8361 | Response Time: Within 2–4 Business Hours (07:00–24:00 CST) | All submissions protected under strict NDA.
Request MOQ & Sample Details