When Should Your Sourcing Team Evaluate MOVEVOX as a Factory?
This page is most relevant after general product discovery. The buyer may already know what product it wants to manufacture; the remaining task is to determine whether the factory, production resources, operational controls and commercial structure are suitable for long-term cooperation.
Evaluate the Operation Behind the Product
MOVEVOX should be evaluated as an operating manufacturing system rather than as a catalogue supplier.
This becomes particularly relevant when sourcing teams are moving toward RFQ, second-source approval, product transfer or repeat commercial production.
New Supplier Qualification
For established brands adding a Seamless Yoga source to an approved supplier pool.
Second-Source Qualification
For buyers reducing dependence on one existing supplier or production location.
Existing Product Transfer
For programs beginning from a Tech Pack, approved garment or legal reference sample.
Repeat-Production Review
For brands assessing whether a factory can support continued commercial production after approval.
Start Factory Qualification With Defined Operating Facts
Headline factory statistics are useful only when the buyer understands what they represent. These figures describe the principal manufacturing and technical resources within the MOVEVOX core operating structure.
Yiwu Core Manufacturing Base
Approximately 6,000 m² of core manufacturing space in Yiwu, China.
Santoni Machines
Italian Seamless knitting equipment operated at the core base.
Garment Machines
Core sewing and garment resources supporting applicable Cut & Sew production.
Development Team
Two design roles, two pattern roles and four sampling or sample-garment roles.
QC Personnel
Quality personnel supporting relevant production, finished-garment and packing control.
Factory Access
Scheduled visits, remote or video review and agreed third-party inspection can be supported according to project requirements.
Connect Santoni Equipment to Actual Seamless Production
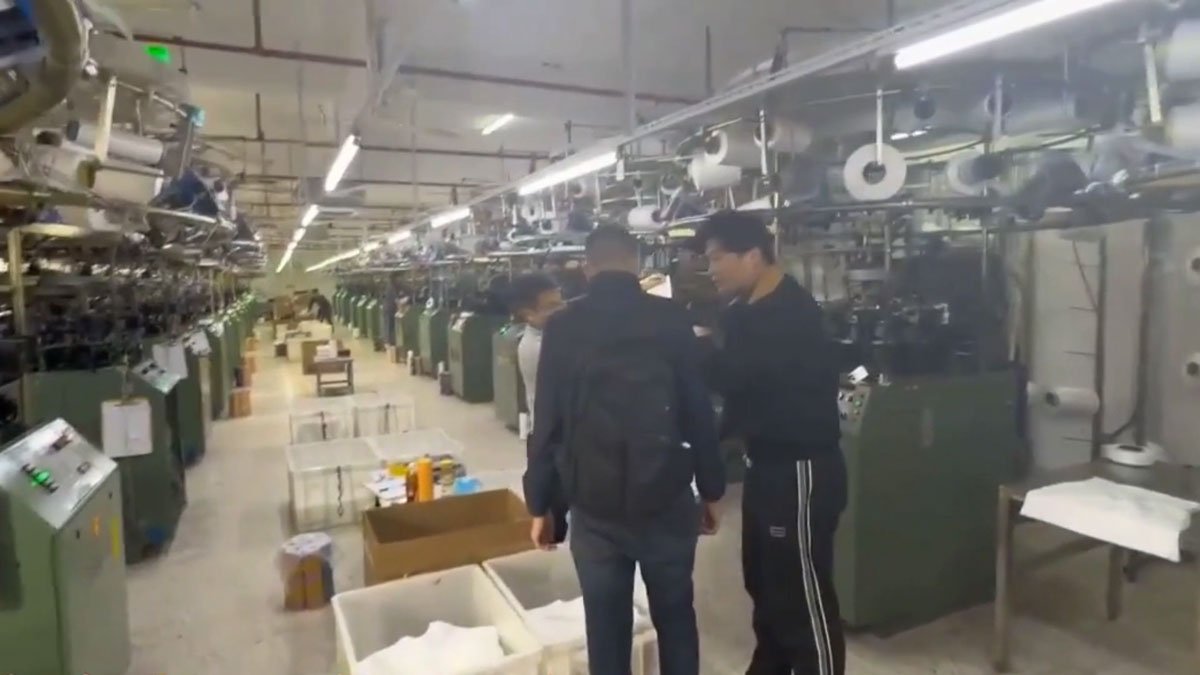
For a Seamless Yoga factory, equipment is a fundamental supplier-qualification point. Machine count becomes more useful when buyers can connect the equipment to the physical production floor, operators, material inputs and actual manufacturing activity.
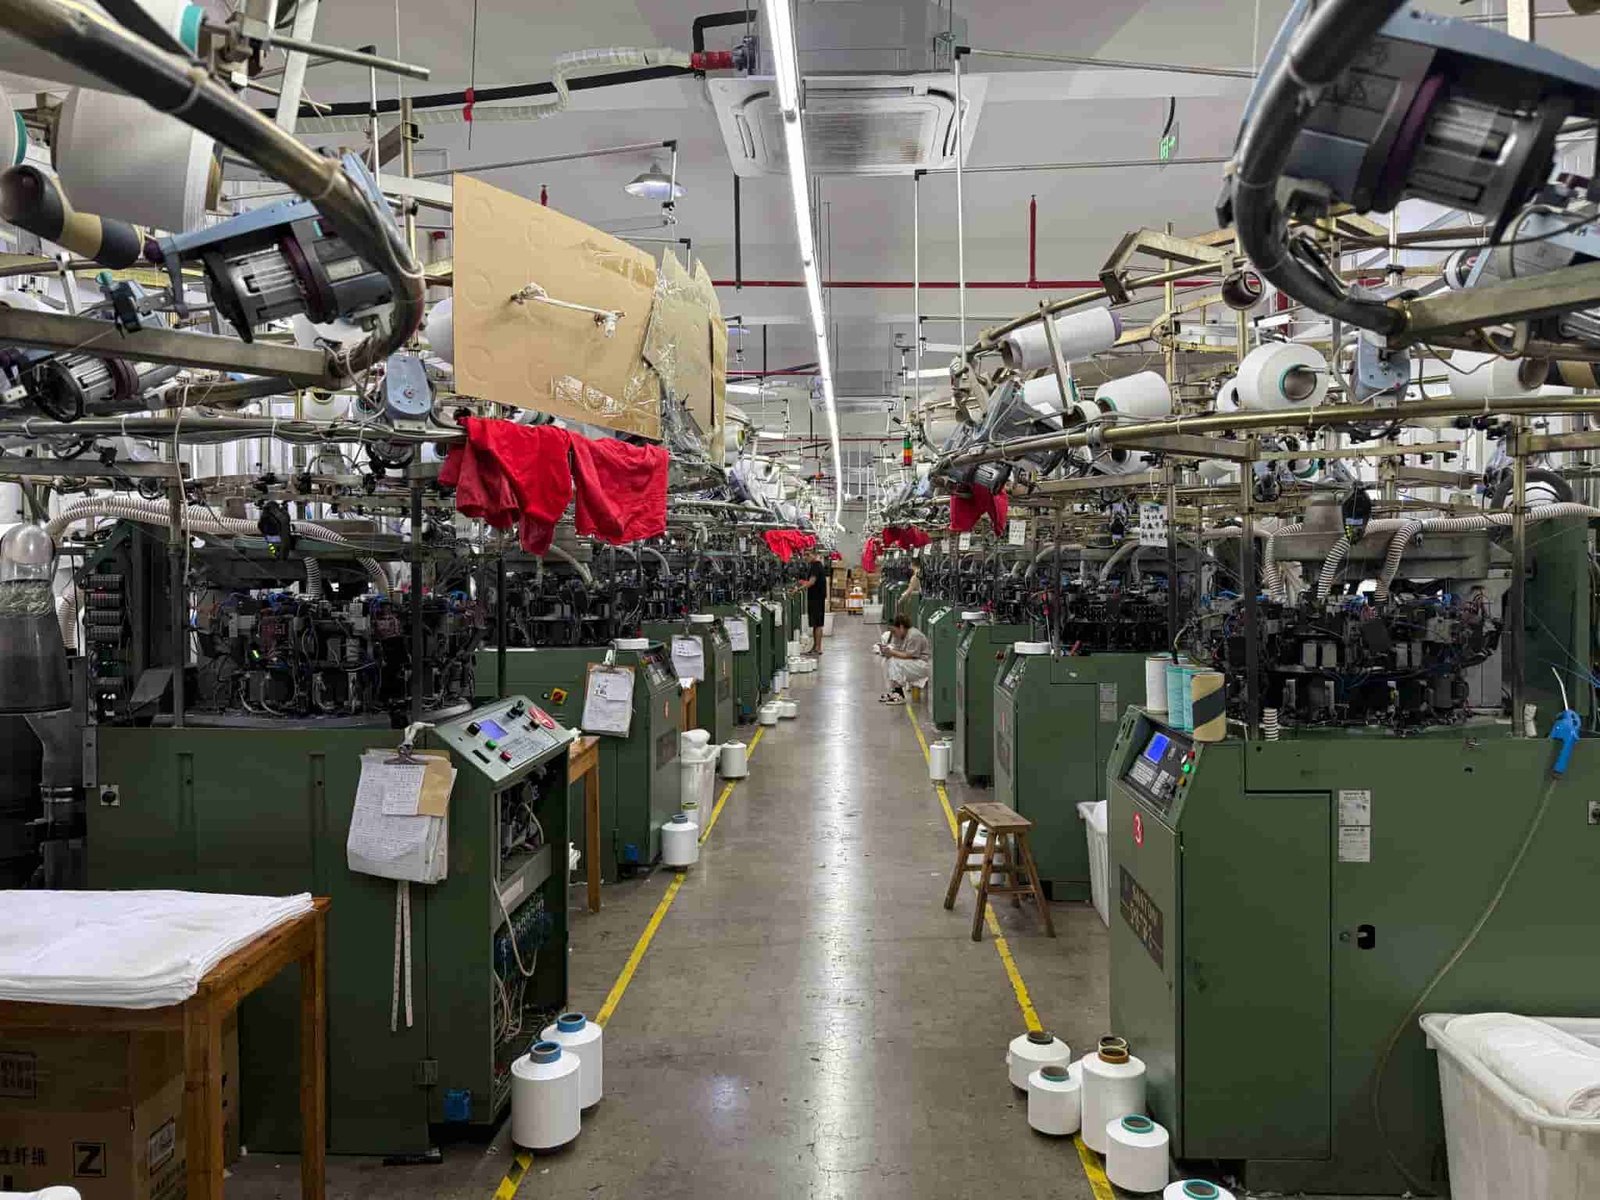
Machine Floor
The 28 Italian Santoni machines should be reviewable as installed manufacturing resources.
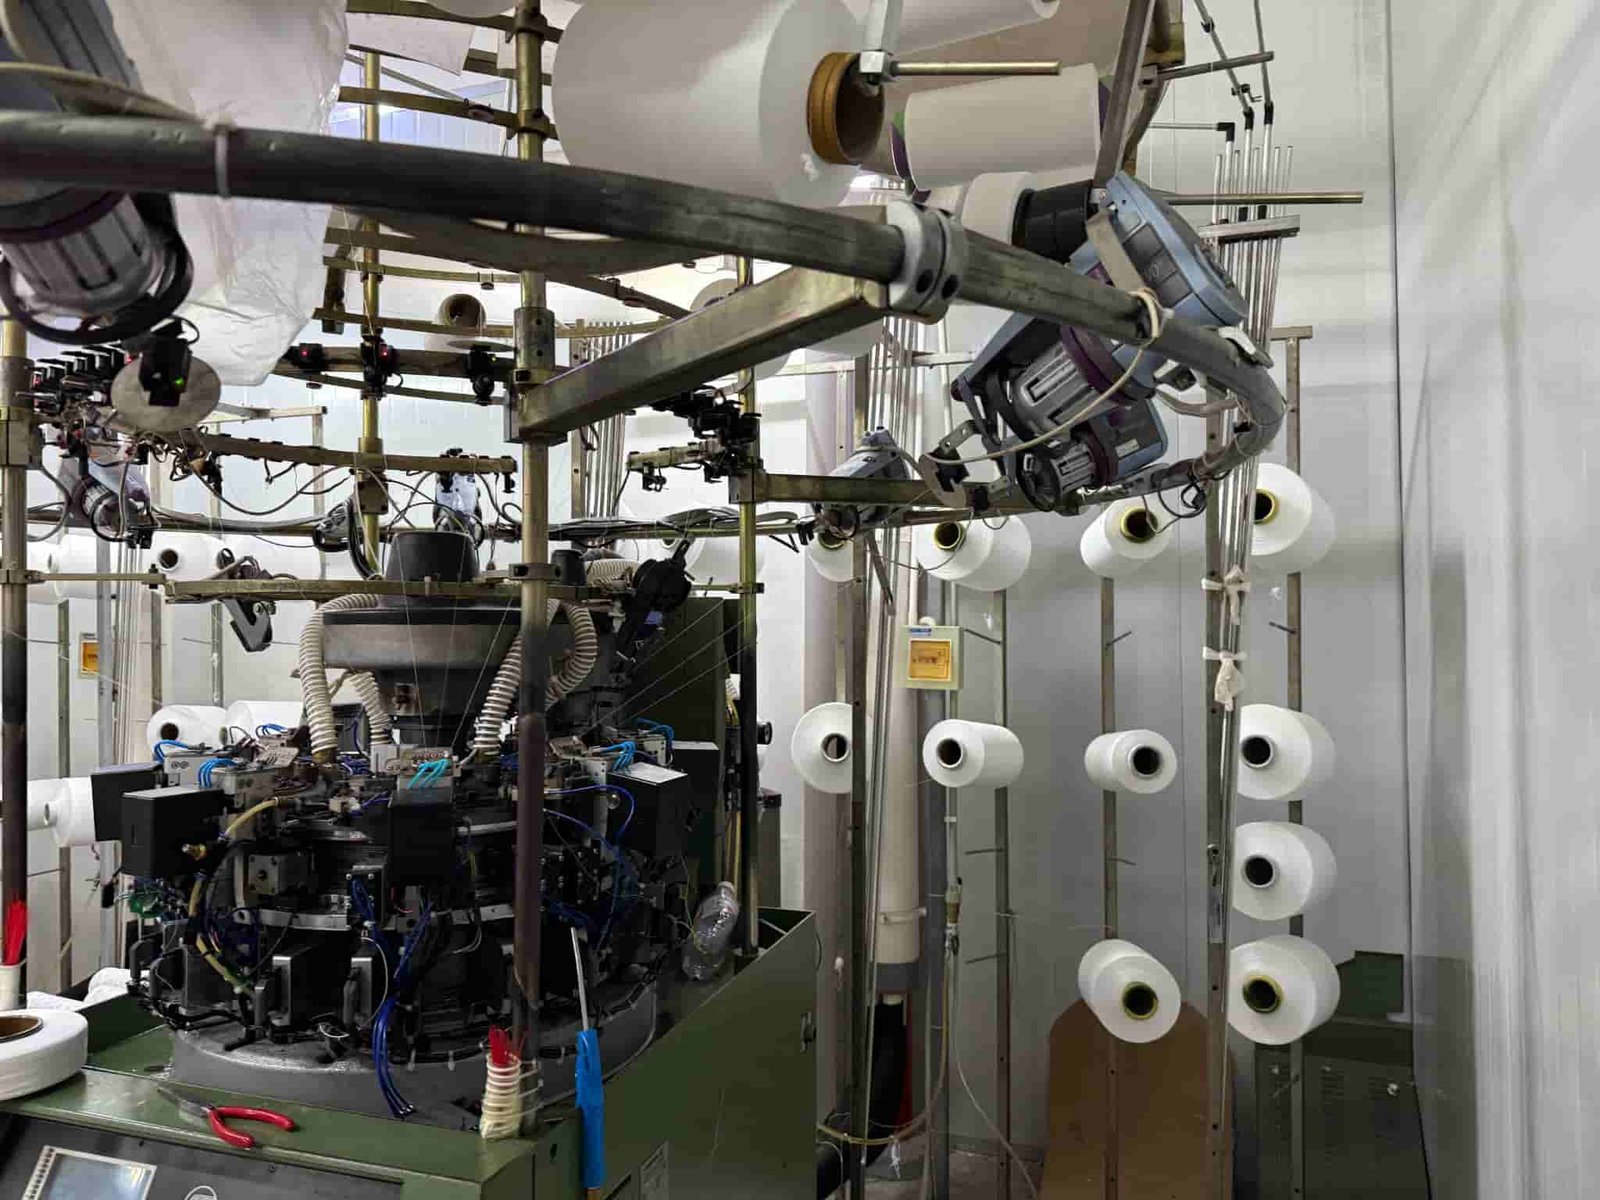
Machine Operation
Production evidence should show equipment being used rather than only isolated machinery.
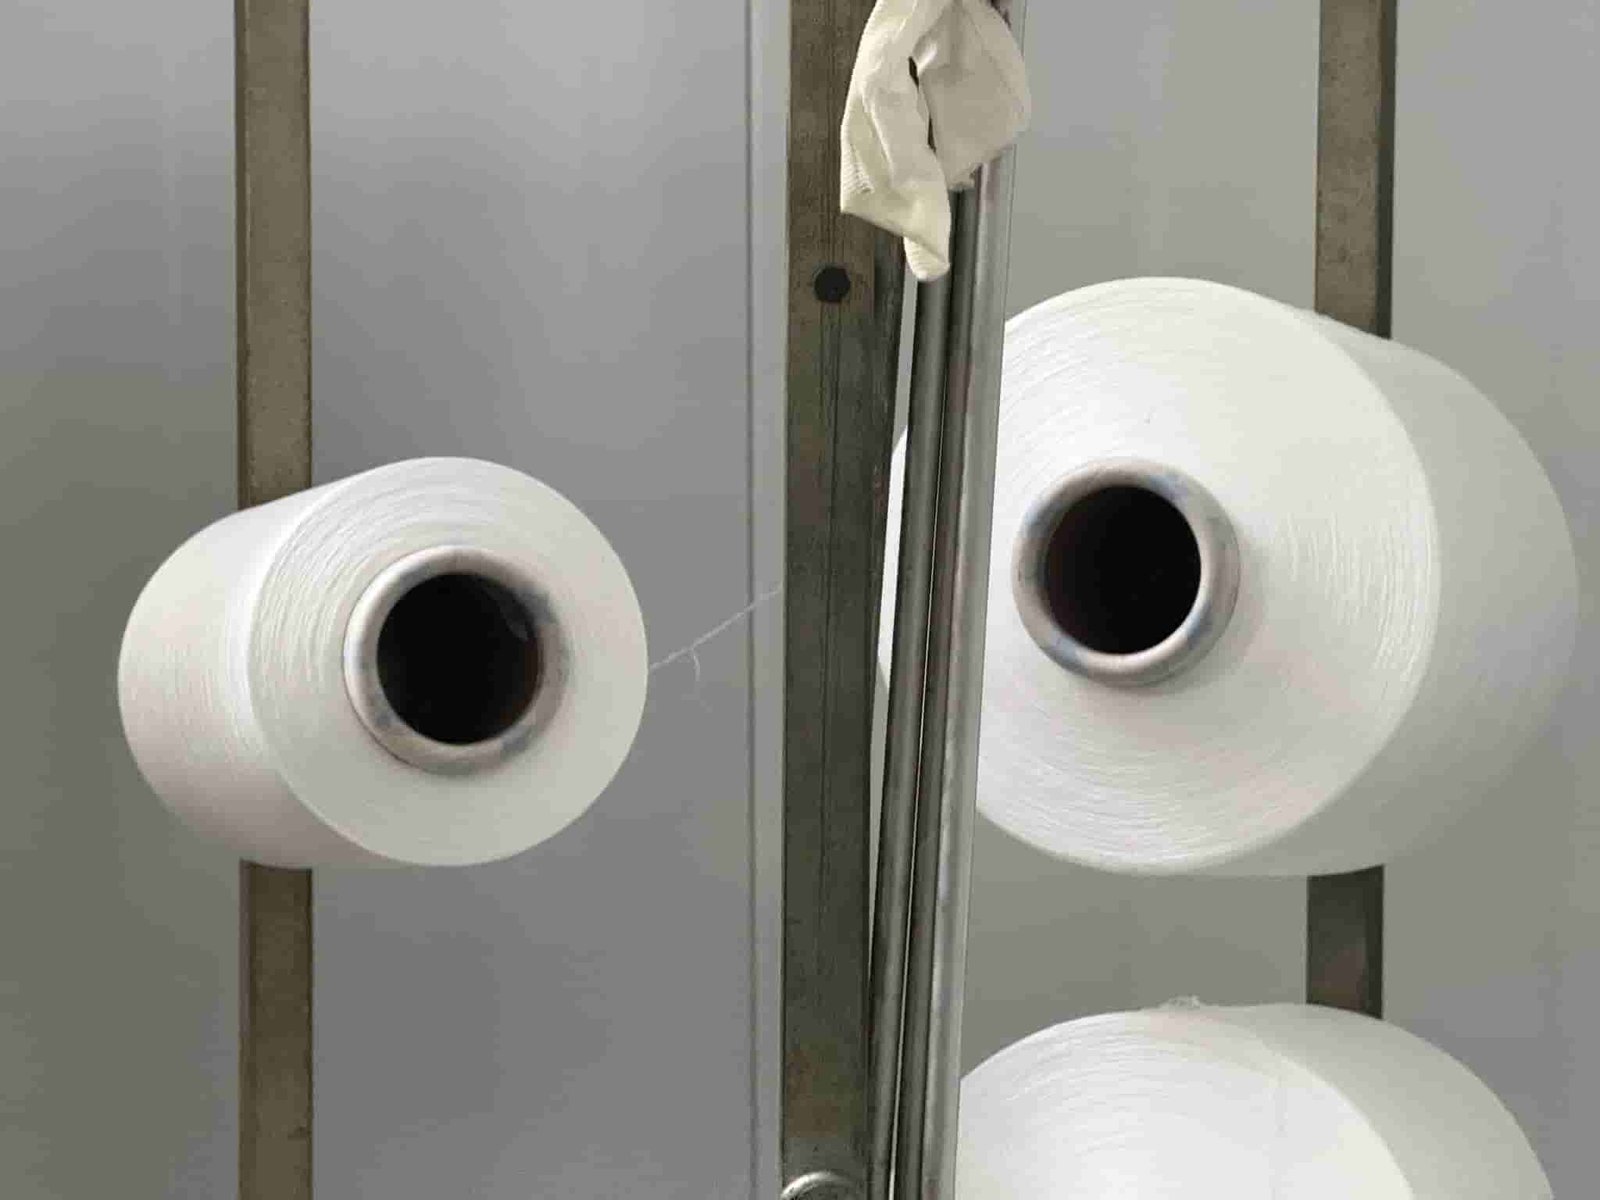
Yarn Input
Physical yarn inputs connect the knitting platform to an actual production program.
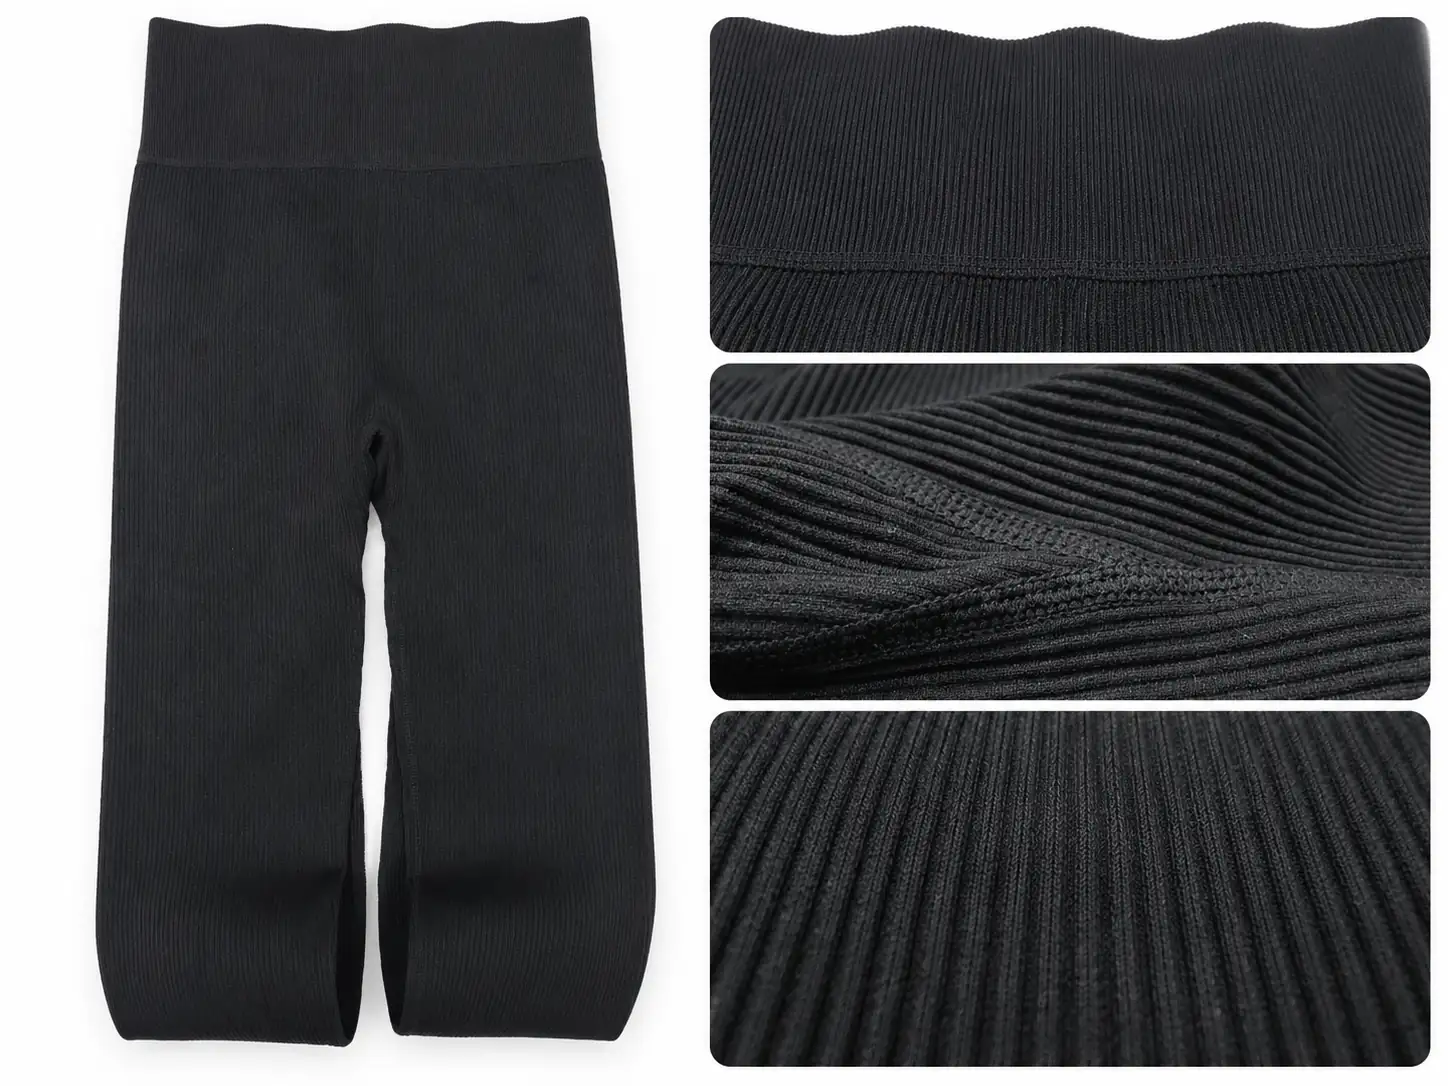
Knitted Output
Garment or knit output provides another link between equipment and commercial manufacturing.
The purpose of this module is factory verification—not detailed knit-structure education.
See the Physical Operation Behind MOVEVOX
A professional factory page should not use product photography as a substitute for manufacturing evidence. Different parts of the operation should be visible without repeatedly showing the same machine floor or QC image.
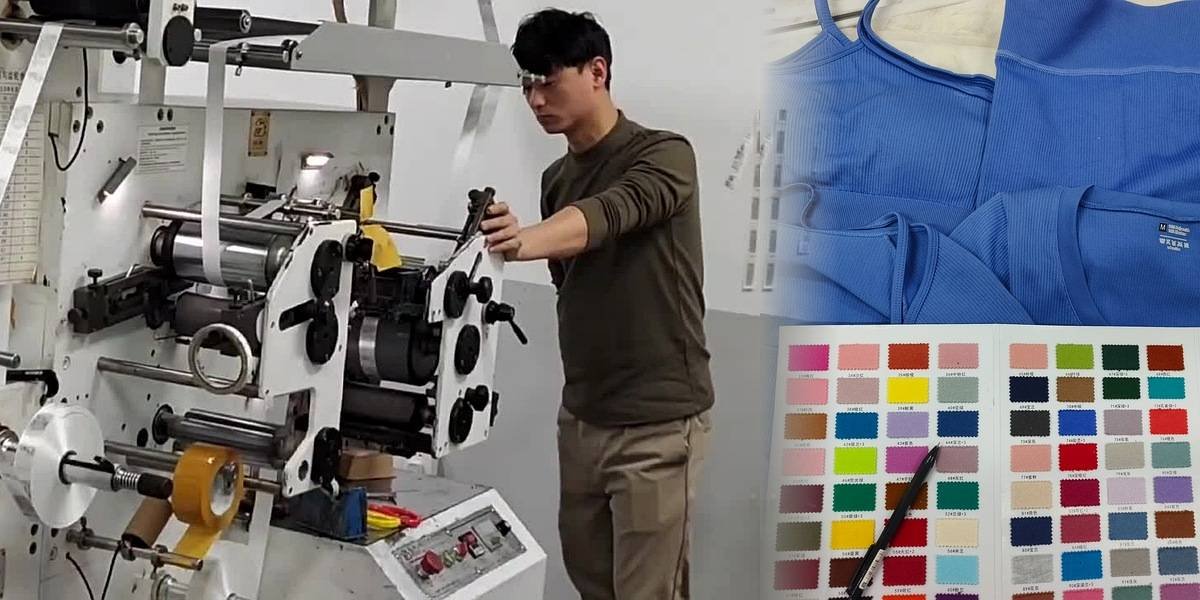
Seamless Production
Actual manufacturing environment supporting Seamless production.

Cut & Sew Resources
Physical sewing and garment resources for applicable products.
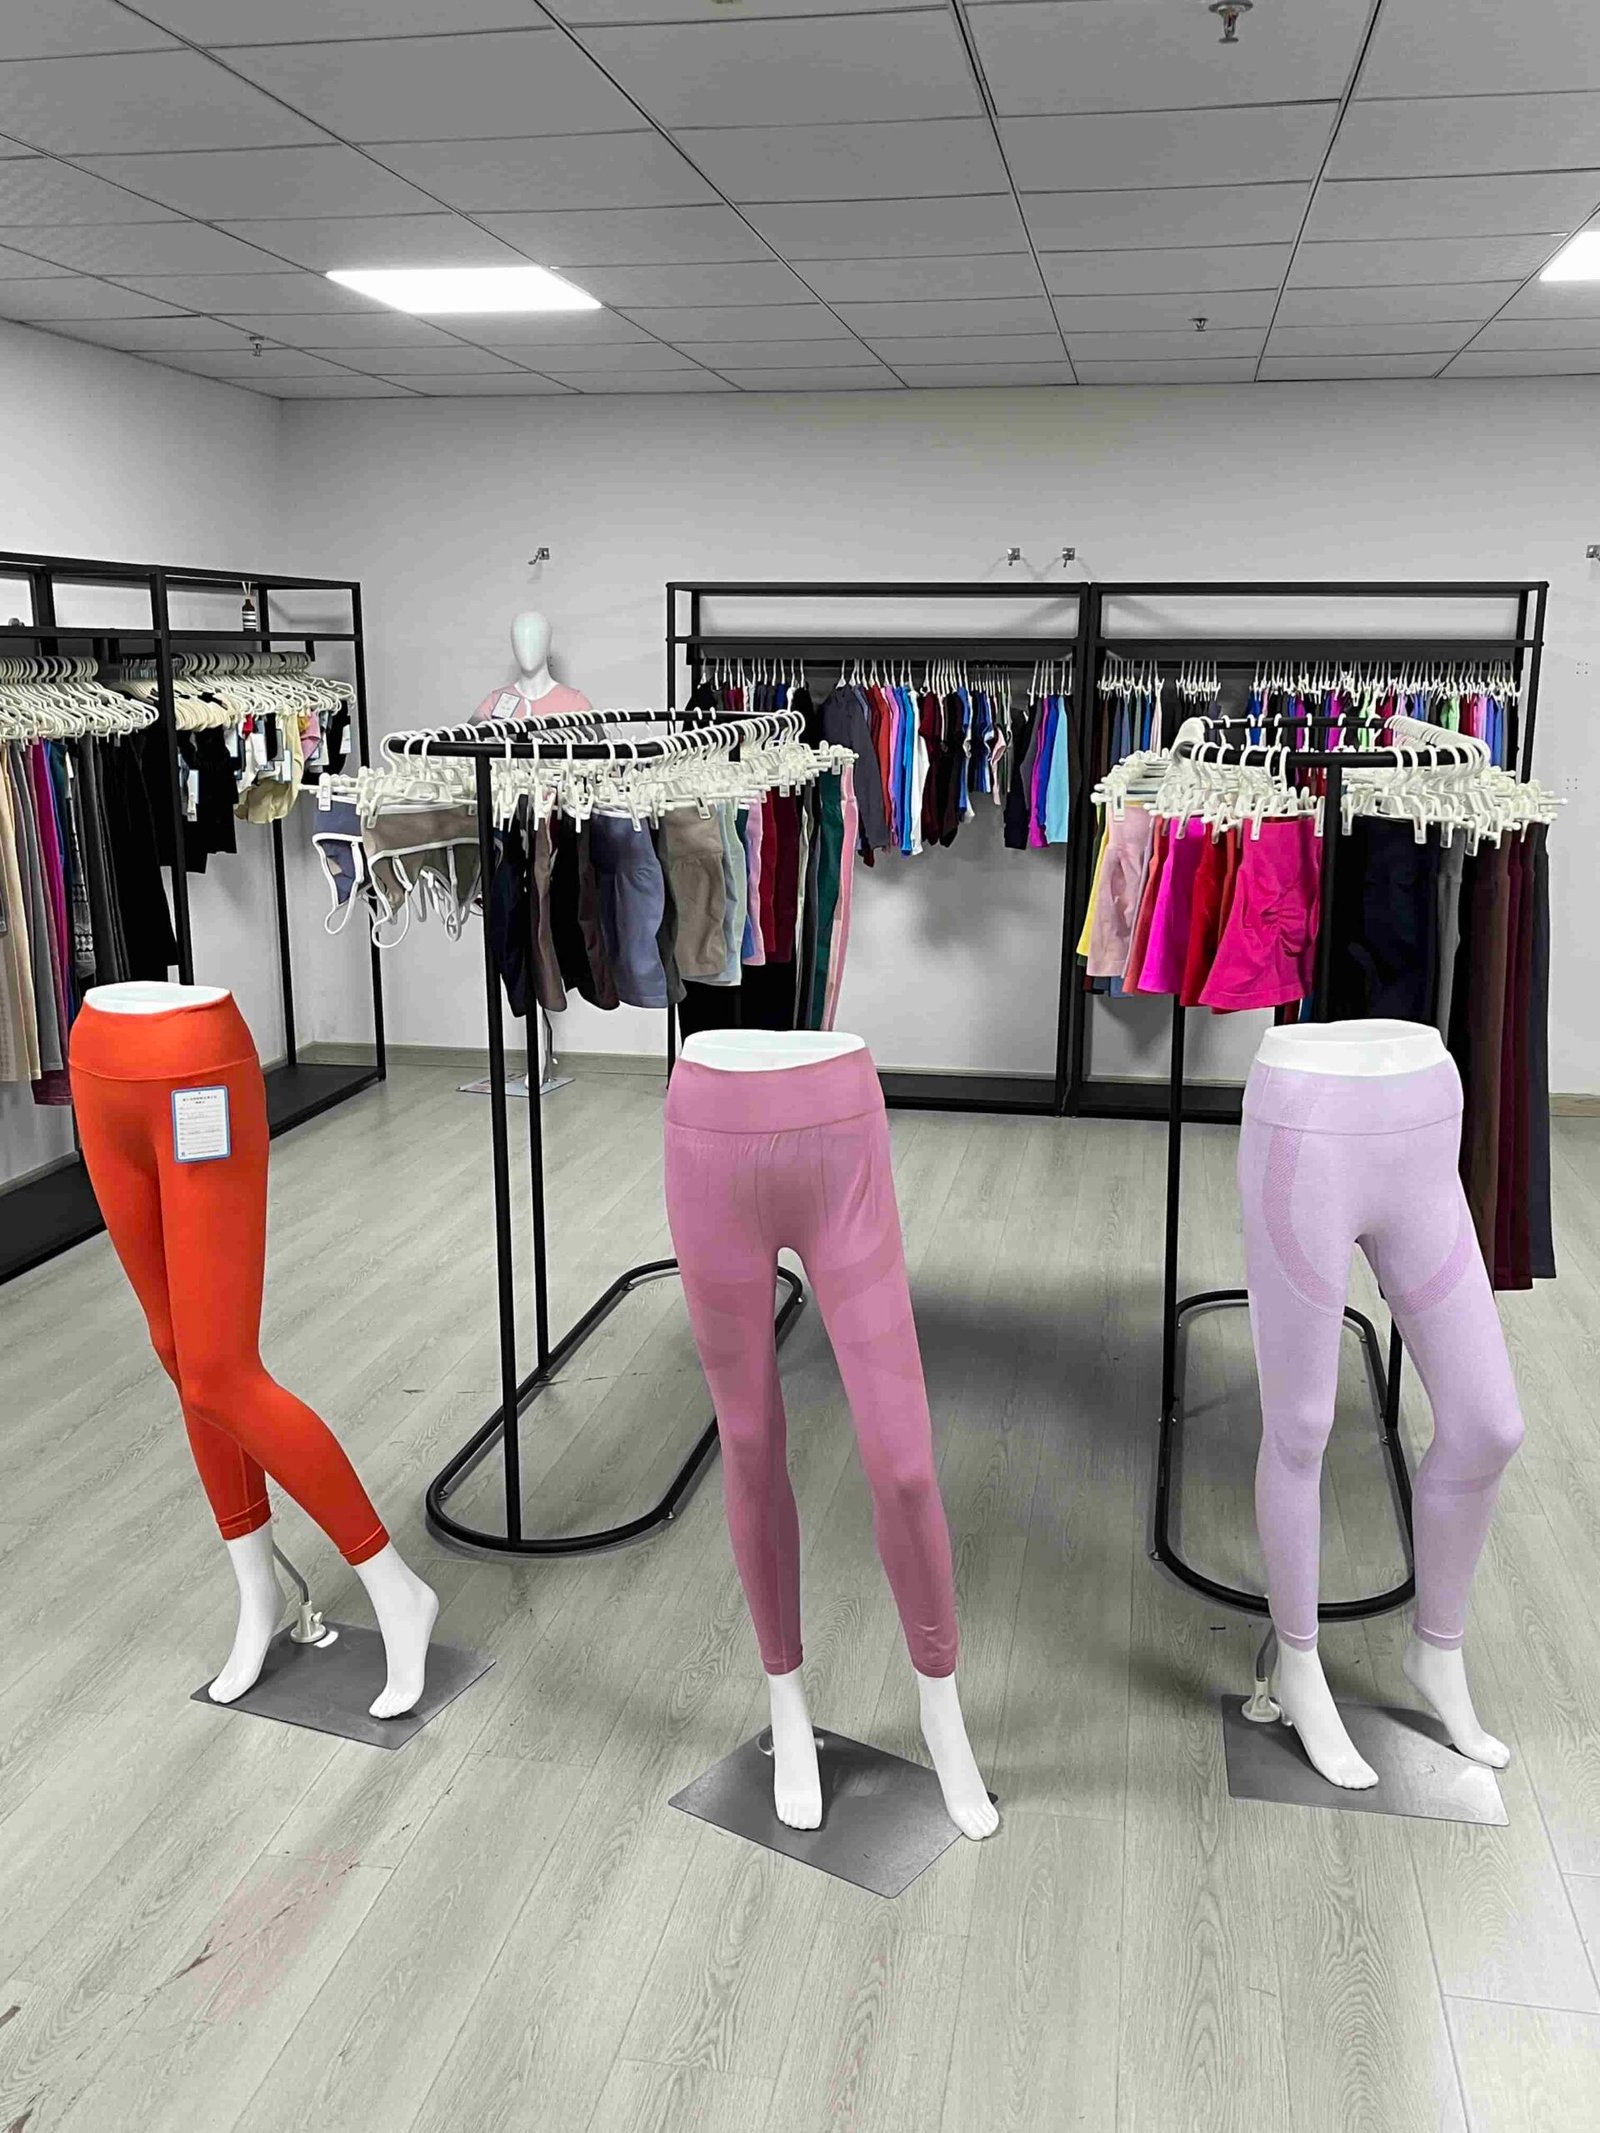
Sample & Development Area
Physical resources supporting development before commercial production.
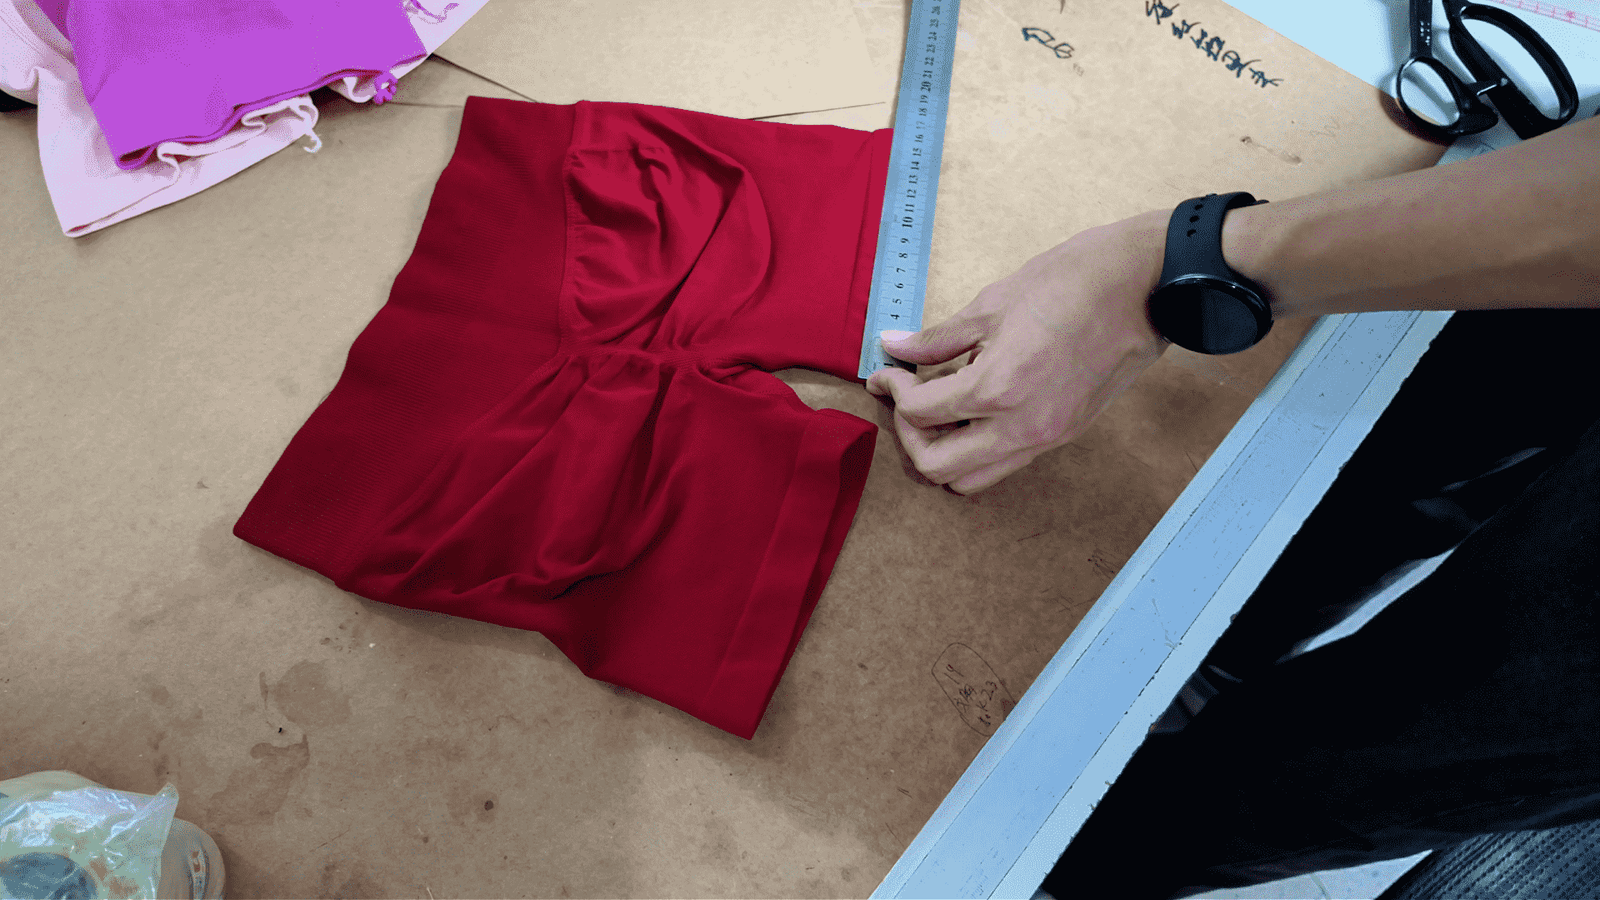
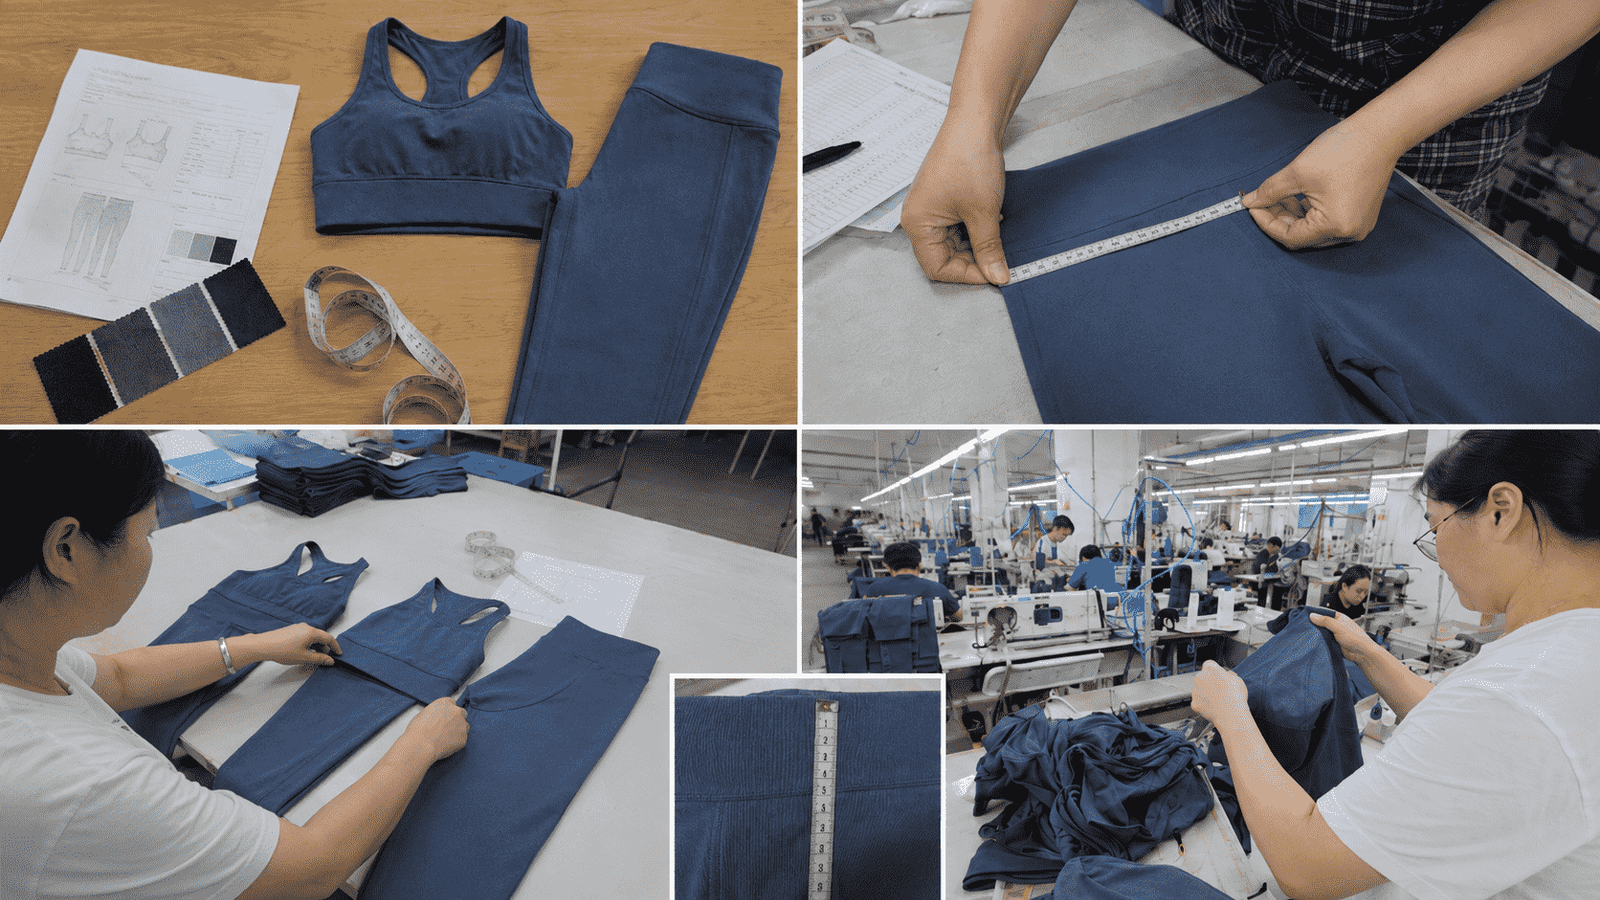
Quality Activity
Actual garment checking, measuring or inspection activity.
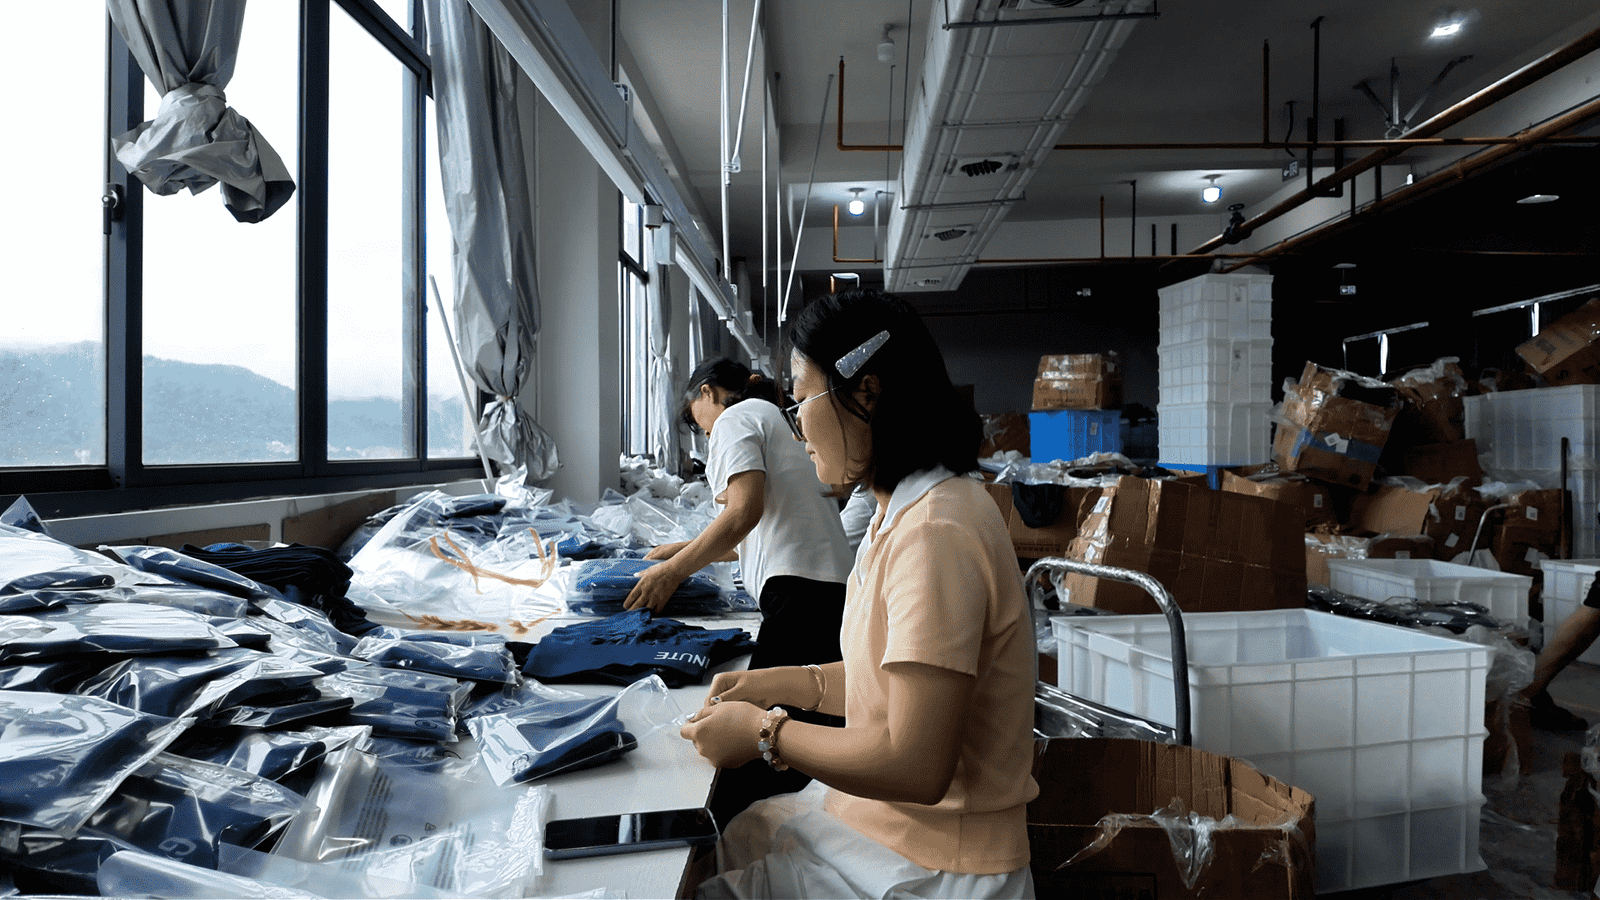
Packing Operation
Finished products moving through relevant packing processes.
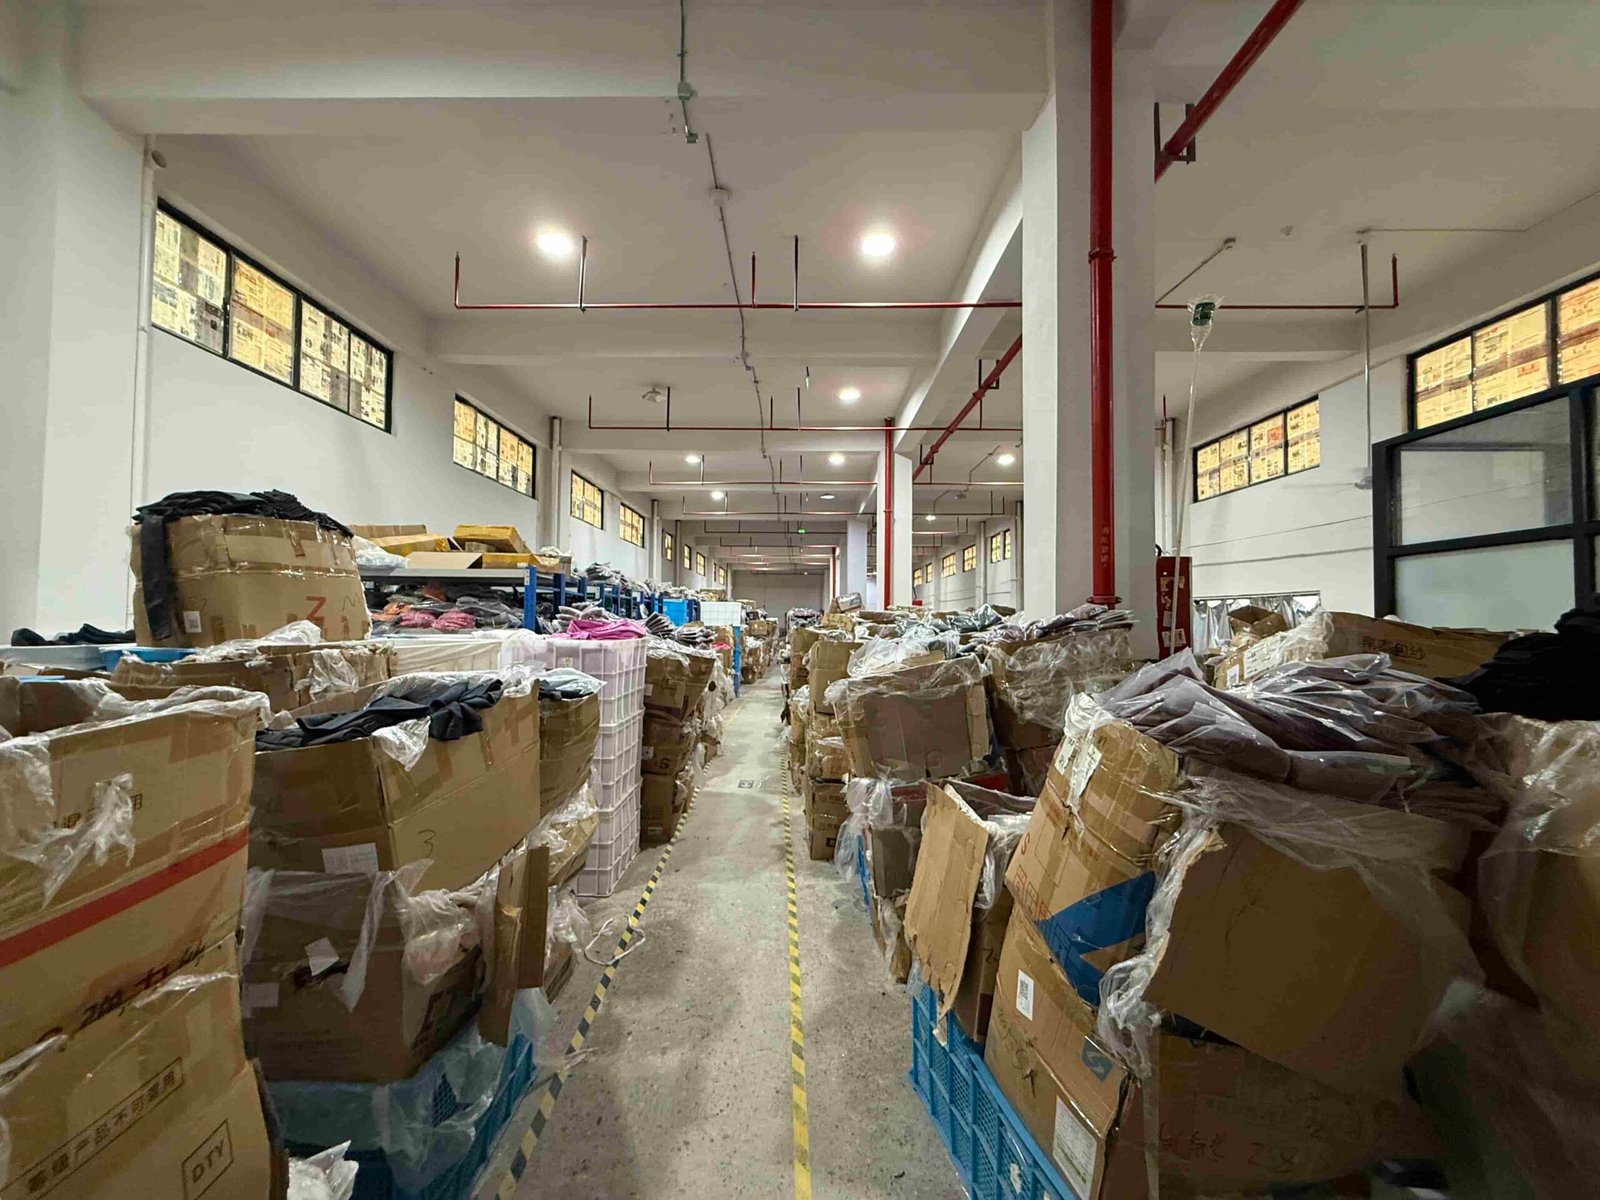
Finished-Goods Handling
Warehouse or shipment-preparation activity connected to commercial orders.
Use Seamless or Cut & Sew According to the Product Construction
MOVEVOX operates both Seamless and Cut & Sew manufacturing resources. Factory feasibility should follow the actual product architecture, specification and commercial requirement.
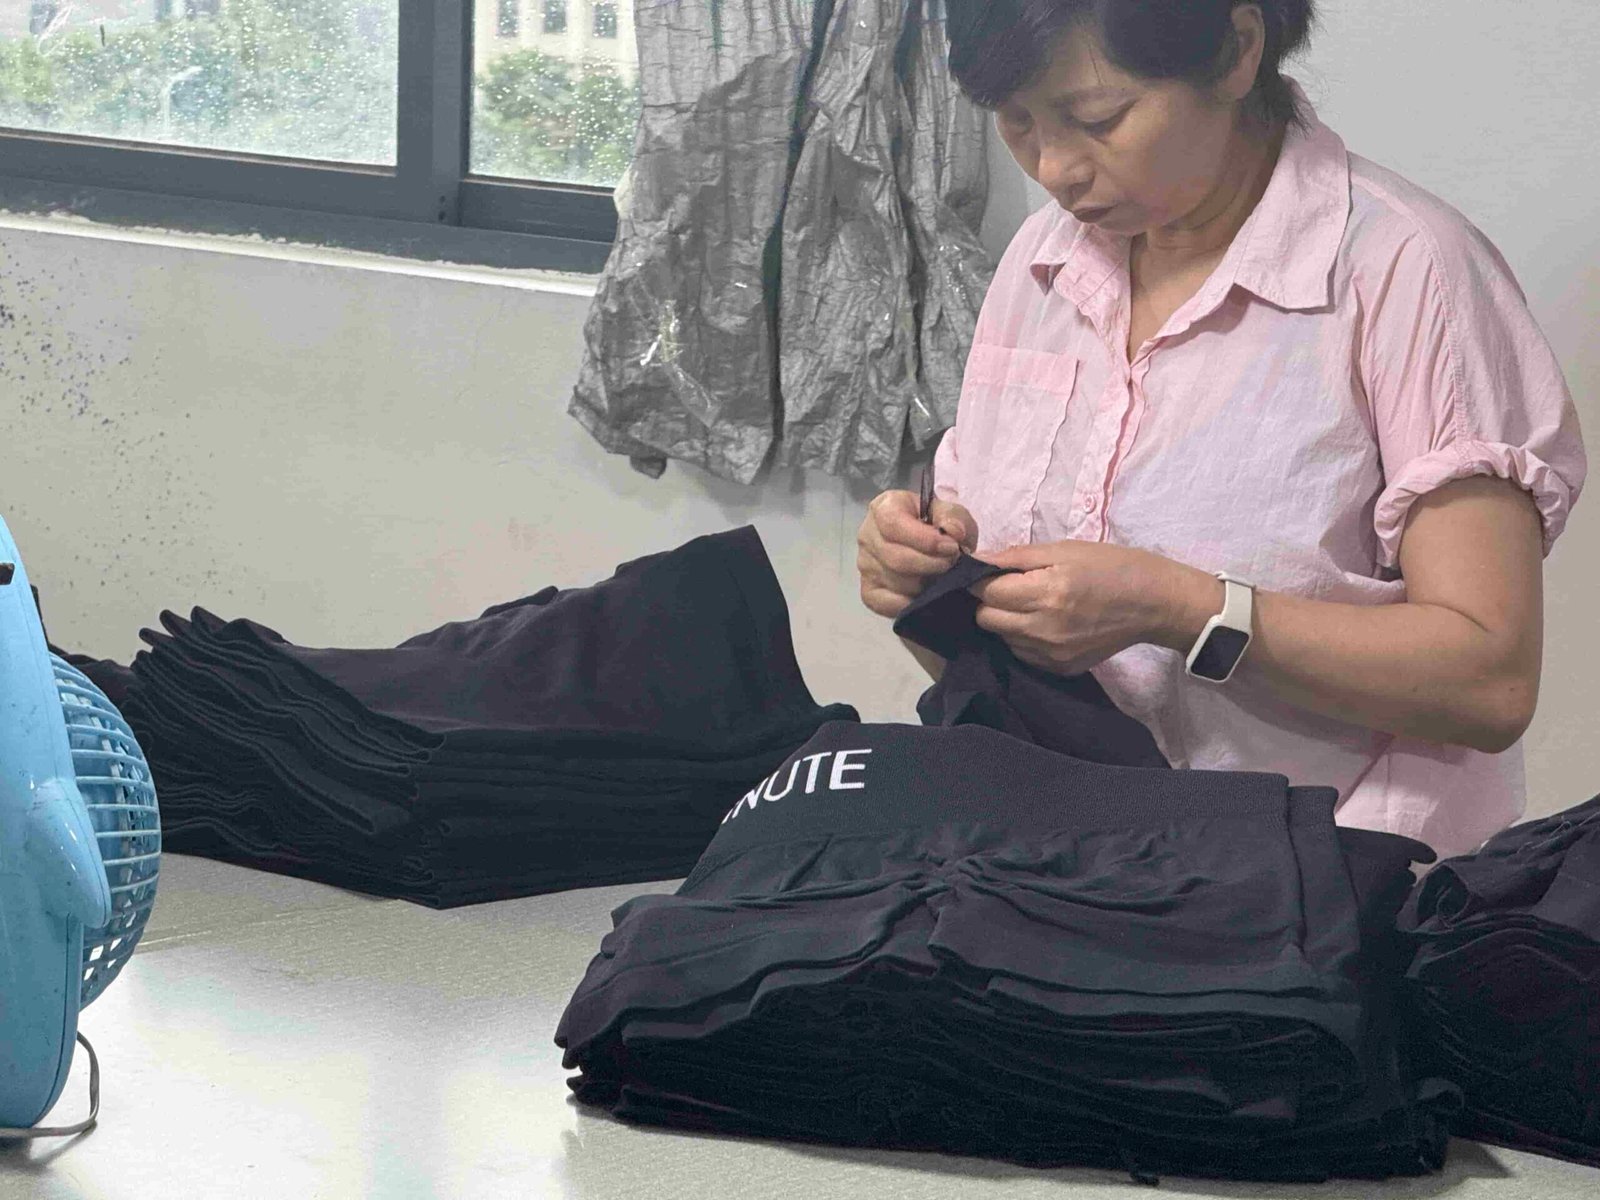
Circular-Knit Manufacturing
Circular knitting and the applicable Santoni machine program are used where the product is designed for Seamless construction.
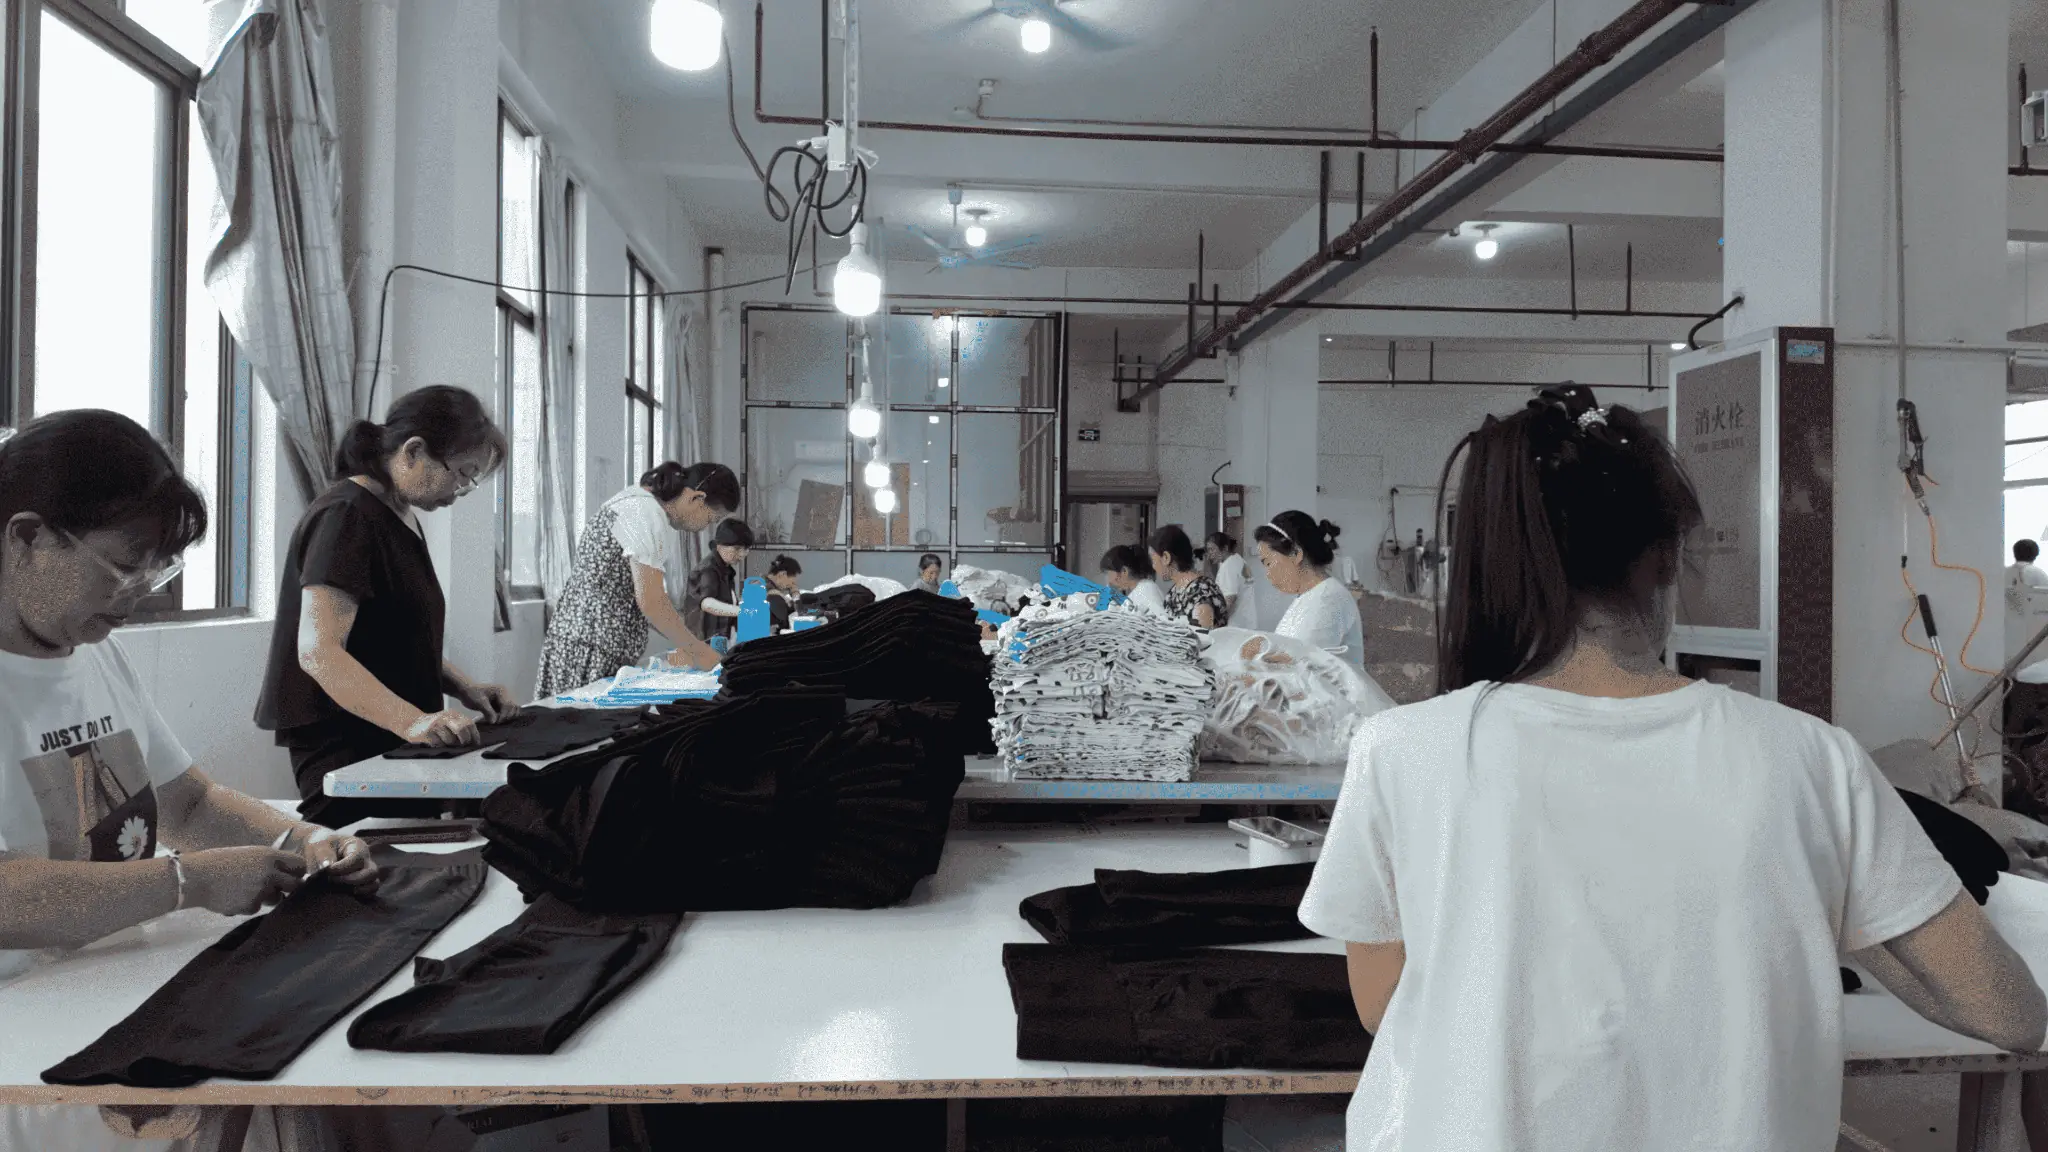
Pattern-Based Manufacturing
Fabric, pattern, cutting and sewing are used where conventional panel construction is more appropriate.
Mixed Collection Route
A broader Yoga or Activewear program can combine both manufacturing routes within one coordinated supplier relationship.
Dual-route capability can reduce the need for brands to coordinate separate supplier interfaces for every product construction type.
What Does MOVEVOX Mean by a Core Manufacturing Base?
Physical Operation in Yiwu, China
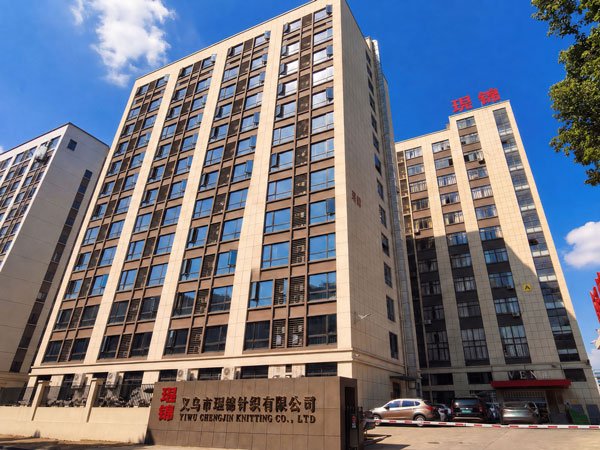
MOVEVOX operates an approximately 6,000 m² core manufacturing base in Yiwu.
The term “core factory” is important because MOVEVOX also manages controlled external capacity where appropriate. These two resource types should not be presented as identical.
A buyer evaluating MOVEVOX should be able to distinguish the directly operated core base from additional controlled production resources.
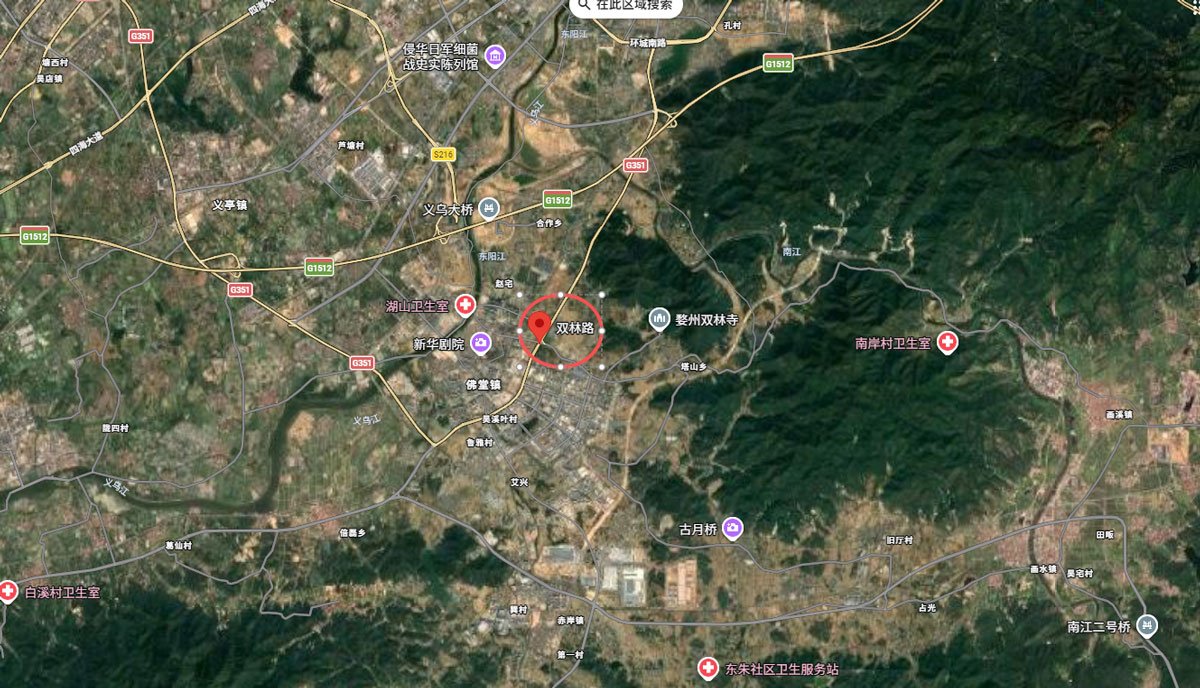
Physical Operation
The core manufacturing base is located in Yiwu, China.
Direct Seamless Resources
The base includes 28 Italian Santoni seamless knitting machines.
Applicable Cut & Sew Resources
Approximately 24 core sewing and garment machines support relevant conventional production.
Development and QC Support
Product-development roles and five QC personnel form part of the broader operating structure.
How Does Additional Capacity Stay Connected to MOVEVOX Control?
Controlled external capacity should not be presented as MOVEVOX-owned factories. The sourcing question is whether production remains connected to the correct technical documents, material requirements, planning, QC and final accountability.
Core Factory
Directly operated manufacturing resources remain the central production base.
Controlled Capacity
Additional production resources may support appropriate projects when required.
Technical Documentation
Current product standards remain centrally coordinated.
PMC
Production planning and allocation remain connected to the current order.
QC
Applicable quality requirements remain under MOVEVOX coordination.
Final Release
Finished products proceed through the agreed review and release structure.

Move Through Factory Qualification in Defined Stages
Supplier qualification does not need to begin with a full factory audit. A sourcing team can first determine whether the basic supplier facts and manufacturing resources justify deeper review.
Evidence Screen
Review supplier identity, factory facts, equipment and available supporting evidence.
Factory Review
Verify the physical operation through an agreed visit or remote review.
Production-Control Review
Understand how released product requirements move into manufacturing and QC.
Independent Inspection
Where required, define the scope for an agreed third-party inspection.
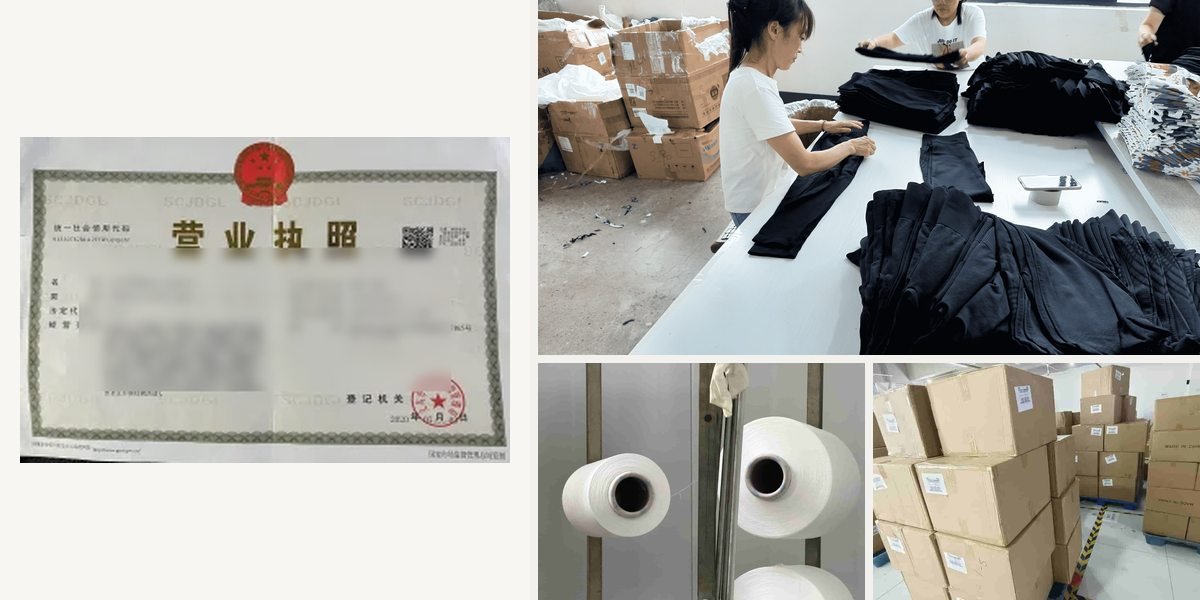
More detailed verification can be added according to the value, complexity and compliance requirements of the proposed program.
What Should a Technical Factory Review Confirm?
The purpose of a technical factory review is not to repeat product development. It is to determine whether the factory can take an already defined product standard and maintain that standard through production.
Released Product Reference
Identify the current Tech Pack, approved product or production standard.
Manufacturing Route
Confirm Seamless or applicable Cut & Sew execution.
Material Standard
Identify the relevant yarn, fabric, color and supporting-material direction.
Measurements
Confirm the applicable approved measurements and tolerances.
Early Production Gate
Define the required first-production review before broader output.
Quality Checkpoints
Confirm relevant measurement, workmanship, in-line, final and packing checks.
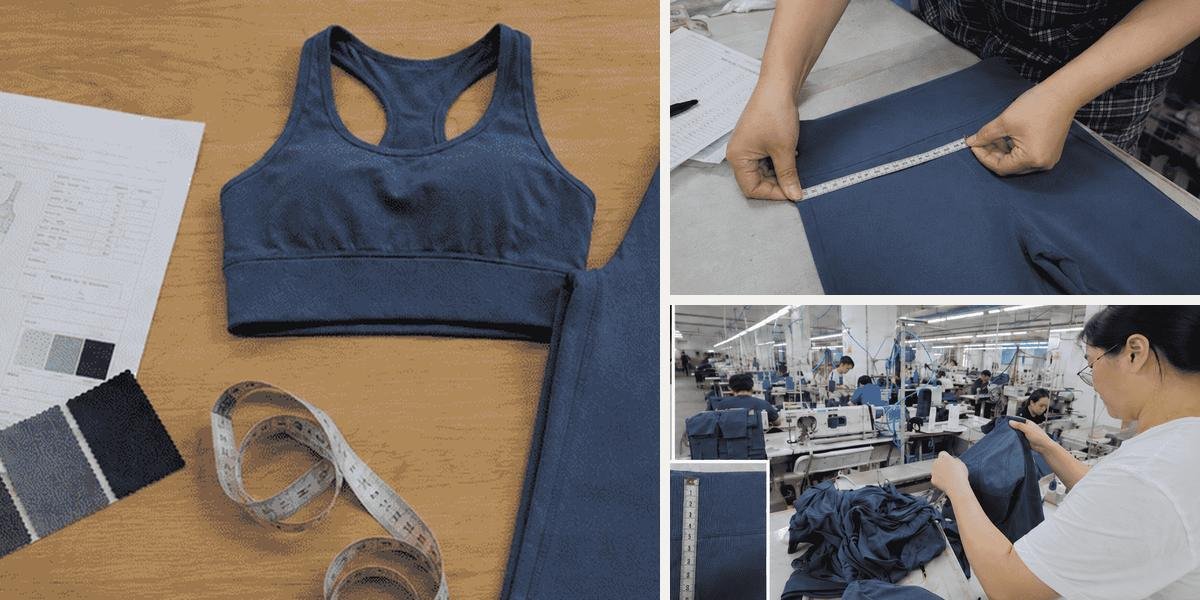
Brand files, testing requirements and customer-specific inspection criteria can also be included where relevant to the program.
Verify Key Factory Areas Before an On-Site Visit
Remote review can be useful where international travel is not practical at the early qualification stage. The review should have a defined agenda rather than functioning as a generic video call.
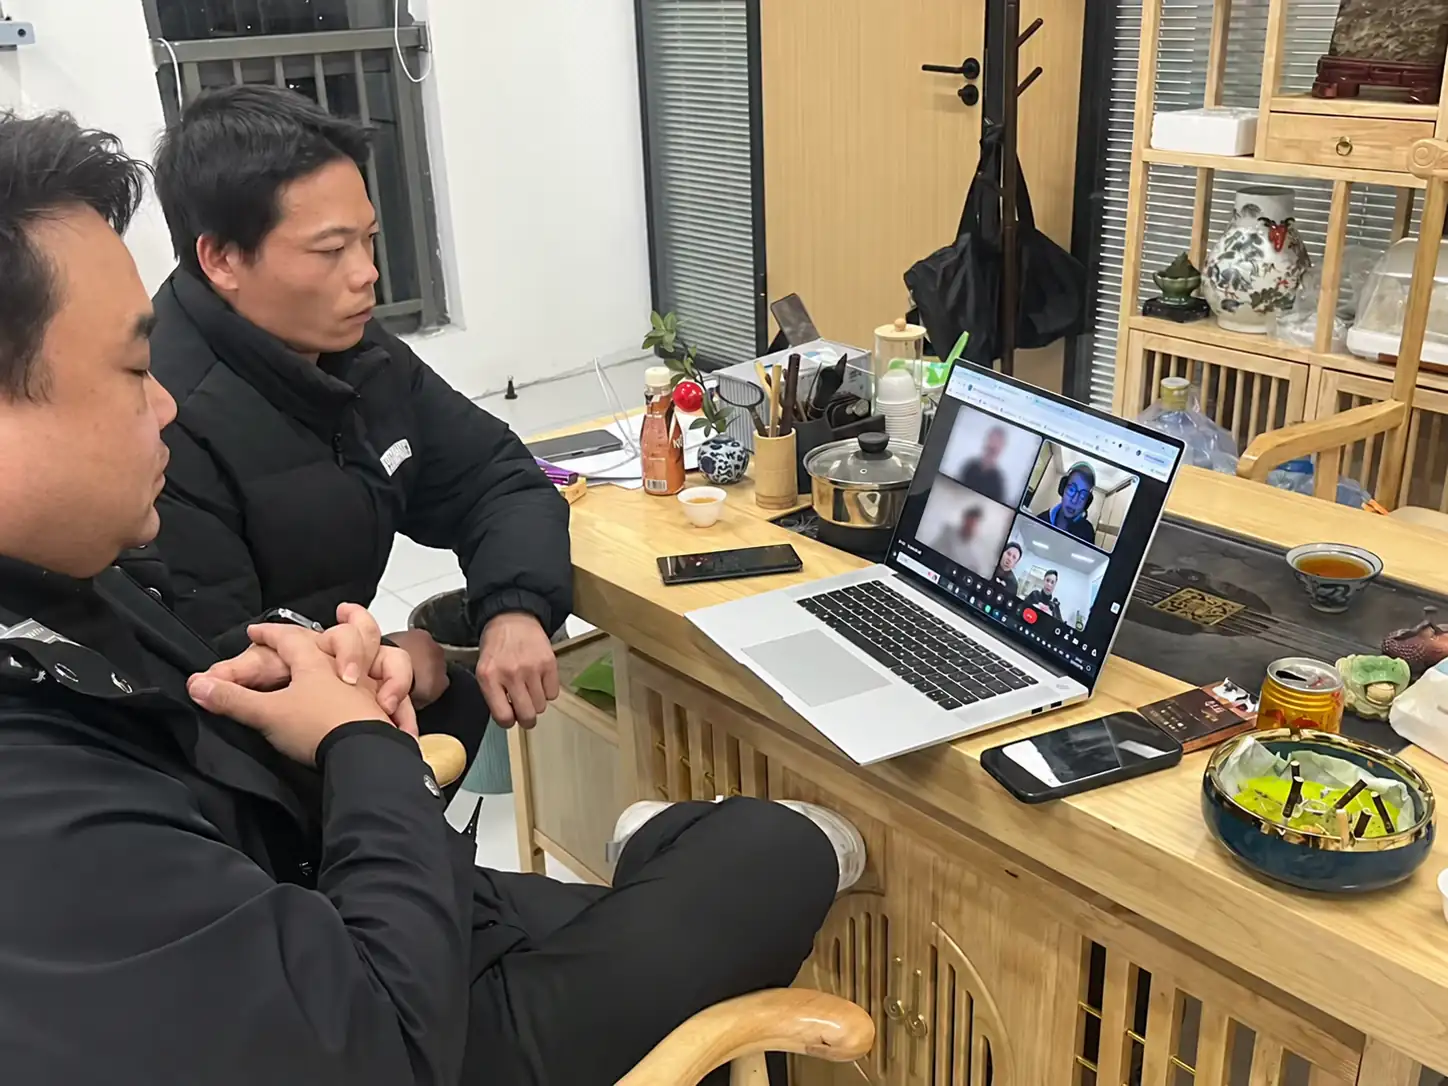
Live Factory Review
Use live video to connect the supplier team to the actual manufacturing environment.
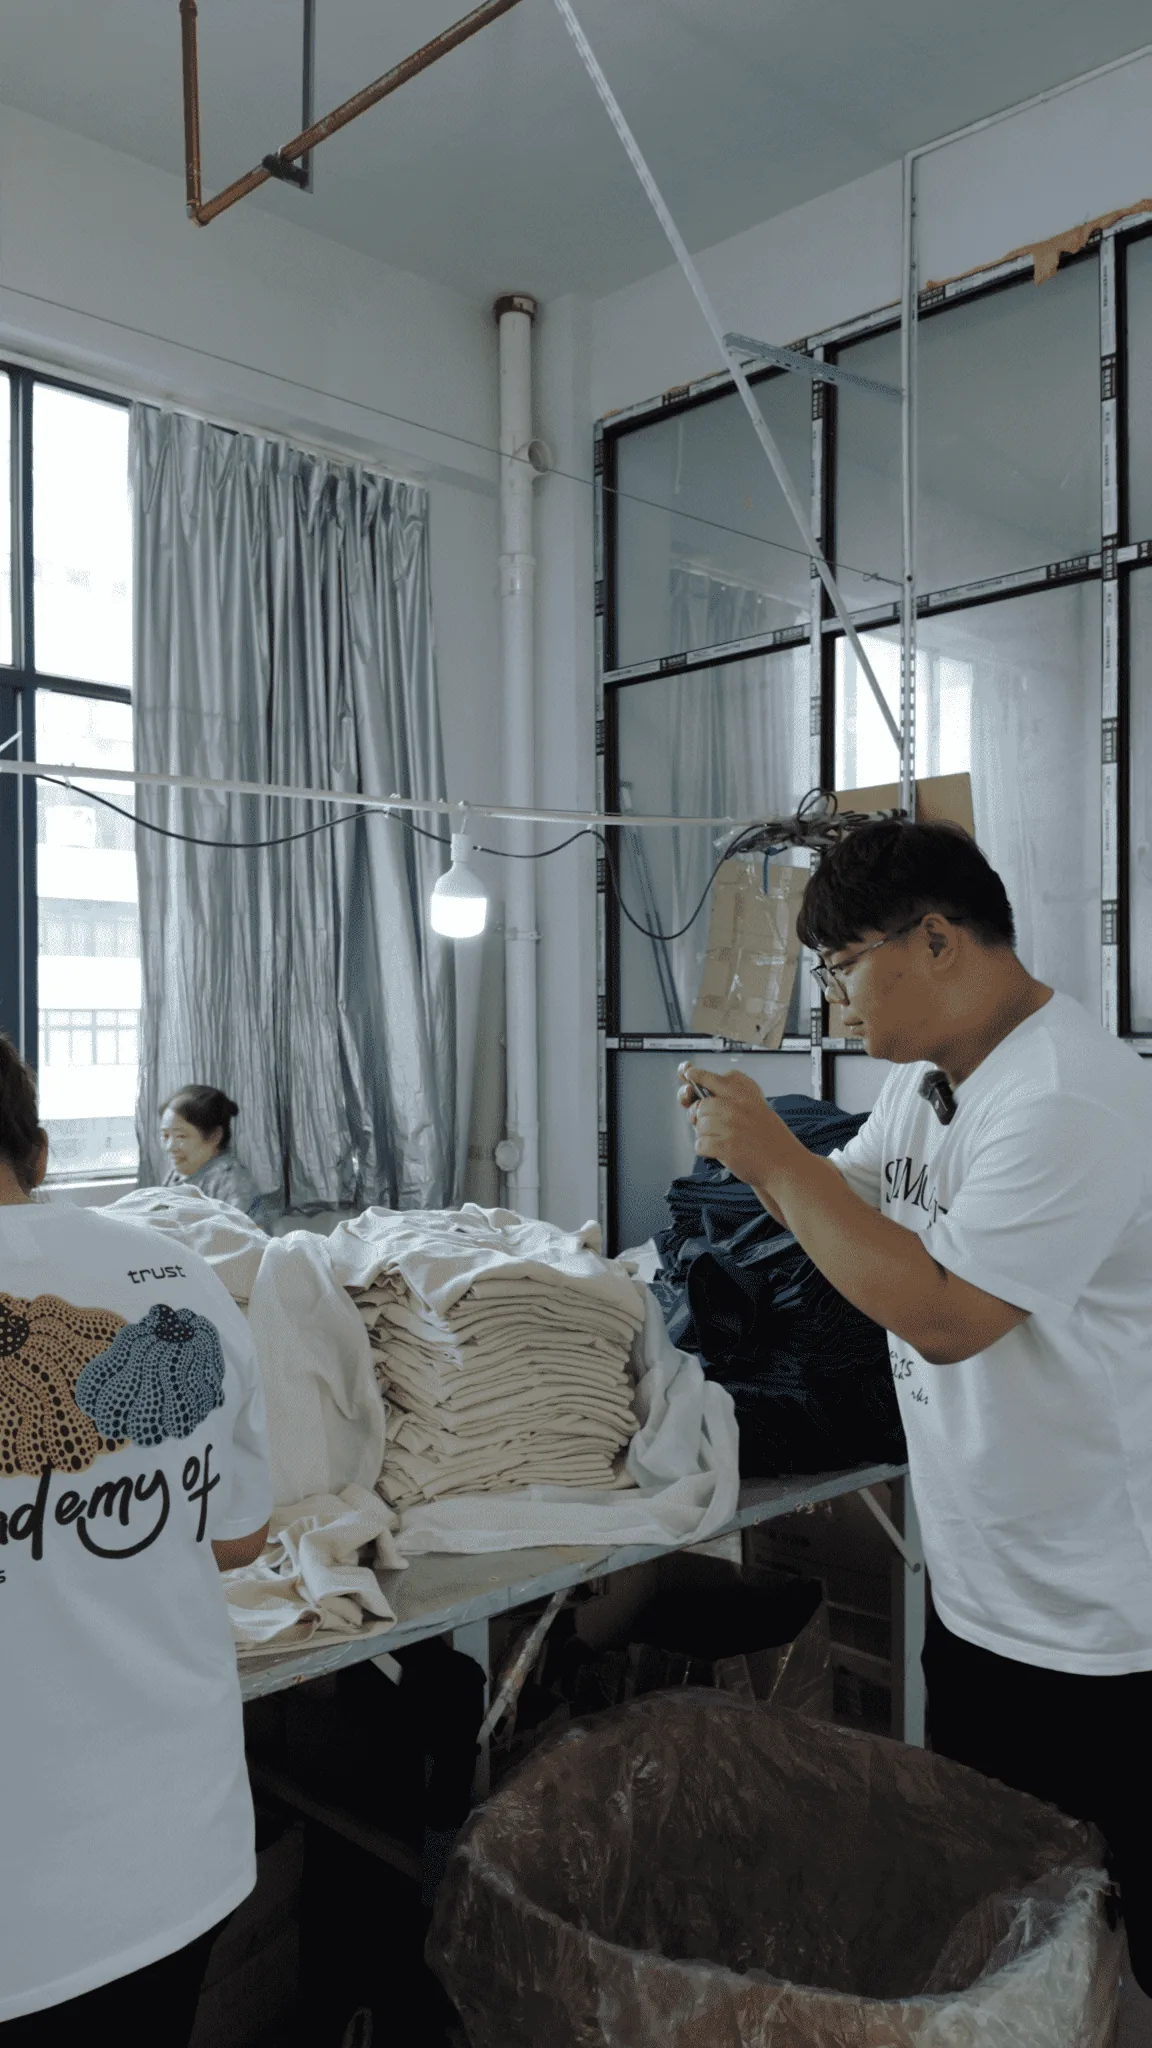
Production Area
Review agreed Seamless or garment-production areas.
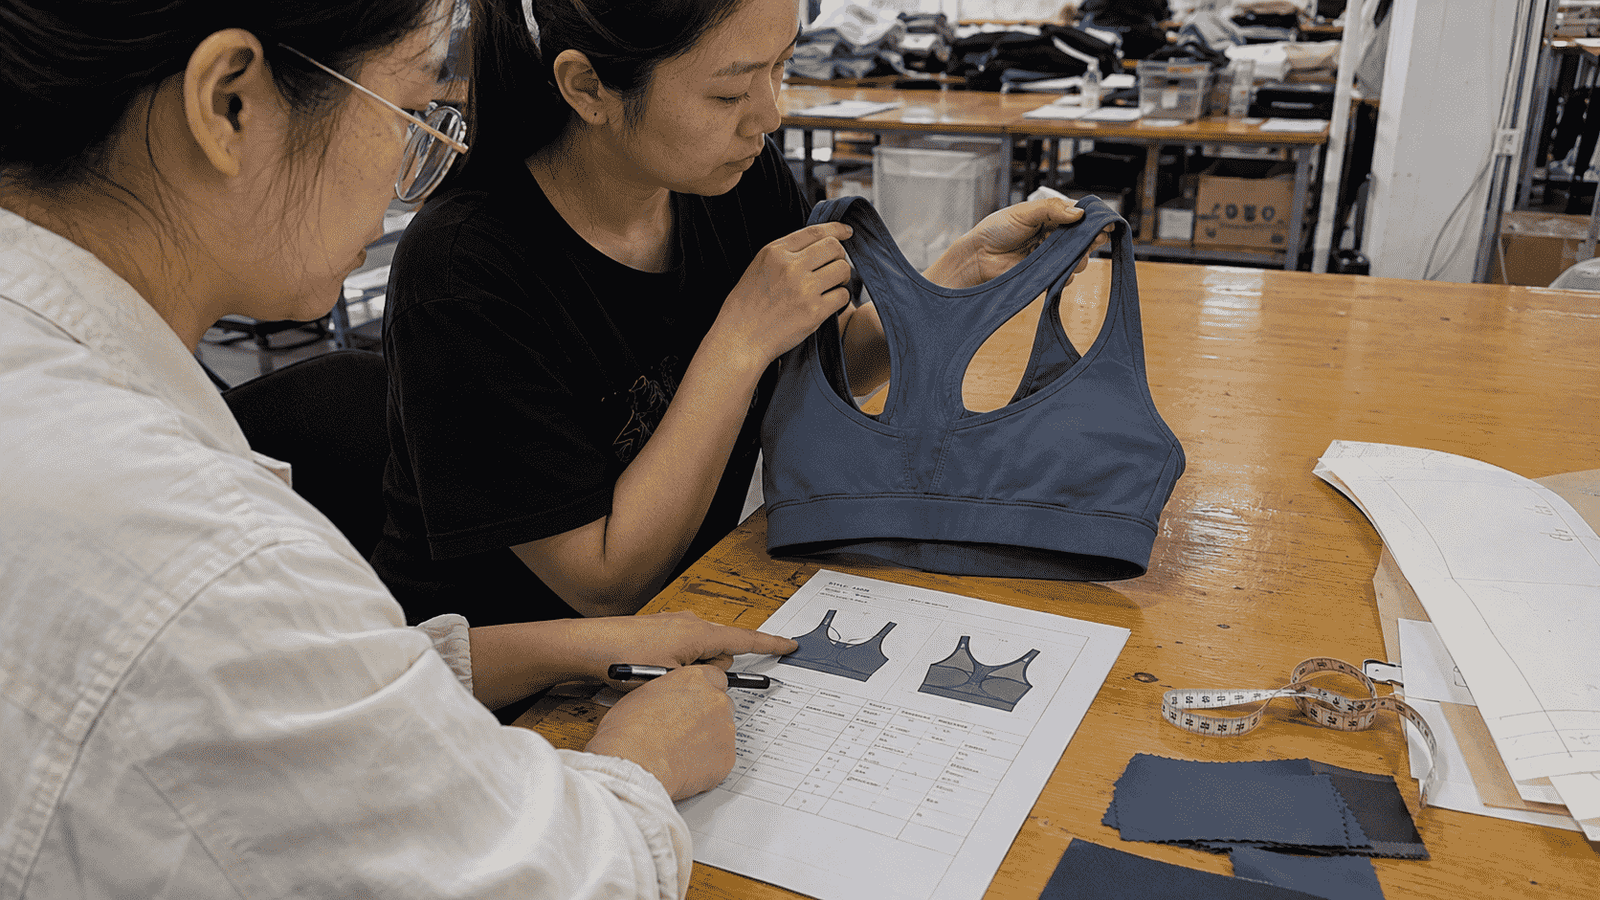
Development Resources
Review relevant sample-development capability where required.

Quality Activity
Review actual measurement, garment-inspection or packing-control practices.
Buyers can identify the factory areas, resources and records they want to see before the session begins. Remote review complements, rather than replaces, any later on-site or third-party review required by the buyer.
Can an Independent Inspector Review the Production Program?
Agreed Third-Party Inspection Can Be Supported
The buyer and MOVEVOX should define the purpose, timing and inspection scope before the review.
This makes the inspection more useful and helps keep unrelated production or confidential customer information outside the agreed scope.

Define the Inspection Scope
Agree whether the inspection covers production, finished garments, packing or another stage.
Use the Current Product Standard
Inspection should refer to the applicable released product and order requirements.
Protect Customer Information
Customer-specific documents should remain within the agreed confidentiality scope.
Inspection Is Not Certification
Inspection support should not be presented as undocumented factory certification.
Keep the Correct Product Version Connected to Factory Execution
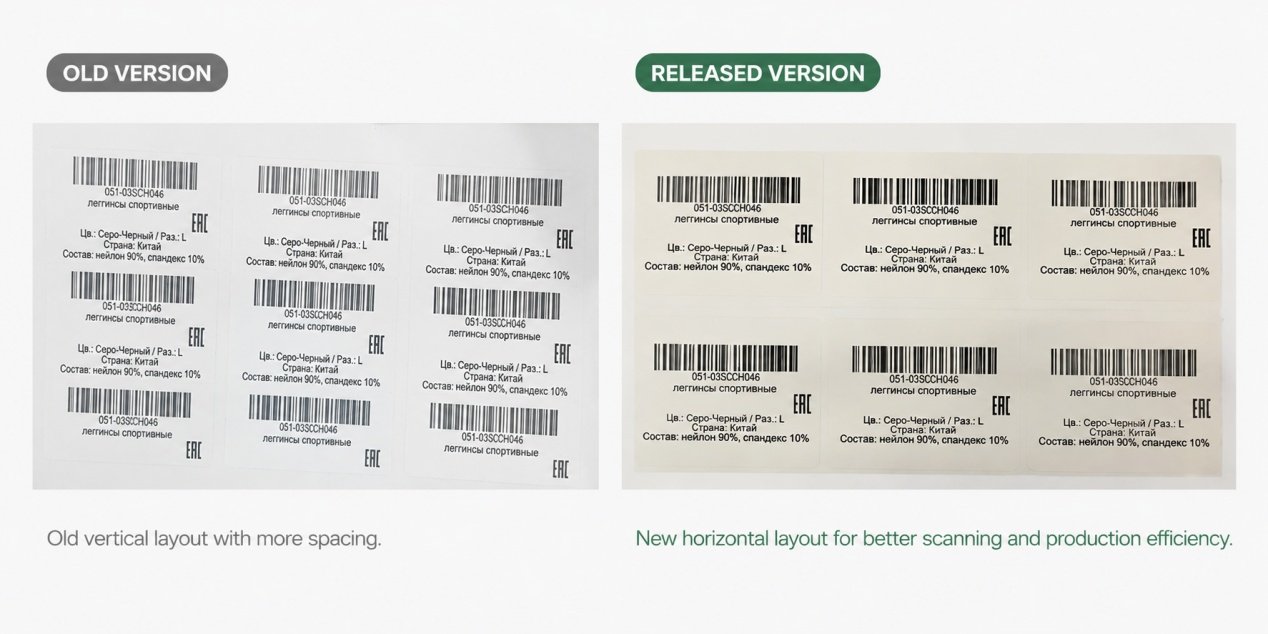
Production-control failures do not always come from poor equipment or workmanship. An obsolete measurement chart, old logo file, incorrect label or outdated product version can also create bulk-production errors.
Approved Reference
Identify the current released product and technical standard.
Version Identification
Keep product, measurement, material and brand information aligned.
Obsolete Information
Separate old or hold versions from current production information.
Change Approval
Review relevant changes before they enter production.
Production Access
Ensure production and QC work from the current released information.
Commercial Complexity
Document control becomes increasingly relevant across multiple styles, revisions, colors and repeat orders.
Connect the Approved Product Standard to Bulk Production
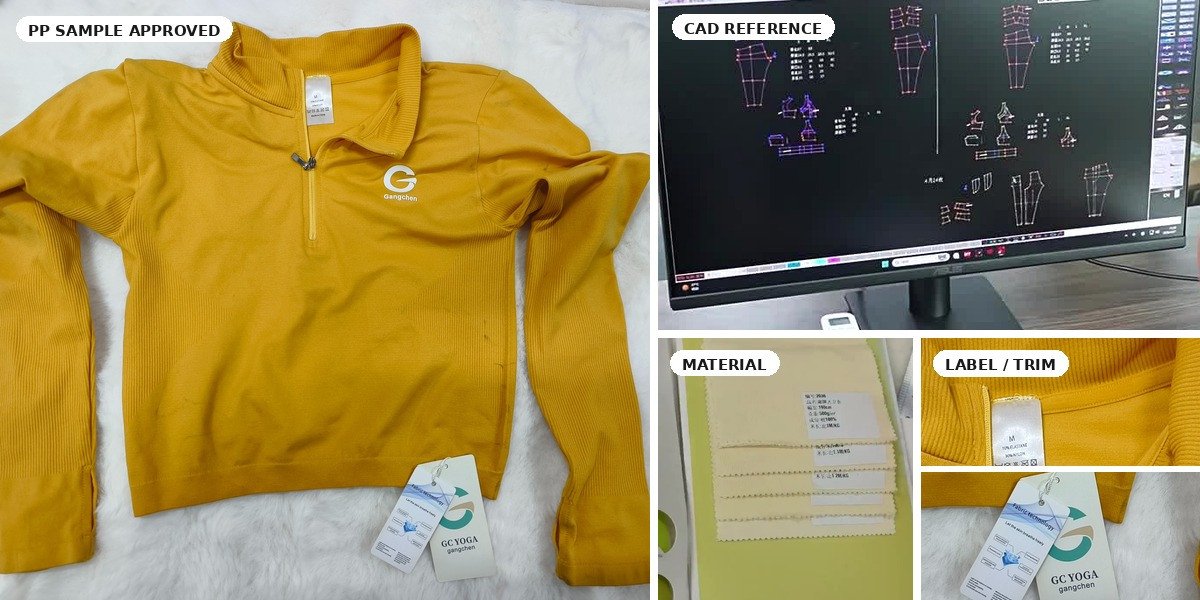
This module intentionally begins after product development is approved. The factory-level question is whether that approved standard remains identifiable when the order moves into manufacturing.
Approved Product
The current physical sample should remain identifiable where it forms part of the production standard.
Production Reference
Measurements, manufacturing information and applicable materials should refer to the same released version.
Quality Reference
First-production and bulk-quality reviews should compare against the applicable approved standard.
The Manufacturer page can explain how a product reaches approval. The Factory page shows what happens after approval: whether the approved standard remains connected to production.
Confirm Material Readiness Before Production Allocation
This is not a yarn-engineering module. The factory-level issue is whether the already selected material direction is available, identifiable and linked to the correct order before production begins.
Approved Direction
Confirm the current yarn or fabric reference.
Physical Color Standard
Use the relevant physical color reference where applicable.
Lot Identification
Maintain material-batch identification where required.
Incoming Review
Check relevant incoming material requirements before production use.
Order Allocation
Connect the material to the correct style and production order.
Production Release
Proceed after the applicable material requirements are confirmed.
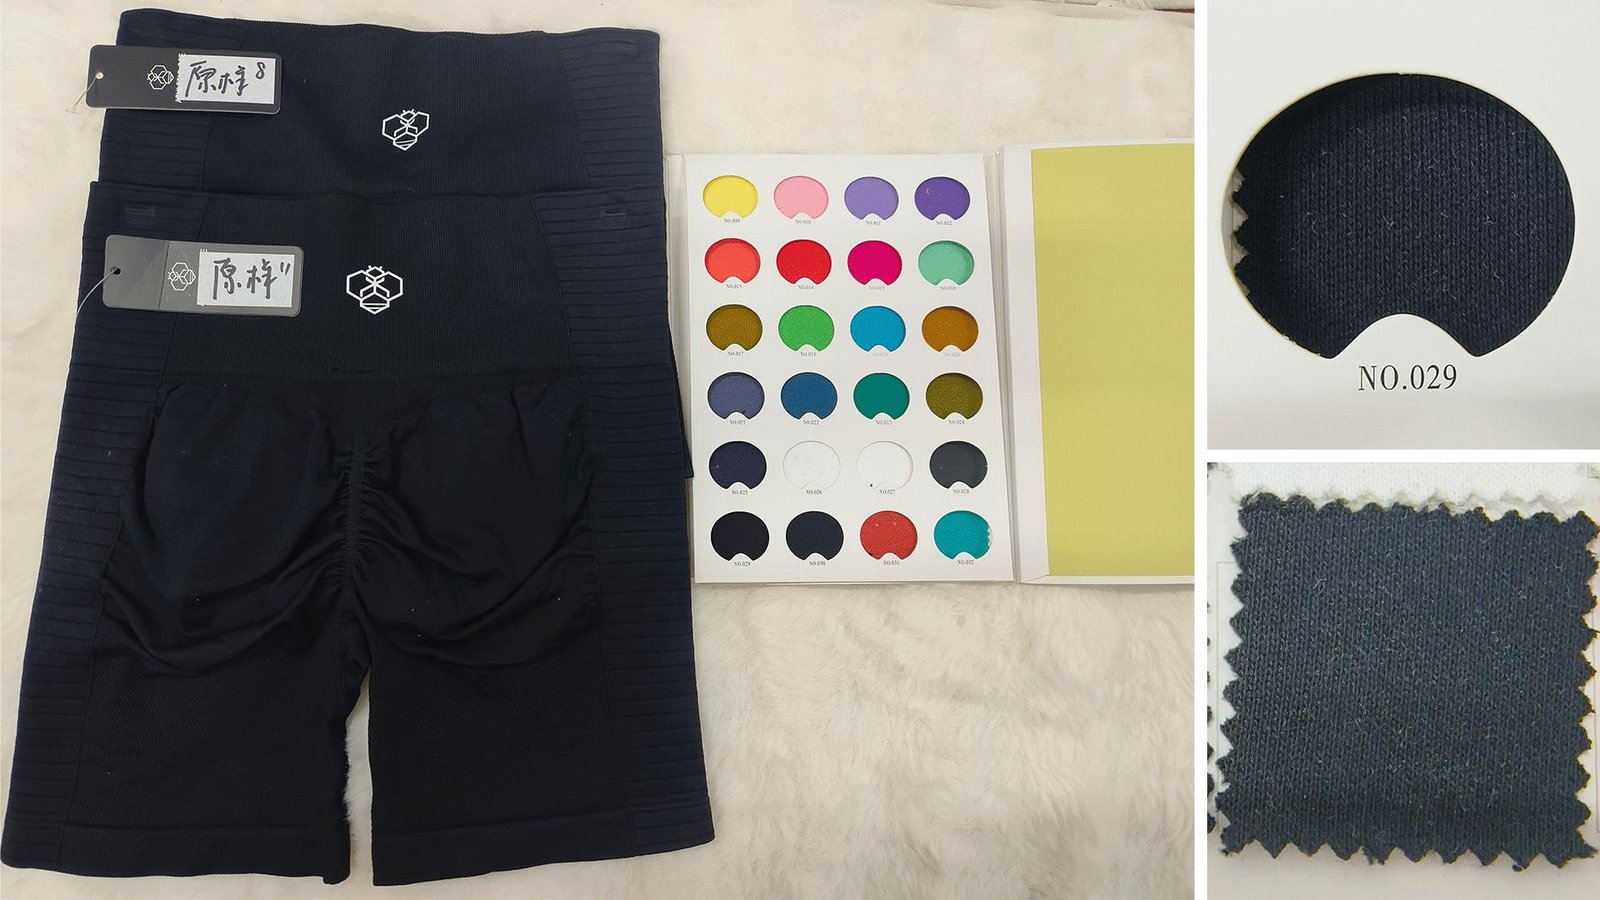
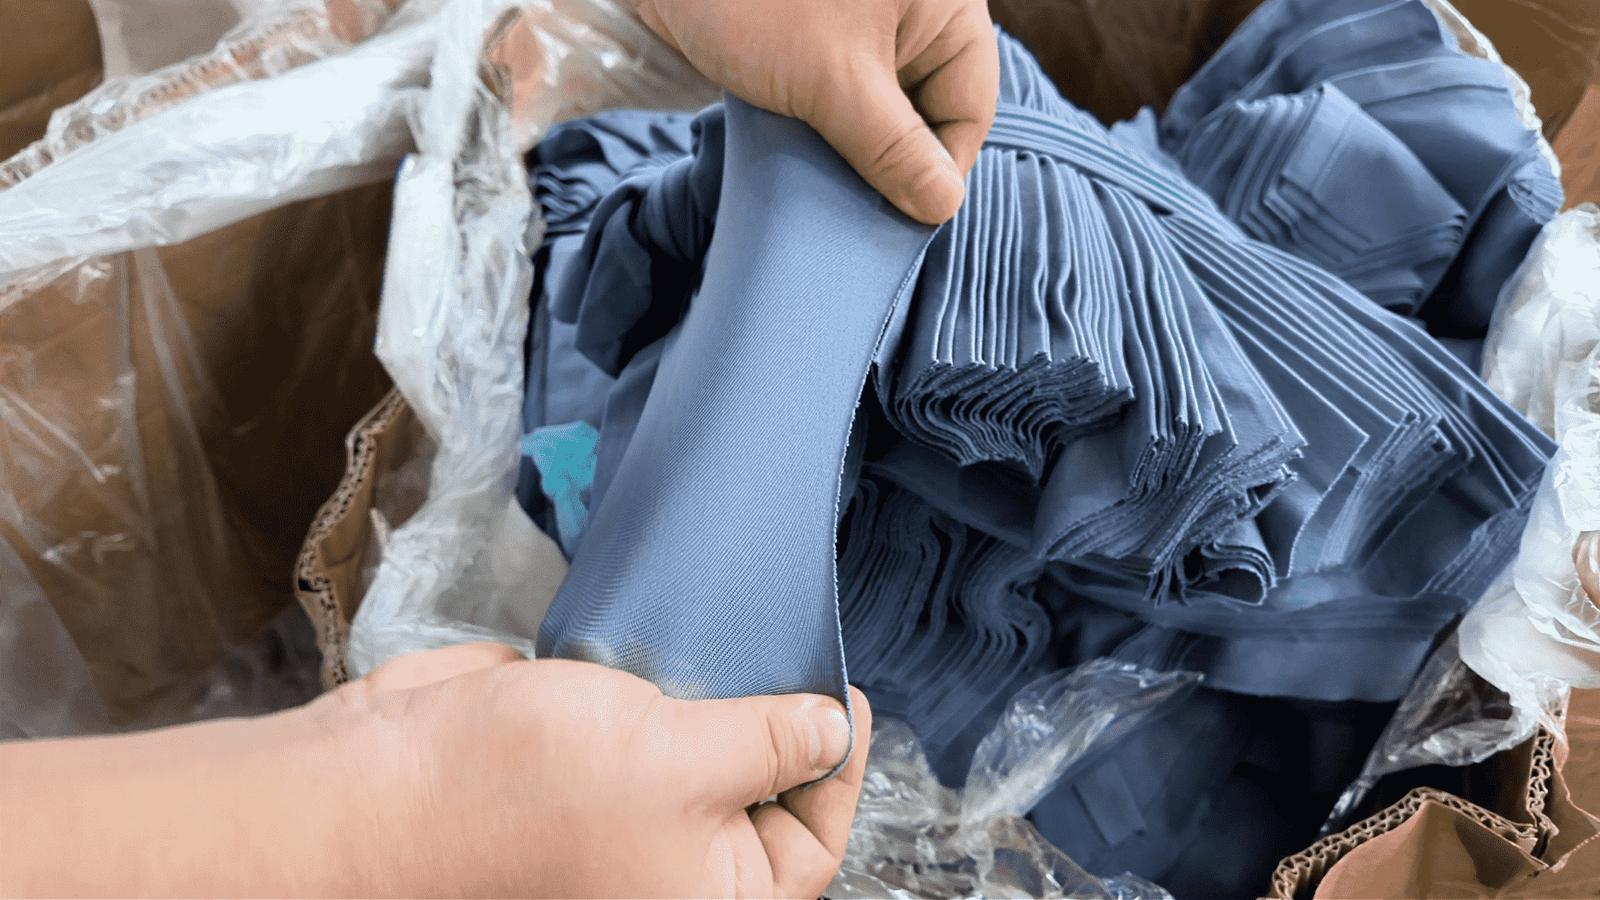
Custom color is often assessed around the 400–600-piece level, but actual feasibility depends on the yarn, material, style and order structure.
Align Production and Quality Requirements Before Bulk Starts
The pre-production release review connects the approved commercial product to the factory teams responsible for execution.
Released Product
Confirm the current approved product reference.
Material Readiness
Confirm relevant production materials and colors.
Manufacturing Route
Confirm the applicable Seamless or Cut & Sew process.
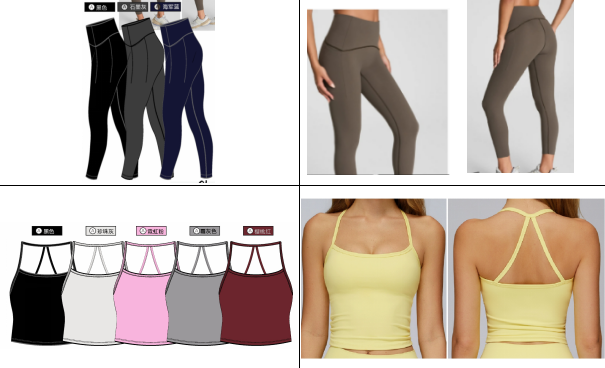
Quality Checkpoints
Define the relevant first-production, in-line and final controls.
Brand and Packing Information
Confirm applicable labels, SKU, barcode and packaging requirements.
The purpose is not to repeat sample development. It is to verify that the information being released to manufacturing is consistent before resources are committed to bulk production.
Check Initial Production Before the Order Scales
An early production gate gives the factory an opportunity to identify execution problems before they affect a larger quantity.

Review Initial Production
Review product identity, relevant measurements, manufacturing execution, workmanship and applicable branding details.
AFTER APPROVALContinue the Main Production Run
Continue bulk production against the released standard and agreed quality controls.
The exact first-production review depends on the product and buyer requirements. The objective is risk reduction—not a claim that every possible defect can be prevented through one inspection stage.
Track the Order While Production Is Still in Progress
Waiting until final inspection to understand production status can leave fewer options for correction. Work-in-progress control keeps order progress, production allocation and relevant quality activity visible while manufacturing remains active.
Released Order
Style, quantity, route and production requirement confirmed.
Material Ready
Applicable inputs available for manufacturing.
Initial Production Reviewed
Early output checked where required.
Bulk WIP
Production progress and relevant quality risks monitored.
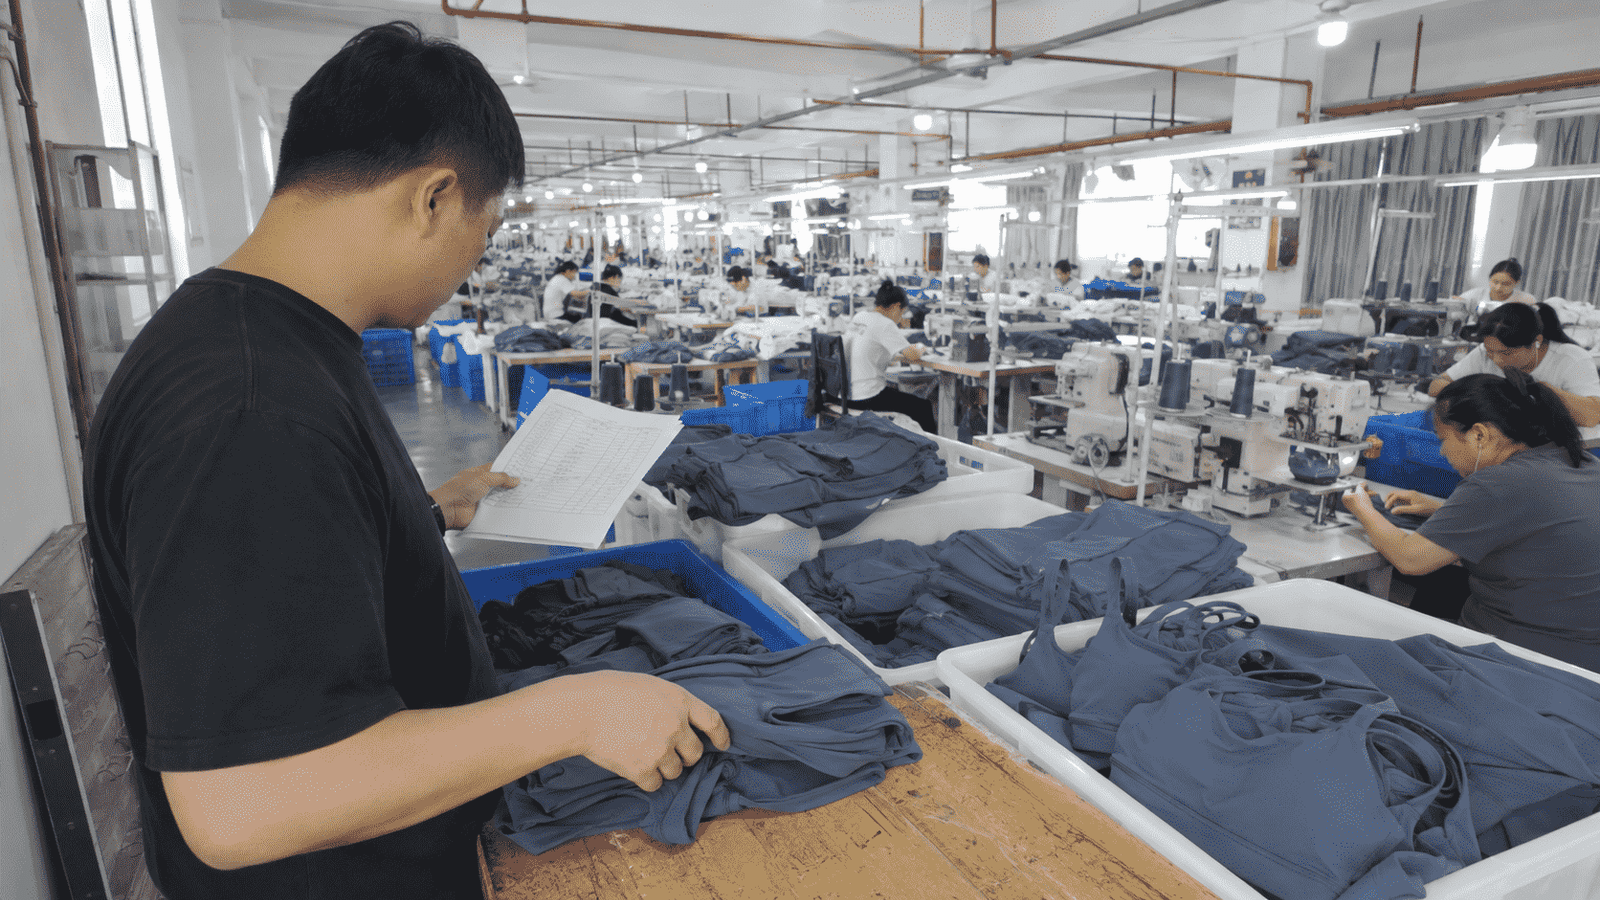
Final Review
Finished-product requirements are reviewed according to the applicable project.
Packing Release
Applicable packing and product-identification requirements are reviewed before release.
Make Quality Records Reviewable by Production Stage
“We inspect every order” is a weak supplier statement if there is no way to understand what the inspection refers to. Records become more useful when they are connected to a production stage and product identity.
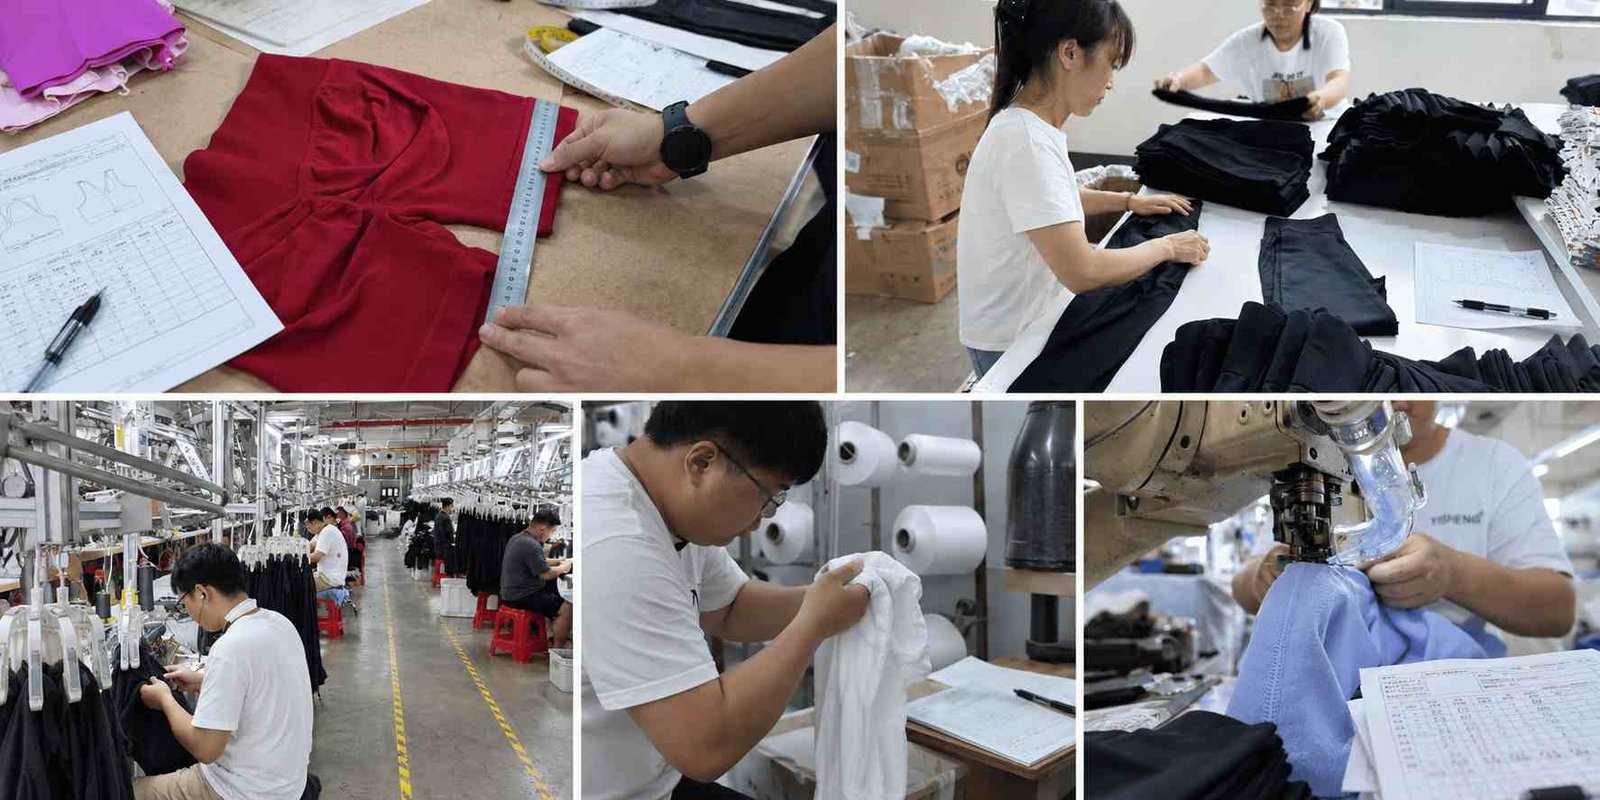
Initial Production Record
Document relevant findings before wider production.
In-Line Record
Record relevant production findings and follow-up.
Measurement Record
Connect applicable garment dimensions to the current standard.
Final Inspection Record
Document relevant finished-product or packing findings.
Version Reference
Where appropriate, records can identify the product, style, color, size, SKU or production version involved.
Customer-specific information should be anonymized before being used as public supplier evidence.
Connect the Purchase Order to Production and Shipment Evidence
For multi-SKU and repeat programs, traceability should extend beyond the production floor. The commercial order should remain connected to the correct product, production activity, inspection and shipment preparation.
Purchase Order
Start from the released commercial requirement.
Style / SKU
Identify the correct commercial product.
Production Batch
Connect manufacturing activity to the relevant order.
Inspection
Link quality evidence to the applicable production scope.
Carton
Maintain commercial identification through packing.
Shipment
Keep the commercial order connected through final release.
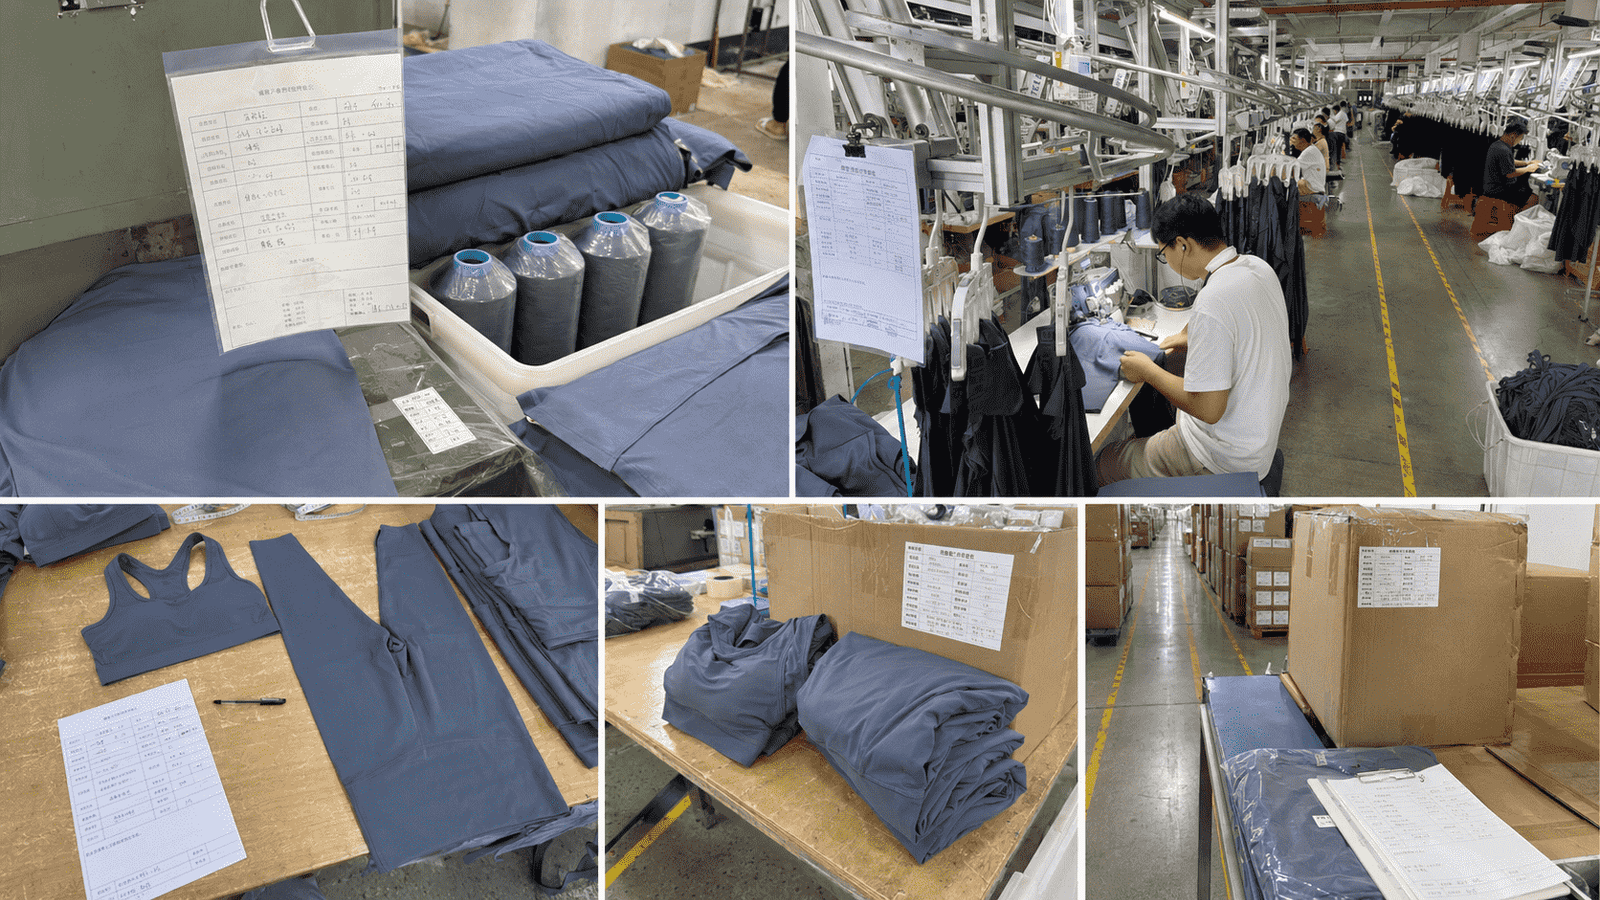
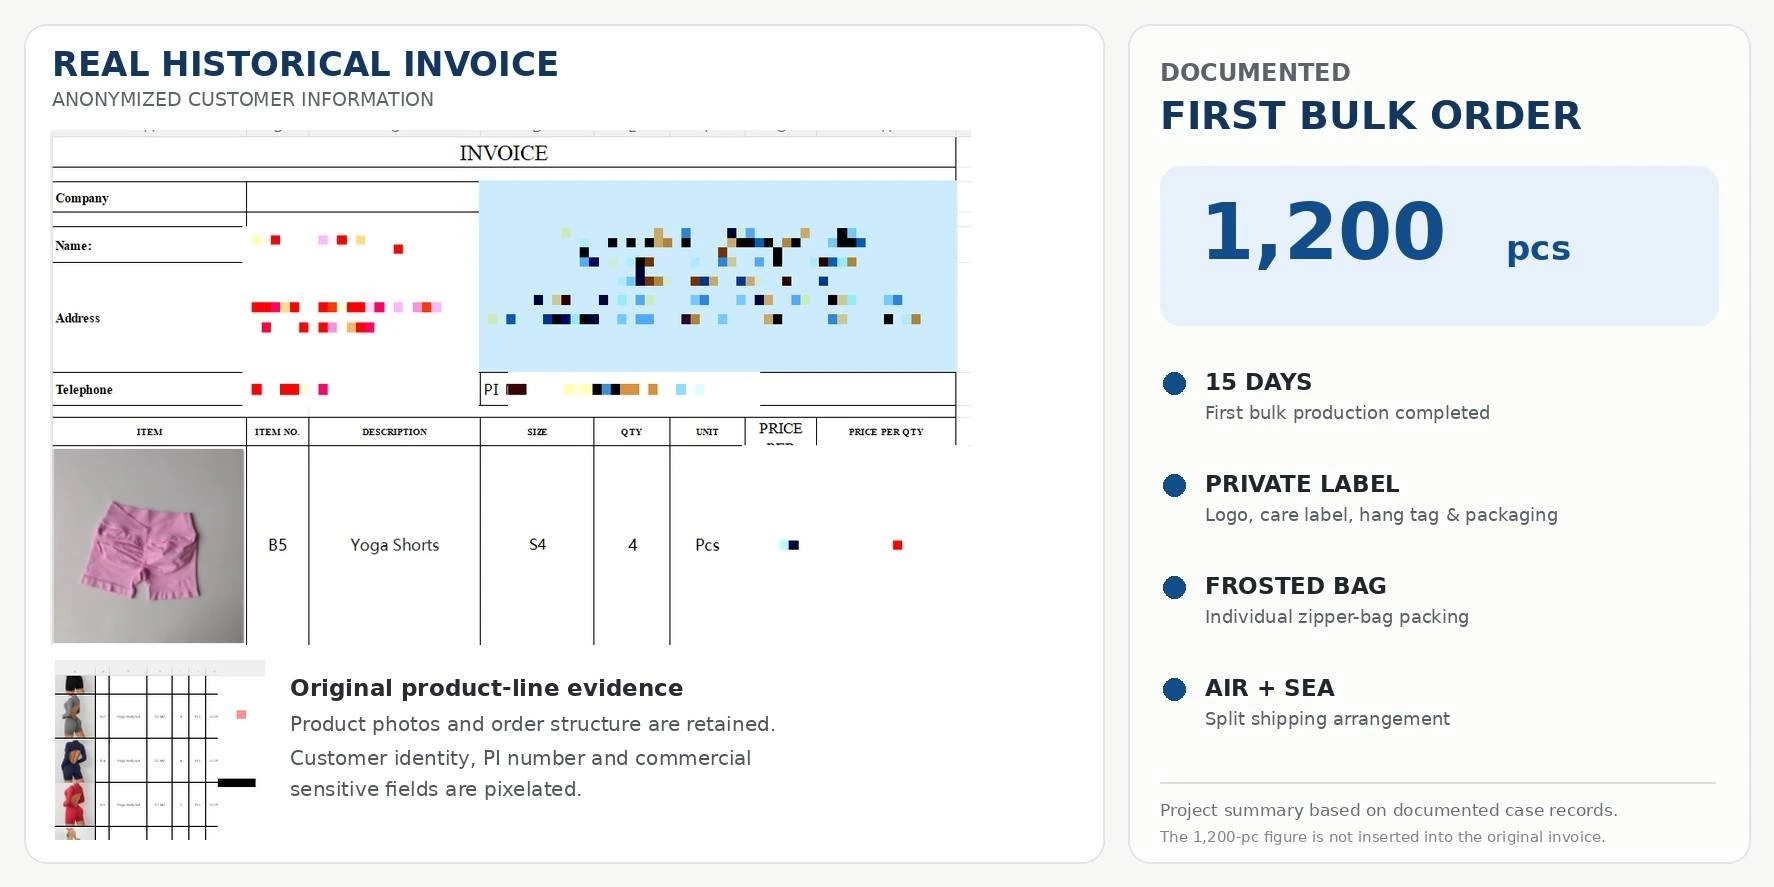
The exact documentation structure can vary by project.
Keep Packed Units Connected to the Correct SKU
Packing mistakes can create commercial problems even when the garment itself is correct. For multi-style, multi-color and multi-size programs, carton and SKU traceability remains part of factory execution.
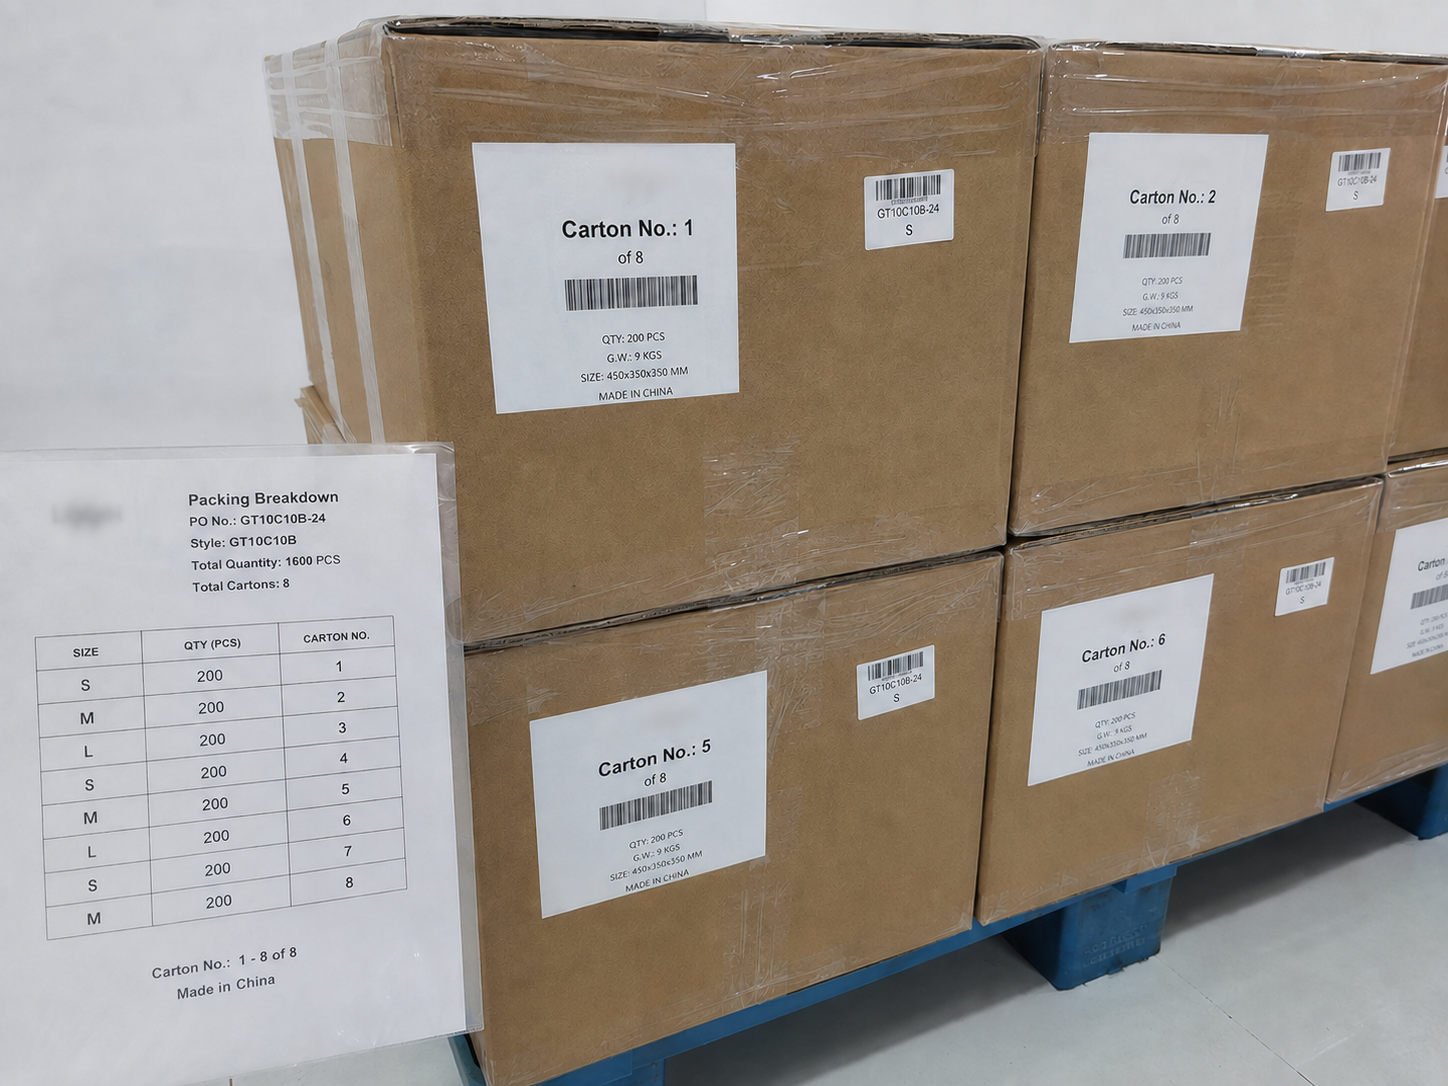
Carton Identification
Match carton information to the relevant SKU and packing breakdown.
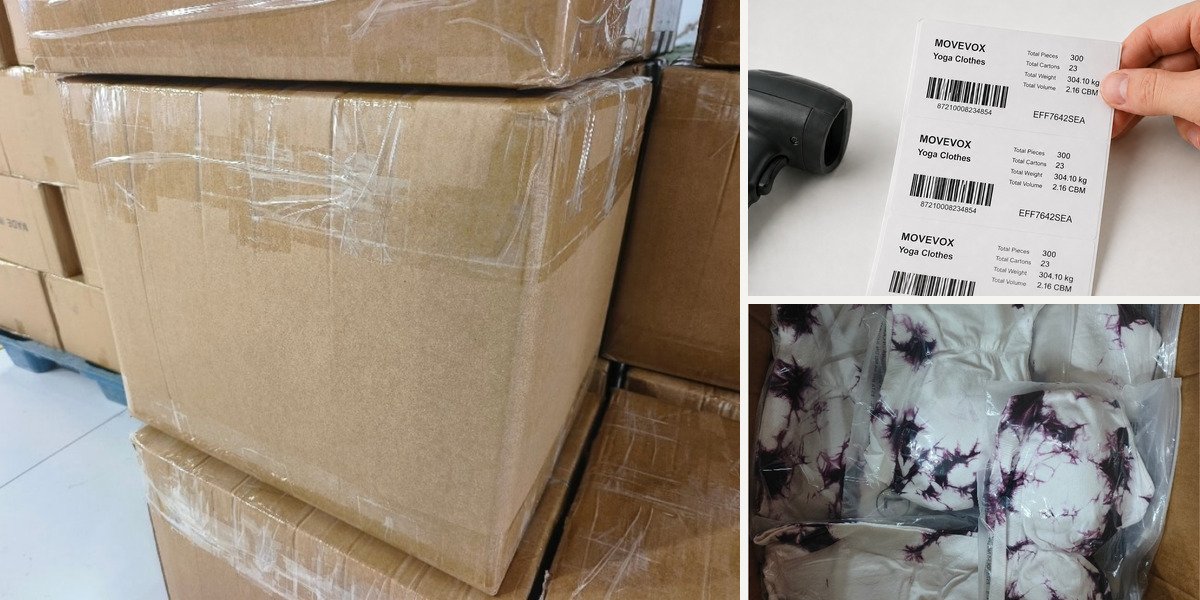
Finished Cartons
Review carton condition and identification where relevant.
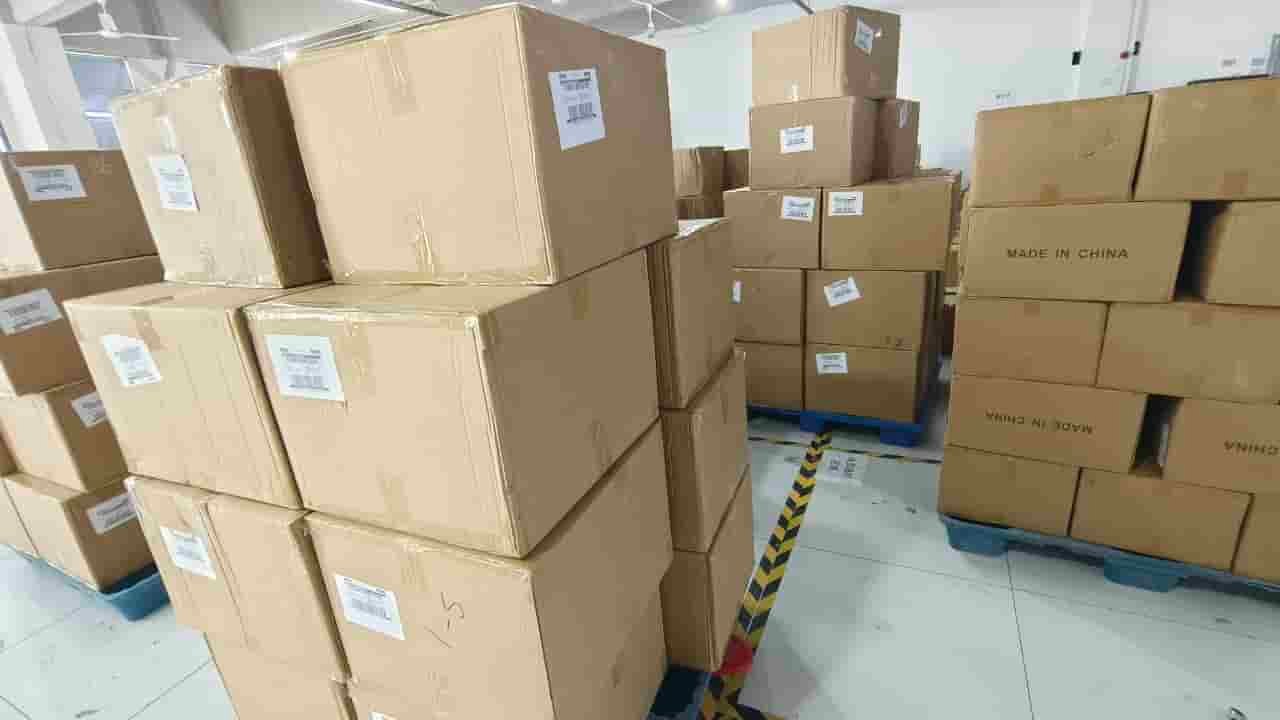
Shipment Preparation
Maintain product identification through final warehouse or handoff preparation.
Quantity Reconciliation
Applicable packed quantities should be confirmed before release.
Scale Through Planned Production Allocation
For larger programs, the value of capacity is not the headline number alone. It is whether production can be allocated and controlled against the actual commercial program.
Initial PO
Confirm product, SKU structure and commercial requirements.
Repeat Forecast
Review likely follow-on demand where available.
Production Allocation
Match appropriate production resources to the program.
Initial Output at Scale
Review early output after a significant allocation change where relevant.
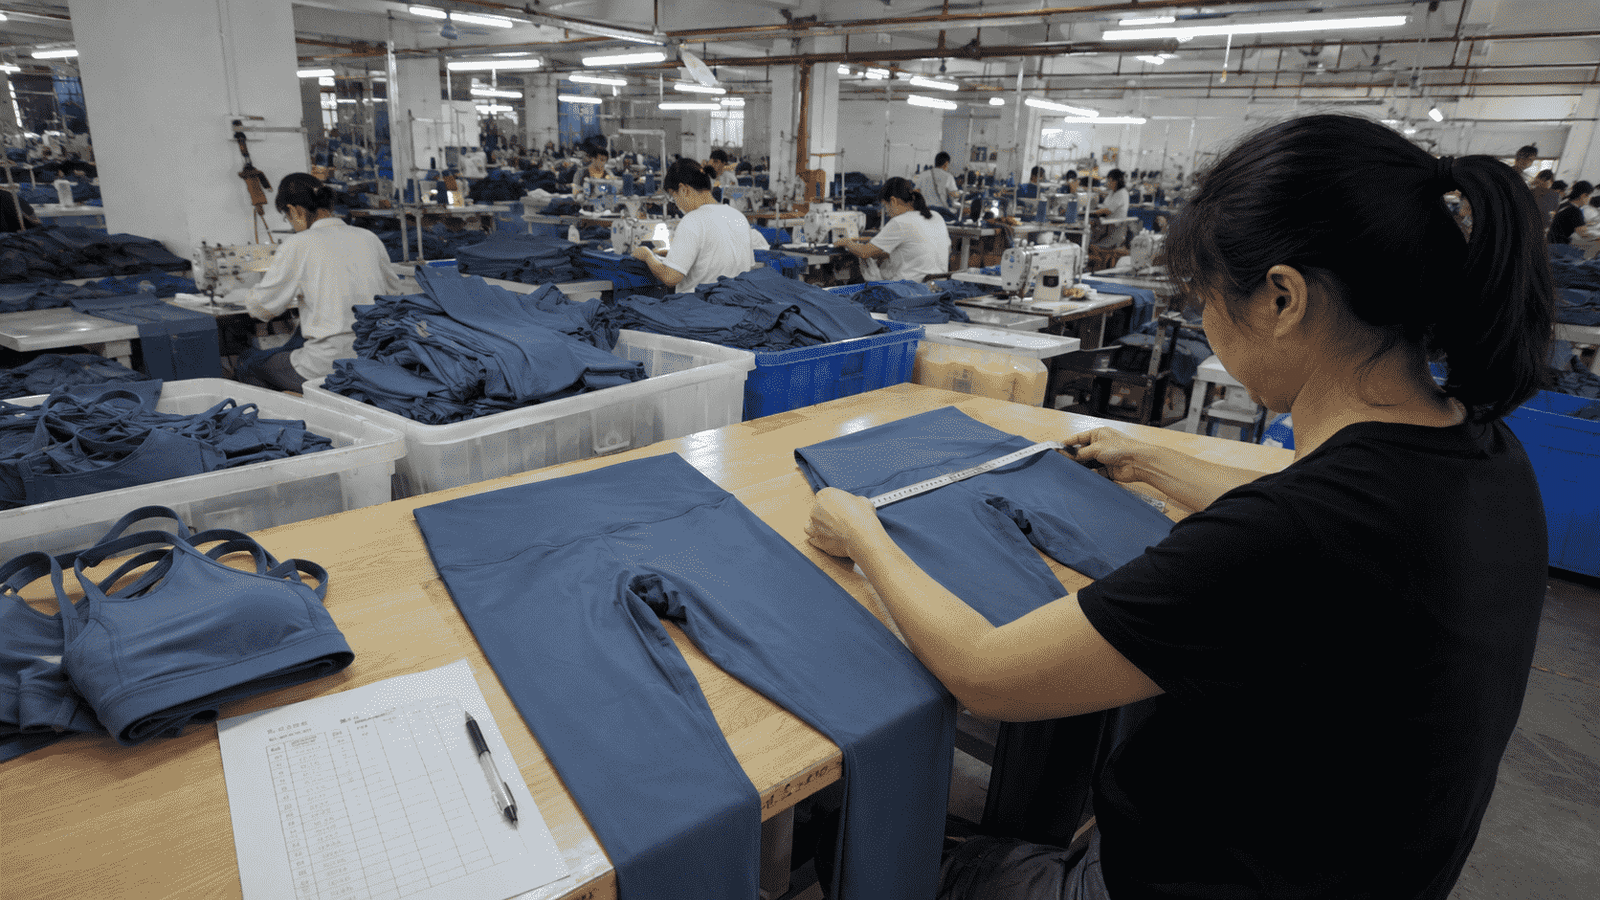
Managed Stable Monthly Delivery Capacity
MOVEVOX's managed stable monthly delivery capacity is approximately 150,000–200,000 pieces under normal conditions.
This figure describes managed stable delivery capacity, not theoretical maximum equipment output.
QC and Next Program
Execution evidence from the current program can support subsequent repeat planning.
Match Compliance Evidence to What Was Actually Tested
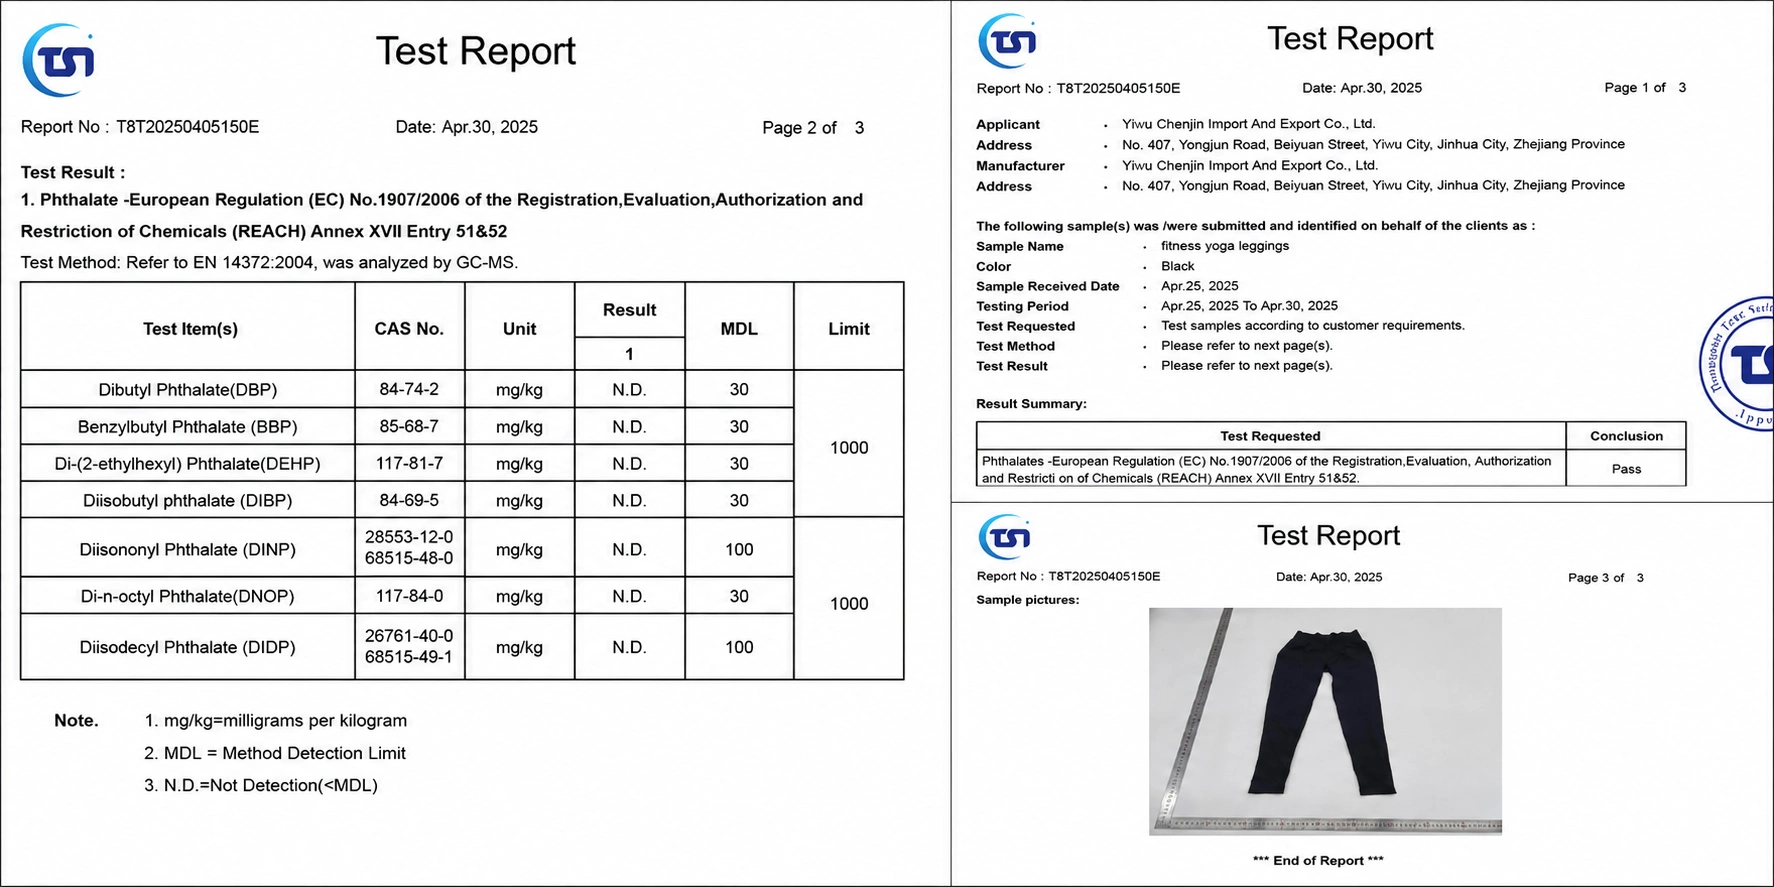
For professional procurement, displaying a certificate image is not enough. The buyer should understand what was tested, which sample was involved, what test scope was used and whether the evidence is relevant to the product under review.
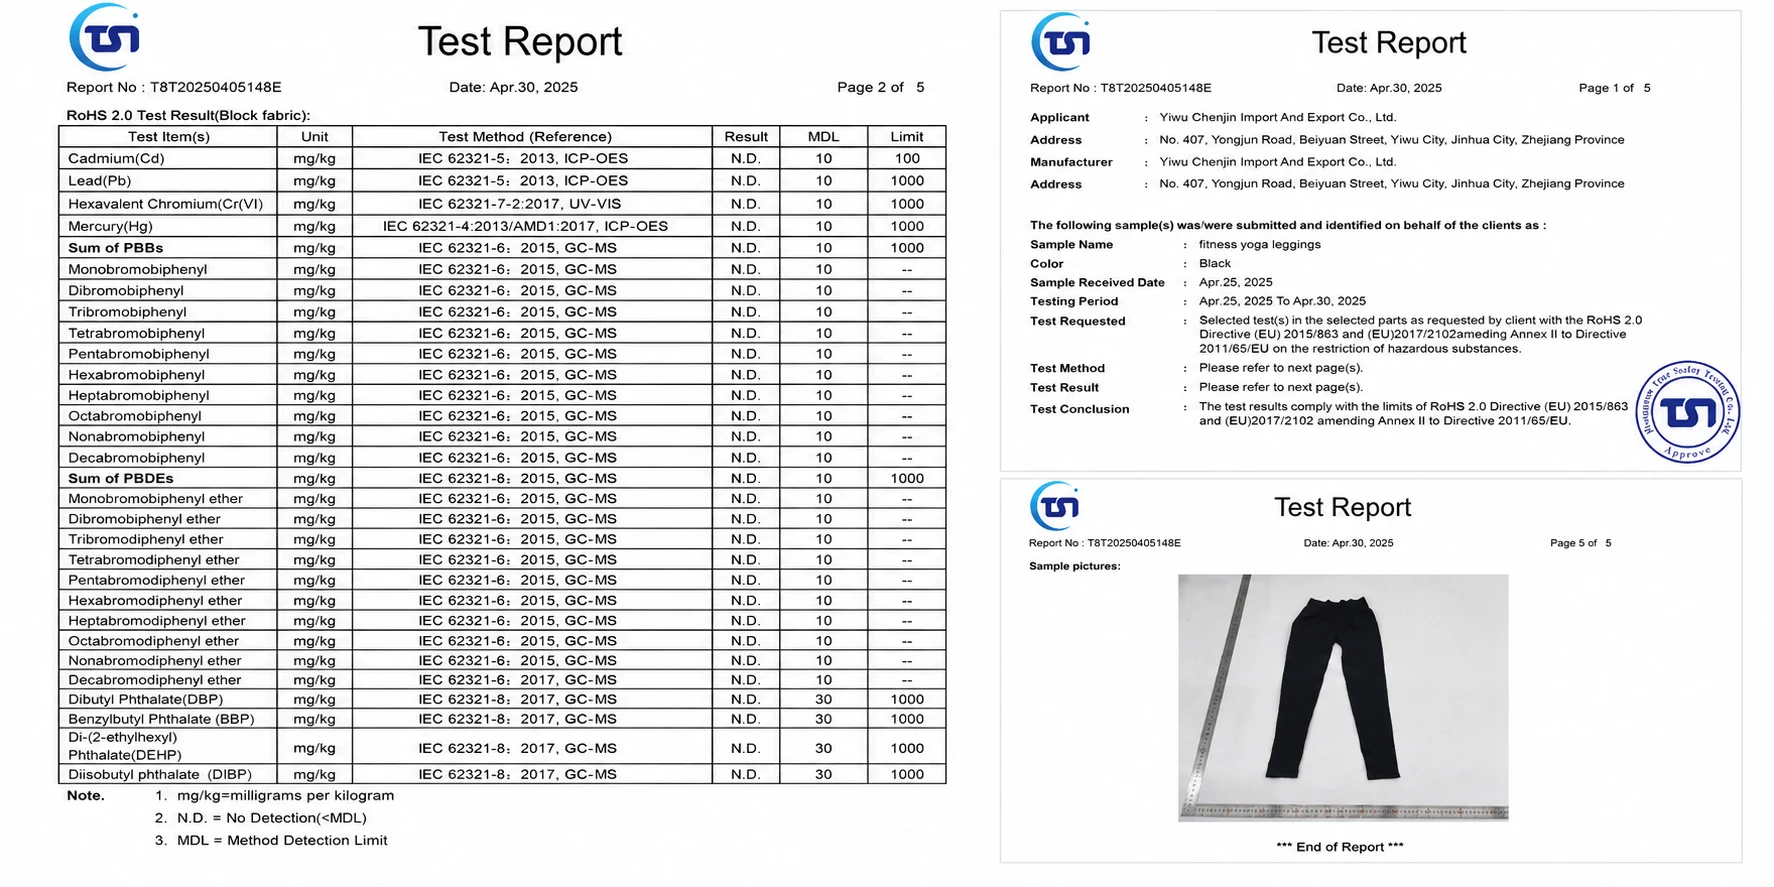
RoHS Evidence
RoHS Certificate/Report TST20250405148EC / TST20250405148E, dated April 30, 2025, relates to a tested black fitness yoga leggings sample.
REACH Phthalates Evidence
REACH Annex XVII Entry 51 & 52 report TST20250405150E, dated April 30, 2025, relates to black fabric from the tested fitness yoga leggings.
Evidence Boundary
The available reports apply to the stated sample and test scope.
Not Blanket Factory Certification
They should not be presented as certification covering every product or future production.
Organize Supplier Evidence by What It Actually Proves
Not every procurement question should be answered with the same type of evidence. An effective vendor file separates legal identity, manufacturing proof, production-control documents, quality evidence and product testing.
Company Identity
Evidence relating to the commercial supplier entity.
Factory Evidence
Physical factory, machine and operating-environment evidence.
Production Evidence
Current product standards and production-control references.
Quality Evidence
Applicable inspection or measurement records.
Product Testing
Sample-specific testing interpreted within the relevant scope.
Factory Review Options
Visit, remote review and agreed third-party inspection support.

This structure gives sourcing teams a clearer picture of what has actually been verified and what may still require additional review.
Extend Factory Control Through Packing and Shipment Release
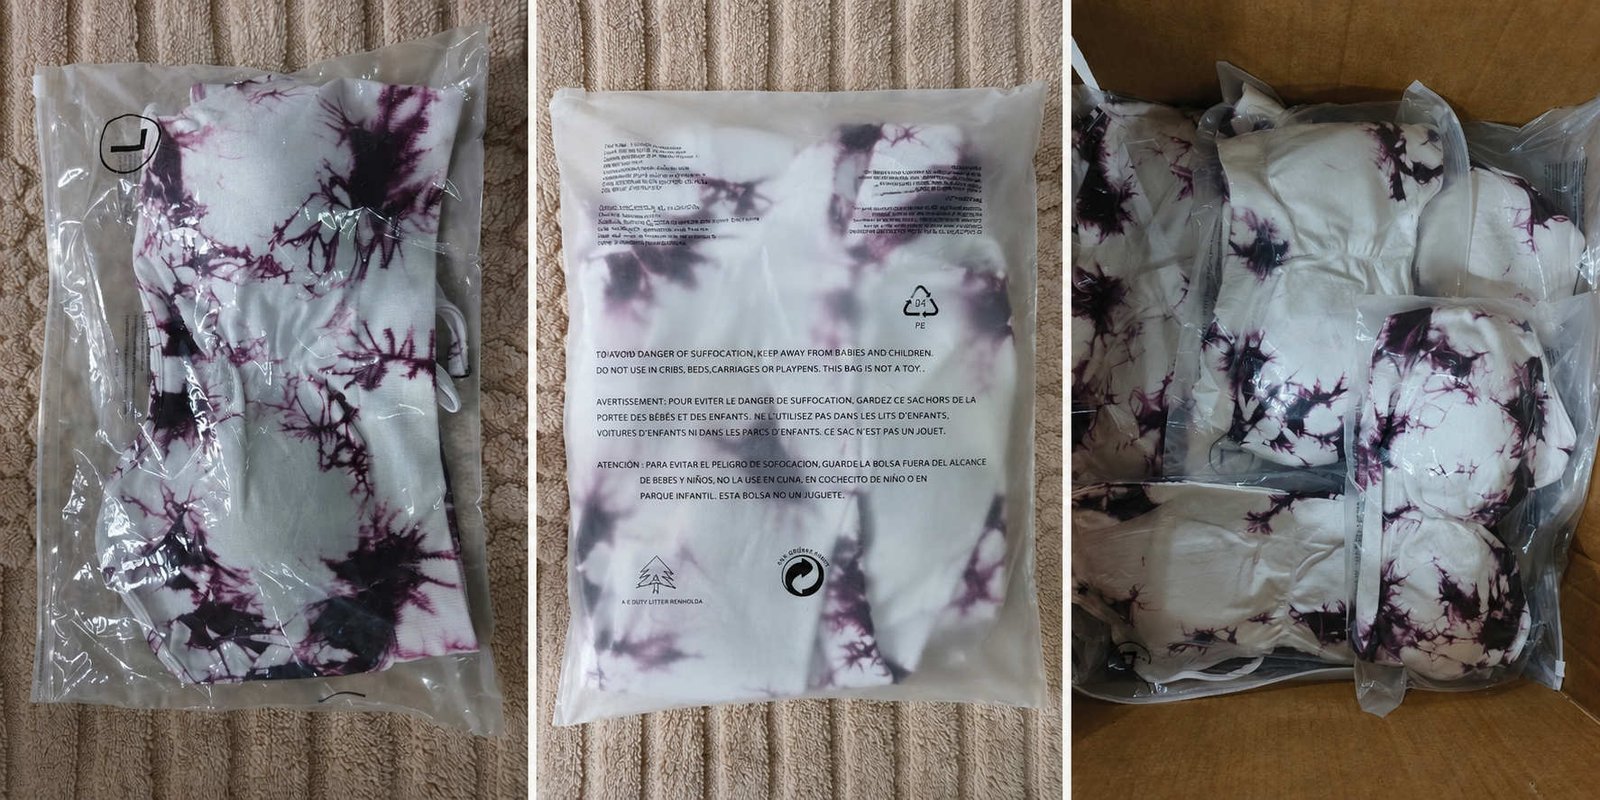
Factory execution does not end when the garment passes workmanship inspection. For private-label programs, product identification and agreed packaging requirements must remain connected to the correct commercial product.
Unit Packaging
Confirm the applicable individual packing and product identification.
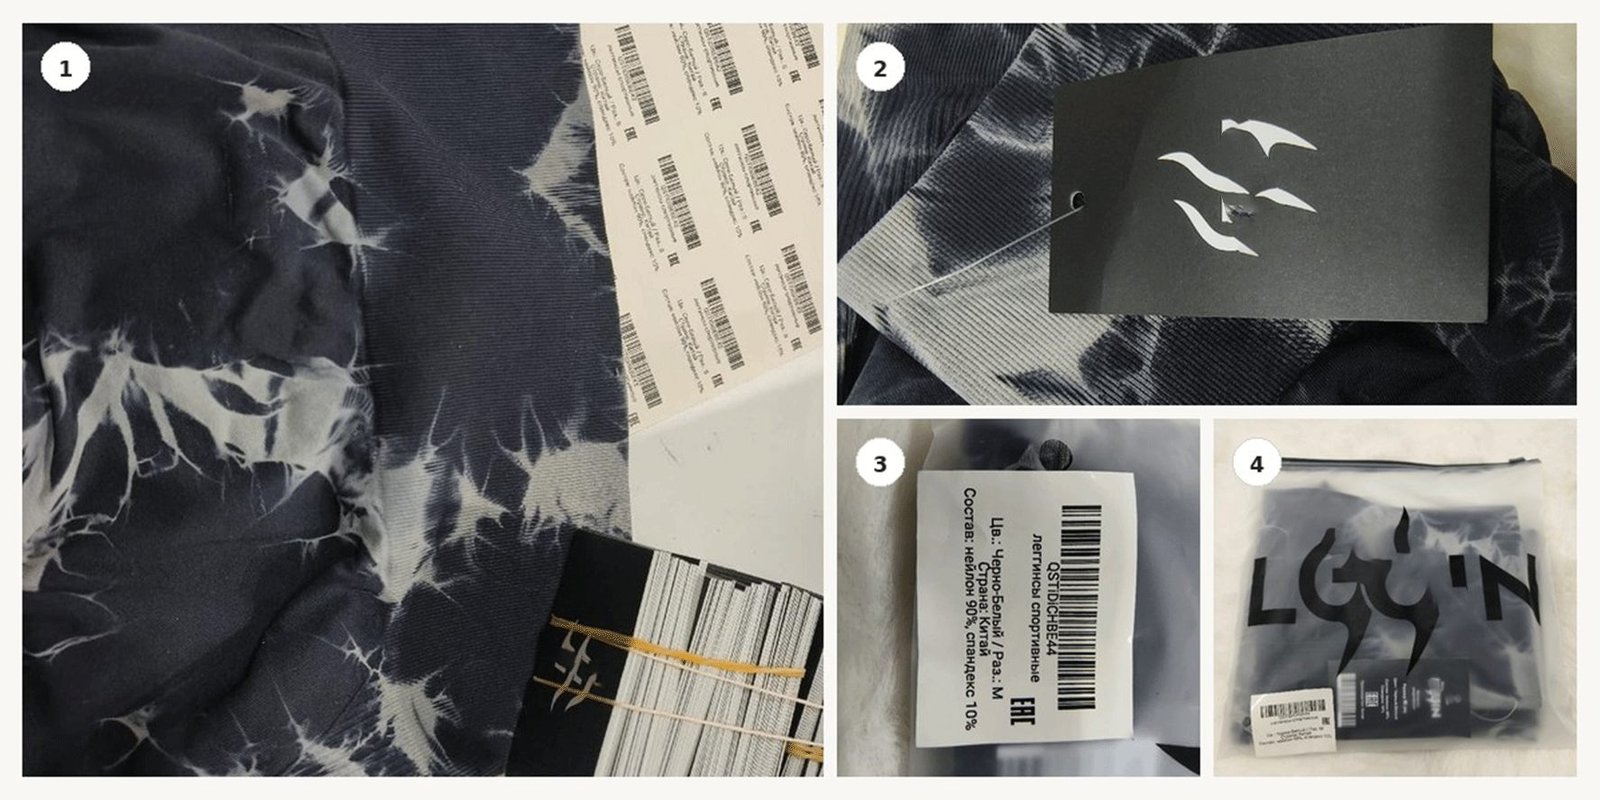
SKU Reconciliation
Keep garment, label, barcode and packaging data aligned.
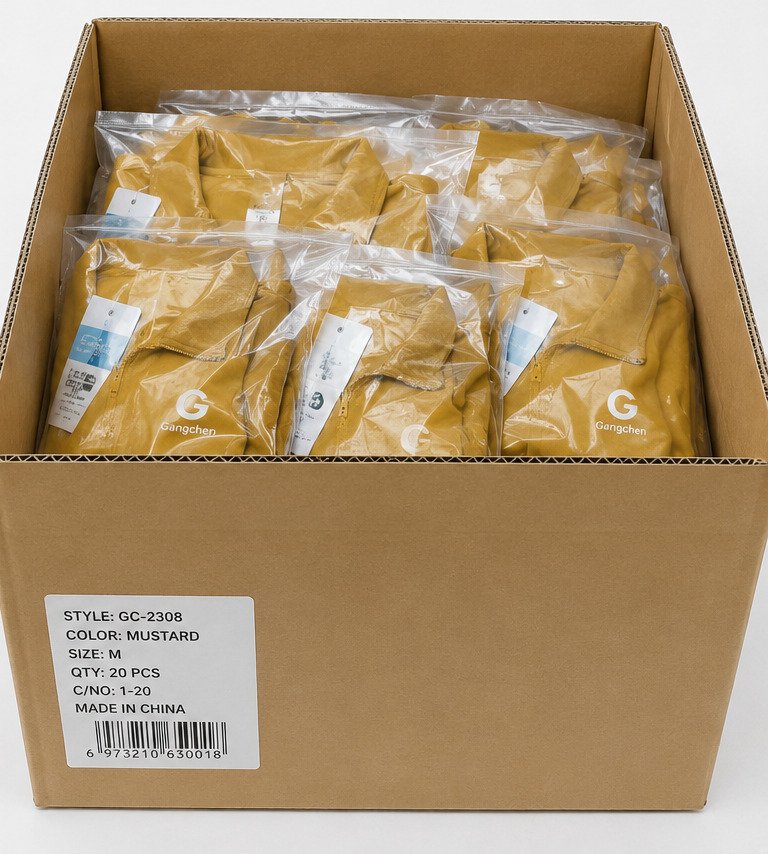
Shipment Release
Maintain relevant product identification through final shipment preparation.
MOVEVOX supports private-label packaging according to the agreed project structure.
Use the Latest Approved Standard as the Starting Point for Reorders
A reorder should not automatically assume that every production condition remains unchanged. Material availability, color, quantity, SKU mix and packaging can alter production requirements even when the core product is familiar.
Previous Approved Standard
Identify the latest approved product and production references.
Change Review
Confirm whether material, color, size, branding, packing or quantity has changed.
Material & Capacity Review
Evaluate input readiness and production allocation for the new PO.
Repeat Production
Apply relevant production and QC controls to the reorder.
Performance Feedback
Use commercial execution information to support the next program.
Next Forecast
Where available, use follow-on requirements to support production planning.