What Racerback Projects Fit MOVEVOX Best?
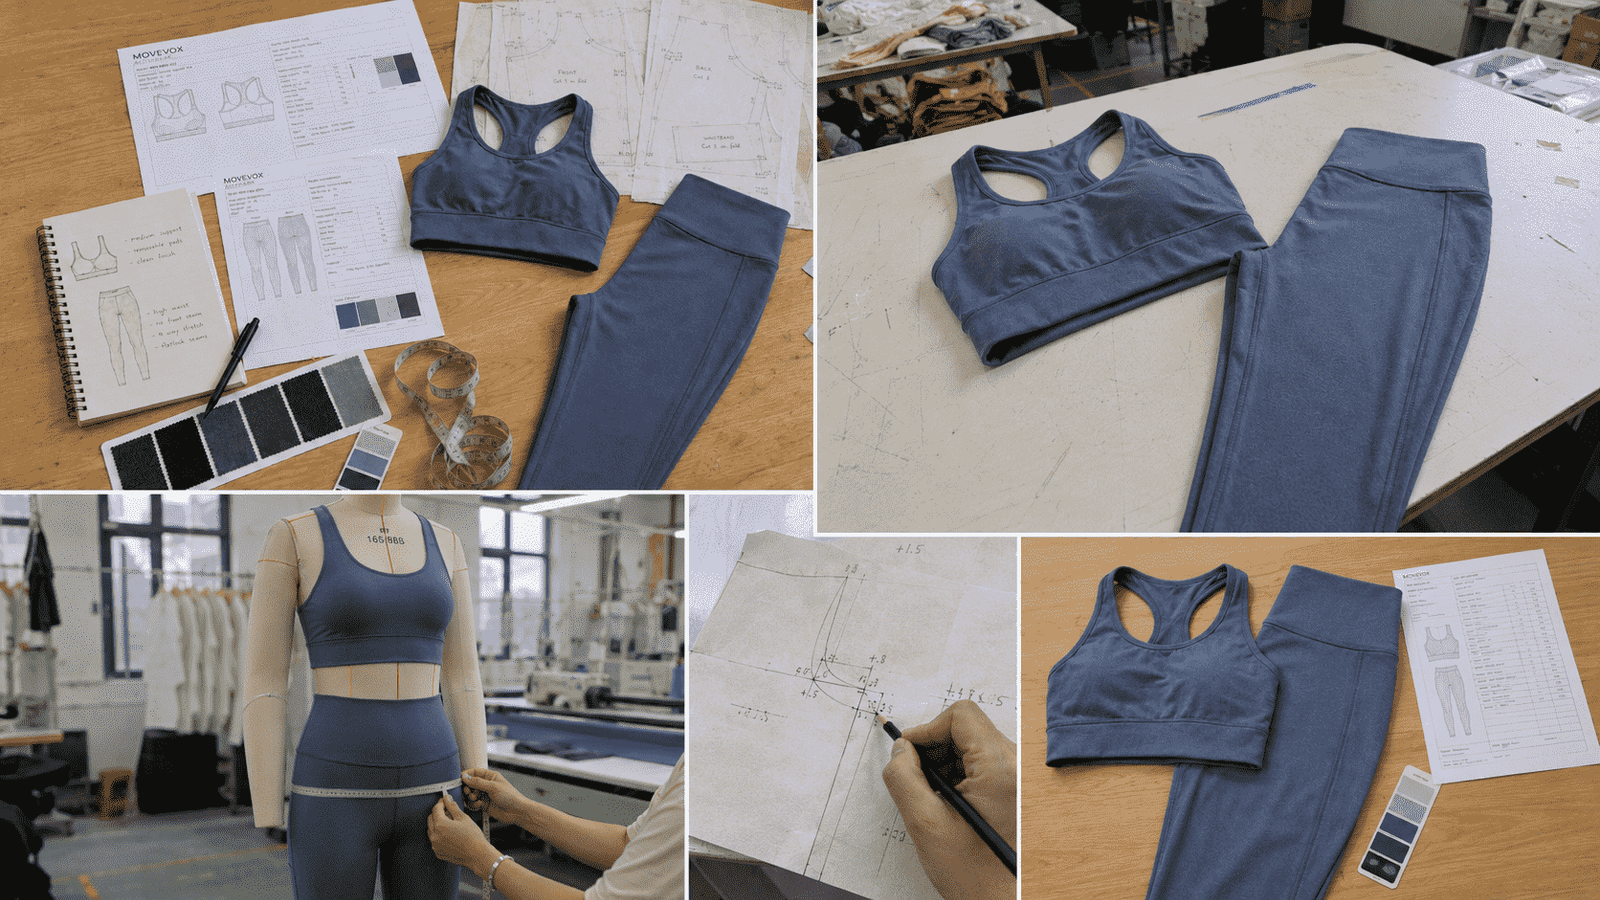
MOVEVOX is most relevant to brands that need a racerback silhouette translated into defined garment measurements, strap and back construction, physical fit approval and repeatable production. Projects may begin from a Tech Pack, legal reference garment, sketch, image or sufficiently defined product concept.

Existing Style Transfer
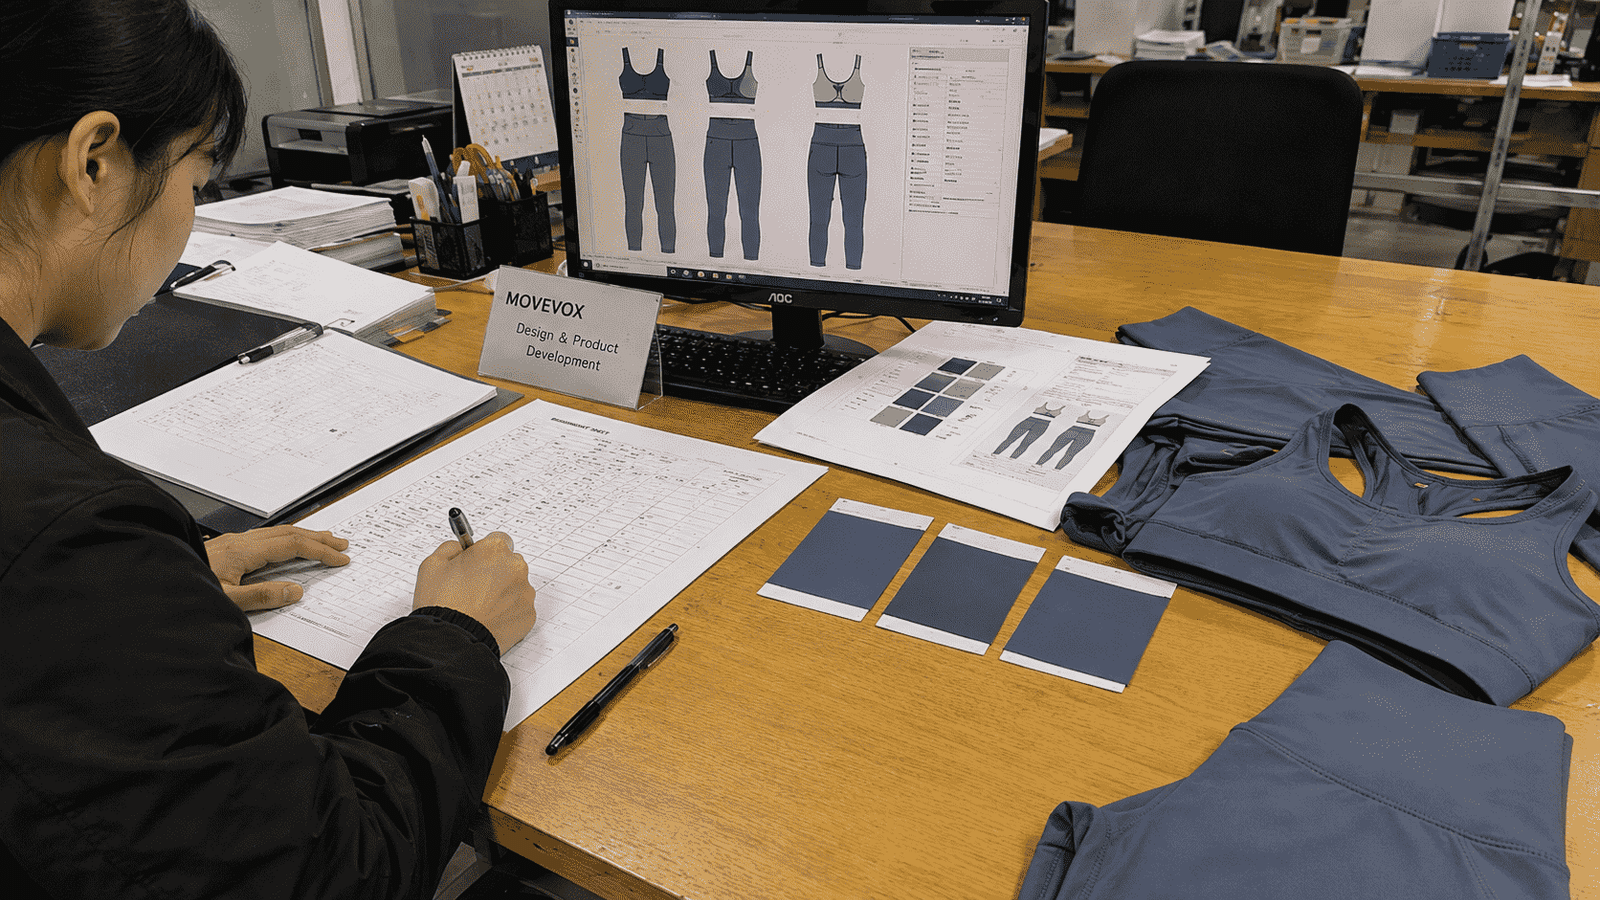
Brands transferring an existing racerback can provide the approved reference, Measurement Chart, construction details and material direction. The objective is to establish an executable MOVEVOX production standard rather than reproduce appearance from photographs alone.
New Core Bra
A new racerback program can begin from the intended activity, support direction, back silhouette, strap concept, material, pad direction and target size range. Unresolved variables remain development points until the buyer approves them.
Seamless Racerback
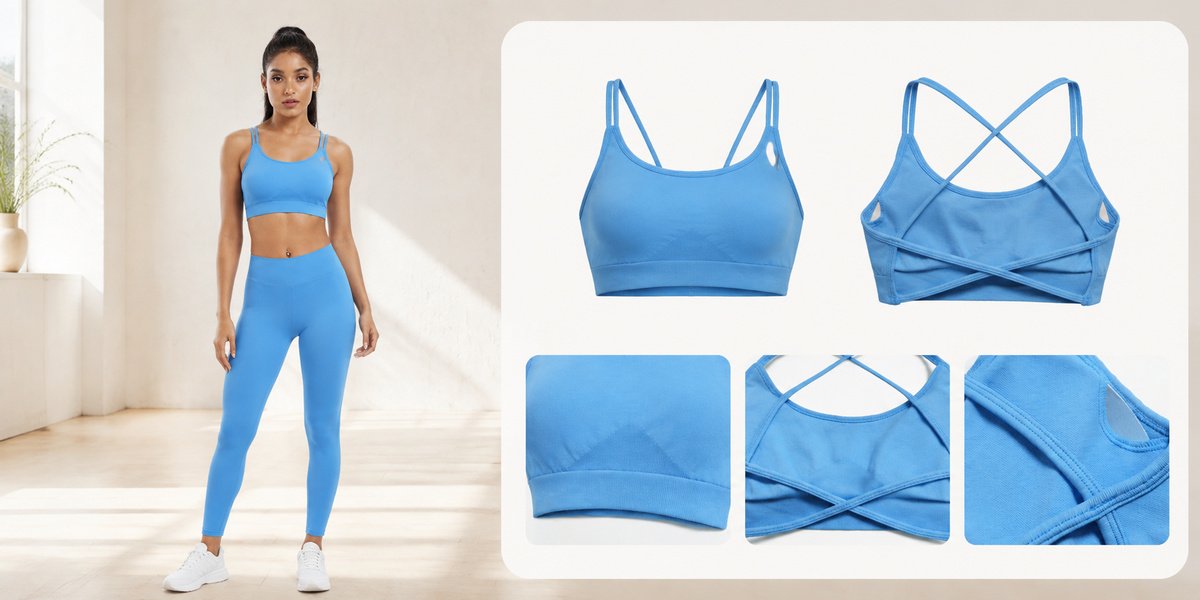
A Seamless project can integrate body structure, rib, density or back shaping through Santoni programming, while still using downstream sewing or finishing where required by the approved product.
Brand Collection
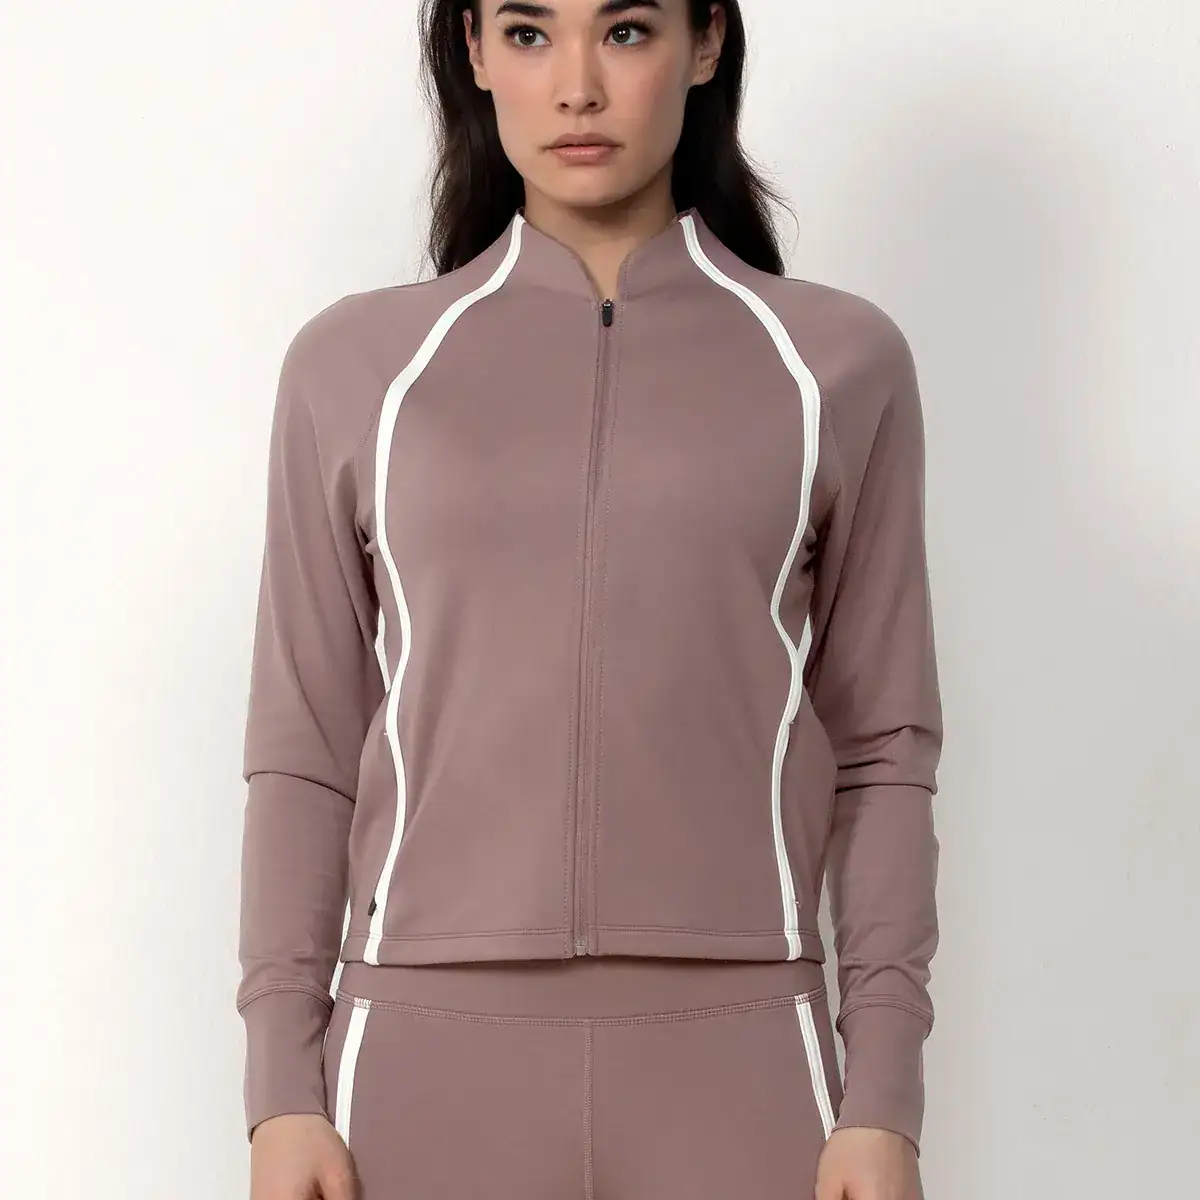
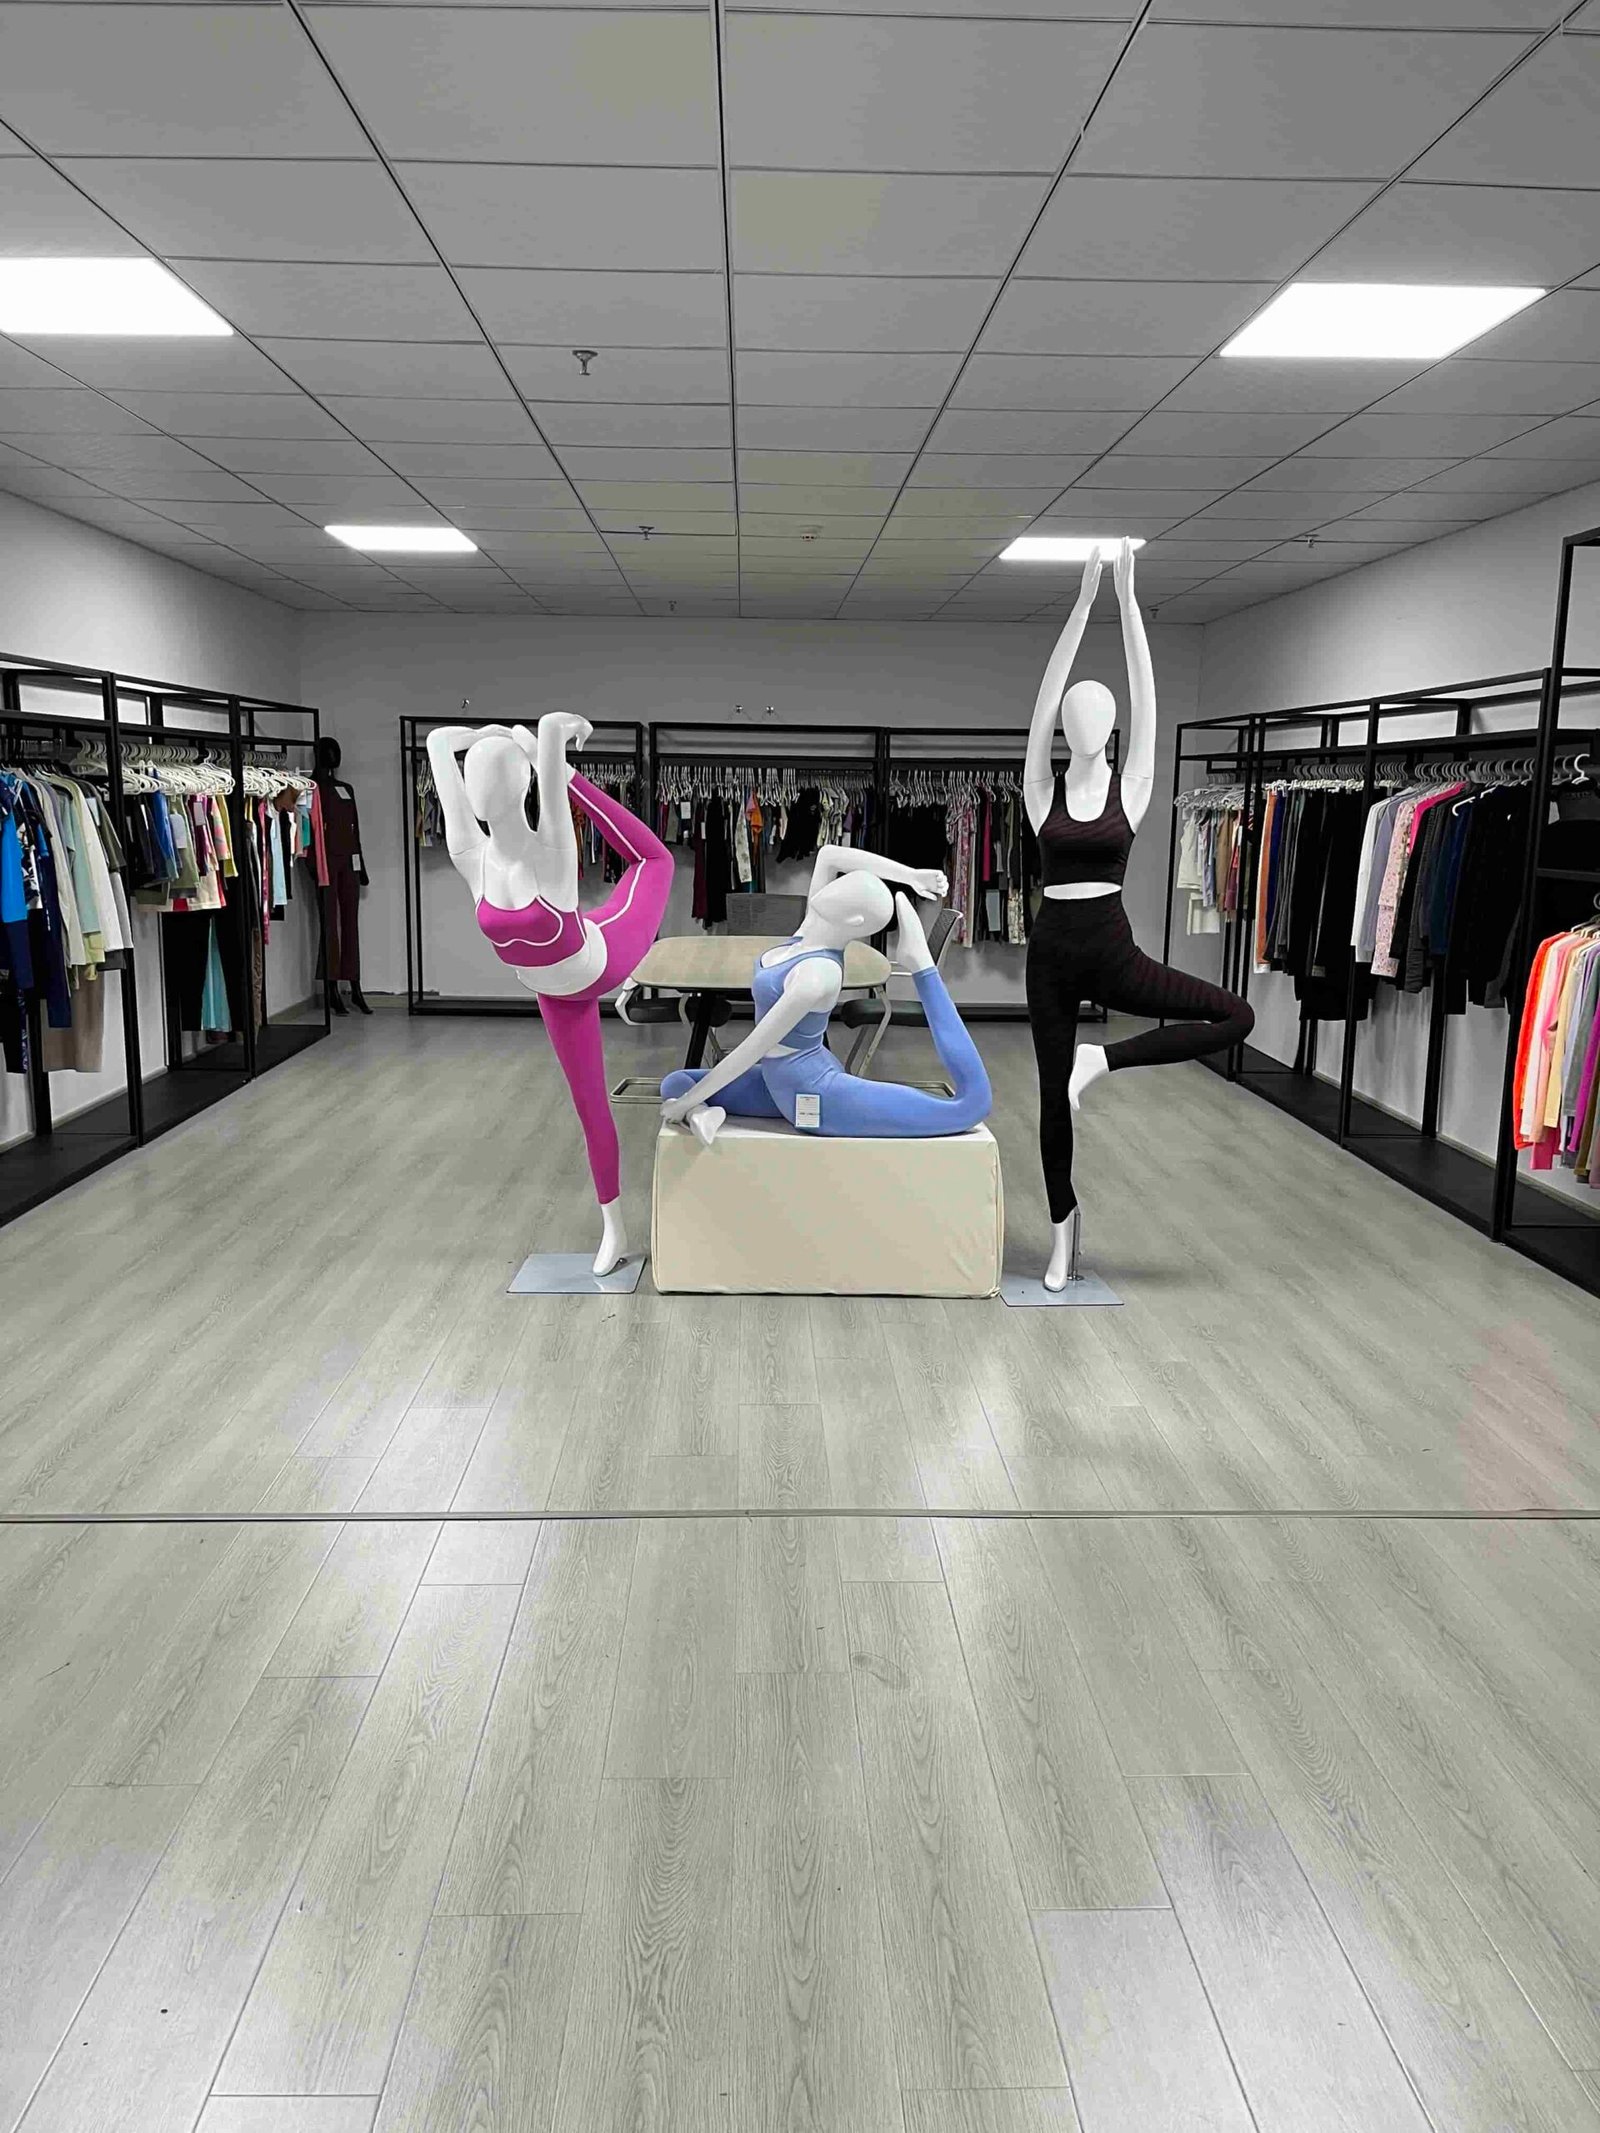
A racerback Sports Bra can be developed as part of a wider activewear range with leggings, shorts, tops, colors, logos, labels and packaging, while each SKU retains its own technical standard.
Manufacturing Facts Behind Racerback Sports Bra Development
These operating references describe the current MOVEVOX manufacturing and development system. Actual timing and capacity still depend on product structure, materials, size range, approvals and production conditions.
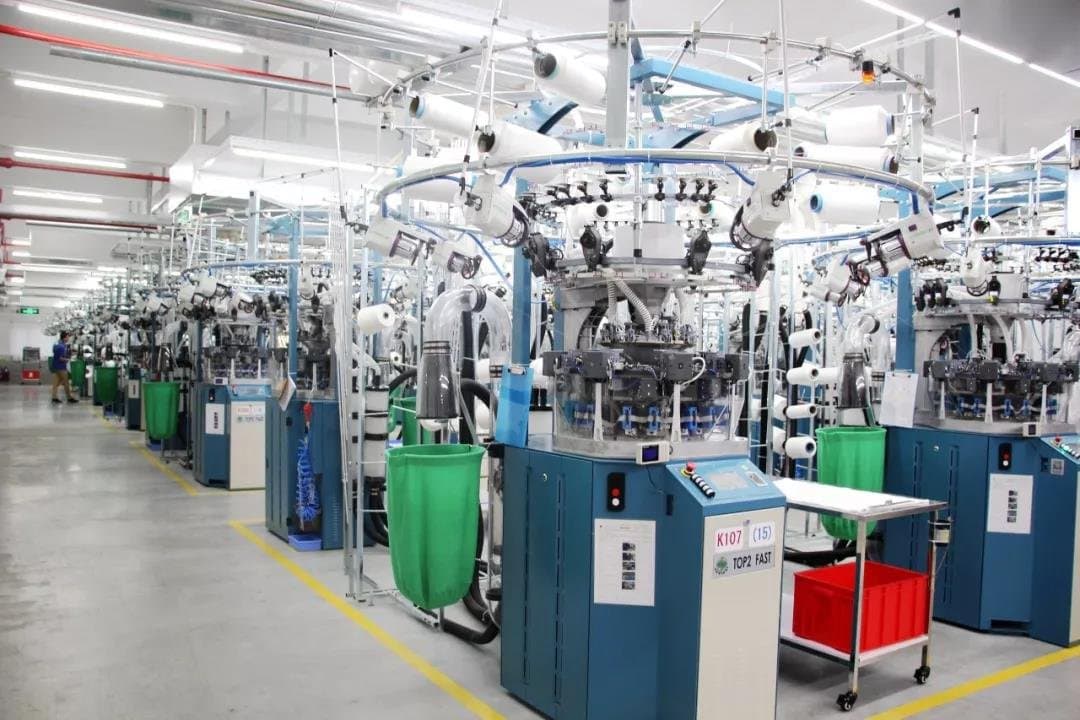
Santoni Machines
Italian Santoni equipment within MOVEVOX's core Seamless manufacturing system supports technically suitable Sports Bra and activewear programs.
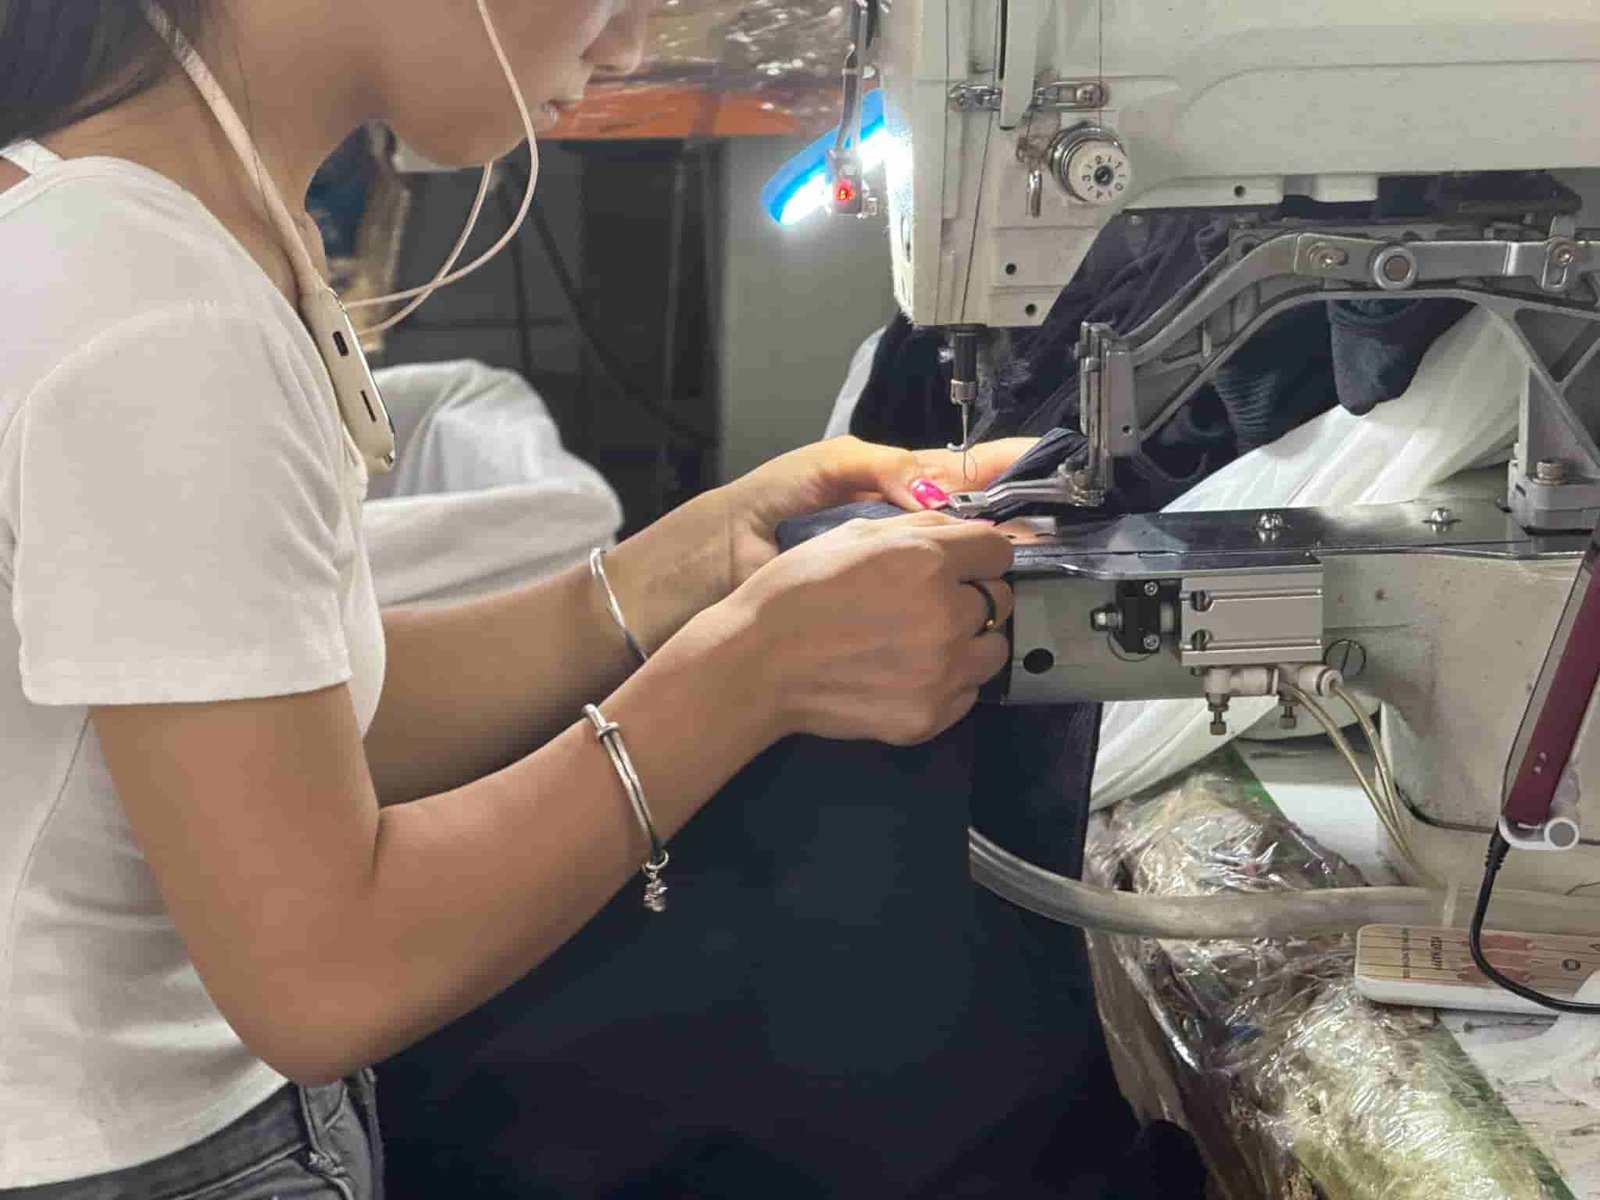
Garment Machines
Approximately 24 principal sewing and garment-production machines support MOVEVOX's current core Cut & Sew manufacturing operations.
Development Personnel
The current development organization includes design, pattern-making, sample-making and related product-development functions.
QC Personnel
Five current QC personnel support applicable incoming, production, finished-garment, packing and shipment-related quality activities.
Standard Sampling
A normal development sample generally requires approximately 5–10 working days after the information needed for execution has been sufficiently confirmed.
Managed Monthly Capacity
Normal comprehensive managed delivery capability is approximately 150,000–200,000 pieces per month across the controlled production system.
Inside a Controlled Racerback Sports Bra
The racerback is a connected geometry system. Each hotspot should be evaluated in relation to garment size, material, intended activity and the complete physical Sports Bra.
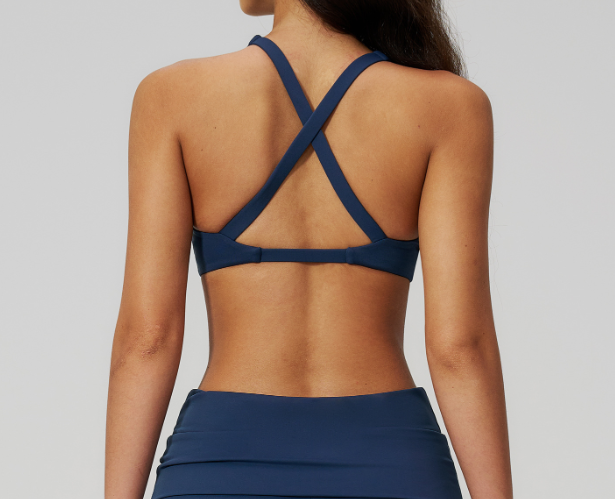
Shoulder Strap
Strap width, effective length and shoulder position influence how the front cup area connects to the center-back structure. Width alone does not determine support or comfort.
Strap Angle
The path from the shoulder toward the center back affects neck proximity, arm movement and the final visual proportion of the racerback.
Back Junction
The convergence point defines where straps or back panels come together. Its position should remain symmetrical and appropriate to the approved garment size.
Back Width
A wider or narrower back changes visual openness and the relationship between shoulder blades, straps and garment stability. The correct width is product-specific.
Armhole
Armhole shape influences shoulder clearance, side coverage and the transition between front and back. Restriction cannot be judged from back appearance alone.
Side Coverage
Side height and side-body geometry connect the front cup area with the racerback and should be reviewed together during Fit.
Underband
The underband establishes an important lower reference for overall garment position. Racerback geometry should not compensate for an incorrect band Fit.
Neckline
Front neckline and back structure work together through the shoulder straps. Changes at either end can alter effective strap length and overall garment position.
Compare Racerback Structures Before Selecting the Construction Route
Different racerback silhouettes create different Fit, grading and manufacturing requirements. The comparison should begin with the buyer's product architecture rather than assuming one back style is universally more supportive.

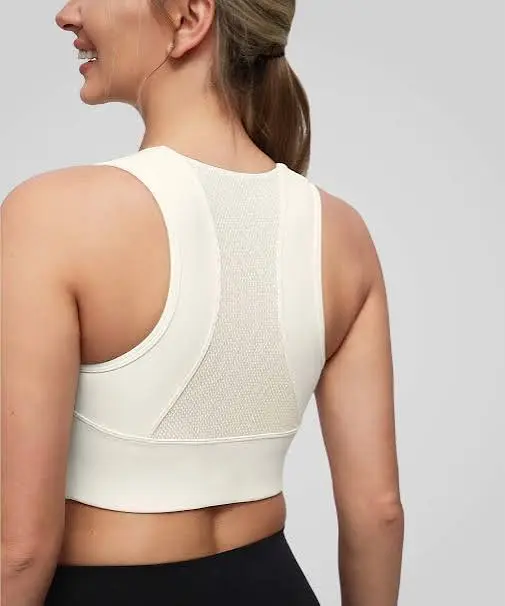


| Racerback Direction | Visual Character | Key Geometry | Main Fit Risk | Manufacturing Direction | Validation Priority |
|---|---|---|---|---|---|
| Classic Racerback | Balanced center-back shape | Moderate strap convergence | Junction shifts by size | Seamless or Cut & Sew | Alignment and shoulder movement |
| Wide Racerback | More back coverage | Wide straps and back body | Excessive neck or shoulder contact | Seamless or Cut & Sew | Strap width and armhole |
| Narrow Y-Back | Open athletic appearance | Narrow convergence zone | Strap concentration near neck | Project-specific | Strap path and Fit |
| High-Neck Racerback | More front coverage | Neckline and racerback linked | Armhole or neckline restriction | Seamless or Cut & Sew | Movement and grading |
| Open Racerback | More exposed back | Reduced back-body area | Stability changes with material | Often Cut & Sew | Material and strap relationship |
| Longline Racerback | Extended torso silhouette | Back plus longer lower body | Band and body-length interaction | Seamless or Cut & Sew | Underband and torso Fit |
Control the Construction Behind Racerback Strap Geometry
Racerback appearance depends on how straps, edges and back panels are physically constructed. MOVEVOX evaluates each area against stretch, Fit, workmanship and the approved manufacturing route.
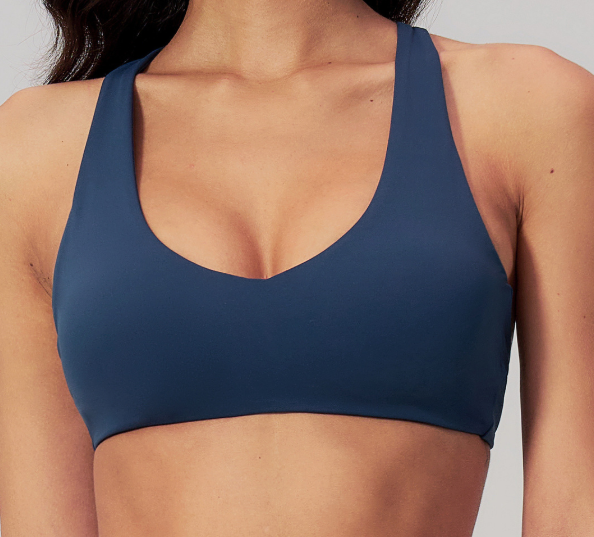
Fixed Shoulder Straps
Fixed straps create a defined path between the front body and racerback. Their effective finished length, width and attachment position need to match the approved Fit rather than being copied from one generic Sports Bra block. Construction should also account for material stretch and the specific edge-finishing method used on the garment.
Evidence Focus
Wide Strap Structure
A wider strap changes the contact area and visual proportion around the shoulder. It can also alter armhole geometry and the way the back converges. MOVEVOX should therefore sample strap width together with neckline, back width and underband instead of describing a wider strap as automatically more supportive.
Evidence Focus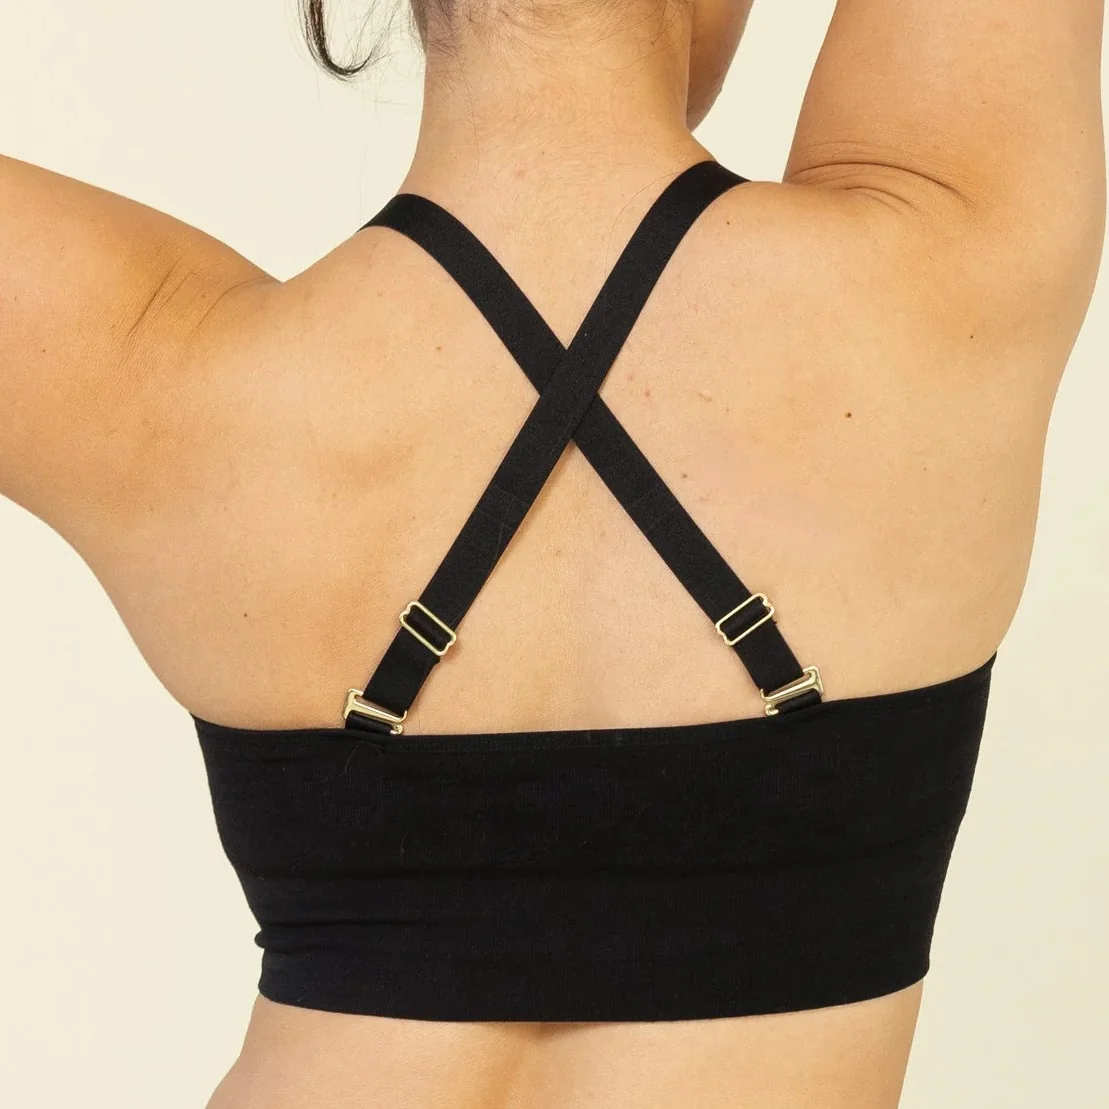
Narrow Back Junction
A narrow racerback junction creates a concentrated center-back visual point. Pattern shape, knitted structure, joining method and left-right alignment all influence the result. The junction must remain centered and visually balanced in the completed garment, including representative sizes where the buyer requires broader grading validation.
Evidence Focus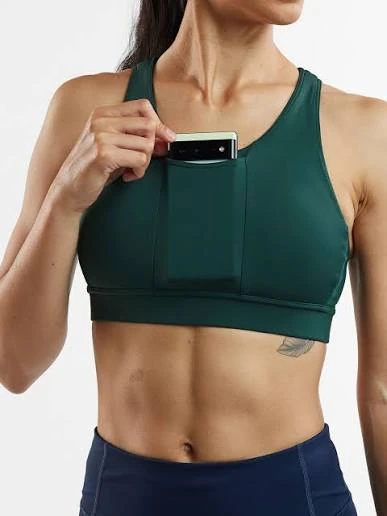
Bound Edge Construction
Binding can finish curved strap, neckline or armhole edges on suitable Cut & Sew designs. The selected binding material, tension and seam method should follow the actual body fabric because excess tension can distort the curve, while insufficient control can create waviness or inconsistent edge recovery.
Evidence Focus
Seamless Back Transition
In a Seamless Sports Bra, back shaping can be integrated through yarn, stitch structure, rib, density or programmed geometry. However, shoulder joining, labels, pad openings or other details may still require downstream sewing. The final finished garment—not only the knitted blank—should therefore become the approval standard.
Evidence Focus
Lined Back Construction
Where a Cut & Sew racerback includes lining or multiple internal layers, those materials can influence stretch, thickness and edge behavior. The lining should be approved in the complete sample because changing the internal layer can alter the Fit even when the outside pattern remains unchanged.
Evidence FocusReview Racerback Geometry During Real Shoulder Movement
A racerback that appears balanced on a flat garment still needs physical movement review. The objective is to identify whether the approved geometry behaves appropriately for the buyer's intended use.
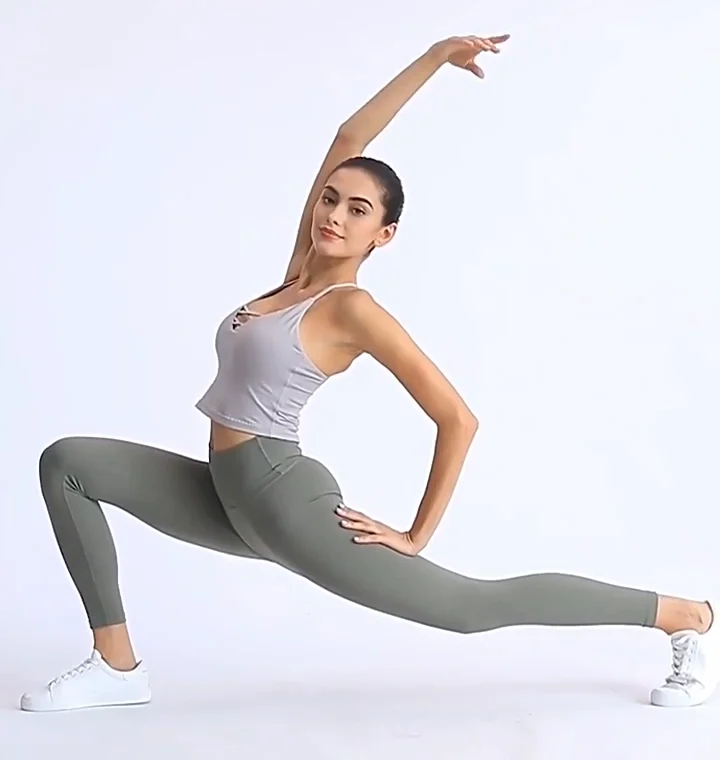
Observe the Racerback Through Relevant Shoulder Movements
Overhead reach: Raising both arms can reveal whether straps move excessively toward the neck, whether the armhole becomes restrictive or whether the underband and body shift upward. The observation should be compared with the original standing Fit rather than judged from movement alone.
Forward reach: Reaching forward changes the relationship among the shoulder blades, straps and center-back junction and can expose excessive strap tension, back-body restriction or asymmetry.
Arm sweep: Moving the arms through a broader range can reveal whether the armhole edge interferes with movement or whether strap placement changes unexpectedly around the shoulder.
Torso rotation: Rotation can help identify whether the back structure remains visually balanced and whether one side moves differently from the other.
The objective is to identify the variable that actually needs correction. “The racerback feels tight” is not an executable factory instruction. The issue may come from strap length, back width, armhole shape, underband, material recovery or another measurement.
MOVEVOX should not describe this movement review as a standardized laboratory test or as proof of universal shoulder comfort.
Translate Movement Feedback Into Measurable Product Revisions
Useful movement feedback needs to become technical information before the next sample is made. If a strap feels too close to the neck, the team should determine whether the relevant variable is shoulder position, strap angle, effective strap length, back-junction position or the entire upper-body pattern.
If the armhole feels restrictive, the review should distinguish between armhole shape, side height, material stretch, binding tension and overall garment size. A wider armhole is not automatically the correct answer because increasing one curve can change coverage and strap relationship elsewhere.
If the racerback rises during overhead movement, the team should also examine underband measurement, body length, material recovery and total Fit rather than adjusting only the back.
The revised physical sample should be evaluated under the same relevant condition used to identify the issue. Buyer comments should then be consolidated into the current technical version before further development.
Reduce Pressure Risks Around Racerback Contact Areas
Racerback straps bring garment structure toward the upper back and shoulders. Comfort therefore depends on several physical contact points, not on the word “racerback” itself.
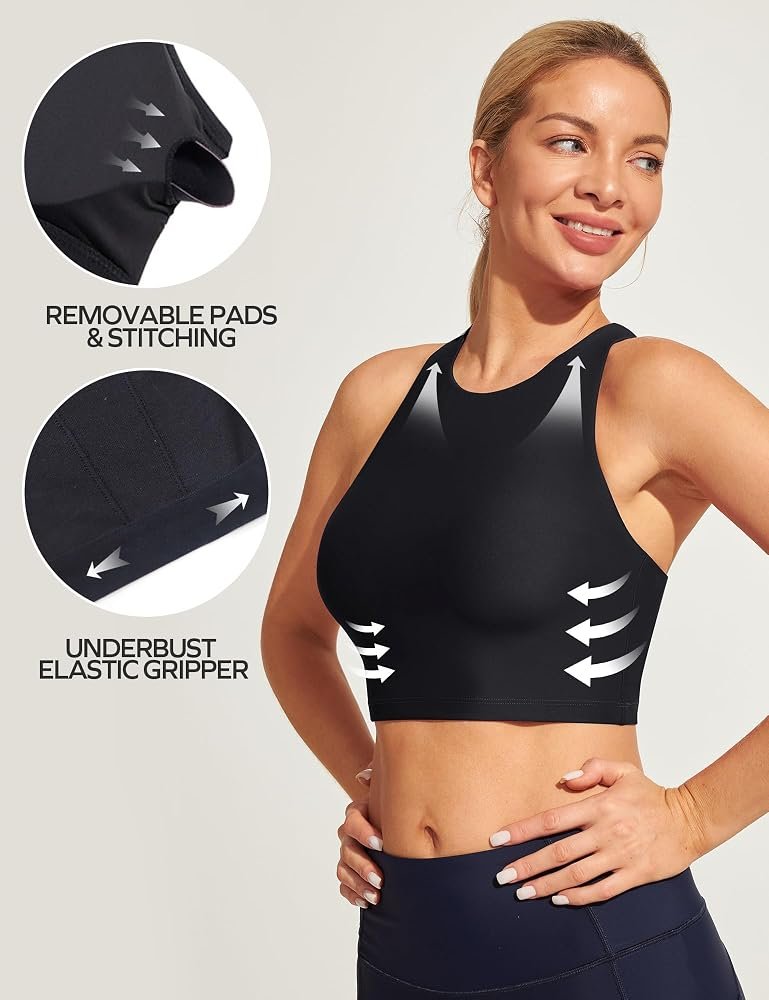
Neck Proximity
A strap path that moves too close to the neck can create unwanted pressure or distraction for some Fit targets. The correct position depends on shoulder width, neckline, back convergence, strap dimensions and complete garment Fit rather than one fixed universal distance.
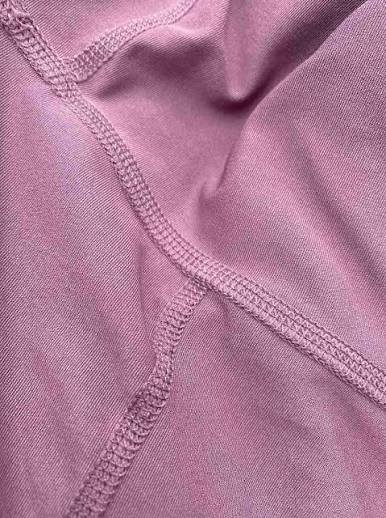
Strap Edge
Strap edge construction can influence how the garment feels against the shoulder. Binding, seam allowance, knitted edges and finishing should suit the selected material so the approved product does not gain unnecessary local thickness or uncontrolled edge tension.
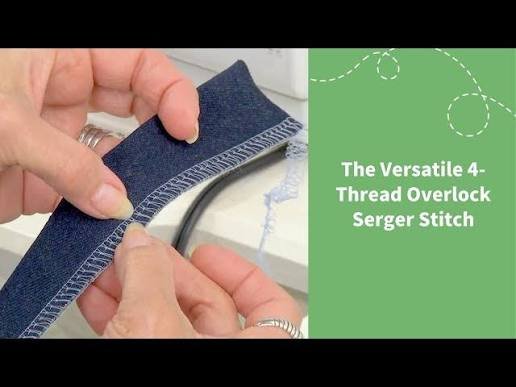
Shoulder Join
A shoulder seam or joining point can create additional bulk at a high-contact area. MOVEVOX should select and approve the construction against the actual fabric and design, then inspect whether both sides remain consistent during production.
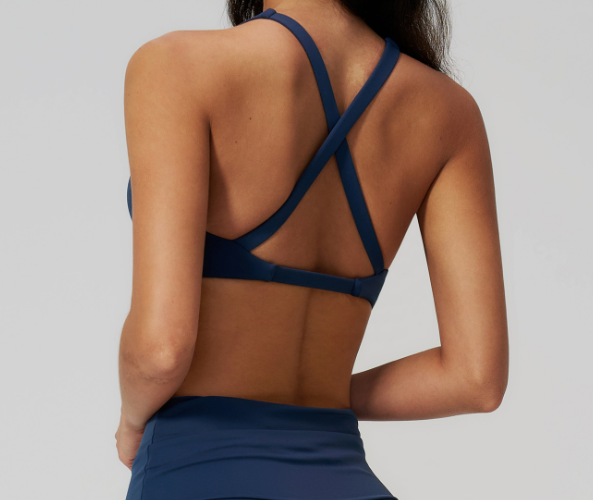
Armhole Edge
Armhole geometry sits directly beside shoulder movement. A smooth visual curve can still feel restrictive if the measurement or edge tension is incorrect. Fit Sample review should therefore consider both static appearance and buyer-defined movement.
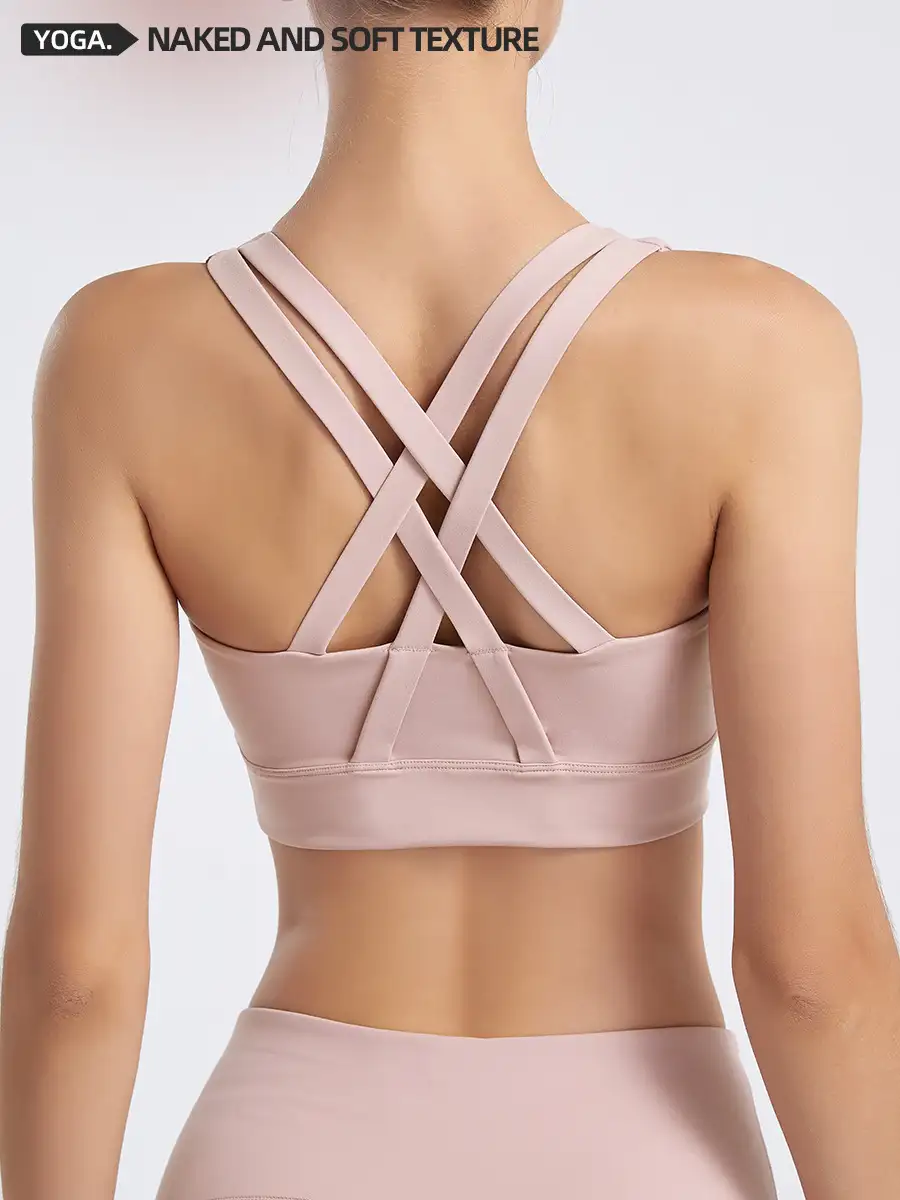
Back Junction
The racerback convergence area can combine straps, seams, lining or multiple fabric layers. Excess bulk, twisting or poor alignment should be corrected before bulk rather than hidden behind a statement that racerback construction is inherently comfortable.
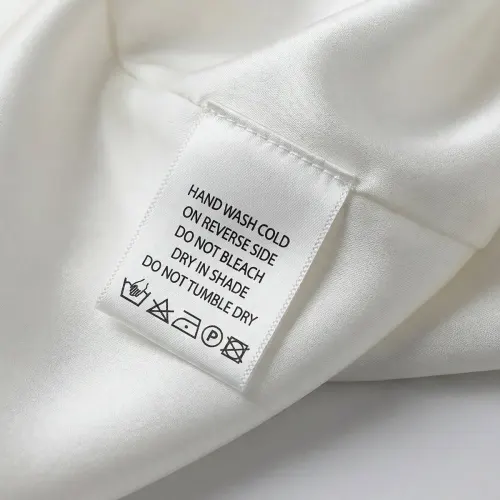
Internal Label
Care or brand labels positioned near the upper back can introduce a separate contact point unrelated to racerback geometry itself. Location and attachment should follow the buyer-approved sample and relevant labeling requirements.
Connect Racerback Geometry With the Underband Construction
The racerback sits above a lower garment reference. Underband structure, measurement and recovery therefore affect overall Sports Bra position and cannot be separated from back Fit.
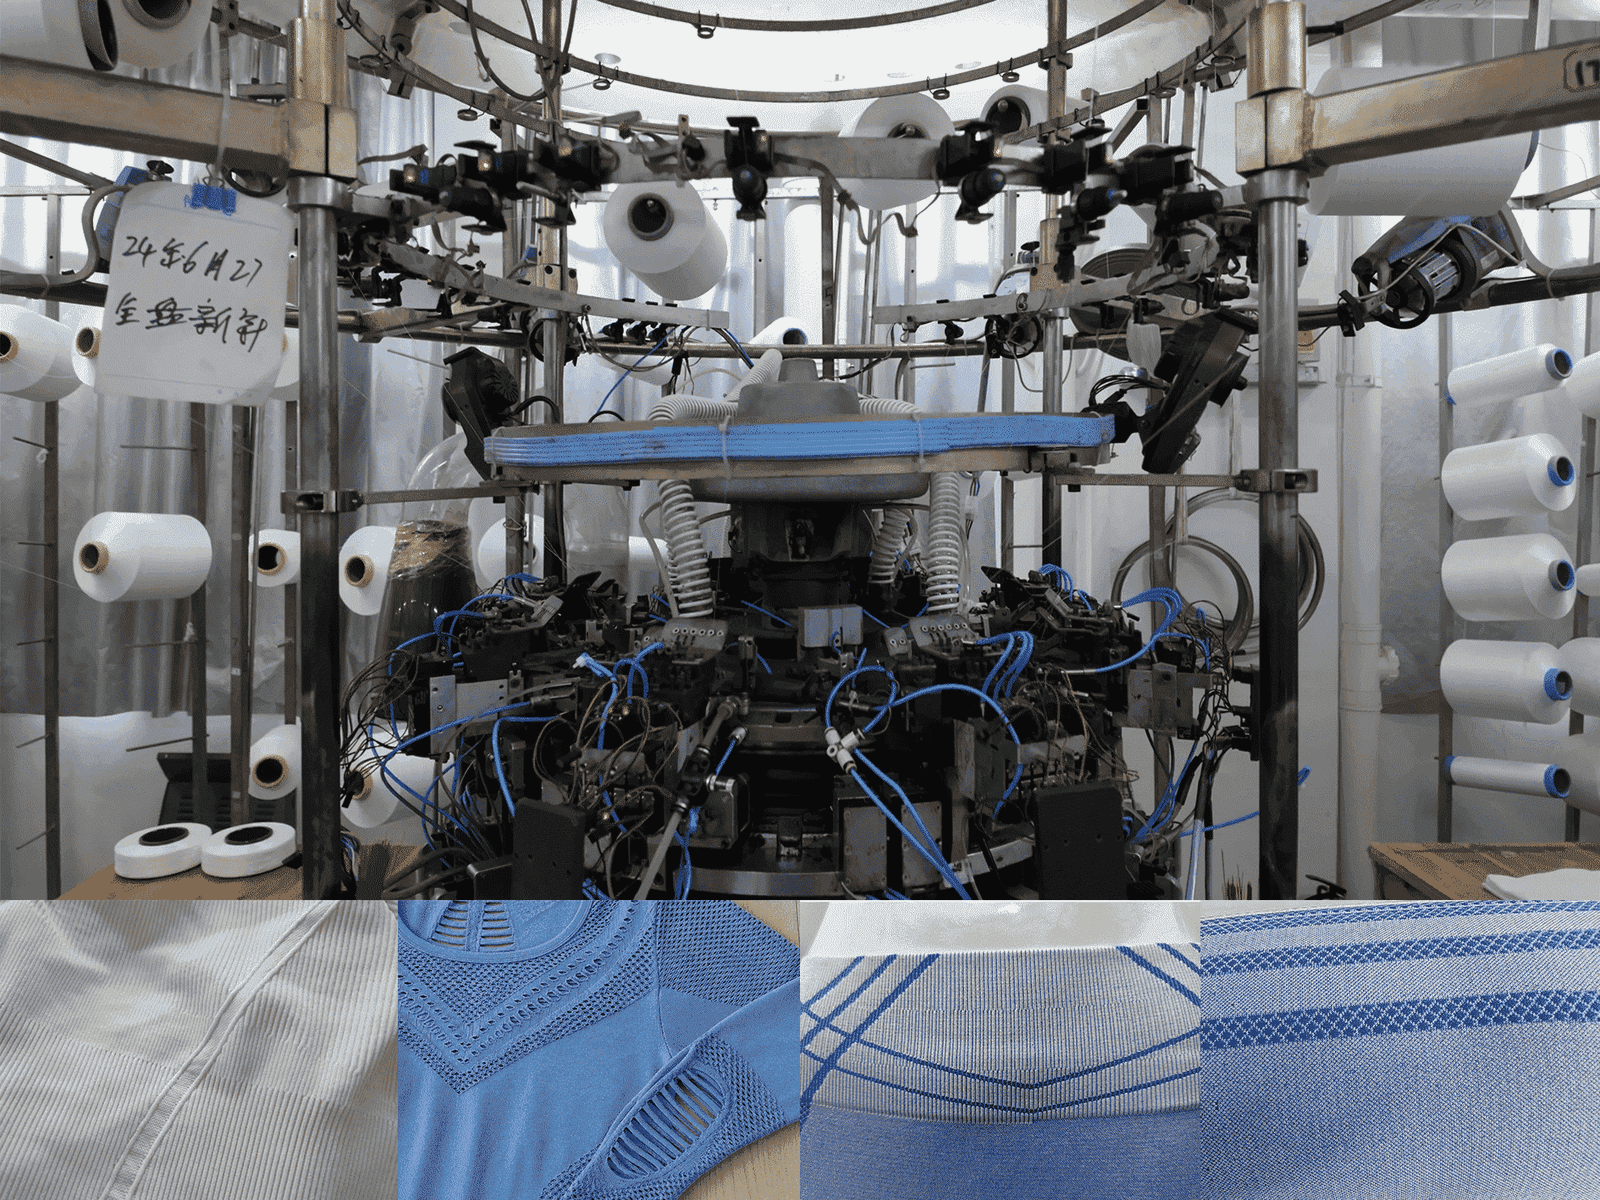
Knitted Underband
A Seamless underband can integrate rib, density or other programmed structure into the garment body. The finished measurement and actual Fit still need approval because knitted appearance alone does not establish a universal support level.
Applicable area: Seamless lower Sports Bra body and racerback transition.
Control value: Maintains an integrated lower reference when correctly programmed and fitted.
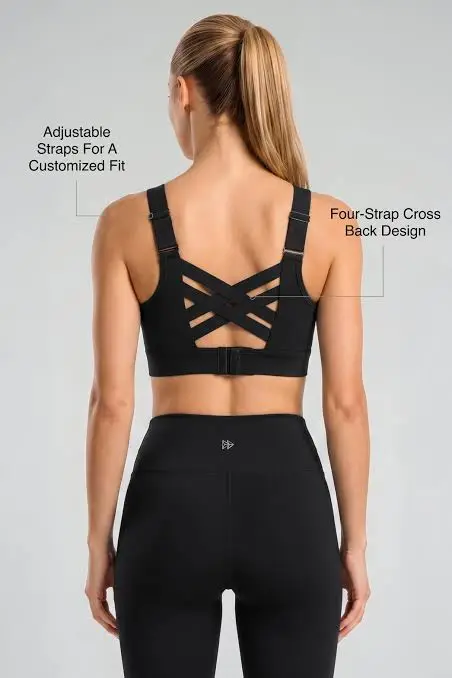
Elastic Underband
Cut & Sew Sports Bras can use dedicated elastic within or along the lower garment construction. Elastic width, stretch direction, joining and finished measurement should follow the approved product rather than a generic factory standard.
Applicable area: Cut & Sew lower band and side-back construction.
Control value: Provides a definable lower structural element within the complete Fit system.

Enclosed Elastic
Elastic can be enclosed within fabric where the design requires a covered appearance. Fabric stretch, seam construction and elastic length must work together, since an incorrect ratio can create gathering, twisting or excessive local tension.
Applicable area: Covered underbands and soft-surface sports bra designs.
Control value: Combines a covered appearance with controlled internal elastic construction.
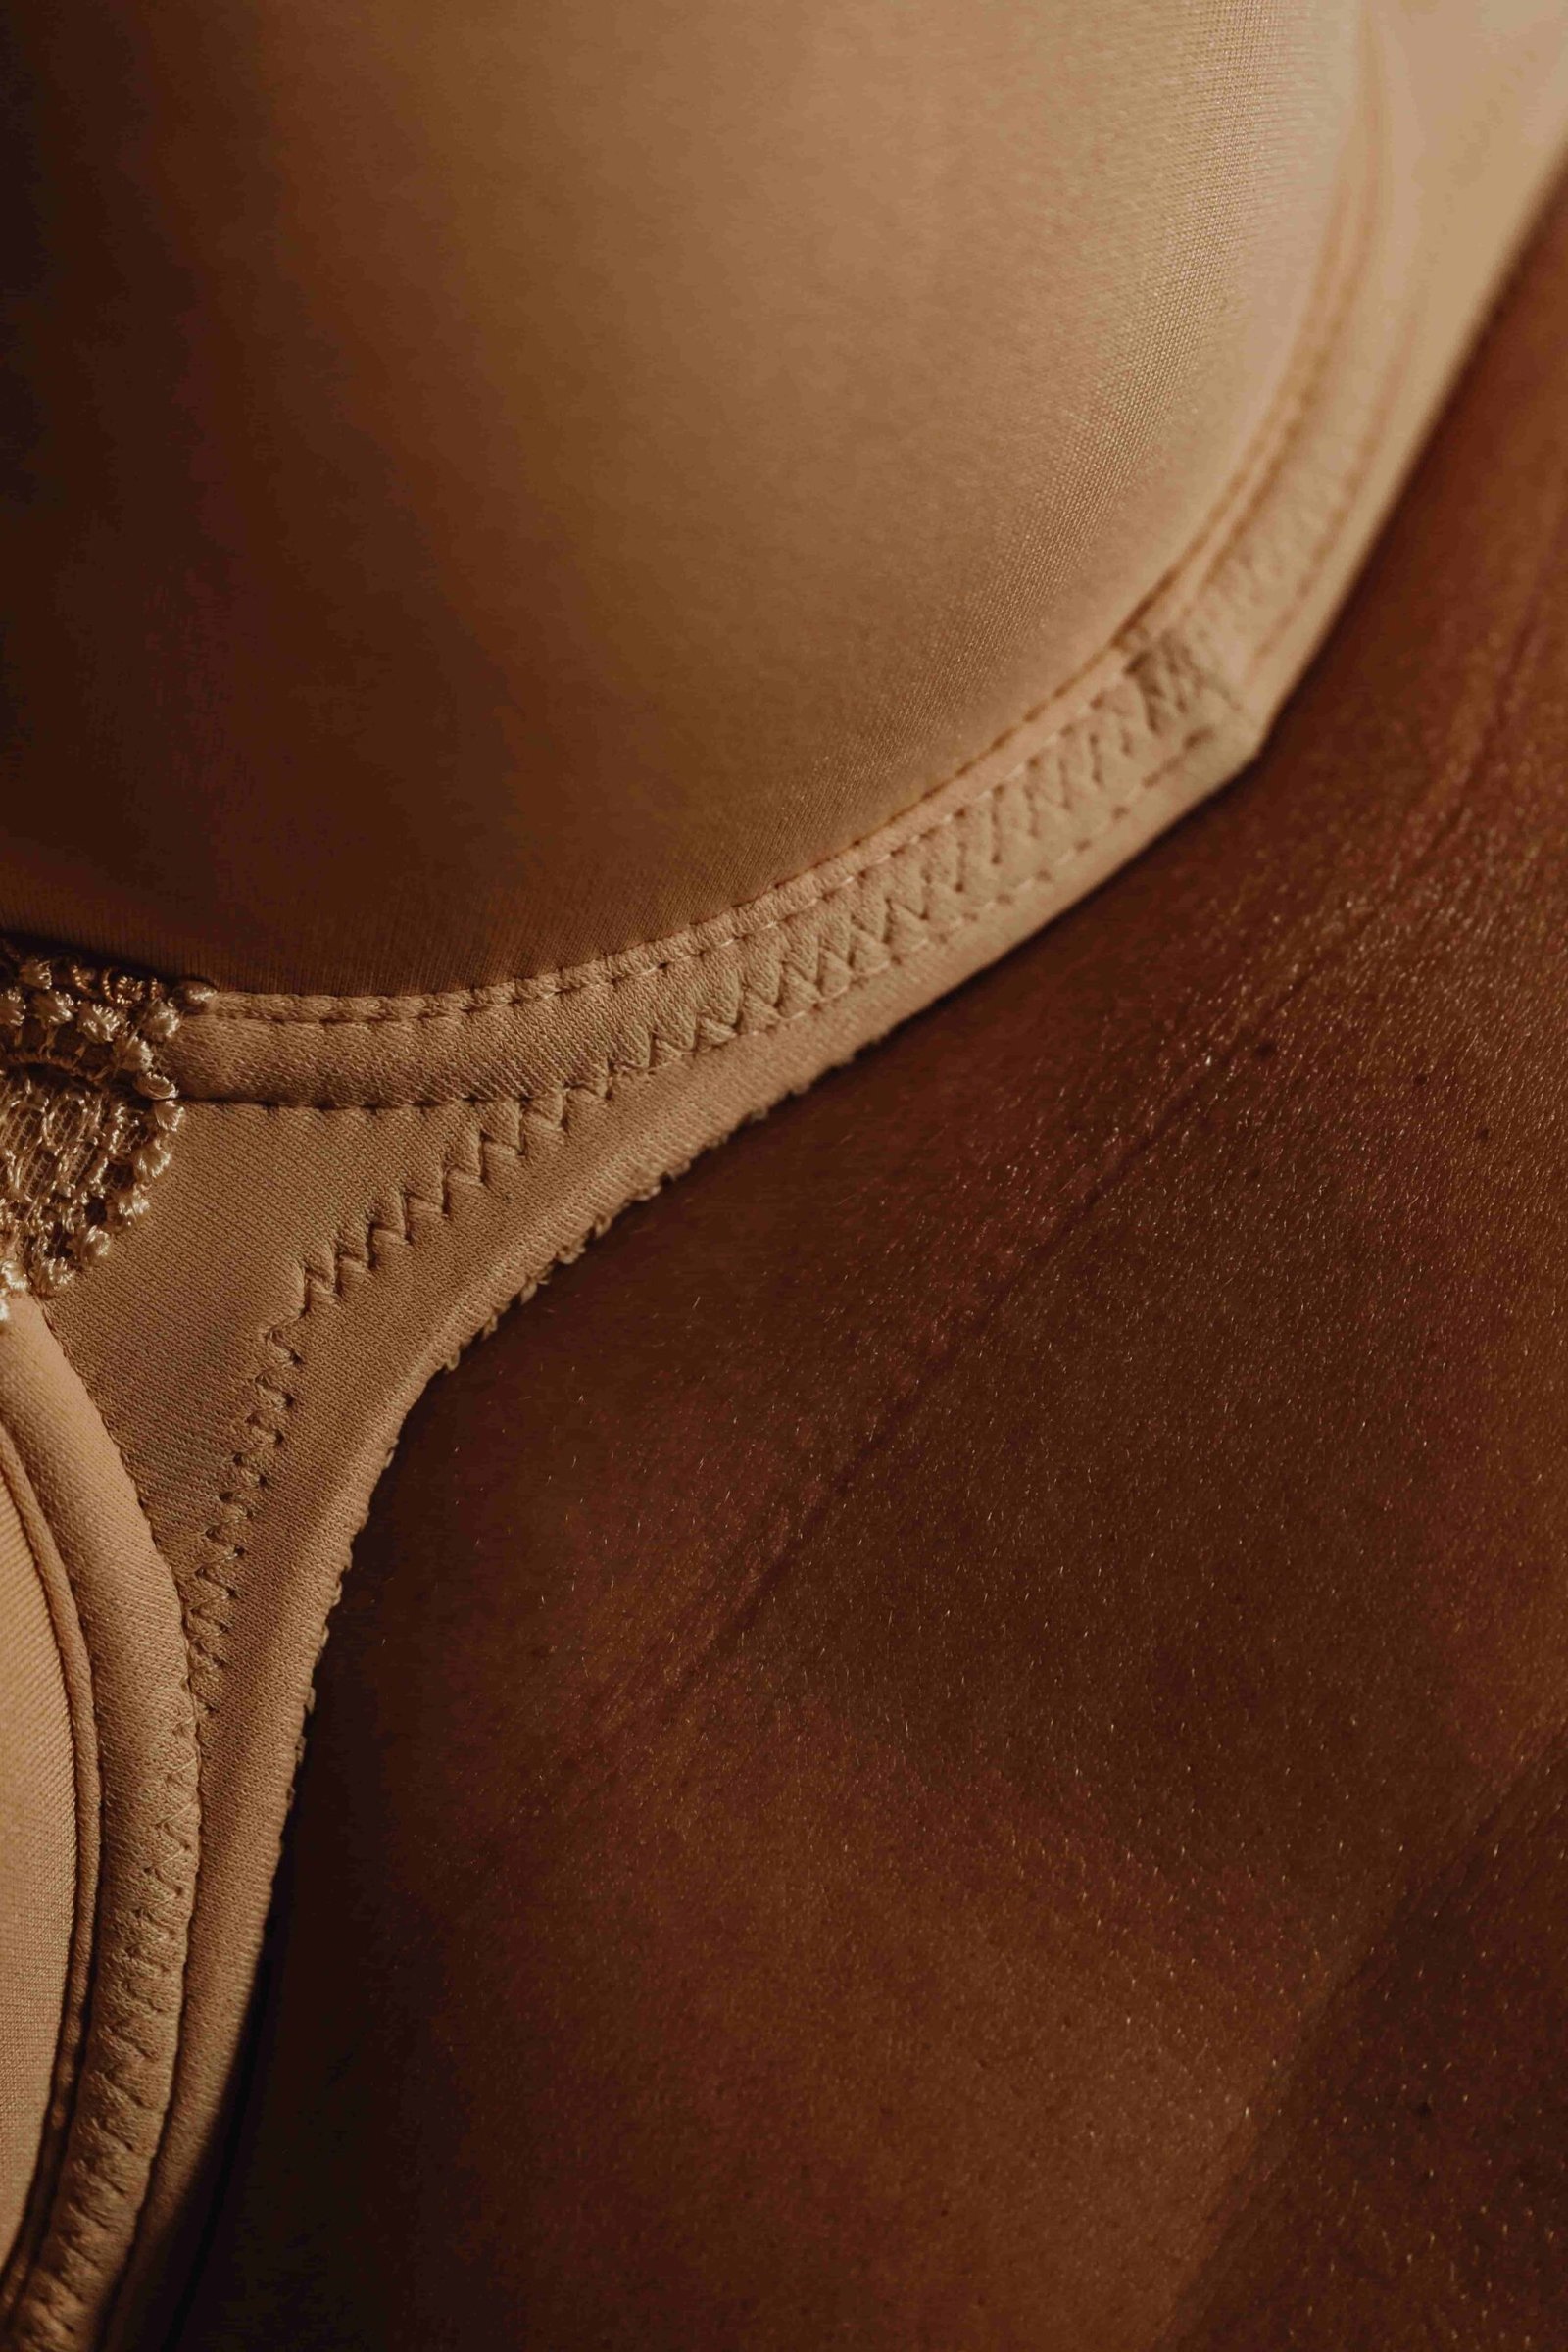
Band Join
The underband join should remain flat, aligned and consistent. The location and seam method can affect local thickness and visual symmetry, especially where it sits near the center back or racerback transition.
Applicable area: Elastic or fabric band joining point.
Control value: Reduces avoidable local bulk when the approved method is maintained.
Back Transition
The point where the back body enters the lower band affects visual alignment. A centered racerback above a twisted or asymmetric lower band does not create an acceptable finished product.
Applicable area: Center-back and lower racerback relationship.
Control value: Keeps upper geometry connected to the approved lower garment reference.
Stretch Seam
Seams around the underband need to accommodate the actual material and garment stretch. Stitch type, tension and construction should be sampled before production because a seam that does not extend appropriately can alter Fit or fail under use.
Applicable area: High-stretch lower-body seams and elastic transitions.
Control value: Supports the required extension without treating one stitch as universally correct.
Measure Racerback Fit as a Complete Bra System
MOVEVOX follows project-specific Measurement Charts rather than one universal public Sports Bra size chart. Racerback dimensions should remain connected to the front body, underband, armhole and overall Fit.
| POM | XS | S | M | L | XL |
|---|---|---|---|---|---|
| Finished Underband | Project-specific | Project-specific | Project-specific | Project-specific | Project-specific |
| Front Body Length | Project-specific | Project-specific | Project-specific | Project-specific | Project-specific |
| Back Body Length | Project-specific | Project-specific | Project-specific | Project-specific | Project-specific |
| Strap Length | Project-specific | Project-specific | Project-specific | Project-specific | Project-specific |
| Strap Width | Project-specific | Project-specific | Project-specific | Project-specific | Project-specific |
| Racerback Width | Project-specific | Project-specific | Project-specific | Project-specific | Project-specific |
| Back Junction | Project-specific | Project-specific | Project-specific | Project-specific | Project-specific |
| Armhole | Project-specific | Project-specific | Project-specific | Project-specific | Project-specific |
| Side Height | Project-specific | Project-specific | Project-specific | Project-specific | Project-specific |
| Neckline Reference | Project-specific | Project-specific | Project-specific | Project-specific | Project-specific |
Fit, Grading and Tolerance
Buyer measurement charts and grade rules should define the production standard. Strap length, racerback width, armhole, neckline and underband may require different grading logic rather than one proportional scale factor. Physical Fit Samples and Size Set or representative sizes can then confirm whether the geometry remains appropriate before bulk.
- Do not apply one universal Racerback measurement chart.
- Do not assume all POMs grade by the same increment.
- Do not release bulk from base-size appearance alone.
Control Racerback Geometry Across the Size Range
A base-size approval does not automatically prove the full commercial range. The following risks should be checked against buyer-defined grading and representative physical samples where required.
| Problem | Business Impact | MOVEVOX Control |
|---|---|---|
| Straps Grade Too Long | Larger sizes can develop excess strap length, changing garment position and moving the racerback lower than the intended visual and Fit reference. | Apply buyer-defined strap grade logic and review representative sizes rather than scaling strap length from one universal percentage. |
| Junction Moves Upward | The racerback convergence point may sit too close to the neck or shoulders in certain sizes, changing both visual proportion and wearing relationship. | Connect the junction reference to back-body and strap measurements, then confirm the physical Size Set where required. |
| Junction Moves Downward | A low convergence point can open the upper back more than intended and change the effective strap path across the shoulder. | Review back length, strap length and convergence position together instead of correcting only one isolated dimension. |
| Armhole Drifts | Armholes can become too deep, too shallow or differently shaped as the body and straps grade, affecting movement and side coverage. | Include armhole and side-height relationships in technical grading and representative Fit review. |
| Back Width Distorts | The back can become disproportionately wide or narrow, changing visual identity and the location of the straps relative to the shoulder blades. | Define back width by product and size rather than relying solely on overall garment-width growth. |
| Underband Relationship Changes | A correctly graded back can still appear wrong if underband growth changes total garment position differently from the upper-body geometry. | Review band, body and racerback as one Fit system before the range is approved. |
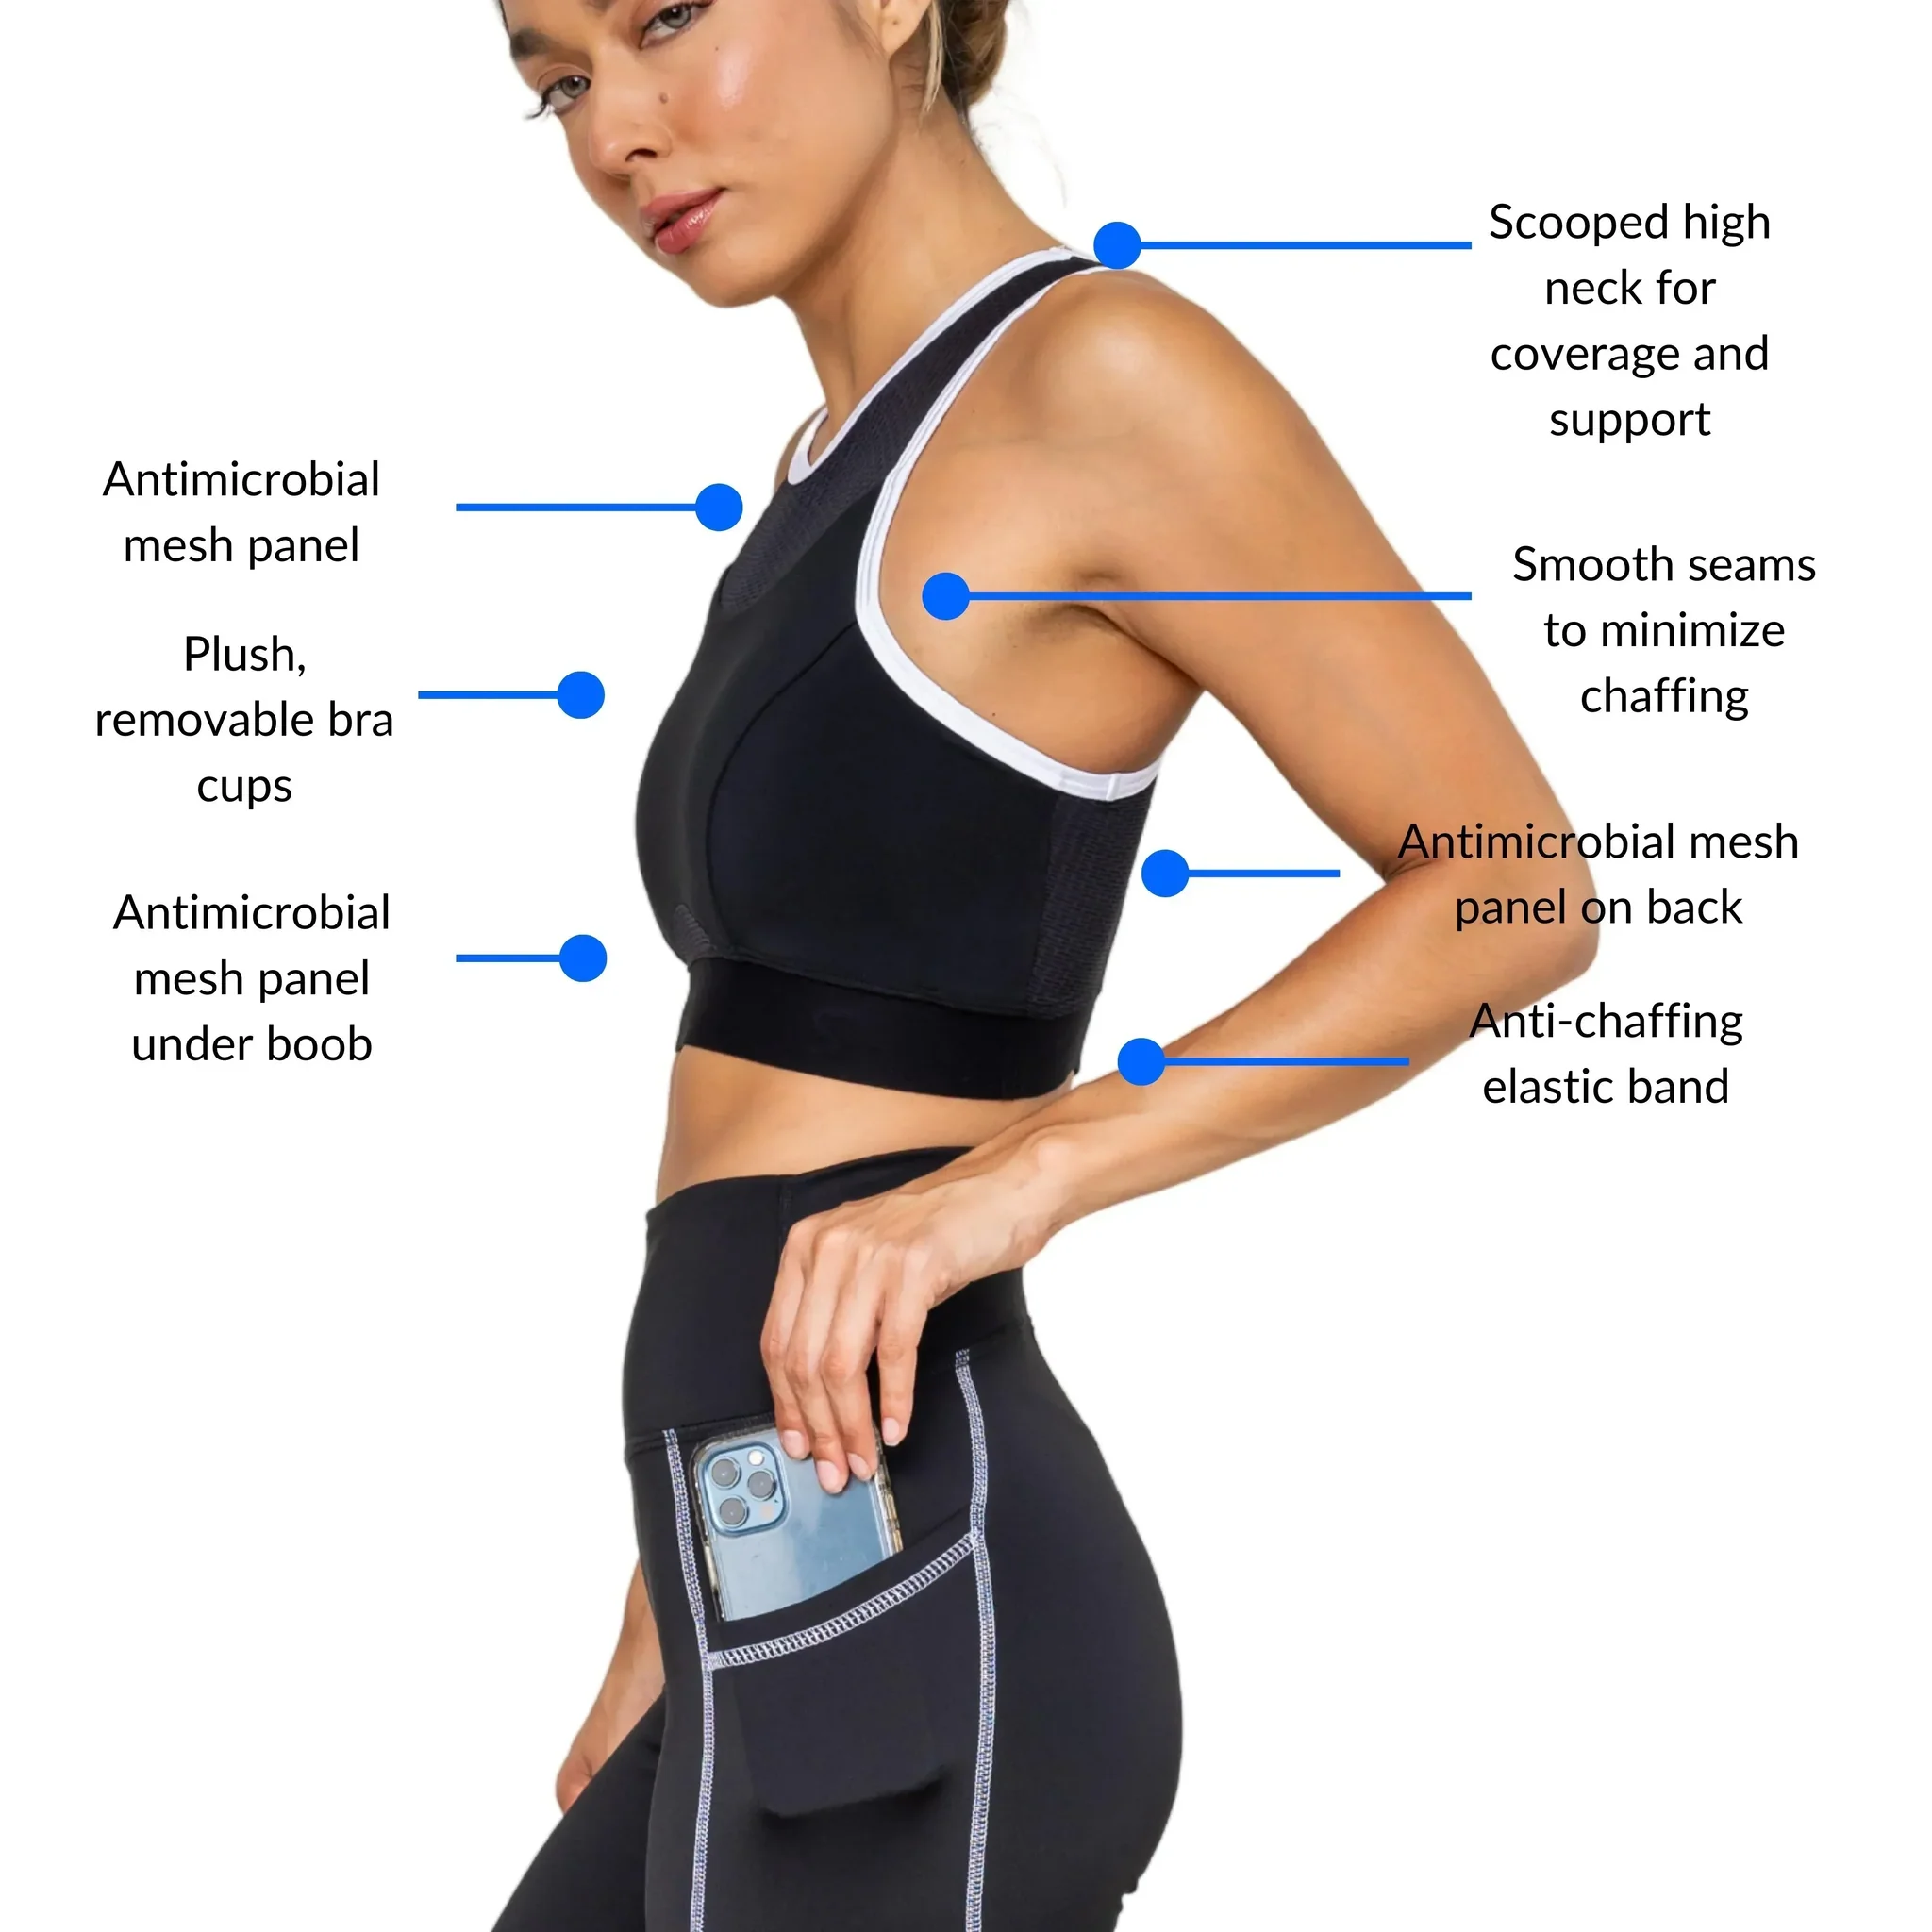
Change Racerback Priorities by Intended Activity
The same racerback silhouette should not be evaluated identically for every use. Activity changes the relative importance of movement, coverage, garment stability and support architecture.
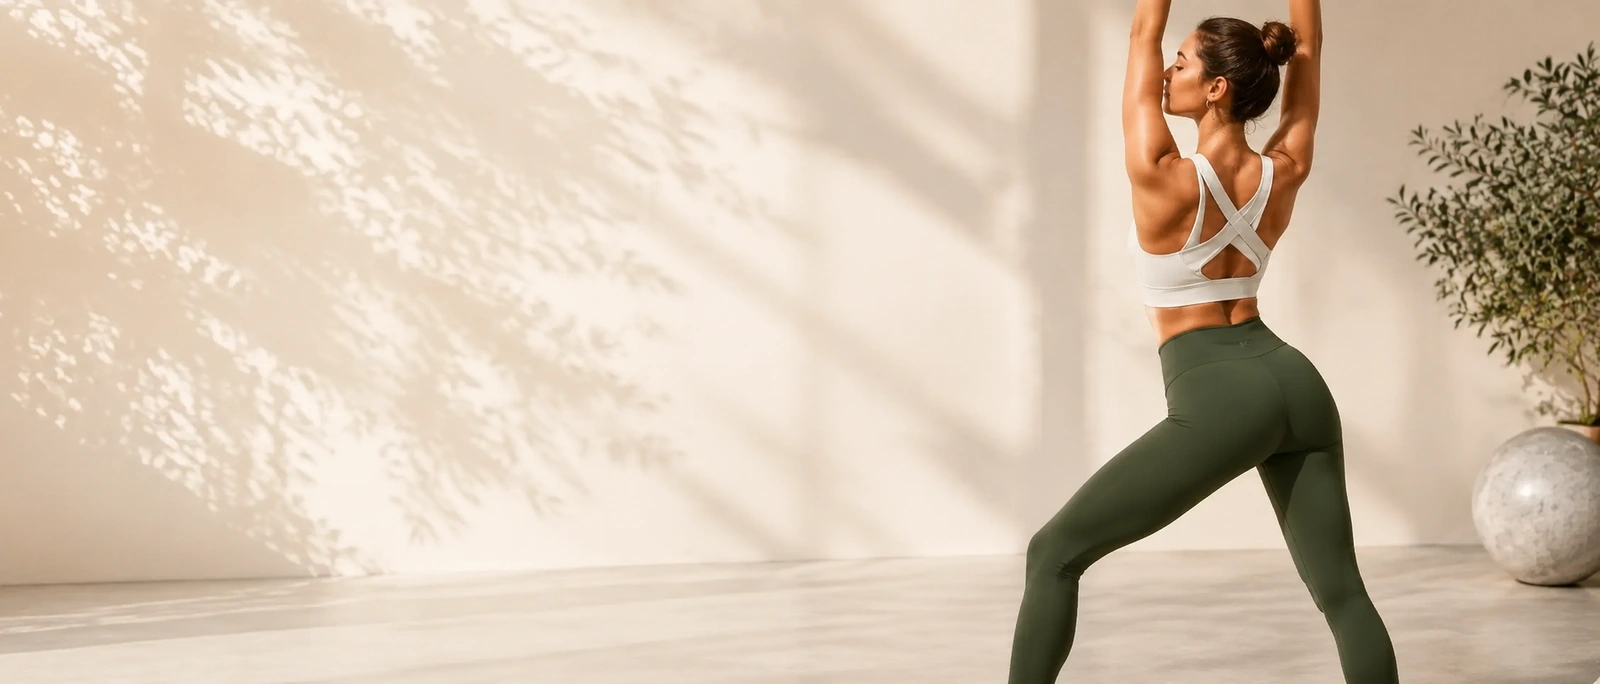
Yoga
A Yoga racerback generally requires the buyer to review shoulder freedom through reaching, twisting and floor-based positions while maintaining the approved neckline, coverage and garment position. A softer handfeel may be part of the brief, but softness alone does not prove Fit stability. Strap geometry, armhole, underband, material stretch and recovery should therefore be reviewed together on the physical product.
- Unrestricted reaching within intended movement range
- Stable neckline and side coverage during position changes
- Soft material combined with approved garment recovery
- Back geometry remains visually balanced
Pilates
Pilates or Studio use can place repeated emphasis on controlled arm positions, torso rotation and close-to-body movement. The racerback should be assessed for strap path, shoulder-blade clearance, neckline position and unwanted local pressure. MOVEVOX should not assume a Studio product must be low support; the support target still follows the buyer's product specification.
- Shoulder and upper-back movement during controlled exercises
- Clean internal and external construction near contact areas
- Stable strap and armhole relationship across movement
- Buyer-defined support and coverage target
Gym Training
Training programs can involve broader or faster upper-body movement and may require a different balance among band stability, strap geometry, coverage and material recovery. The racerback should be considered as part of the full Sports Bra architecture rather than used as evidence of training support on its own.
- Movement-specific strap and back stability
- Underband relationship with total garment position
- Material recovery appropriate to approved Fit
- Workmanship at high-movement construction areas
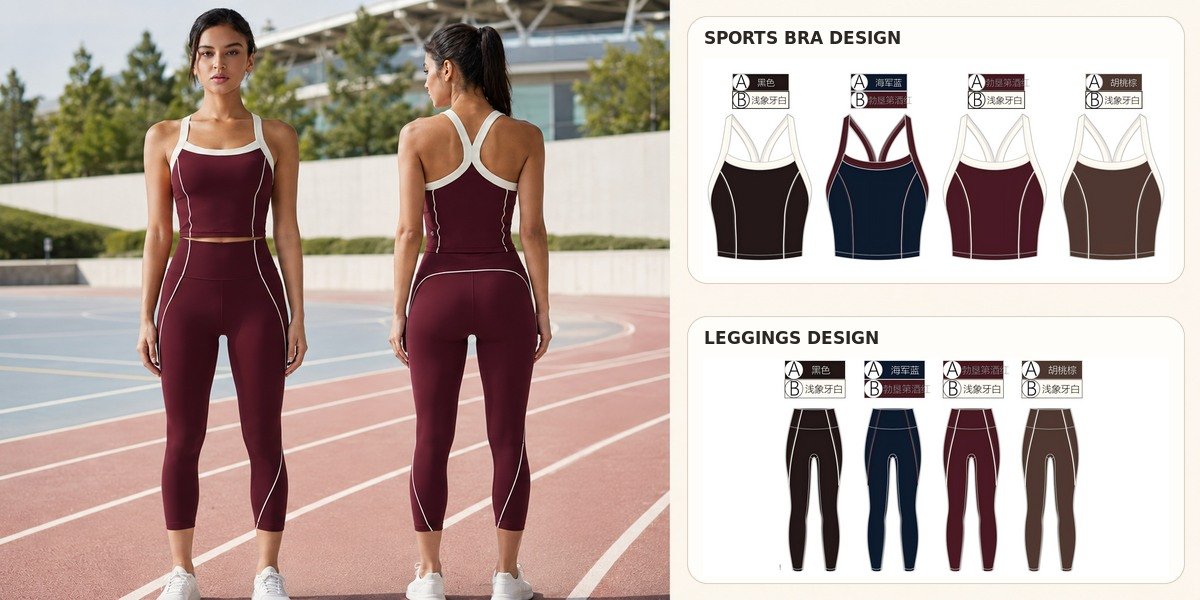
Running Direction
Where a buyer intends a racerback for running, support and motion-control requirements need to be defined separately and validated according to the buyer's own method. The racerback shape alone does not establish suitability. Strap width, underband, front coverage, internal construction, material and complete Fit all influence the final product direction.
- Buyer-defined support and movement requirement
- Strap and underband relationship under repeated movement
- Coverage and internal construction appropriate to brief
- Validation method agreed before performance claims
Compare Fabrics Around Racerback Fit and Recovery
MOVEVOX reviews fabric by composition, weight, surface, stretch and the final garment requirement. Racerback Fit should be approved in the actual production material, not from fiber names alone.
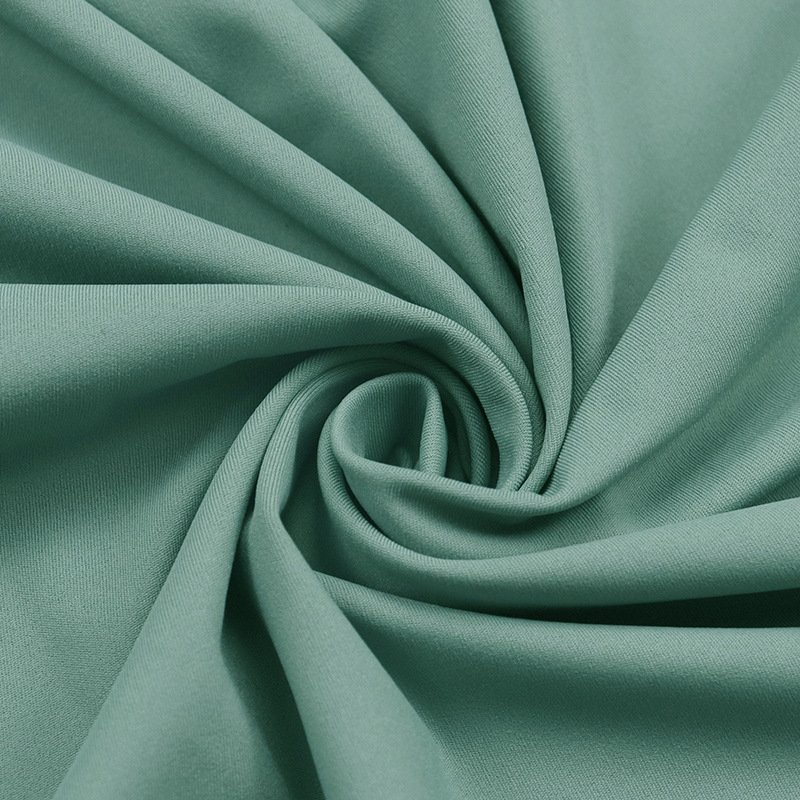
Naked Feel
Composition: 75–82% Nylon / 18–25% Spandex
Weight: 200–240 GSM
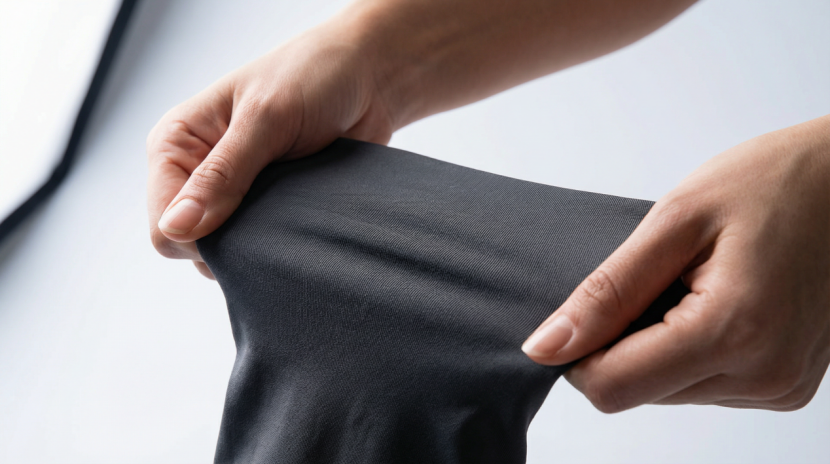
A smooth, soft activewear direction often relevant to Yoga and Studio products. Because a softer handfeel can still have different stretch and recovery behavior, strap and back geometry should be approved in the selected production material.
Soft / Stretch / Yoga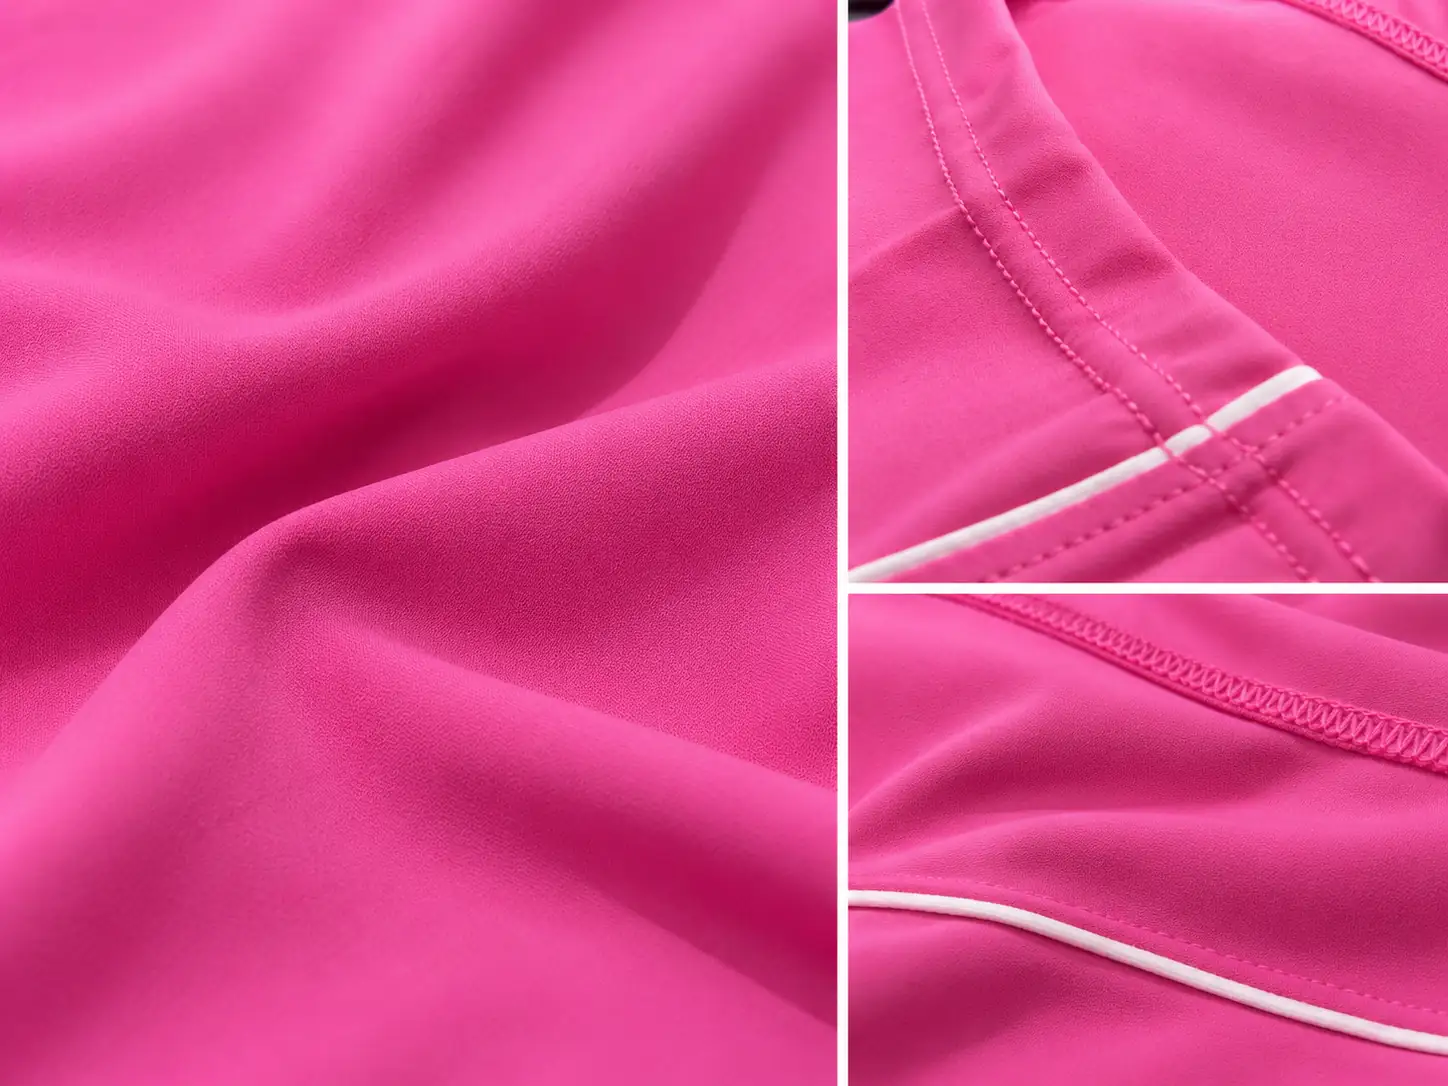
Nylon Spandex
Composition: 70–82% Nylon / 18–30% Spandex
Weight: 190–280 GSM
A broad activewear material family supporting multiple surfaces and Fit directions. The applicable GSM, recovery and finish need to be selected by project rather than assuming one Nylon-Spandex blend produces the same racerback behavior.
Stretch / Recovery / Activewear
Polyester Spandex
Composition: 75–90% Polyester / 10–25% Spandex
Weight: 160–250 GSM
A project-dependent route for activewear programs. Polyester content by itself does not prove quick-dry or moisture-management performance. Racerback suitability should be confirmed through the actual material specification and physical Sports Bra.
Activewear / Project-Specific / Stretch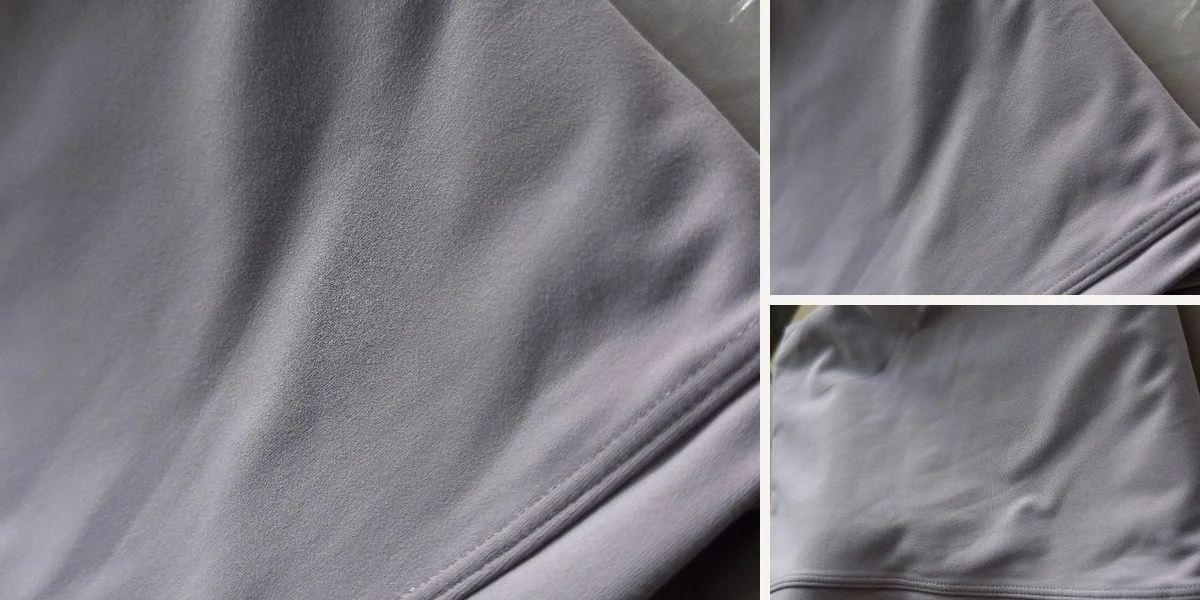
Brushed Fabric
Composition: 75–82% Nylon/Polyester / 18–25% Spandex
Weight: 210–270 GSM
A softer brushed surface can change perceived handfeel and local thickness around straps and bindings. Edge finishing and garment recovery should therefore be evaluated in the real fabric before bulk approval.
Brushed / Soft / Studio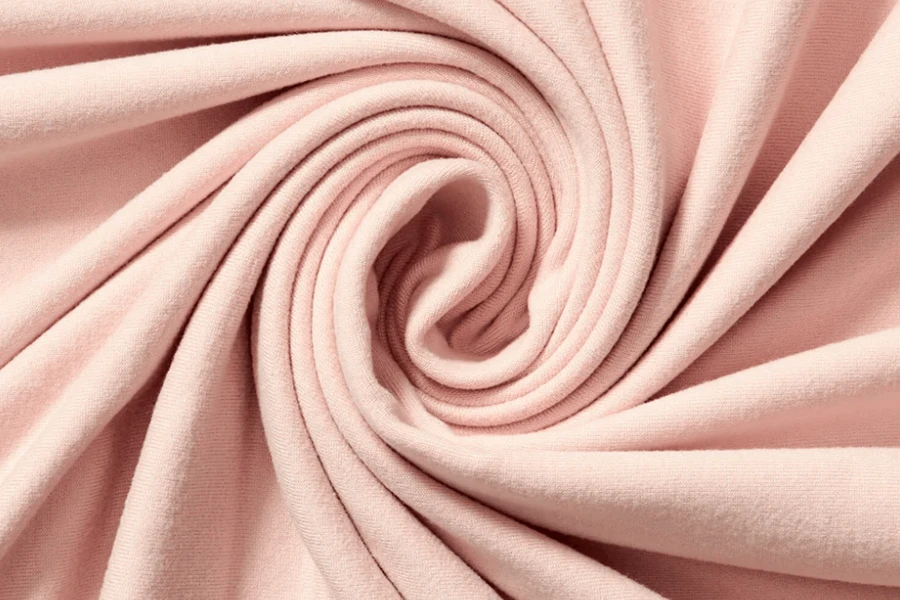
Peach Skin
Composition: 75–85% Nylon/Polyester / 15–25% Spandex
Weight: 190–240 GSM
A peach-surface direction can suit softer activewear concepts, but the surface finish should not be used as evidence of support or durability. Strap construction and Fit remain separate development points.
Soft Surface / Stretch / Activewear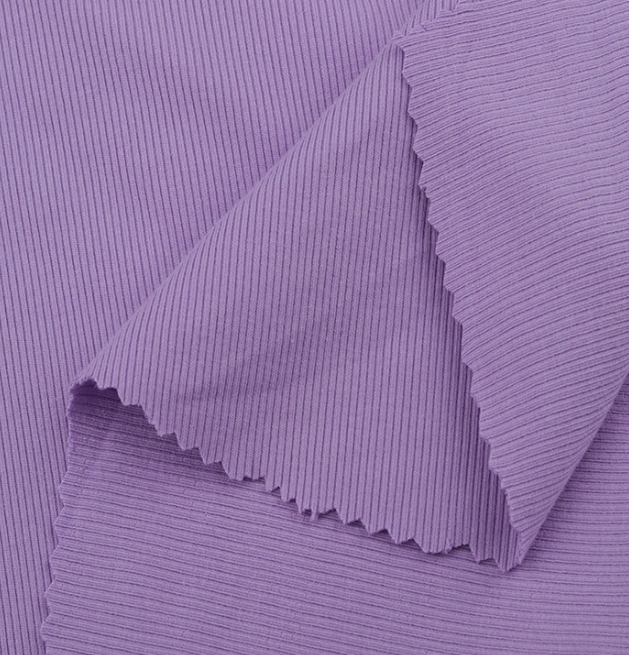
Ribbed Fabric
Composition: 75–90% Nylon/Polyester / 10–25% Spandex
Weight: 220–320 GSM
Rib changes surface texture and directional stretch. Racerback width, strap edge and back convergence should therefore be sampled in the exact rib construction instead of transferring measurements from a smooth fabric automatically.
Rib / Texture / Structure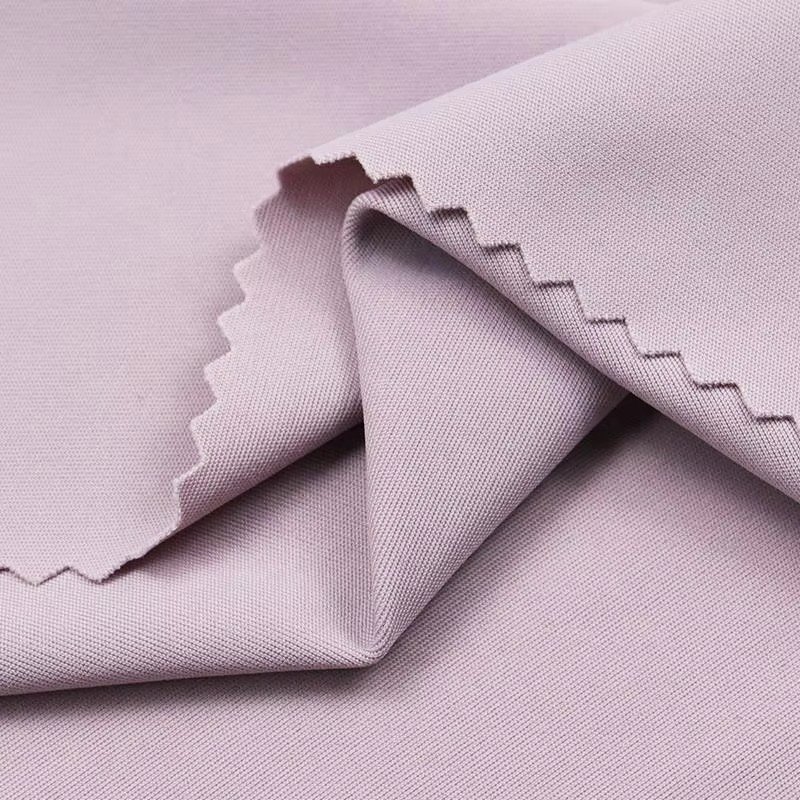
High Stretch
Composition: 70–85% Nylon/Polyester / 15–30% Spandex
Weight: 180–280 GSM
High stretch can improve range of extension but does not automatically create stable Fit. Recovery and garment dimensions remain important, especially where narrow straps and racerback geometry concentrate structural relationships into smaller areas.
High Stretch / Recovery / Fit
Seamless Yarn
Composition: 80–94% Nylon/Polyester + 6–20% Spandex
Weight: Structure dependent
Santoni yarn works together with program, stitch structure, rib, density and finishing. The finished racerback should therefore be approved as a knitted system rather than from yarn composition alone.
Seamless / Yarn / SantoniCompare Material Behavior Before Locking Racerback Geometry
A racerback pattern or Seamless program is only meaningful relative to the selected material. Stretch, recovery, weight and surface can change how the same geometry sits on the body.
| Parameter | Naked Feel | Nylon Spandex | Polyester Spandex | Ribbed | High Stretch | Seamless Yarn |
|---|---|---|---|---|---|---|
| Composition | 75–82% Nylon / 18–25% Spandex | 70–82% Nylon / 18–30% Spandex | 75–90% Polyester / 10–25% Spandex | 75–90% Nylon/Poly / 10–25% Spandex | 70–85% Nylon/Poly / 15–30% Spandex | 80–94% Nylon/Poly + 6–20% Spandex |
| GSM | 200–240 | 190–280 | 160–250 | 220–320 | 180–280 | Structure dependent |
| Surface | Smooth / soft | Multiple finishes | Multiple finishes | Rib texture | Project dependent | Knitted |
| Stretch | High direction | Project-specific | Project-specific | Structure-specific | High | Program dependent |
| Recovery | Must be approved | Must be approved | Must be approved | Must be approved | High stretch ≠ fixed recovery | Yarn + structure dependent |
| Strap concern | Edge visibility / stability | Depends on construction | Depends on construction | Rib distortion | Excess extension risk | Knit structure control |
| Back concern | Softness vs stability | Fit dependent | Fit dependent | Directional stretch | Geometry drift | Program / size relationship |
| Approval | Garment Sample | Garment Sample | Garment Sample | Garment Sample | Garment Sample | Finished Seamless Sample |
Selection Guidance
MOVEVOX should not describe the “highest stretch” fabric as automatically the best Racerback material. A successful product requires the selected material to work with strap width, back geometry, underband, edge construction and buyer-approved Fit. Any major material substitution should trigger renewed technical review before commercial production.
Separate Racerback Geometry From Pad and Lining Design
Racerback defines the back and strap system, not the front cup architecture. Pad and lining choices should therefore be approved as separate but connected product variables.

Removable Pad
A removable-pad Sports Bra uses an internal pocket so the component can be removed and reinserted. On a racerback product, the pad system should still be developed together with front coverage, lining, neckline and complete Fit. The racerback shape does not prove that the pad will remain correctly positioned or that the finished garment provides a particular support level.

Positioned Pad
A positioned or retained-pad direction can keep the component in a more defined internal location according to the approved construction. The product still needs physical sampling because material stretch, cup-area shape and lining can alter the result. MOVEVOX should not describe any retained construction as permanently immovable unless specific evidence supports that claim.
No Pad
A racerback can also be developed without padding when the buyer's product direction, material, lining and coverage support that choice. No-pad construction still requires control of neckline, opacity direction, internal layers and garment Fit. Product quality is determined by execution of the approved specification rather than the presence or absence of foam.
Choose Seamless or Cut-and-Sew for Racerback Development
MOVEVOX operates both manufacturing routes. The racerback should be assigned according to silhouette, materials, internal construction and Fit rather than treating one method as inherently superior.
Seamless Racerback
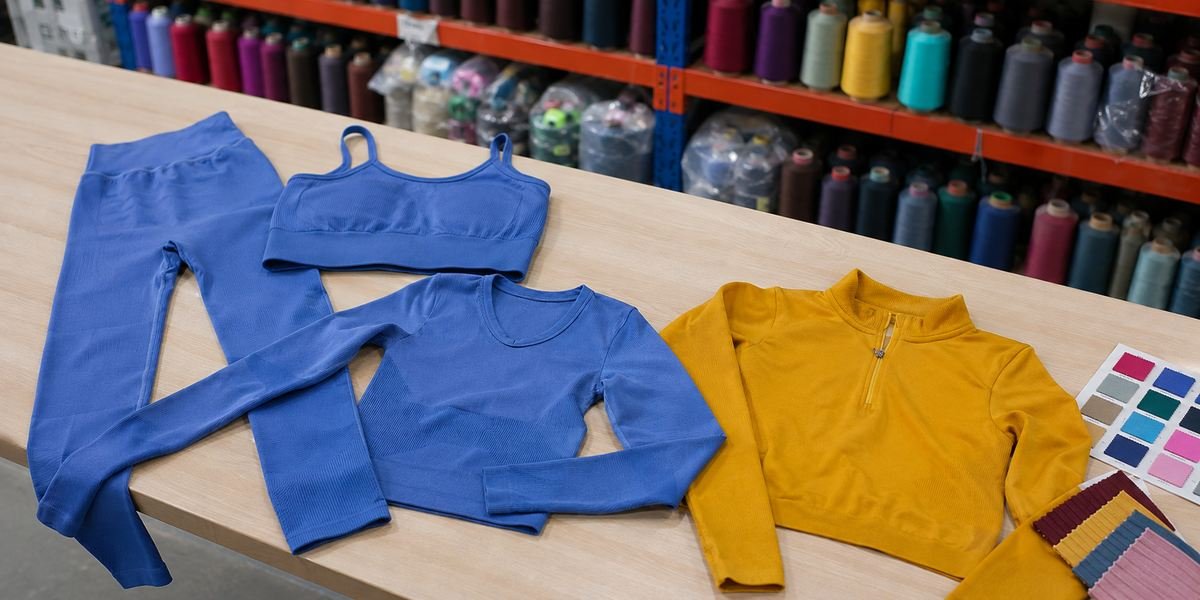
Santoni Seamless manufacturing can integrate back shaping, rib, density, engineered knit structure and selected visual zones directly into the knitted garment body. It can be appropriate when the buyer wants an integrated activewear silhouette with fewer conventional panel seams. The product may still require shoulder joining, pad openings, labels or other downstream sewing. Yarn, program version, garment size and finishing remain important controls, so the final finished Sports Bra—not the knitted blank—must become the approval standard.
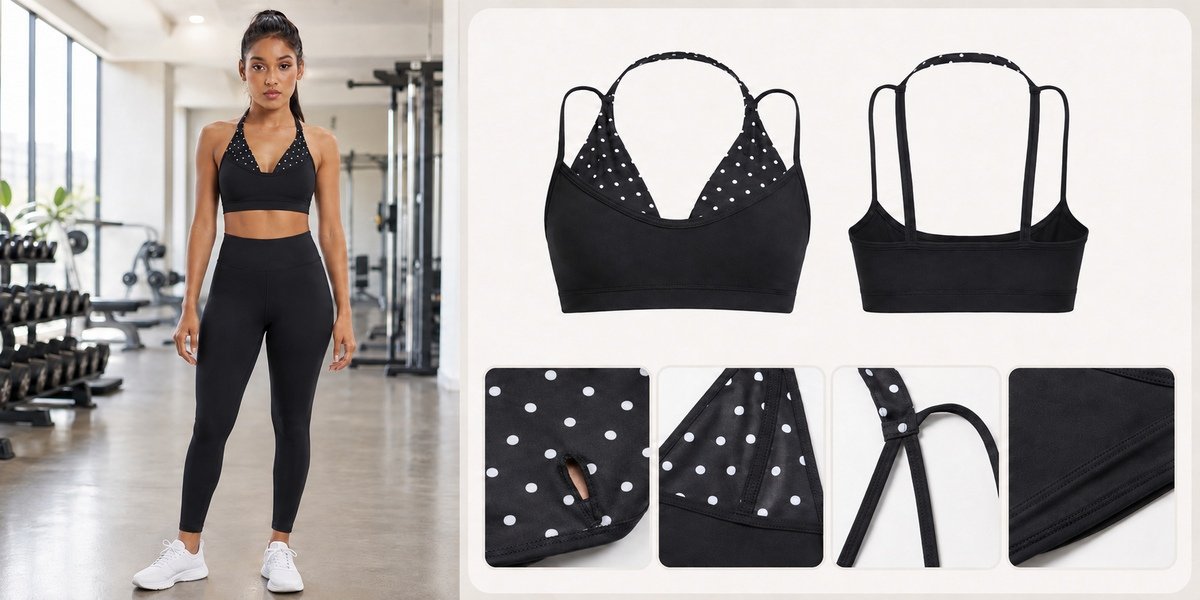
Cut-and-Sew Racerback
Cut & Sew provides greater freedom for shaped straps, separate back panels, multiple materials, lining, binding, elastic and selected hardware or pad constructions. Pattern engineering can control the exact shape of the racerback and its relationship with armholes, neckline and underband. The greater construction freedom can also create more joining, alignment and workmanship points. Approved patterns, BOM, seam methods and First Article inspection therefore become important controls before volume production continues.
Build Racerback Geometry Through Santoni Seamless Manufacturing
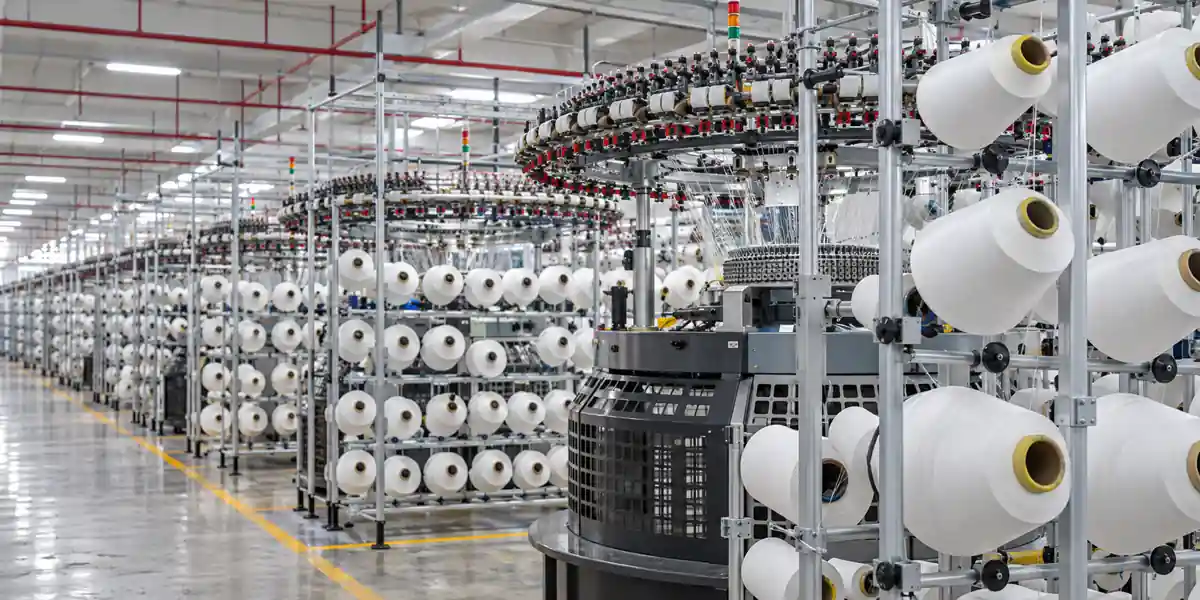
MOVEVOX operates 28 Italian Santoni machines. Seamless Racerback development combines yarn, program, knitted structure, finishing and any required downstream construction into one approved garment system.
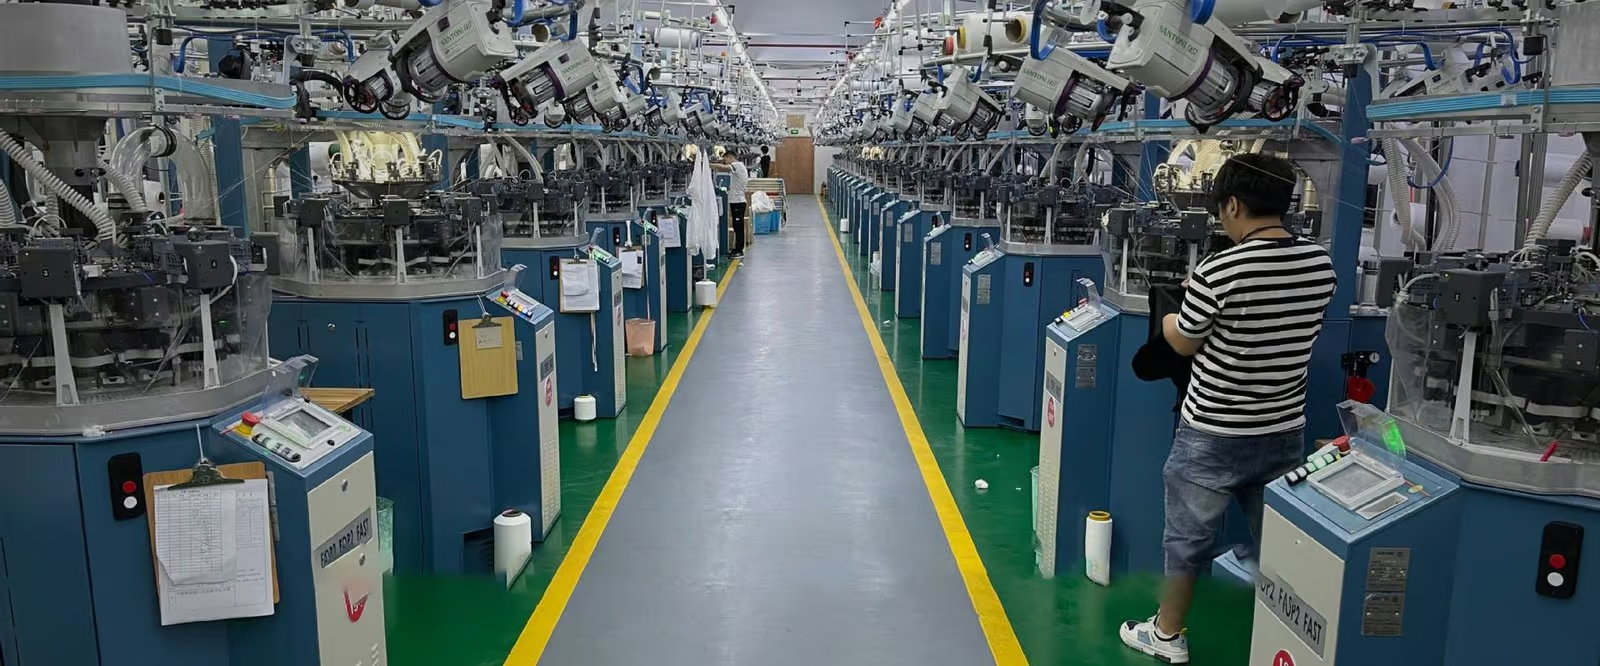
Santoni Knitting
Santoni machines produce the programmed garment body according to the applicable style, size, yarn and current knitting version. Machine capability becomes useful only when the approved structure can be repeated consistently.
28 Santoni machines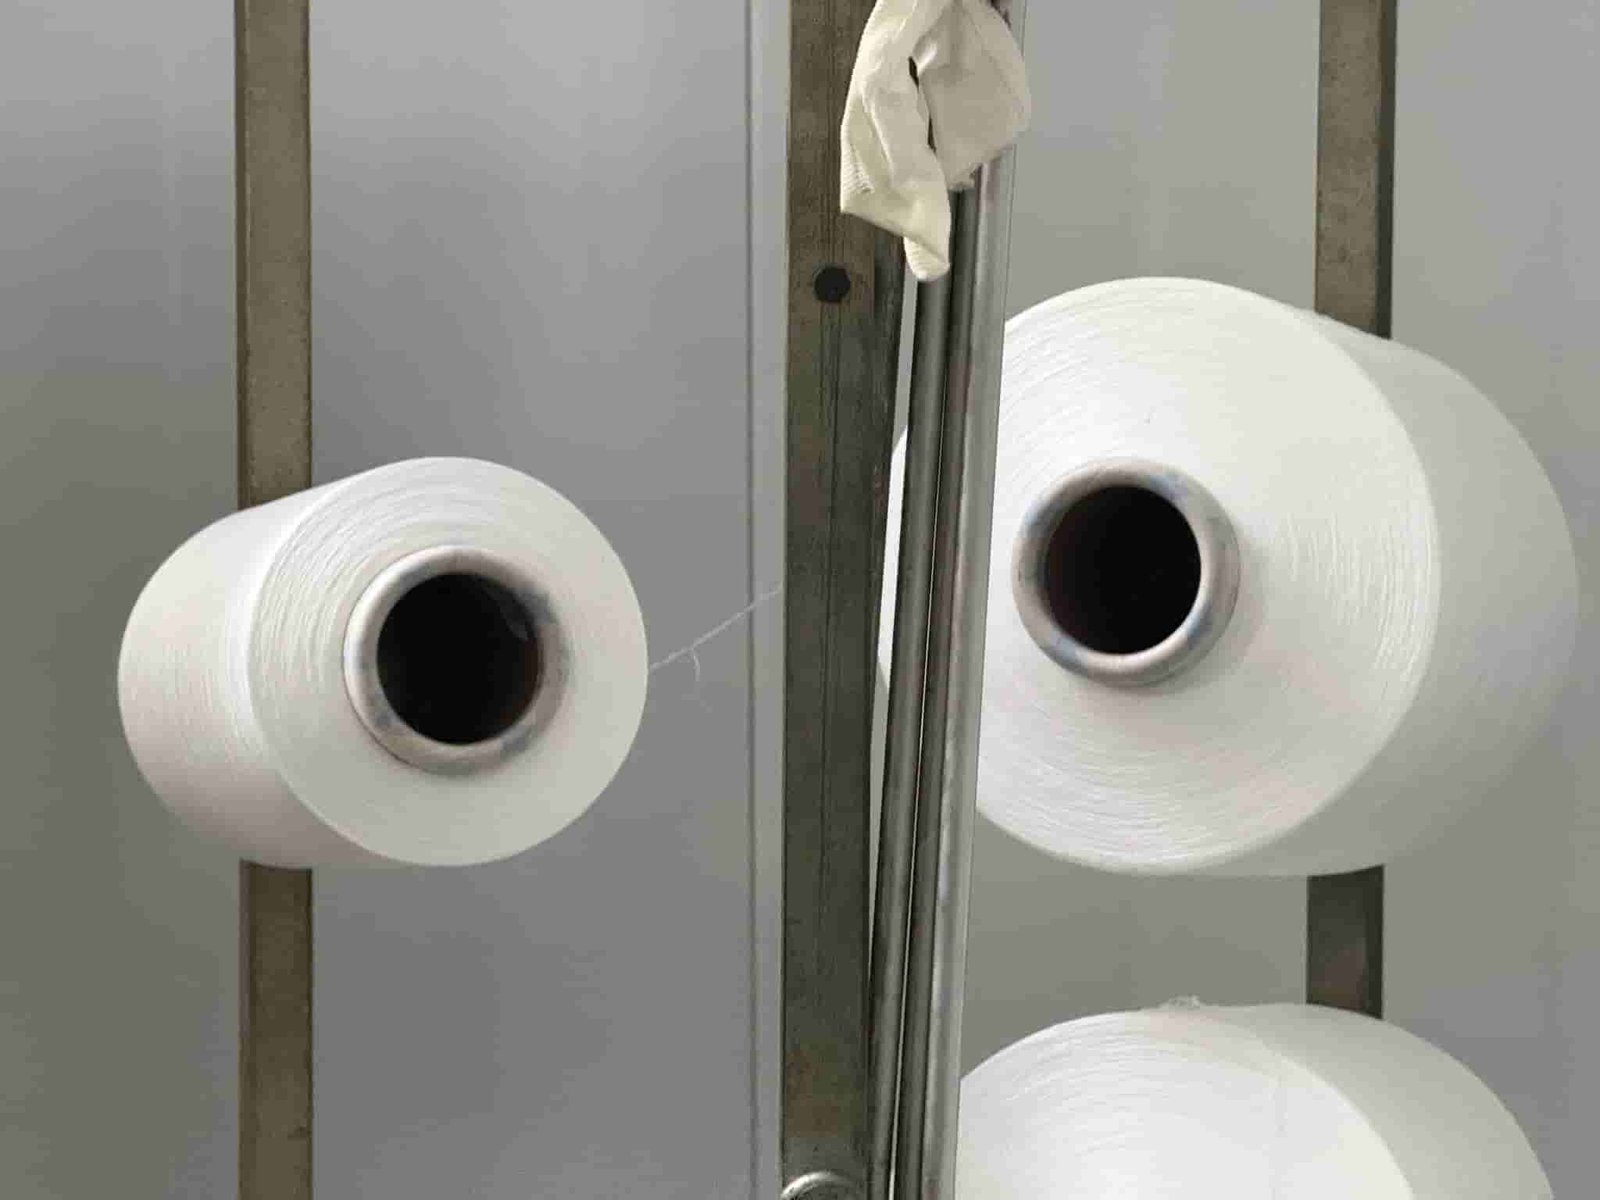
Yarn Control
Yarn composition, supplier, color and relevant lot information influence stretch and finished structure. The approved yarn direction should remain connected to the actual Racerback program.
Project-specific yarn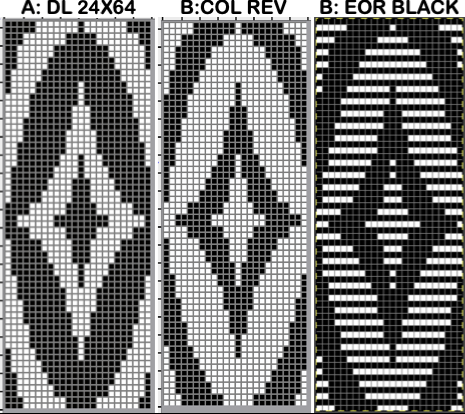
Program Development
The knitting program determines garment dimensions, rib, density and engineered structures. Version changes require control because they can alter the relationship among straps, back width and body measurements.
Current program version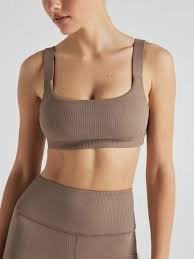
Trial Knitting
Trial garments allow the team to evaluate real knitted dimensions and racerback structure before the program becomes the production reference.
需要真实素材替换 if no releasable trial-knit evidence exists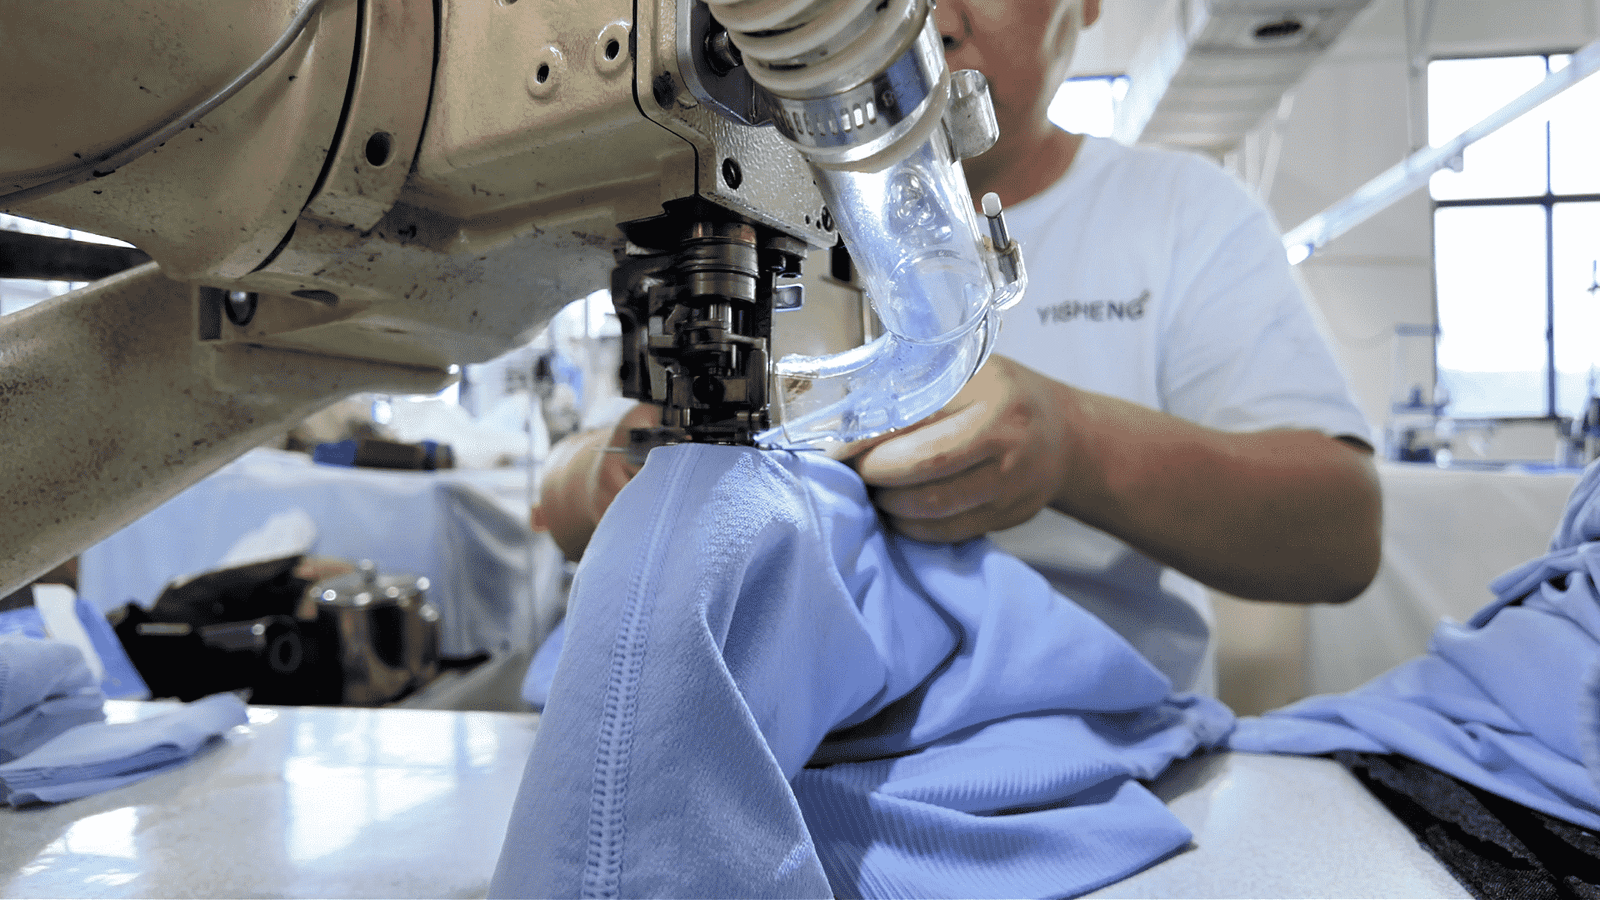
Post-Knit Sewing
Seamless does not necessarily mean zero sewing. Shoulder joins, pad openings, labels and selected finishing can still require downstream garment operations.
Project-specific finishing
Measurement & QC
The completed Sports Bra should be checked for relevant measurements, structure placement, symmetry, knitting defects, sewing and finished appearance before release.
Finished garment QCControl Racerback Geometry Through Cut-and-Sew Production
Cut & Sew converts the approved Racerback pattern, material, straps and internal construction into a sequence of controlled production steps before the finished Sports Bra is released.
Tech Release
The current Tech Pack, Measurement Chart, approved pattern, BOM, artwork and Approved Sample are reviewed before production starts. Open changes should be closed before the factory relies on the documents.
Owner: DevelopmentQC: Current VersionMaterial Check
Outer fabric, lining, elastic, thread, pads and applicable trims are checked against the released project information before cutting and assembly.
Owner: MaterialQC: Approved InputsPattern Release
The current production pattern defines front body, straps, back geometry, armholes, neckline and related pieces according to the approved size.
Owner: PatternQC: Pattern VersionCutting
Approved fabric is spread and cut into identified garment components. Cut pieces should remain correctly grouped by style, color and size.
Owner: CuttingQC: Panel IdentityStrap Assembly
Straps, bindings or relevant layered constructions are assembled using the approved seam and edge method before final garment joining.
Owner: SewingQC: Strap GeometryBack Assembly
The racerback convergence, side-back panels or center-back structure are assembled according to the approved pattern and workmanship standard.
Owner: SewingQC: Back AlignmentBand Assembly
Underband or elastic construction is connected to the garment using the applicable length, seam and finishing method.
Owner: SewingQC: Band MeasurementFirst Article
The first completed production garment is compared with the Approved Sample, measurements and relevant construction details before normal volume continues.
Owner: QCQC: Bulk ReleaseInline Control
Production is checked for strap symmetry, racerback alignment, armhole, measurements, stitching and recurring workmanship issues while the order is still in progress.
Owner: QCQC: Process StatusFinal Inspection
Finished garments are reviewed against applicable workmanship, measurements, branding and packaging requirements before shipment release.
Owner: QCQC: Shipment Release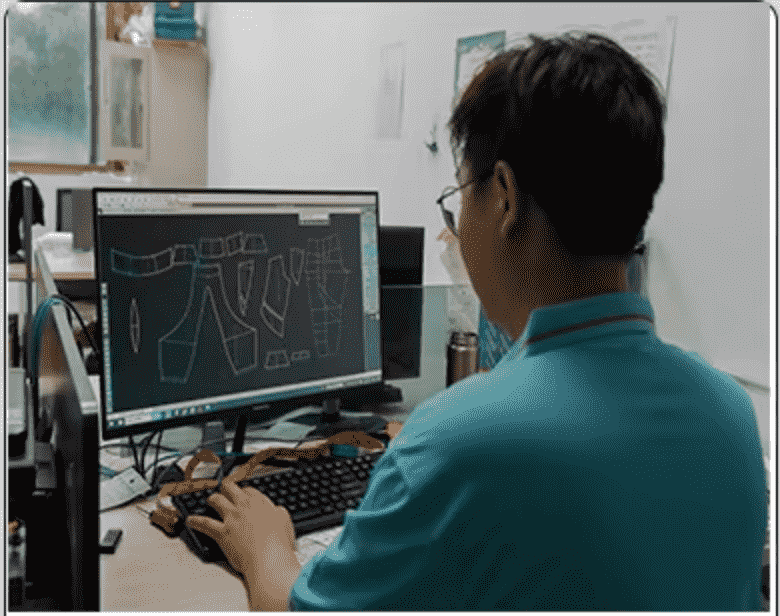
Prepare the Inputs for Racerback Sports Bra Development
Clear technical inputs reduce avoidable sampling cycles. MOVEVOX can begin with incomplete information, but unresolved Racerback, Fit, material or commercial details still need buyer approval before bulk.
Product Reference
Provide a Tech Pack, legal physical sample, sketch, image or sufficiently clear concept defining the desired Sports Bra silhouette. The reference should show the intended front and back rather than only a front product photograph.
Racerback Direction
Define the intended back style—classic, wide, narrow, high-neck, open or another project-specific direction. If the exact geometry is not yet fixed, identify which visual elements are mandatory and which can be developed.
Strap Requirements
Provide strap width, effective length, adjustability, edge construction or attachment information where already established. If these variables remain open, they should become explicit sample-development decisions rather than factory assumptions.
Measurement Chart
Buyer POMs, grade rules and tolerances give MOVEVOX clearer control of underband, body length, straps, back width, armhole and neckline across the intended size range.
Activity Direction
State whether the product is intended for Yoga, Pilates, Gym, Running or another use. The activity informs movement and Fit review but does not by itself establish support performance.
Support Target
Define the intended support direction separately from the word “racerback.” The required band, material, coverage and internal structure may differ even when two products share a similar back silhouette.
Fabric Specification
Provide nominated material or target composition, GSM, handfeel, stretch, recovery and surface direction. If the factory proposes alternatives, each option should be approved in the physical garment.
Pad & Lining
Define removable, positioned or no-pad direction together with lining or pocket expectations where relevant. Racerback geometry does not automatically define the front internal construction.
Size Range
Specify the intended commercial sizes and any buyer-specific grading rules. A wider size range may require Size Set or representative-size review before final approval.
Branding & Packaging
Provide final logo, labels, hangtag, barcode, SKU and packaging requirements before commercial production release. Branding should not hide unresolved product-development issues.
Testing Requirements
Share buyer RSL, wash, Fit, wearer, material or third-party testing requirements before the supplier is expected to produce corresponding evidence.

Use Each Racerback Sample to Close Specific Risks
Each sample stage should answer a different technical question. One general “sample approved” comment should not hide unresolved Racerback, Fit, grading or production details.
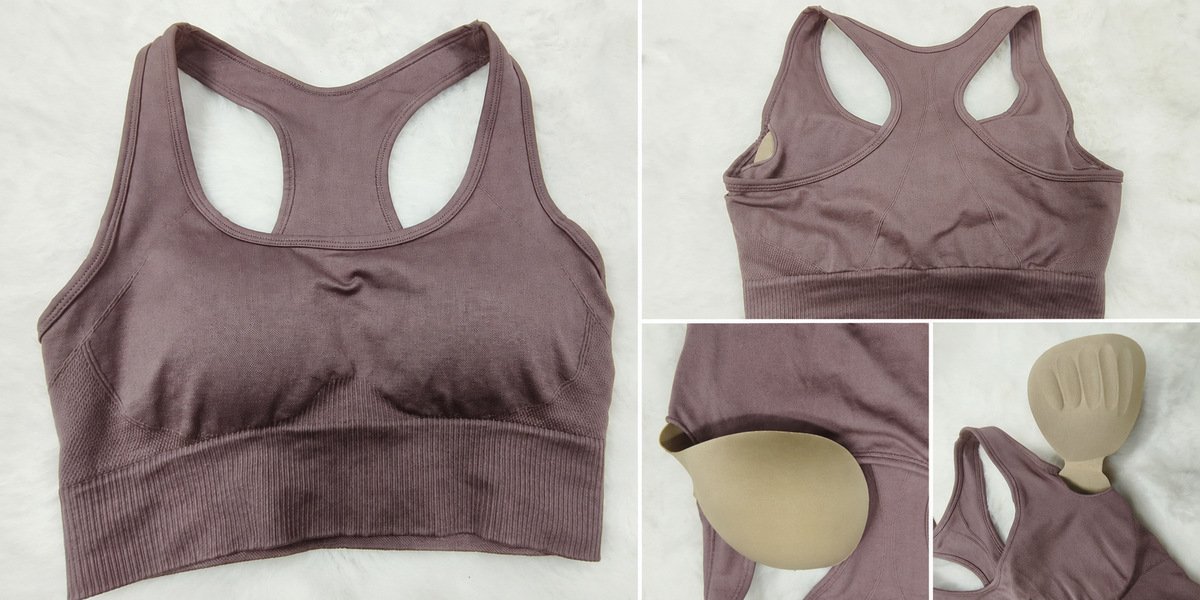
Development Sample
The first physical version establishes whether the silhouette, preliminary Racerback geometry, material and manufacturing route can be converted into a workable Sports Bra.
Buyer inputs: Product direction and reference; Initial size and material requirements; Racerback and support brief
MOVEVOX outputs: Physical development sample; Measurement record; Open-point list
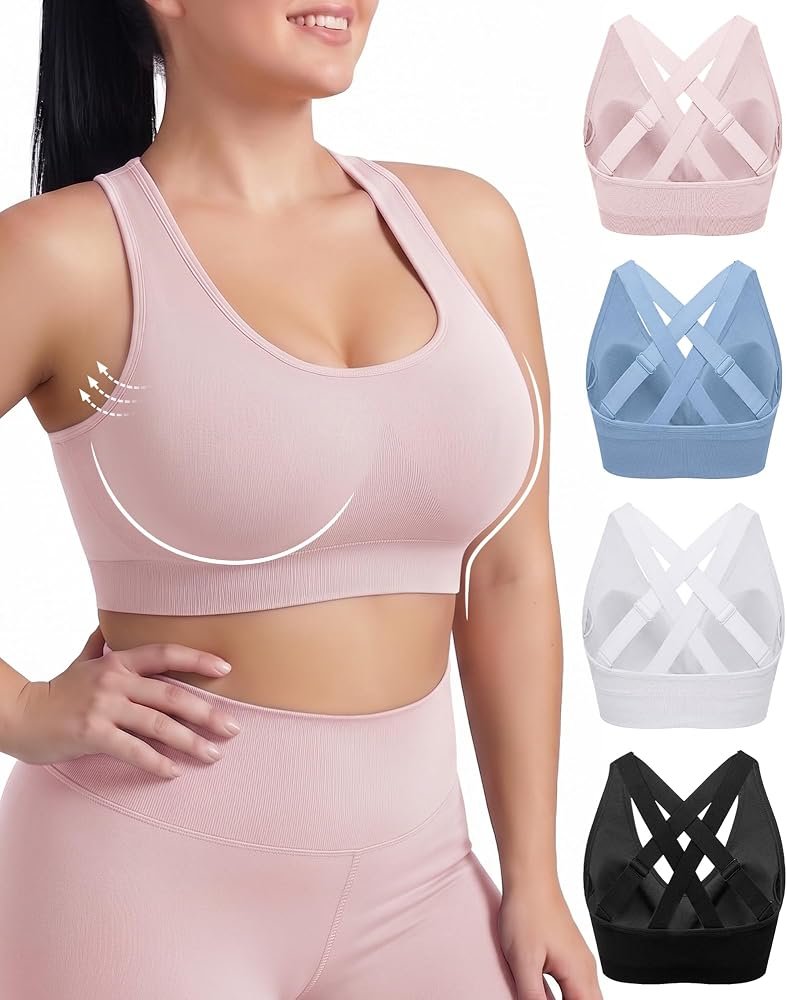
Fit Sample
This stage evaluates the garment on the buyer's Fit Model or defined fitting condition. Strap path, convergence point, armhole, neckline, underband and movement observations are reviewed together.
Buyer inputs: Fit comments; Measurement review; Movement requirement
MOVEVOX outputs: Fit measurements; Technical diagnosis; Proposed revisions
Revised Sample
The next version incorporates approved changes without unnecessarily altering unrelated areas that were already accepted.
Buyer inputs: Consolidated revision comments; Updated technical information
MOVEVOX outputs: Revised Racerback sample; Updated pattern/program; Version reference
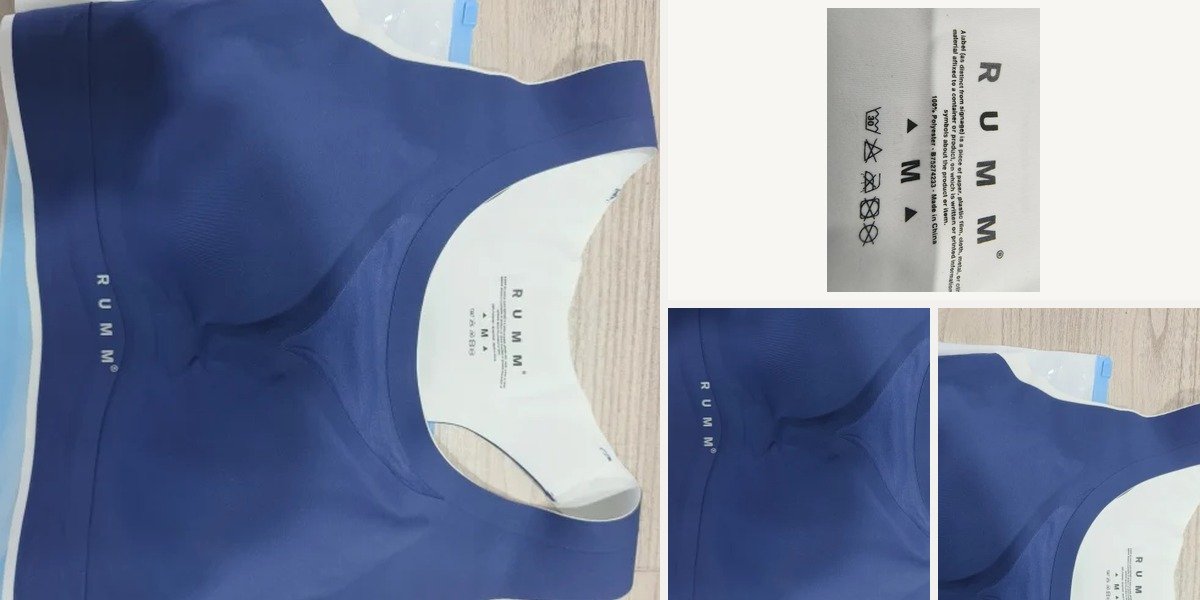
Size Set
Representative or complete size samples can be used where required to validate the relationship among strap length, back width, convergence, armhole, neckline and underband beyond the base size.
Buyer inputs: Grade rules; Required sizes; Fit standard
MOVEVOX outputs: Size samples; Measurement results; Open grading issues
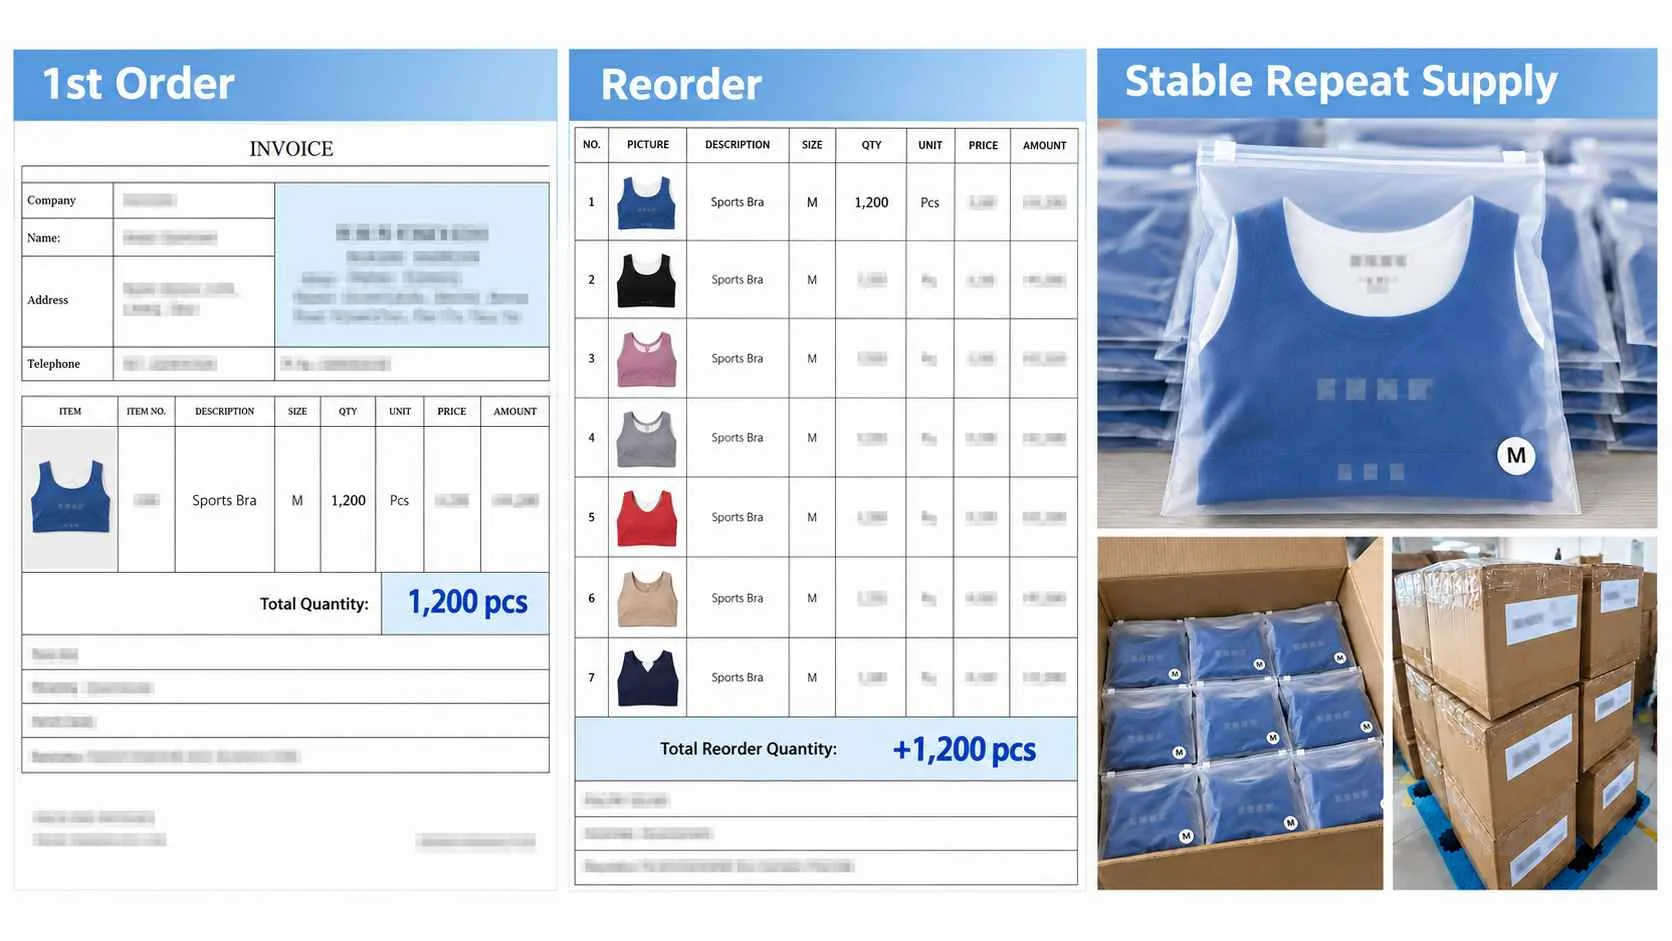
PP Sample
The Pre-Production stage confirms final material, construction, measurements, branding and applicable packaging information before commercial production release.
Buyer inputs: Final technical specification; Artwork and branding; Formal approval
MOVEVOX outputs: PP sample; Production files; QC checkpoints
Turn Racerback Fit Problems Into Measurable Revisions
A useful revision should connect a visible or wearing problem to the exact technical variable being changed. Before-and-after evidence should come from the same development project.
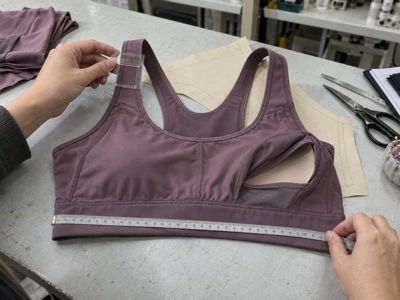
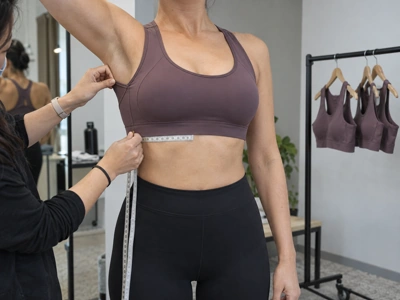
Strap Near Neck
The first sample places the strap path closer to the neck than the buyer's intended Fit, creating an unwanted upper-body relationship during selected movement.
AfterStrap Path Revised
Shoulder position, strap angle, effective length or back convergence is revised according to the confirmed root cause, then the updated sample is reviewed under the same condition.
Junction Too High
The center-back convergence sits higher than the buyer's visual and Fit target, changing the proportion of the racerback and the effective strap direction.
AfterJunction Rebalanced
Back body, strap length and convergence reference are adjusted within the current pattern or program while preserving unrelated approved areas where possible.
Armhole Restrictive
The initial armhole or adjacent strap geometry limits the intended movement or creates unwanted pressure during the buyer's Fit review.
AfterArmhole Revised
The confirmed measurement, curve, side height, binding tension or material relationship is changed, then re-evaluated on the physical Sports Bra.
Back Asymmetry
Left and right straps or the convergence point appear unbalanced in the development sample even though broad garment measurements may remain close to target.
AfterAlignment Controlled
Pattern, cutting, joining or knitted-structure causes are corrected, and center-back plus left-right references are added to the approval or QC standard.
Resolve Racerback Size-Set Questions Before Commercial Production
Size Set review addresses the commercial objections that remain after a base-size Racerback is accepted. The buyer should know what is being graded, sampled and approved.
Does one approved base size prove the full range?
No. A correct base size confirms only the approved reference size. Strap length, back width, convergence, armhole, neckline and underband can change at different rates across the commercial range. Where the buyer requires broader validation, MOVEVOX can prepare Size Set or representative-size samples and compare them with the applicable grade rules and measurement tolerances before production release.
Do all Racerback measurements grade by one percentage?
No. Different POMs can require different grade increments. Underband circumference, strap length, back width and armhole are related but are not necessarily proportional. MOVEVOX should follow the buyer's size chart and grading logic where supplied. If the grade rules are incomplete, unresolved areas should remain development decisions until physically reviewed and approved.
Which sizes should be physically reviewed?
The exact requirement belongs to the buyer and project. Some brands request the complete Size Set; others select representative small, base and larger sizes according to their internal Fit protocol. MOVEVOX should not publish one mandatory set for every customer. The objective is to capture geometry changes that cannot be reliably judged from digital grading alone.
What should the Size Set check?
The review can include underband, body length, strap length and width, back convergence, racerback width, armhole, neckline, side coverage and overall wearing Fit. Relevant movement can also be repeated where the buyer uses it as part of Sports Bra approval. The exact list should follow the technical specification rather than a generic Racerback checklist.
Can material changes affect an approved grade?
Yes. A change in stretch, recovery, GSM, surface or internal construction can alter how the same nominal dimensions Fit on the body. A substitute fabric therefore should not be assumed to preserve the approved size relationship automatically. Significant material changes should be reviewed against the affected sample or Fit approval before they enter commercial production.
When is the size range ready for bulk?
The range is ready when the required measurements, representative samples and applicable Fit comments have been sufficiently closed according to the buyer's approval system. MOVEVOX then freezes the relevant pattern or Seamless-program versions, size references and QC points so commercial production uses the same approved technical basis rather than a later uncontrolled interpretation.
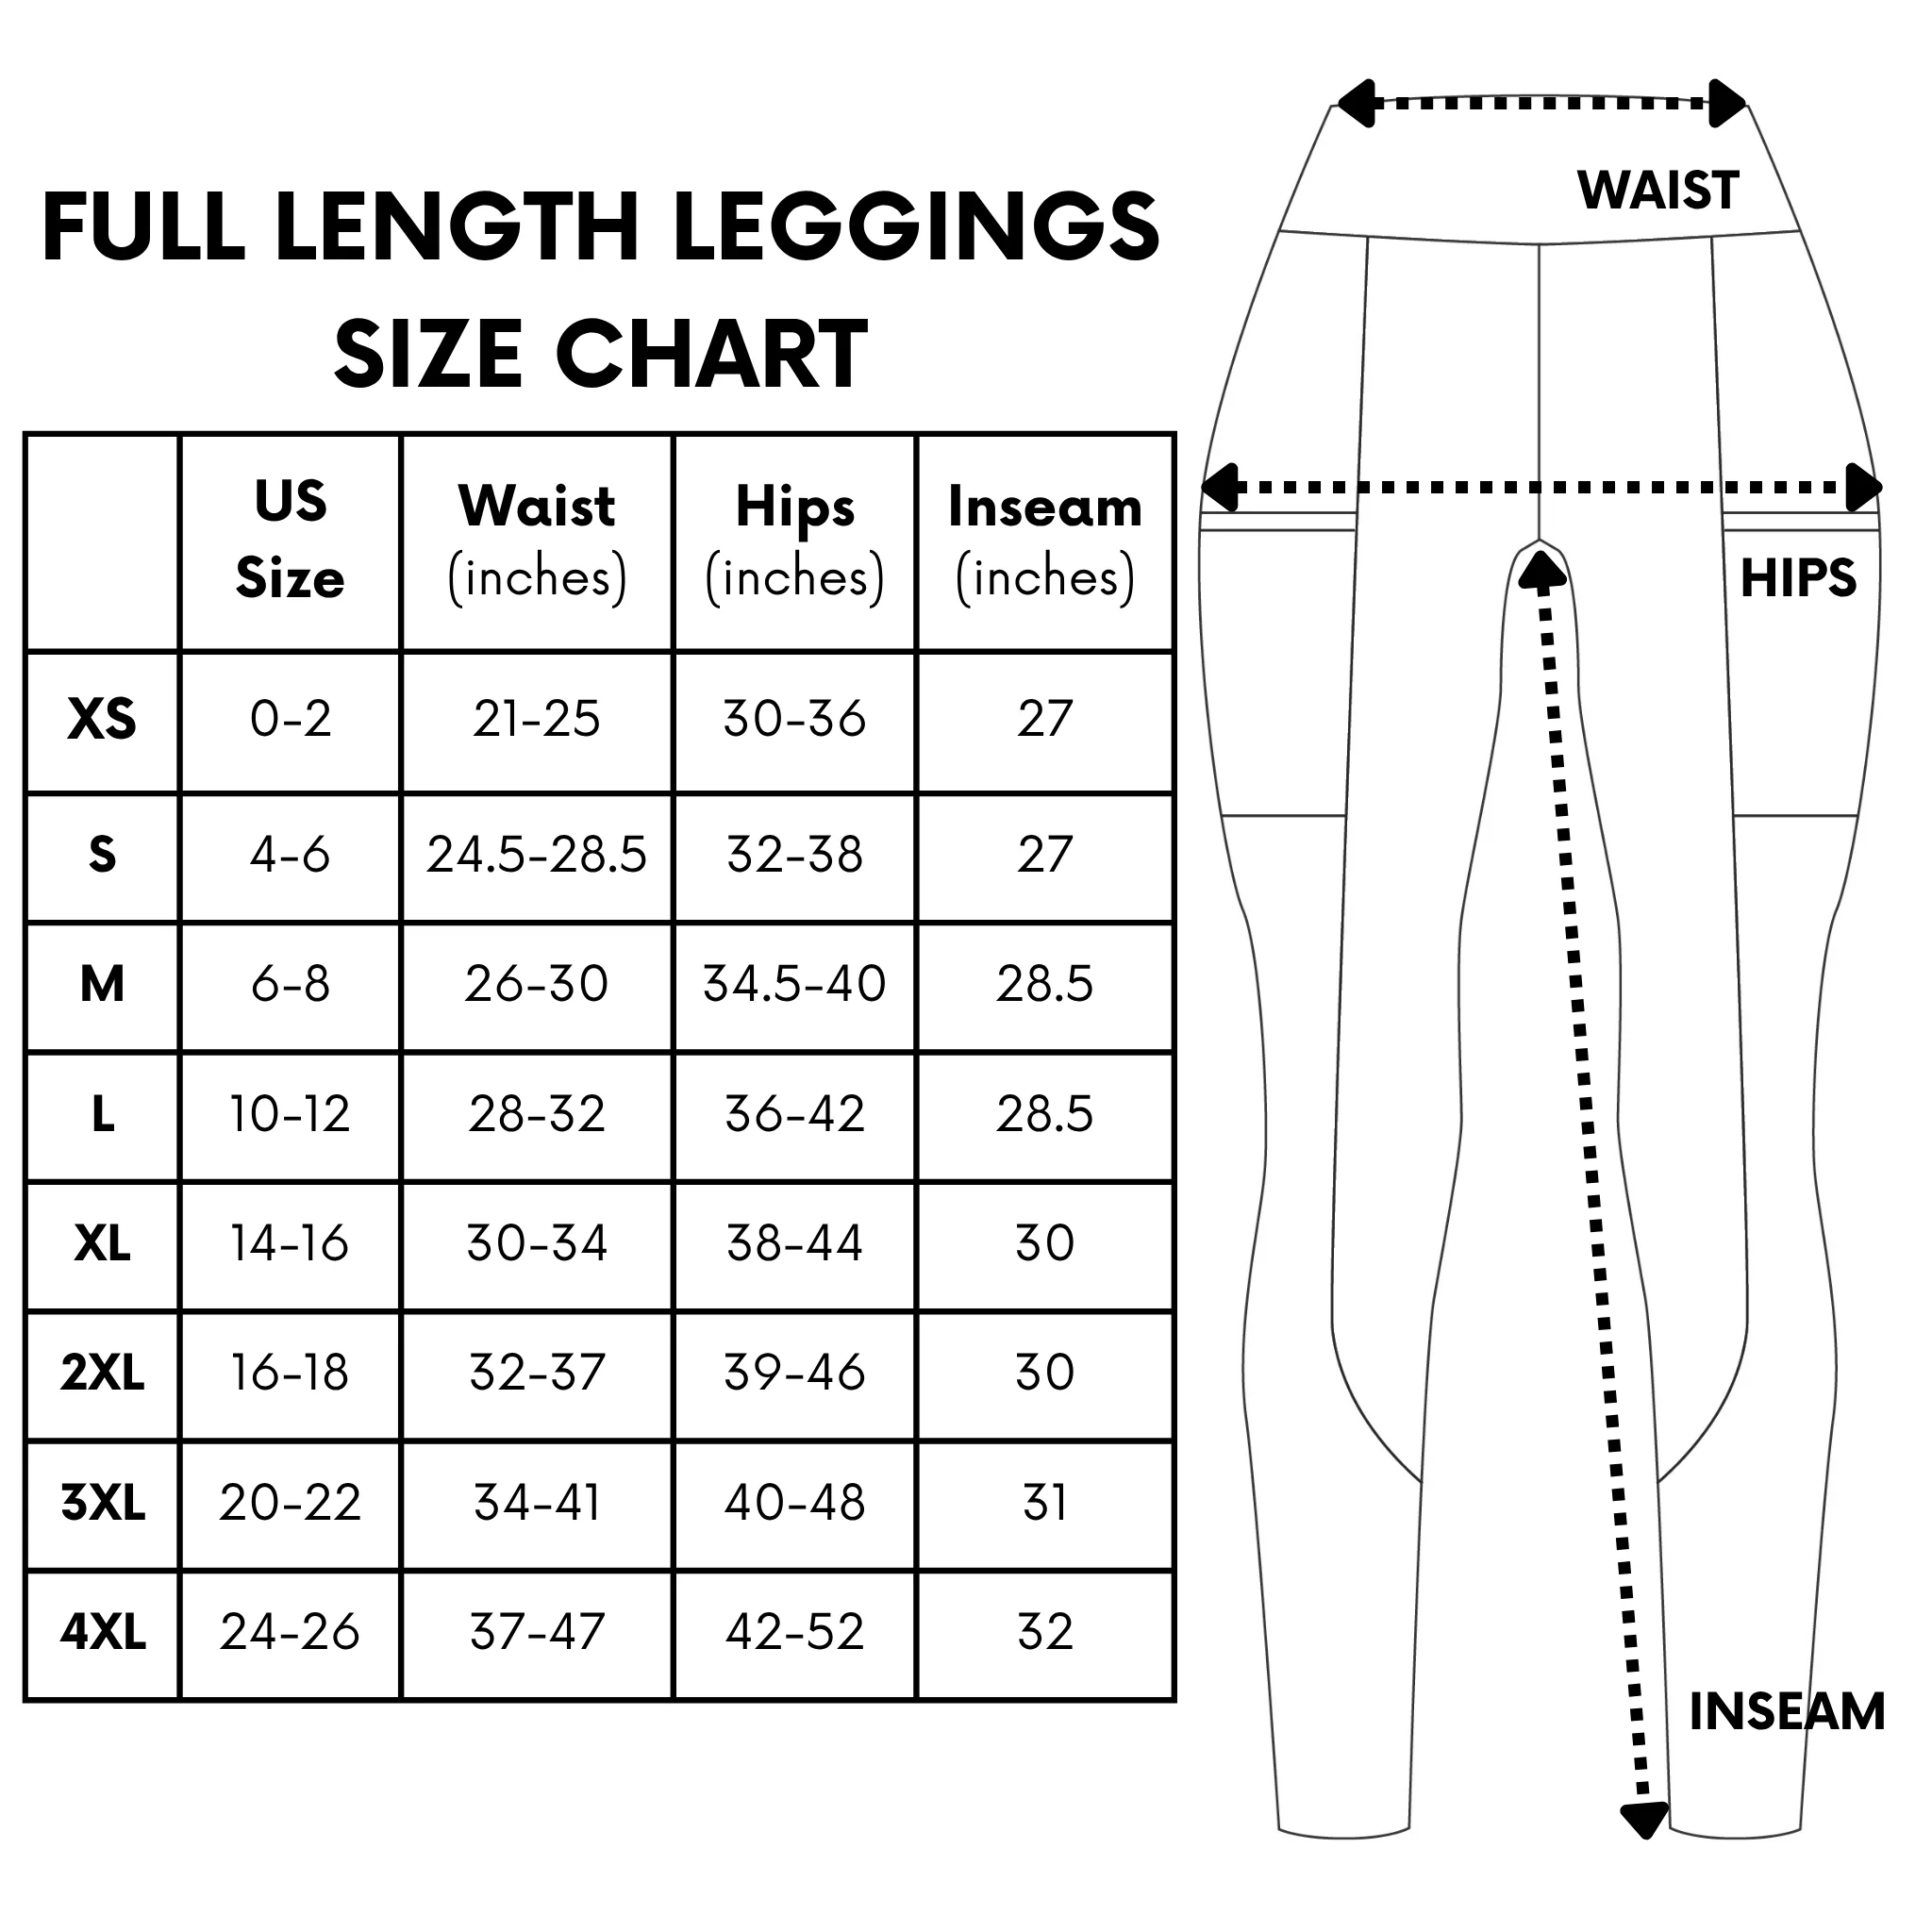
Build Racerback Products Into a Private Label Program
MOVEVOX can coordinate the Racerback product with materials, color, branding, labels and packaging. Product geometry and Fit should be technically approved before commercial branding becomes the focus.
Product
Racerback product development can begin from a Tech Pack, legal reference, sketch, image or defined concept. MOVEVOX reviews strap path, back convergence, armhole, underband, support direction, pad or lining and the appropriate Seamless or Cut & Sew route.
- Classic or buyer-defined racerback
- Seamless or Cut & Sew
- Buyer measurement chart
- Pad / lining direction
- Size-range development
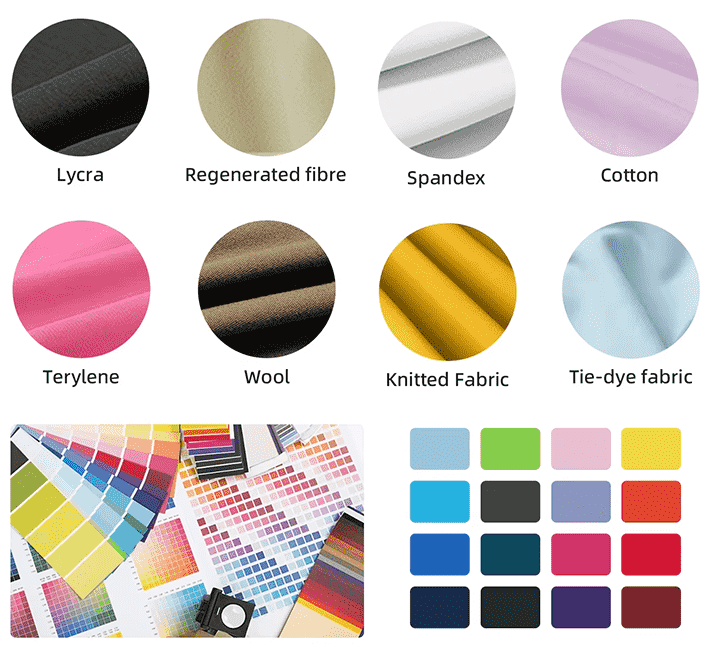
Material & Color
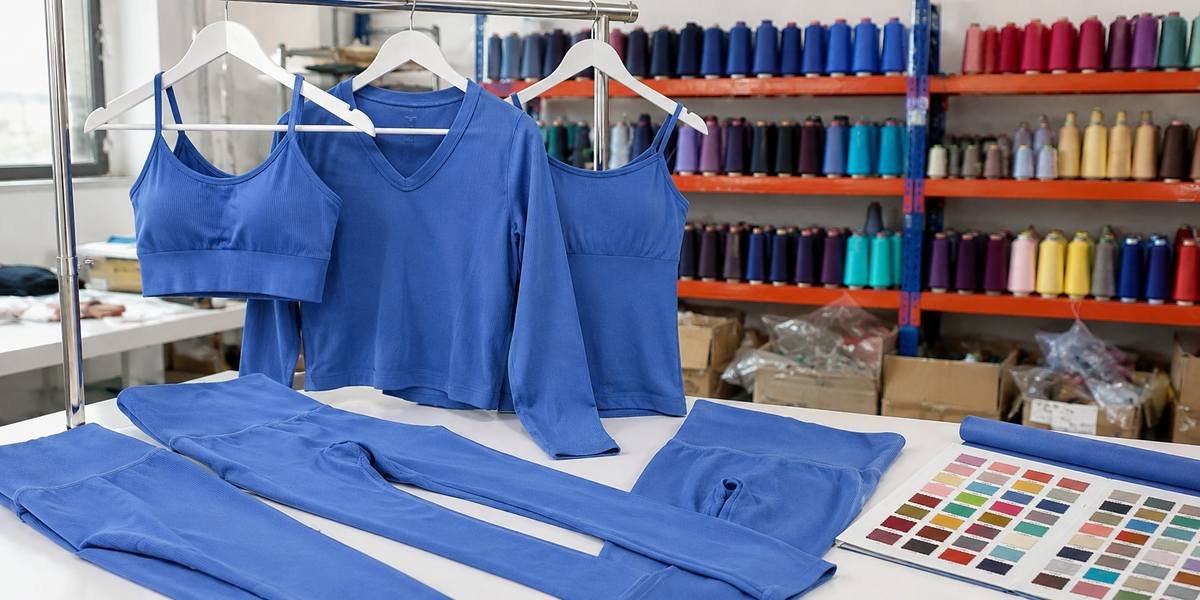
Outer fabric, Seamless yarn, lining and elastic should be approved against the actual Racerback sample. Fiber composition or color alone does not prove Fit stability. Custom color can also create material-level minimums that differ from the base garment MOQ.
- Nylon-Spandex
- Polyester-Spandex
- Naked Feel directions
- Rib / brushed options
- Custom color review
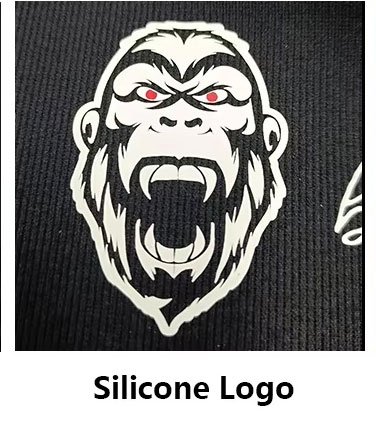
Logo
MOVEVOX can coordinate common branding methods including Heat Transfer, Screen Print, Silicone, Embroidery, Jacquard and Woven Label where technically appropriate. Final position and process should be sampled on the real garment because Racerback logos may sit near curved, stretched or high-movement back areas.
- Heat Transfer
- Screen Print
- Silicone
- Embroidery
- Jacquard
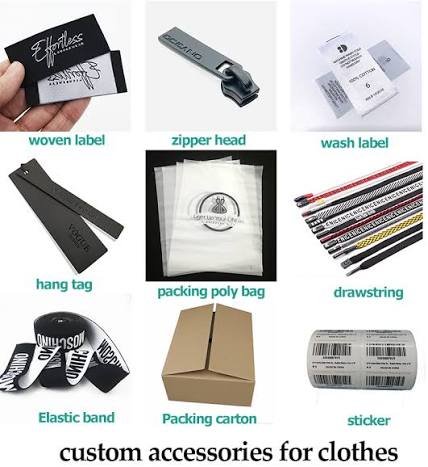
Labels & Trims
Main labels, care labels, size labels, hangtags and approved trims can be linked to the product BOM. Label location should not interfere with upper-back contact areas, and any branded elastic or special trim can introduce separate supplier minimums or development requirements.
- Main label
- Care label
- Size label
- Hangtag
- Approved trims
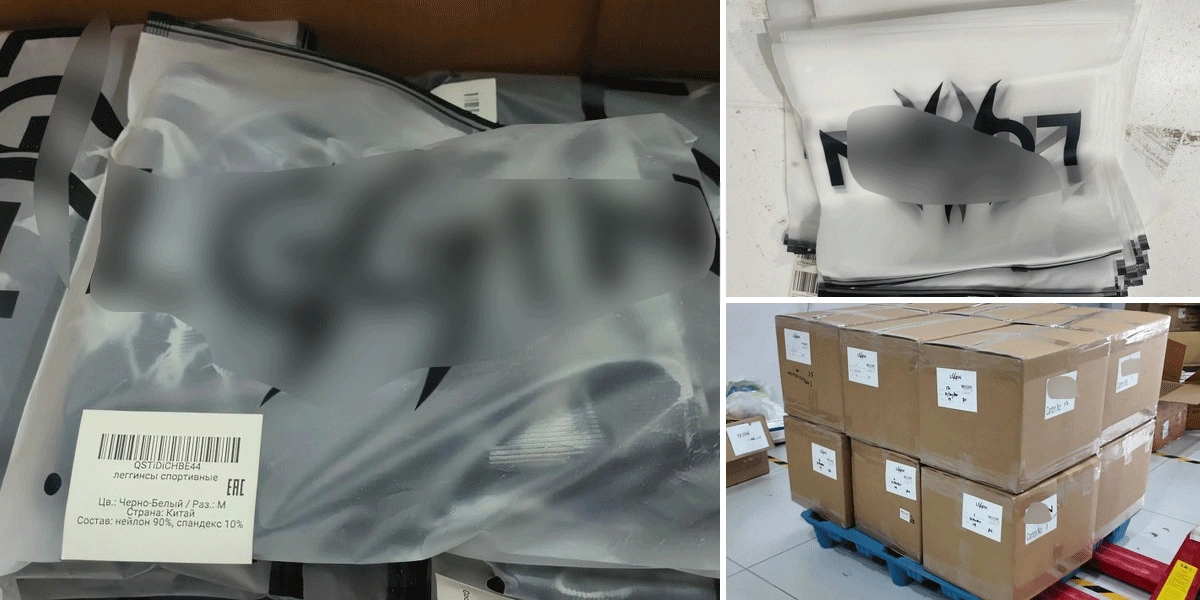
Packaging
Individual polybags, barcodes, SKU labels, stickers, carton marks and buyer-defined packaging can be managed by the applicable style, color and size combination. A multi-SKU Racerback range requires correct product identity through packing so the right garment, branding and commercial SKU remain connected.
- Polybag
- Barcode / SKU
- Sticker
- Carton mark
- Buyer packaging
Protect Approved Racerback Geometry During Bulk Production
The Racerback becomes commercially reliable only when the technical relationship approved in sampling is transferred into current production documents, First Article and in-process QC.
Strap Geometry
Approved strap width, length, attachment and path should remain connected to the current pattern or program and applicable size.
Back Convergence
The approved center-back relationship should be reproduced without uncontrolled movement in junction height, width, symmetry or orientation.
Armhole
Armhole curves and related side-height measurements should follow the approved size and current production reference.
Material
Outer fabric, yarn, lining and elastic should correspond to approved references because substitutions can change how identical geometry Fits.
Pattern / Program
Cut & Sew pattern or Seamless program version must remain connected to the released style, size and approved technical revision.
Underband
The lower garment reference should remain consistent with the Fit Sample so bulk does not change total Racerback position through band variation.
First Article
The first completed production garment provides an early opportunity to compare the actual commercial construction against the Approved Sample.
Bulk QC
In-line and final inspection should include applicable Racerback measurements, alignment, workmanship, branding and packaging before shipment release.
Handover Control
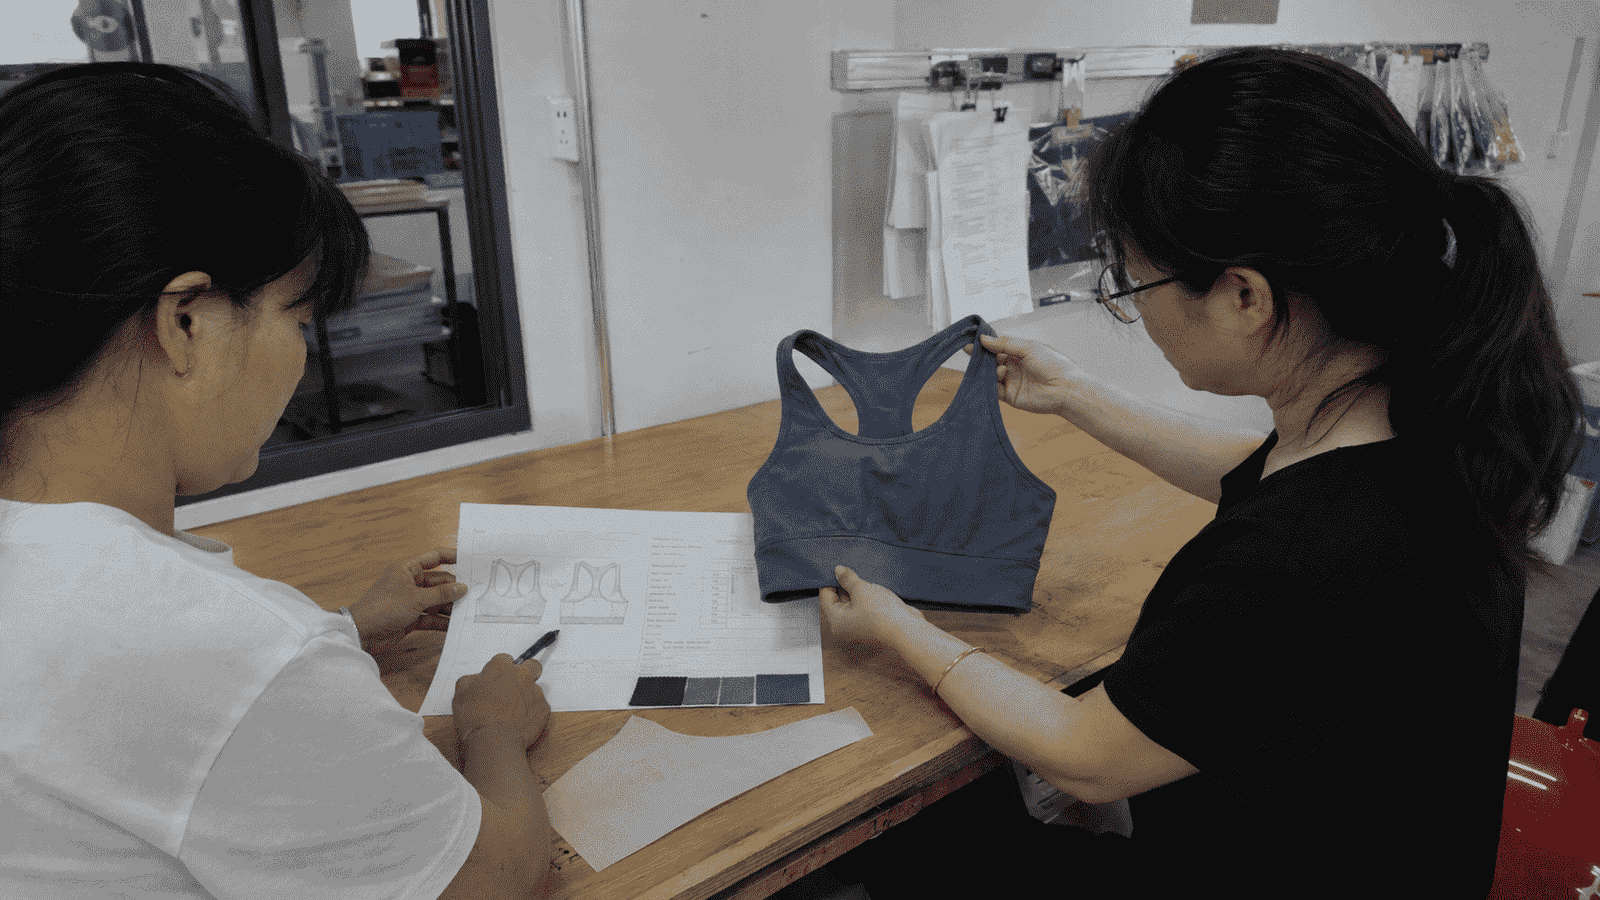
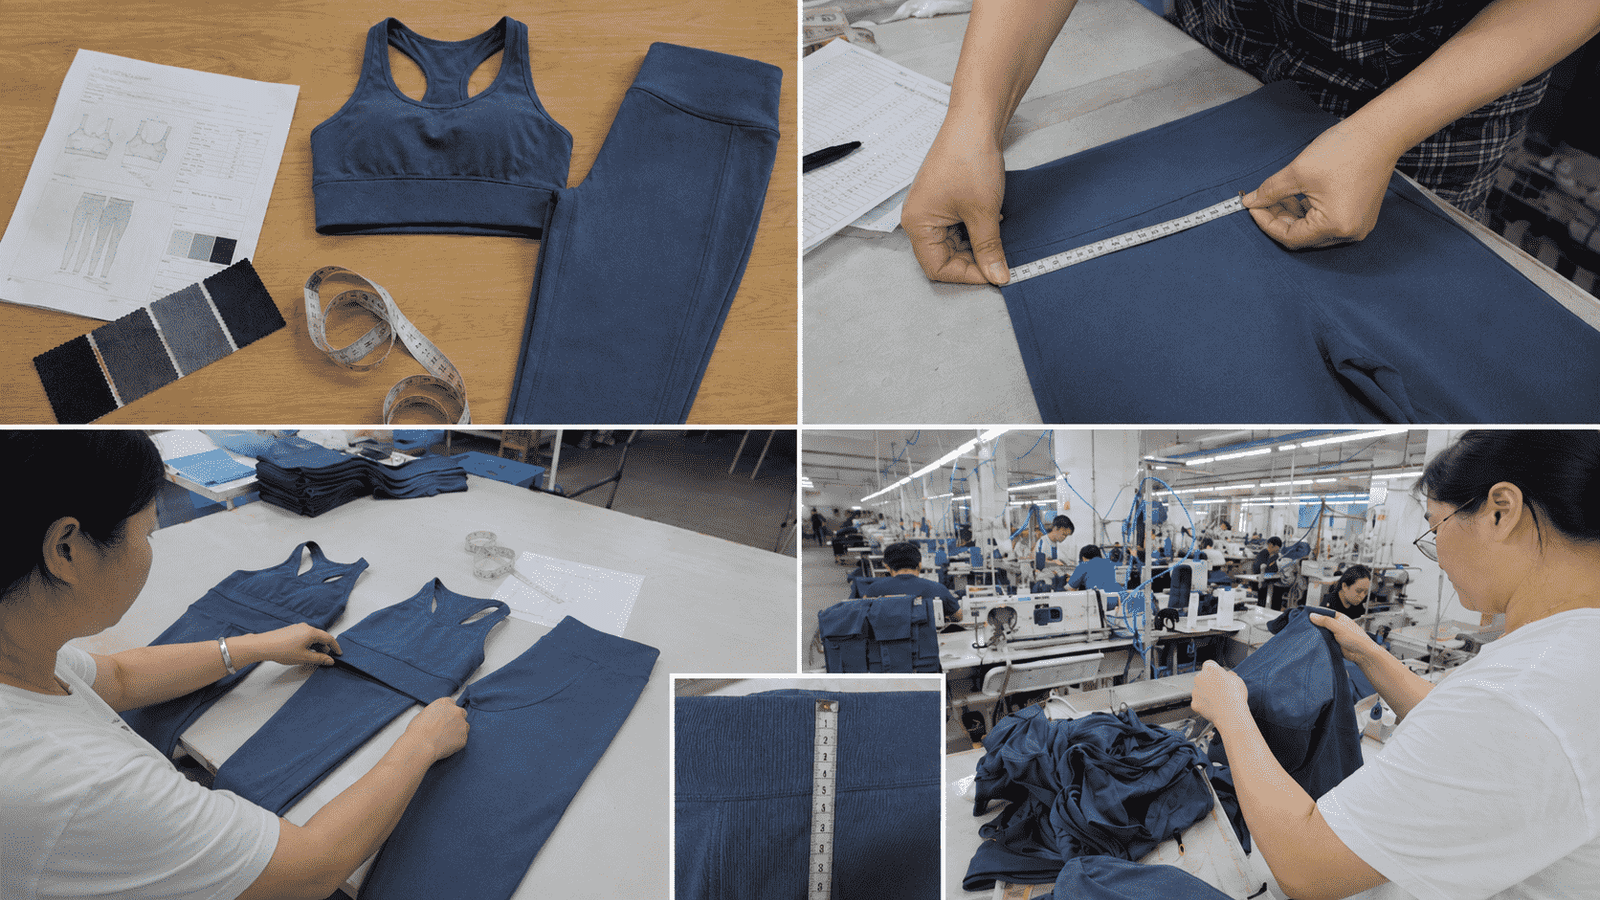
MOVEVOX should carry the Approved Sample, current technical files, materials, pattern or program, First Article and inspection points into one production standard. Same-project Approved Sample versus bulk evidence would provide the strongest visual proof of consistency. If same-project Racerback evidence is unavailable: 需要真实素材替换.
Control Racerback Quality From Incoming Material to Packing
Racerback quality should be managed through multiple production gates rather than one final inspection. Each checkpoint protects a different part of the released product standard.
Material Identity
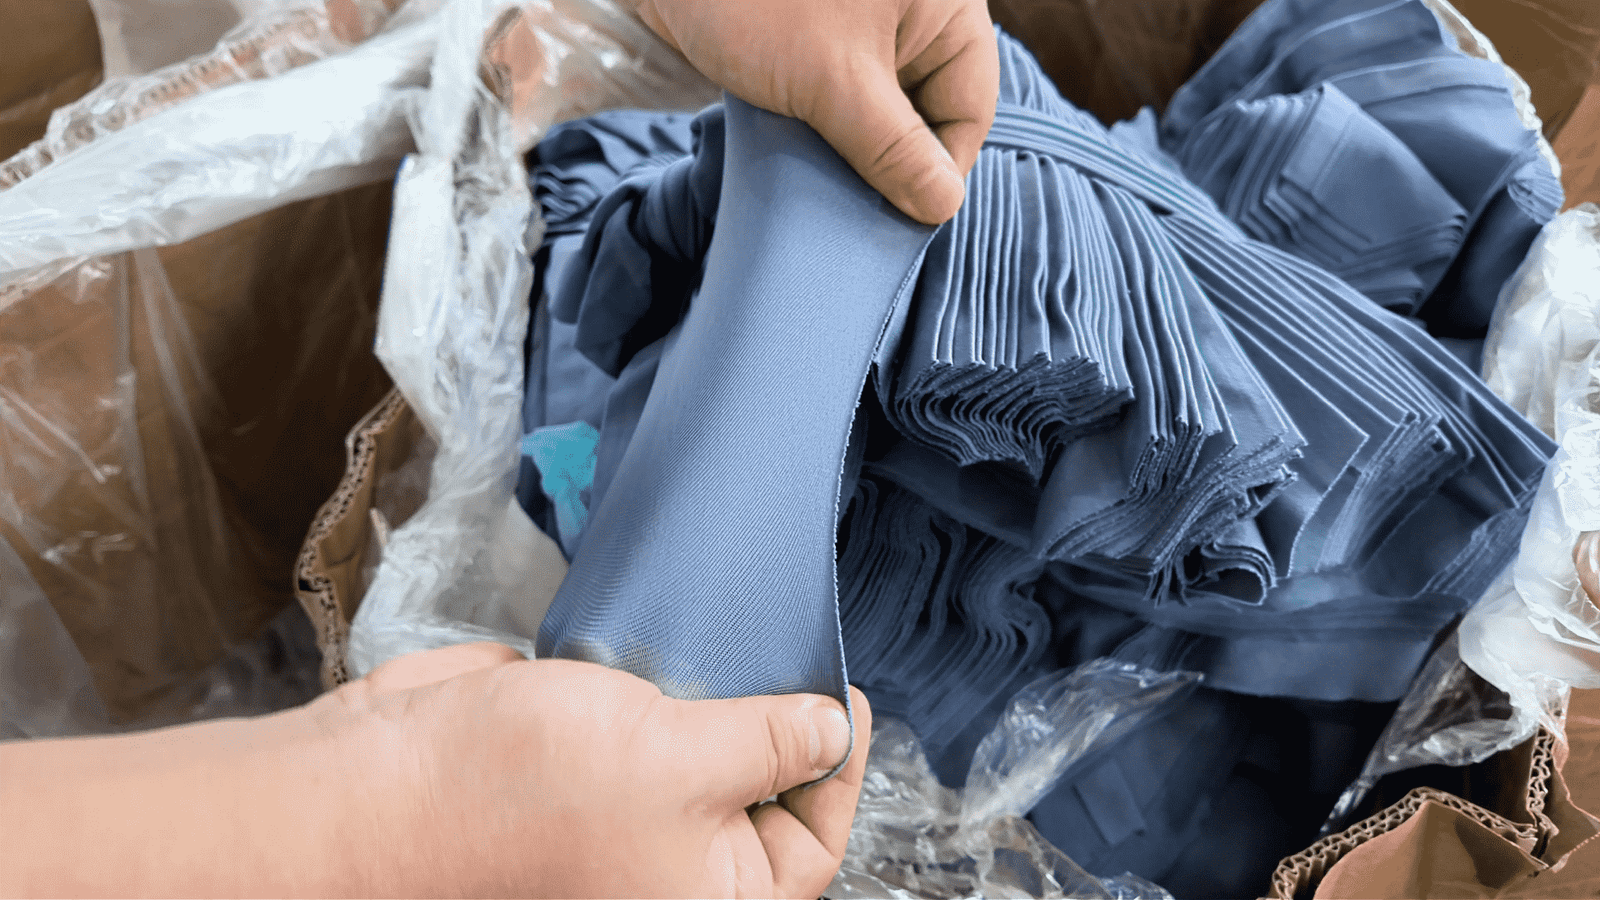
Check that outer fabric, yarn, lining, elastic and relevant trims correspond to the approved project references before normal production use.
- Correct material reference
- Correct color / lot
- Approved project status
Pre-Production Review
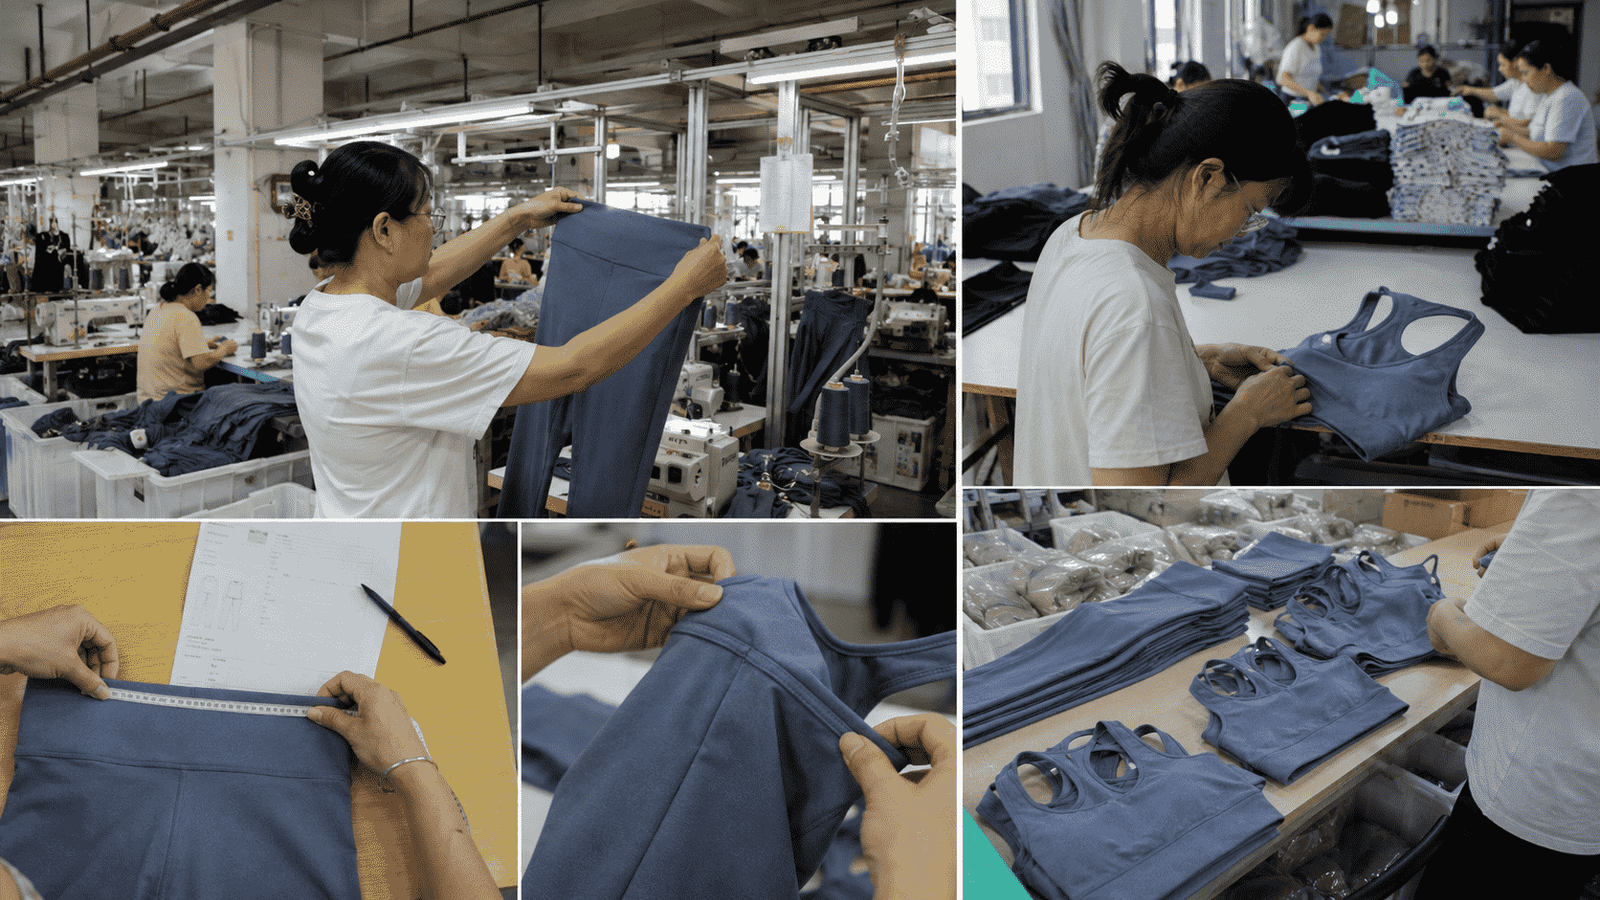
Confirm that current technical documents, patterns or programs, BOM, sample and customer approvals are aligned before volume production begins.
- Current revision
- Approved Sample available
- Open points closed
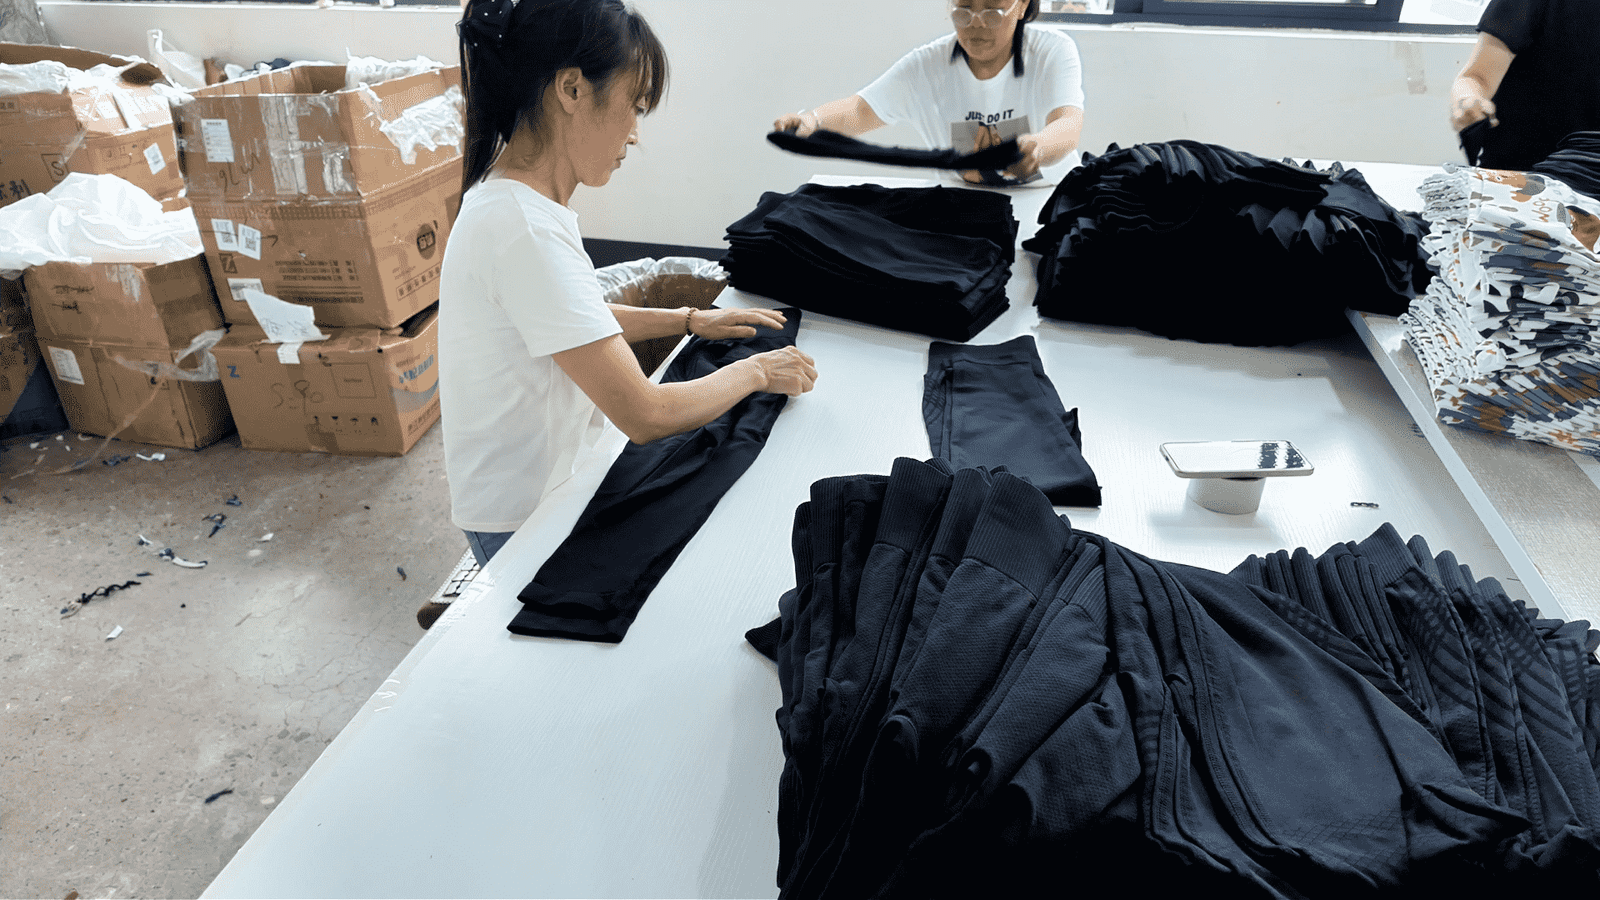
First Article
Compare the first completed production garment against the released Racerback standard before the main run continues.
- Relevant measurements
- Strap and back alignment
- Approved workmanship
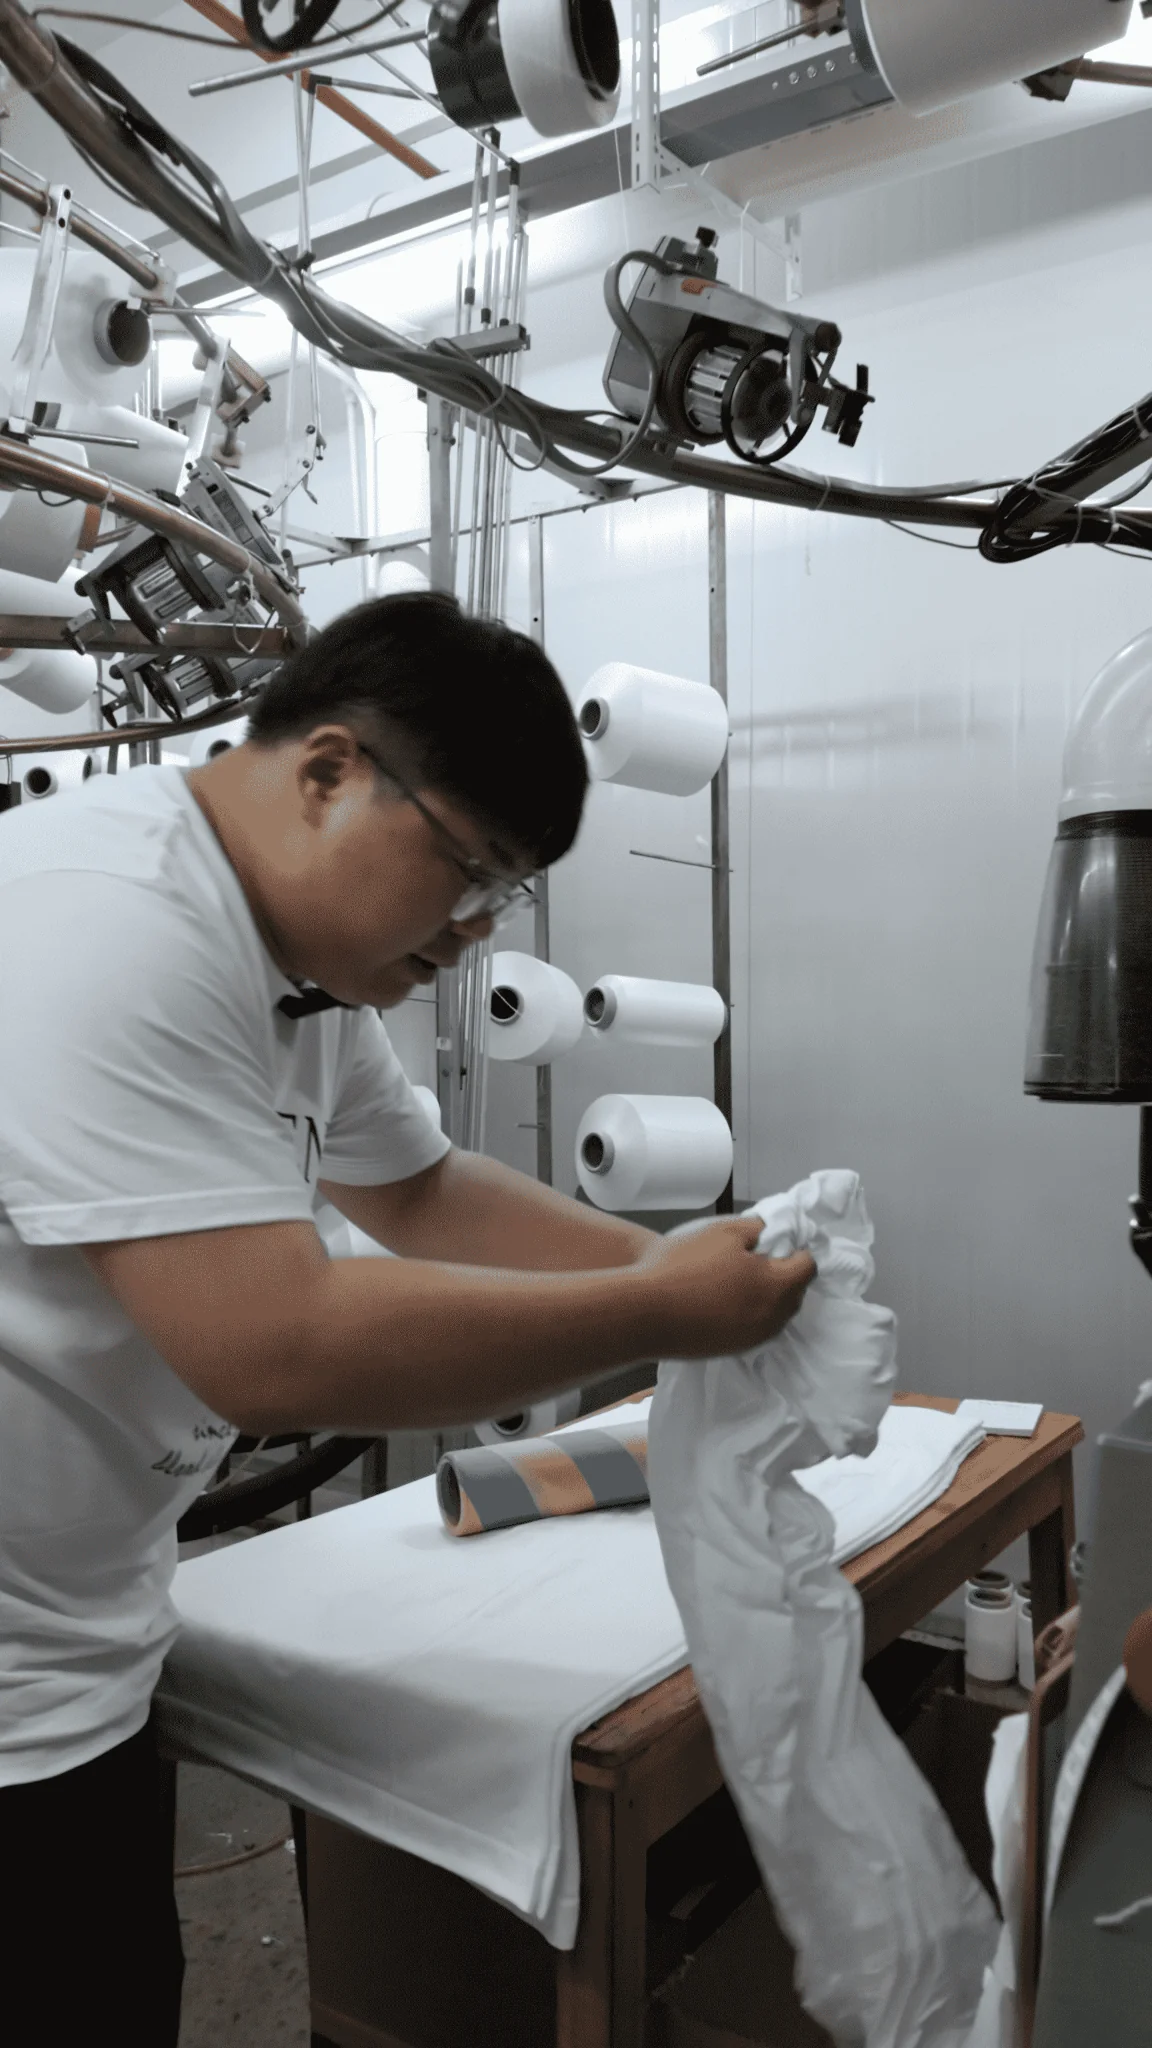
Inline Inspection
Inspect the order while production is still active so recurring Racerback or sewing problems can be identified before they affect a larger quantity.
- Strap symmetry
- Back convergence
- Stitching condition
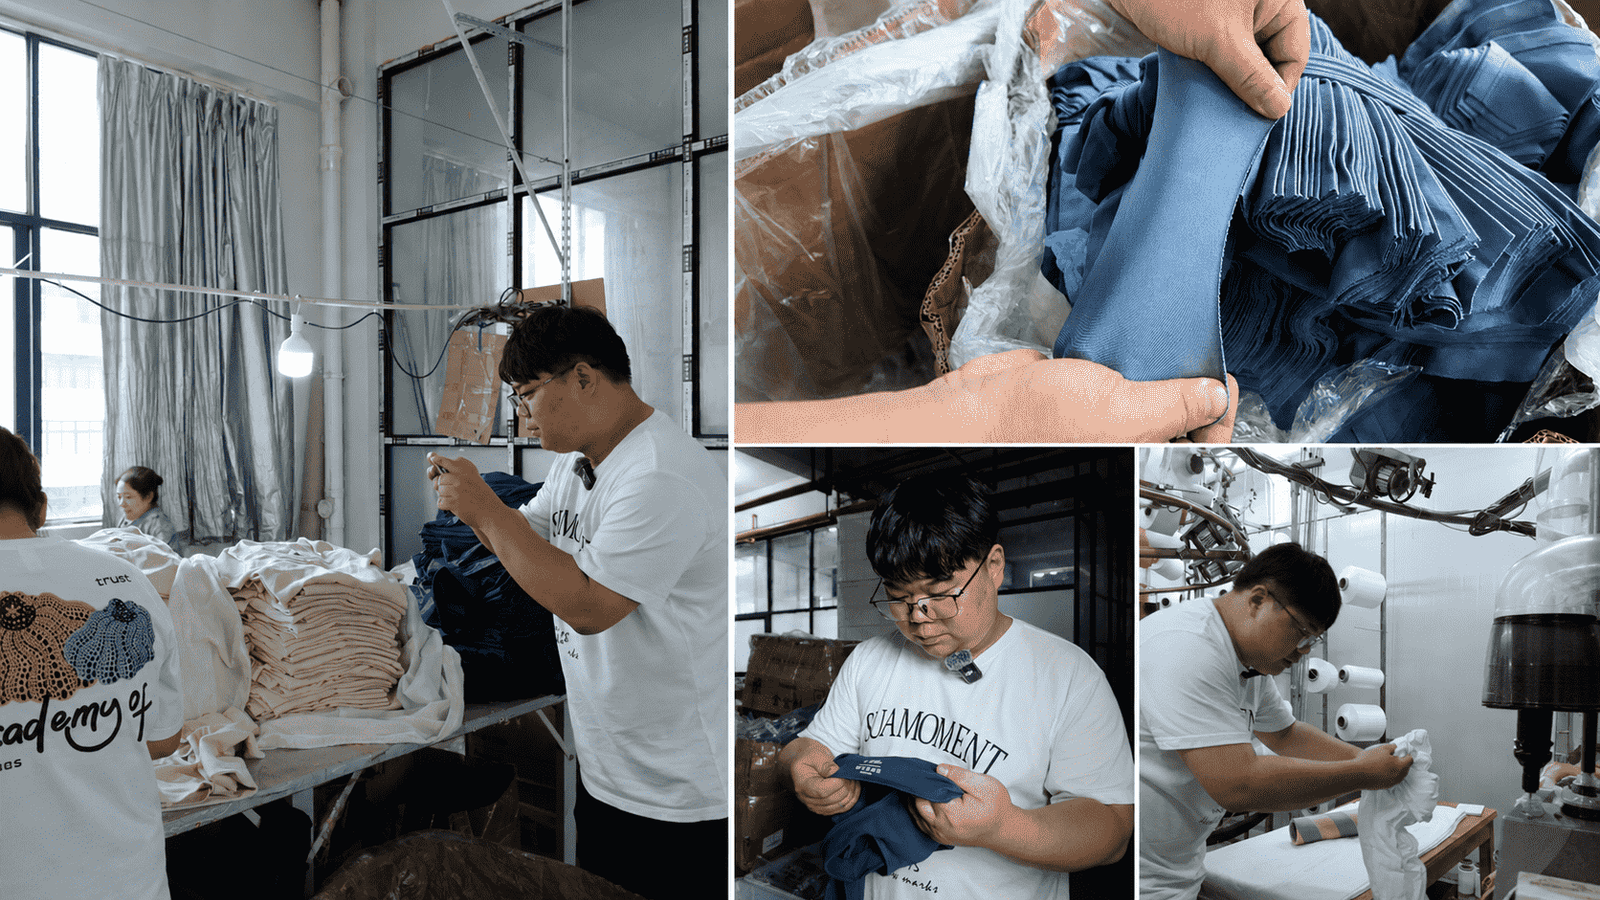
Measurement Check
Verify buyer-defined POMs and tolerances for applicable sizes, including Racerback-related dimensions where they are controlled technical points.
- Underband
- Strap dimensions
- Back / armhole POM
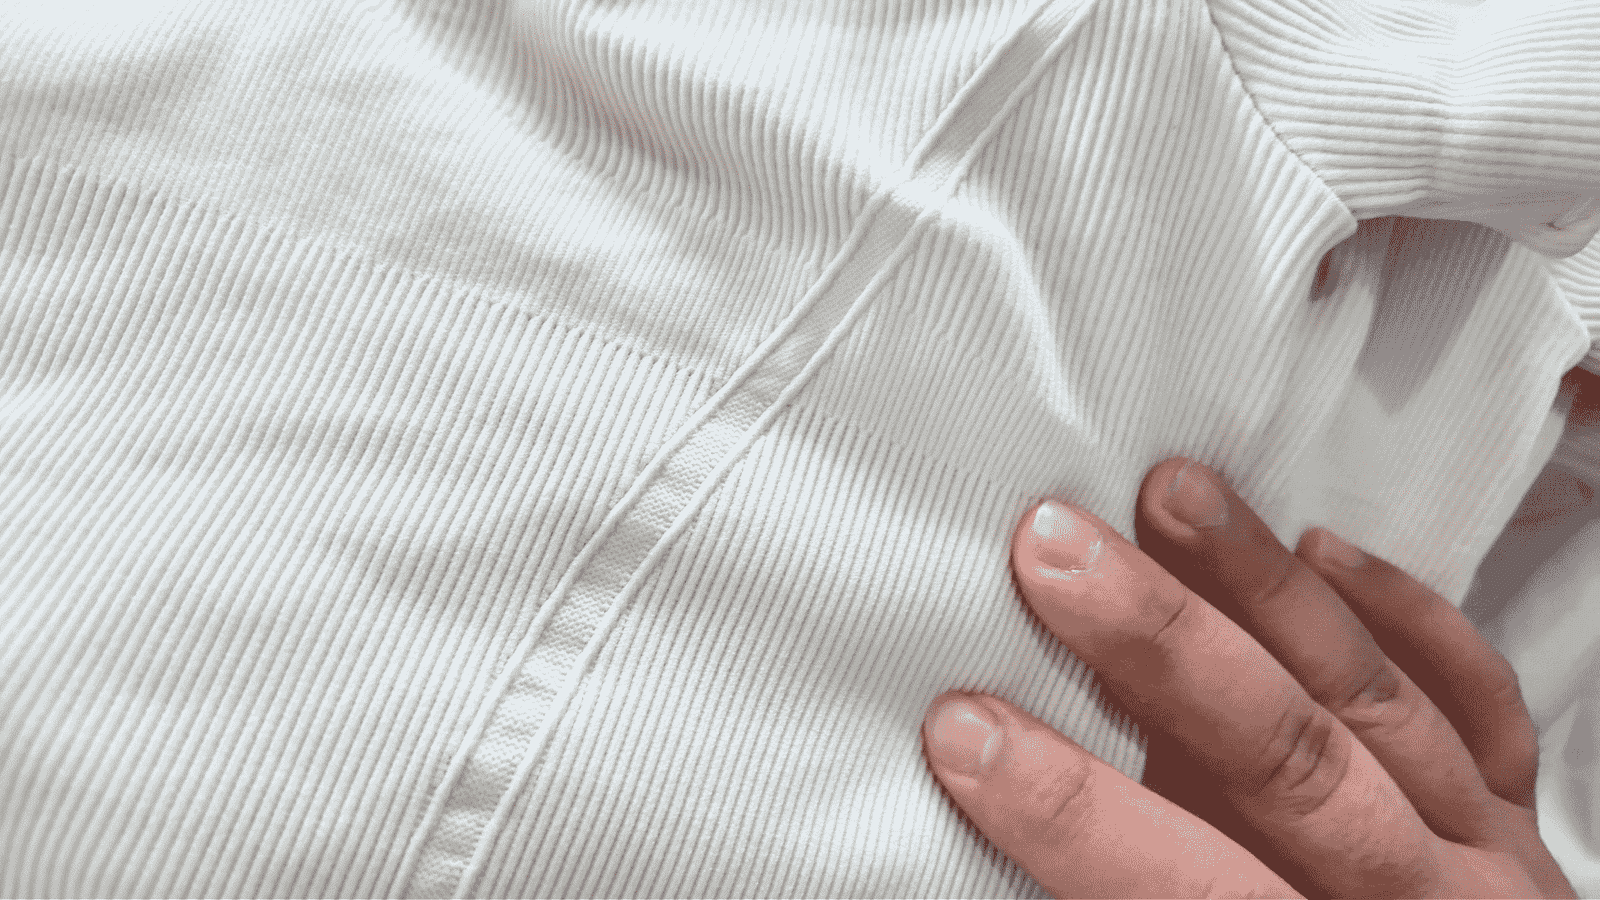
Workmanship Check
Review sewing, joining, binding, reinforcement, knitted structure and internal construction against the approved physical product.
- No uncontrolled twisting
- Left-right consistency
- Approved seam construction
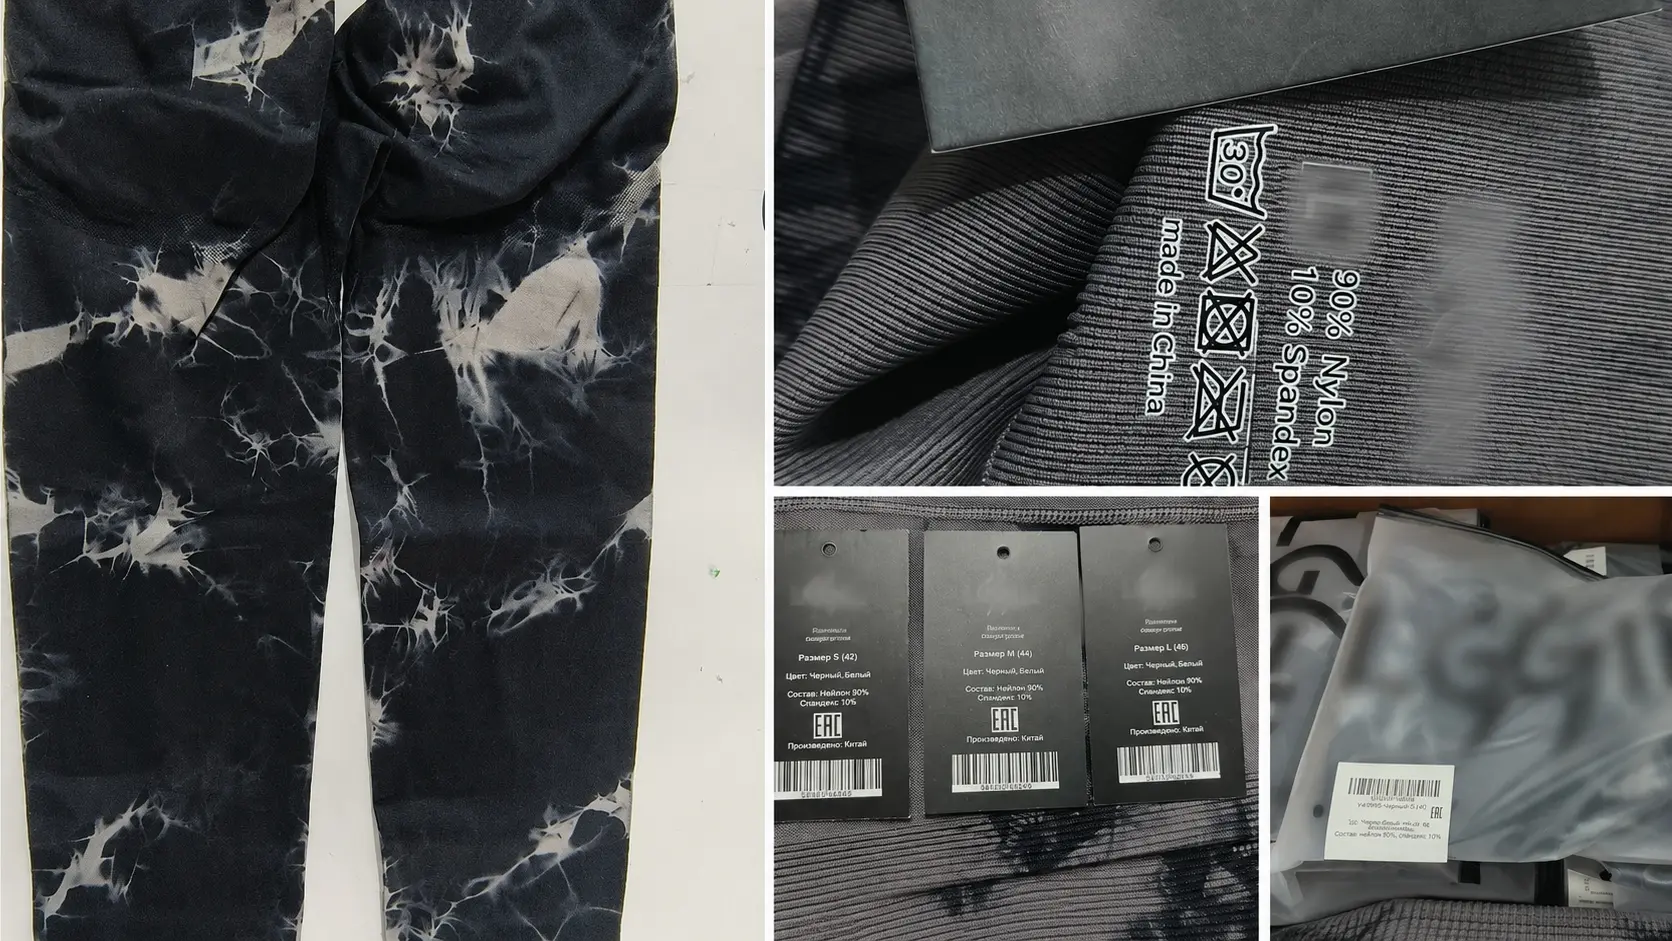
Finished Garment
Review the complete Sports Bra for visible alignment, material appearance, internal components, branding and overall finished condition.
- Approved appearance
- Correct components
- Product identity
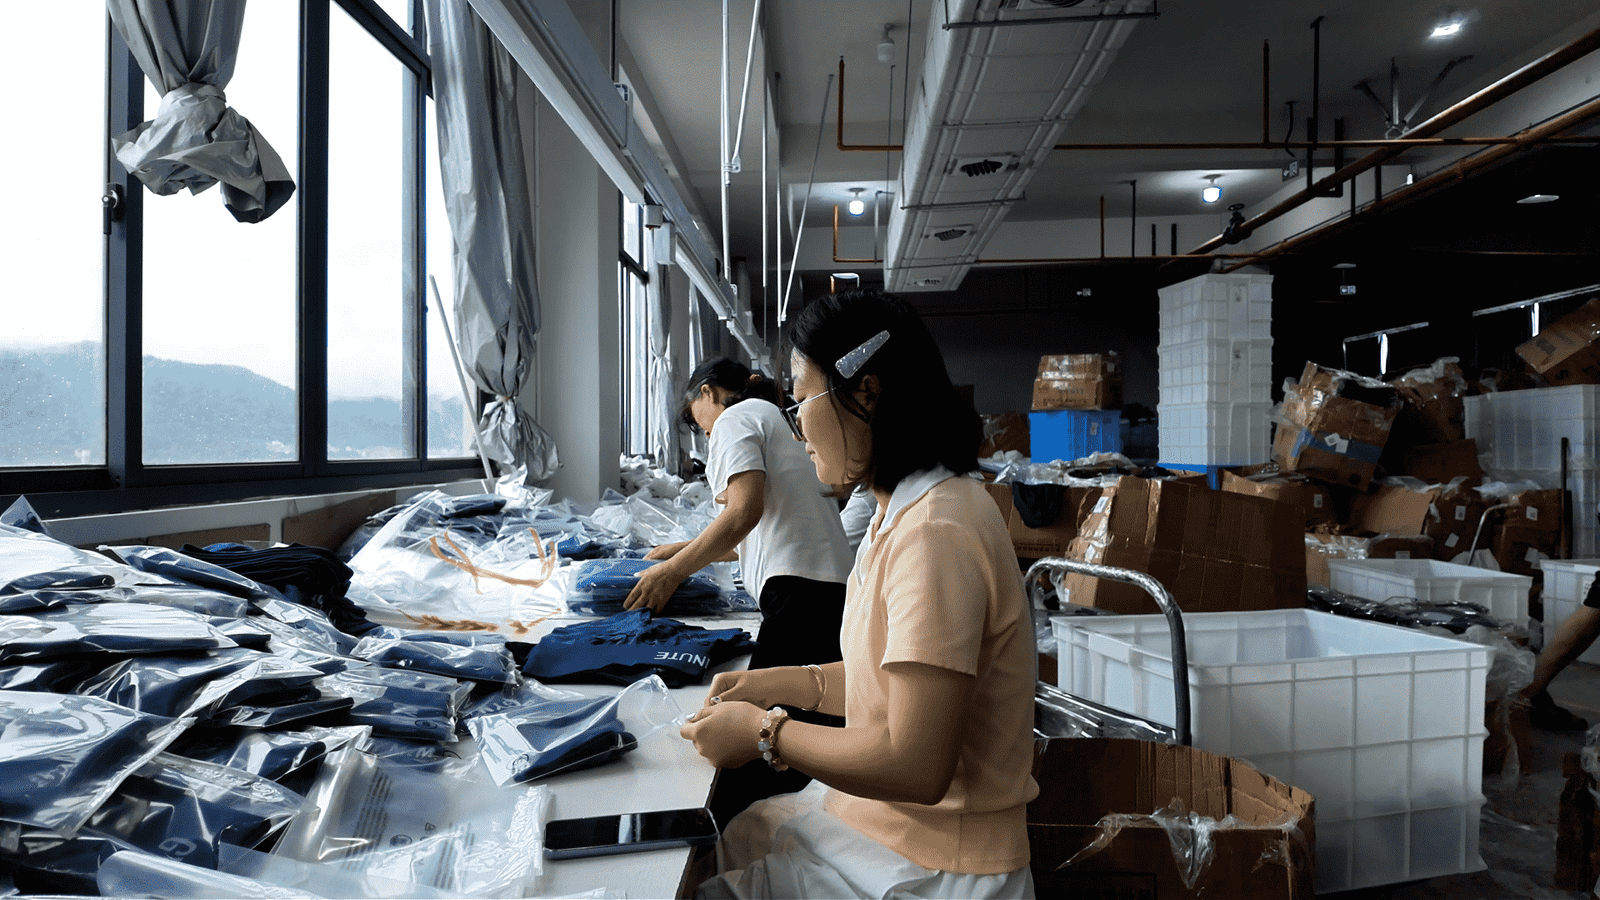
Packing Control
Connect the correct style, color, size, barcode and buyer-defined packaging before carton release.
- Correct SKU
- Correct label / barcode
- Approved packaging
Read Racerback Geometry Inside a Measurement Report
A measurement report should connect Racerback Fit to the exact PO, style, size, tolerance and inspection stage rather than showing isolated numbers without production context.
Product Identity
The report should identify the relevant PO, style, color, size and production stage so the inspected Racerback can be linked back to its commercial order.
Sample Quantity
The record should state how many garments were measured according to the applicable buyer or factory inspection procedure. MOVEVOX should not invent one universal sampling quantity.
Underband
The finished underband provides a critical lower garment reference. Variation can change the total position of the racerback even when upper-back measurements appear correct.
Strap Length
Effective strap length can be checked against the applicable technical method and size so the approved front-to-back relationship is maintained.
Racerback Width
Where specified as a POM, racerback width helps show whether the back body remains proportionate to the intended design across production.
Back Junction
A defined center-back or convergence reference can support alignment review when the buyer treats its location as a controlled technical point.
Armhole
Armhole measurement or curve reference should remain connected to the applicable size because movement and side coverage depend on the surrounding geometry.
Release Decision
Measurement results should be reviewed with workmanship, material, branding and other applicable requirements before commercial goods are released.
Report Use
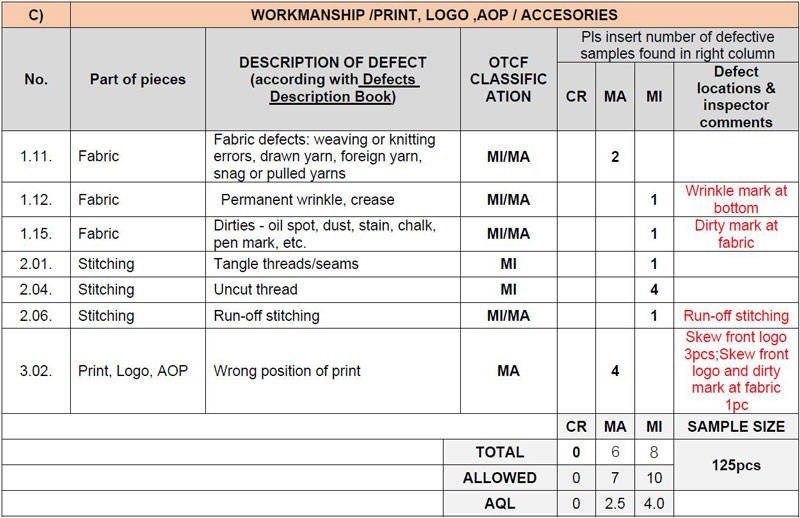
A report only has procurement value when it is tied to the actual buyer-approved specification, current product version and inspected production. Current Racerback-specific anonymized measurement-report example: 需要真实素材替换.
Prevent Common Racerback Workmanship Defects in Bulk
Racerback construction contains highly visible alignment and joining points. Production inspection should connect each defect to its likely cause, prevention method and corrective action.
| Defect | Likely Cause | Prevention | Inspection Point | Corrective Action |
|---|---|---|---|---|
| Uneven Straps | Cutting, sewing, elastic or assembly variation changes left-right finished dimensions. | Use current pattern, construction and measurement reference. | First Article / Inline | Hold affected units and correct the responsible process. |
| Off-Center Racerback | Back junction or strap assembly is not aligned to the center reference. | Define symmetry and center-back control in approval. | Inline / Finished | Rework suitable units and reinforce alignment method. |
| Asymmetric Armholes | Panel, binding, seam or joining variation changes one side differently from the other. | Check cutting identity and assembly method. | First Article / Inline | Correct operation and reinspect affected quantity. |
| Back Twist | Panels, lining, elastic or seam tension create rotational distortion. | Control material direction, joining and tension. | Finished Garment | Identify root cause before shipment release. |
| Edge Waviness | Binding or seam tension does not match fabric stretch. | Approve edge method in actual material. | Inline | Adjust process and re-evaluate affected work. |
| Skipped Stitch | Needle, thread, tension or machine setup is unsuitable or inconsistent. | Use approved sewing setup and operator checks. | Inline | Repair where acceptable and correct machine setup. |
| Reinforcement Variation | Bartack or local strengthening is placed or executed inconsistently. | Define location and workmanship before bulk. | Inline / Final | Rework and reinforce instruction. |
| Neckline Distortion | Strap tension, binding or body assembly pulls the front geometry away from the approved Fit. | Review the complete front-to-back relationship in First Article. | First Article / Fit | Hold and identify the relevant construction cause. |
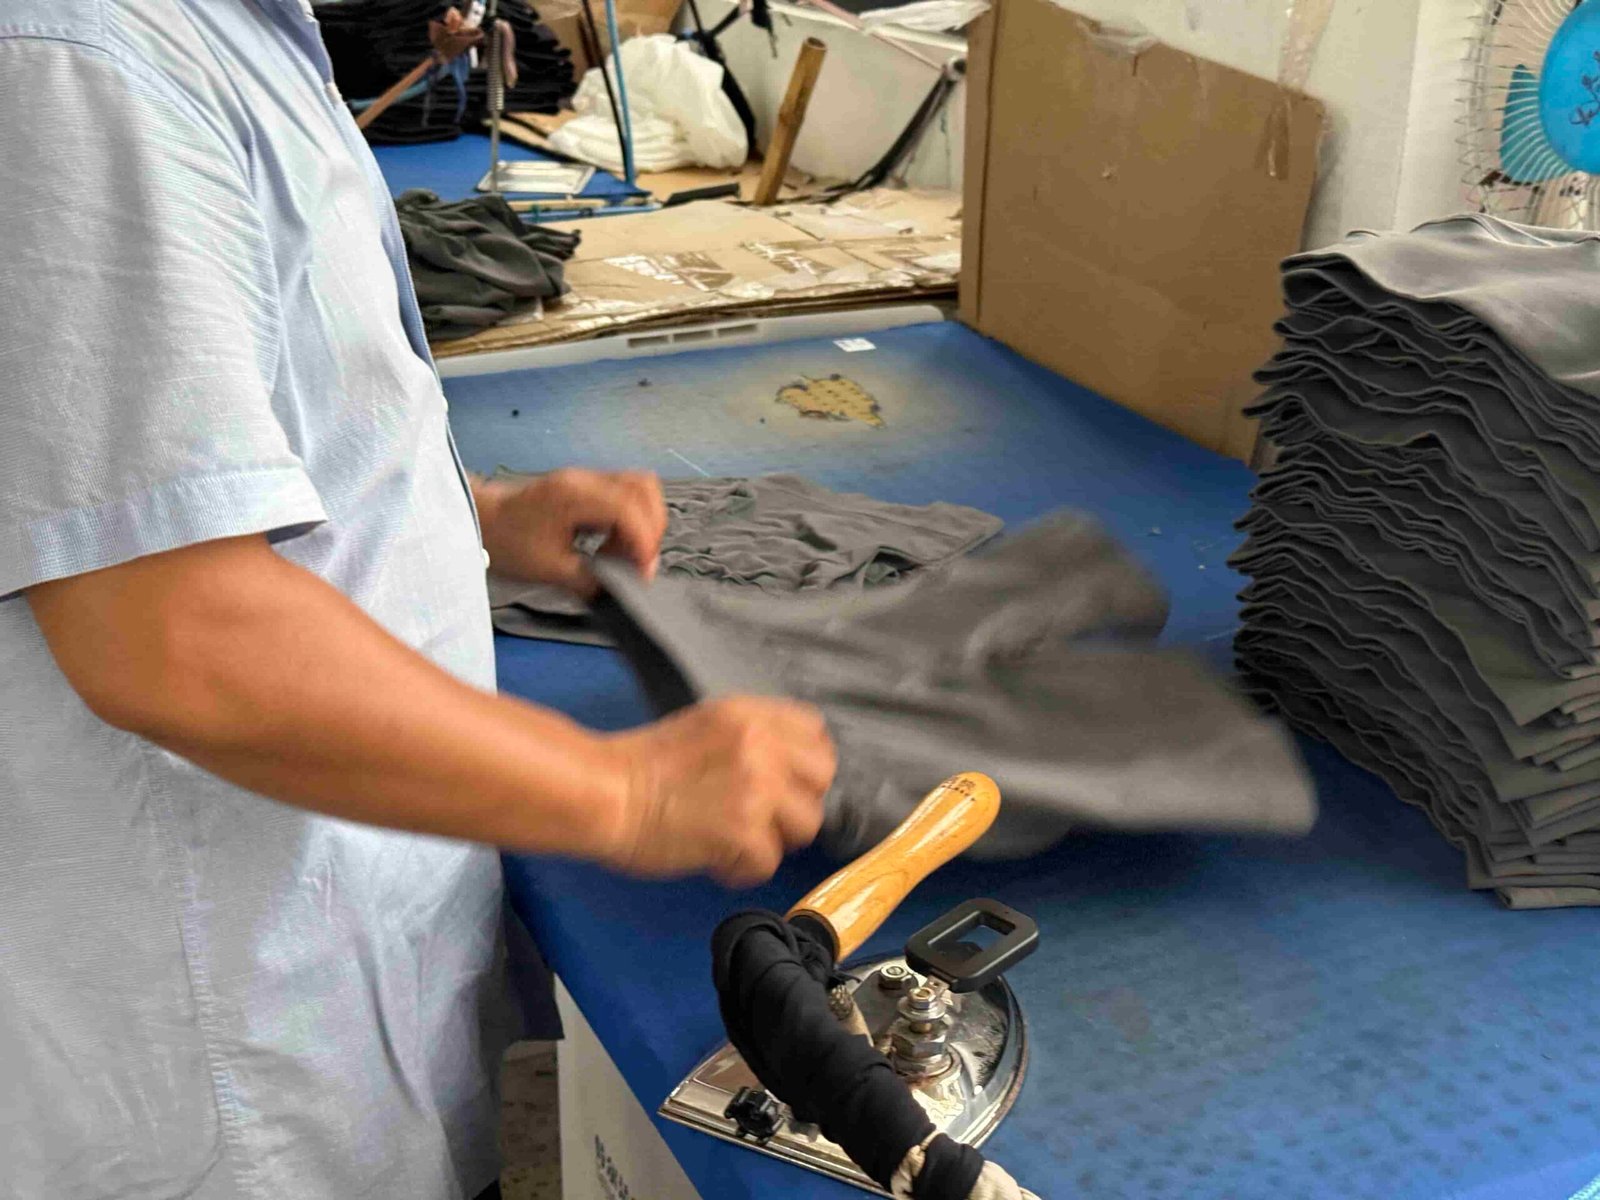

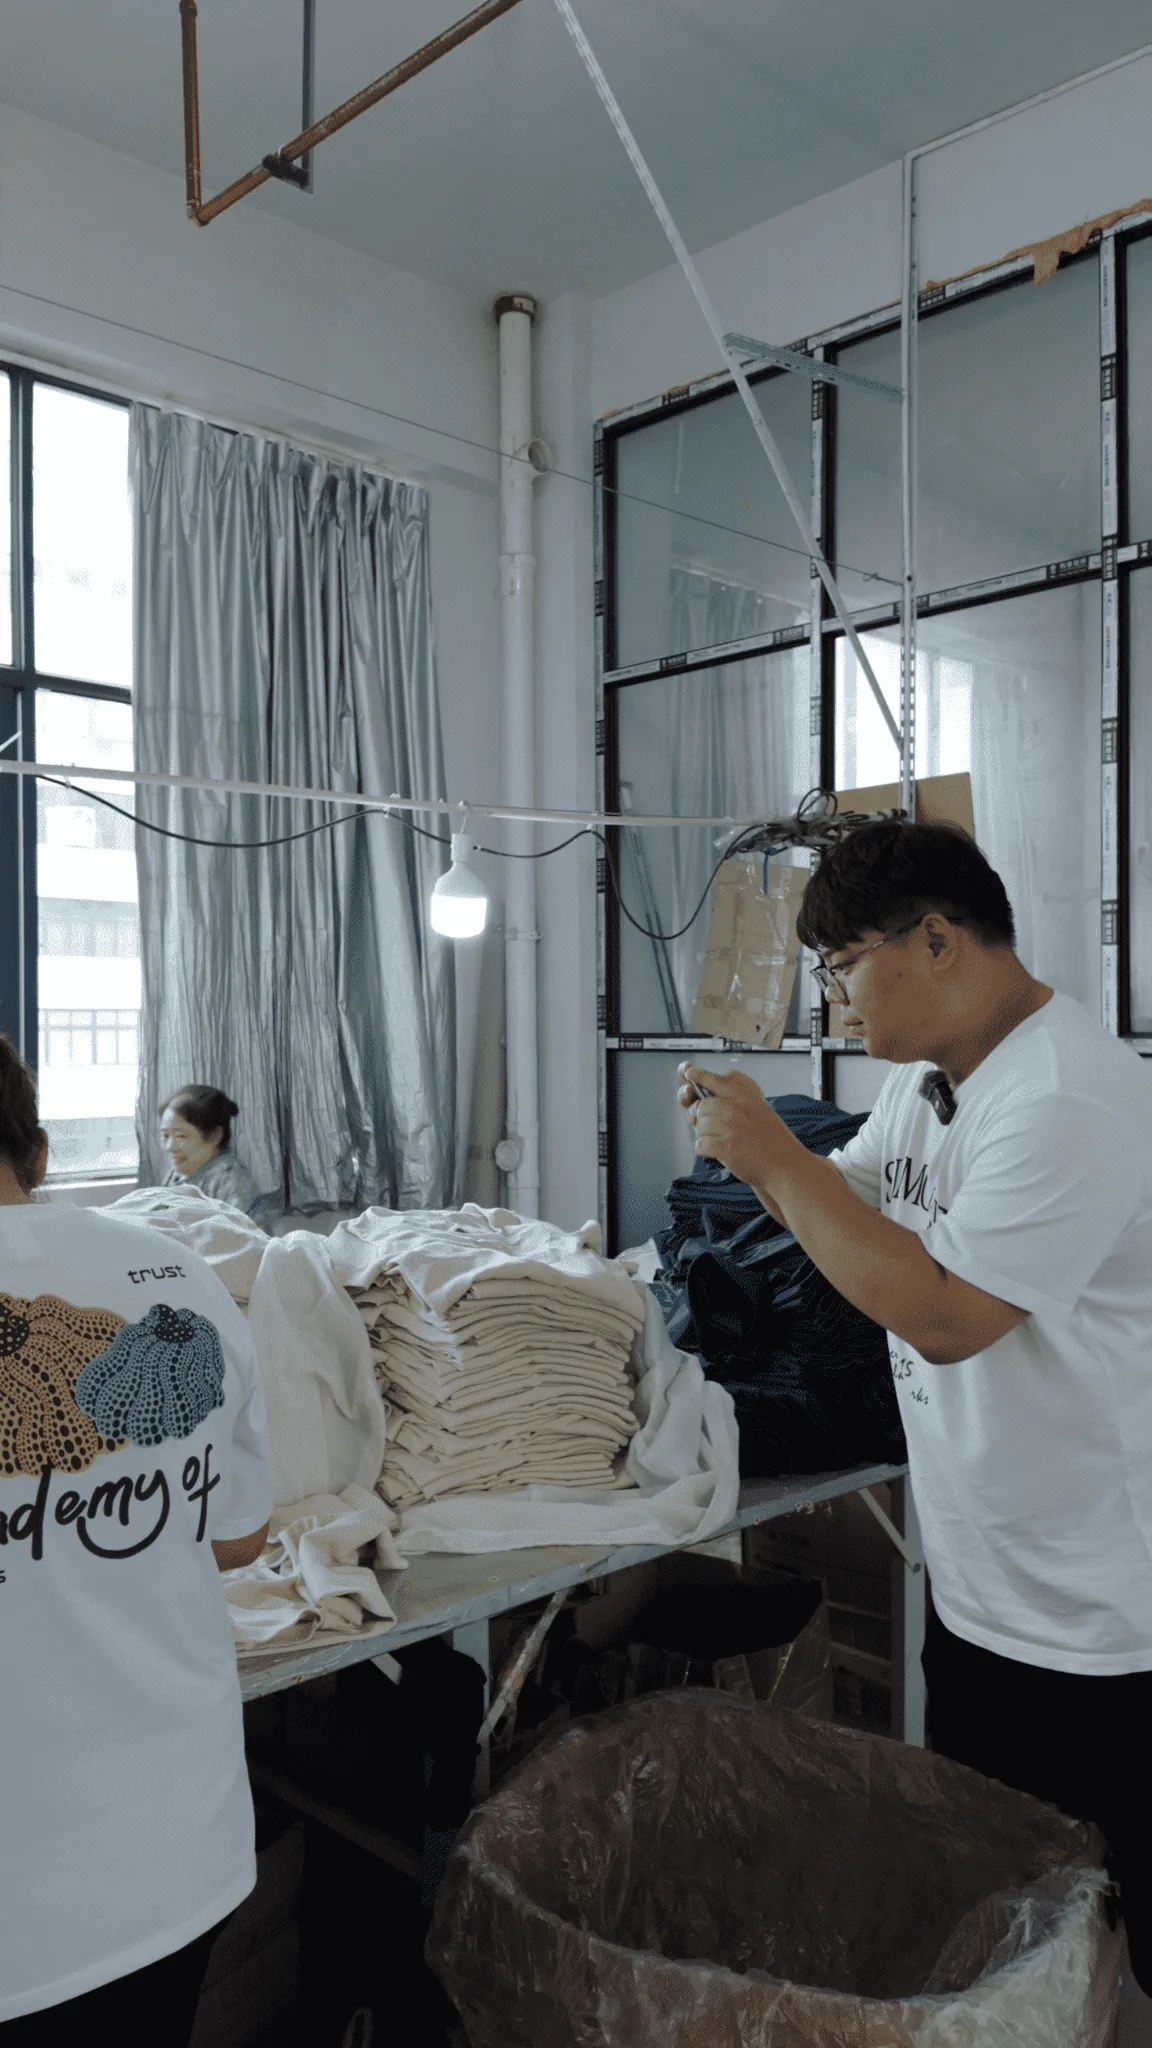
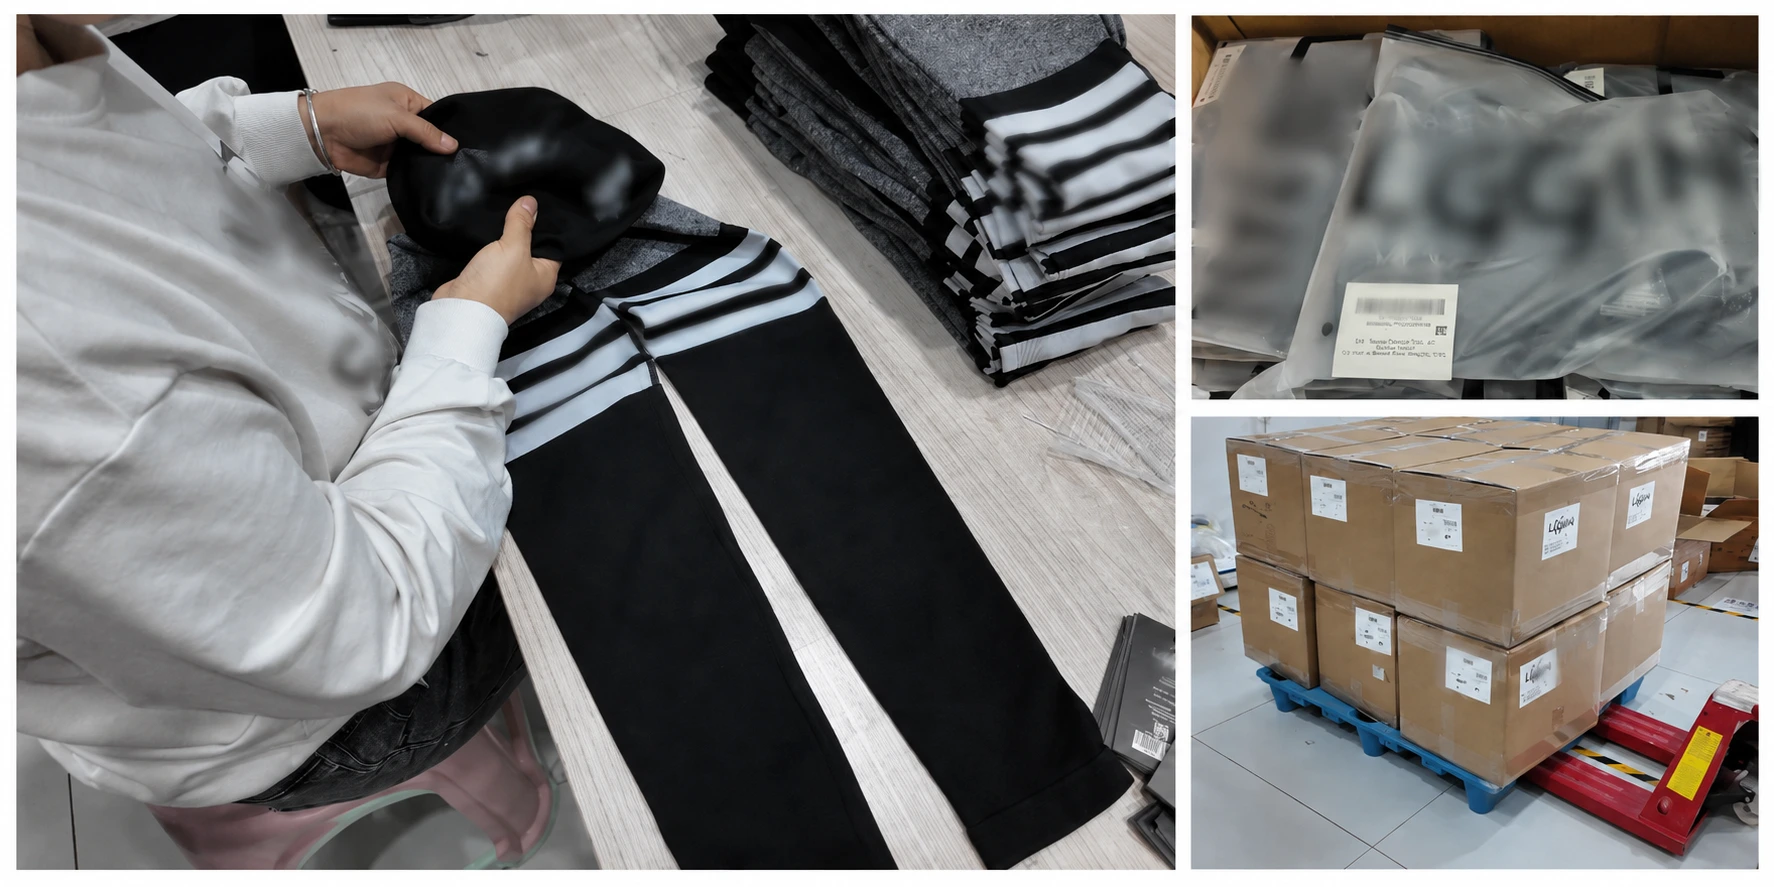
Scale Approved Racerback Programs Through Managed Capacity
MOVEVOX reviews capacity against the actual style, materials, SKU structure and production window. Company-wide capability is useful context, but it does not replace project-specific production planning.
Managed Capacity
Normal combined managed delivery capacity across self-operated and controlled collaborative production, subject to product mix and quality release.
Santoni Machines
Italian Santoni Seamless machines supporting technically suitable Racerback and wider Seamless activewear programs.
Garment Machines
Principal sewing and garment-production machines supporting the self-operated Cut & Sew manufacturing system.
Satellite Facilities
Eight long-term collaborative facilities provide additional managed production flexibility—six in Yiwu and two in Guangzhou.
QC Personnel
Current core QC personnel supporting incoming, production, finished-garment, packing and shipment-related quality execution.
Bulk Reference
Normal bulk-production reference under ready standard conditions after required materials, approvals and capacity are available.
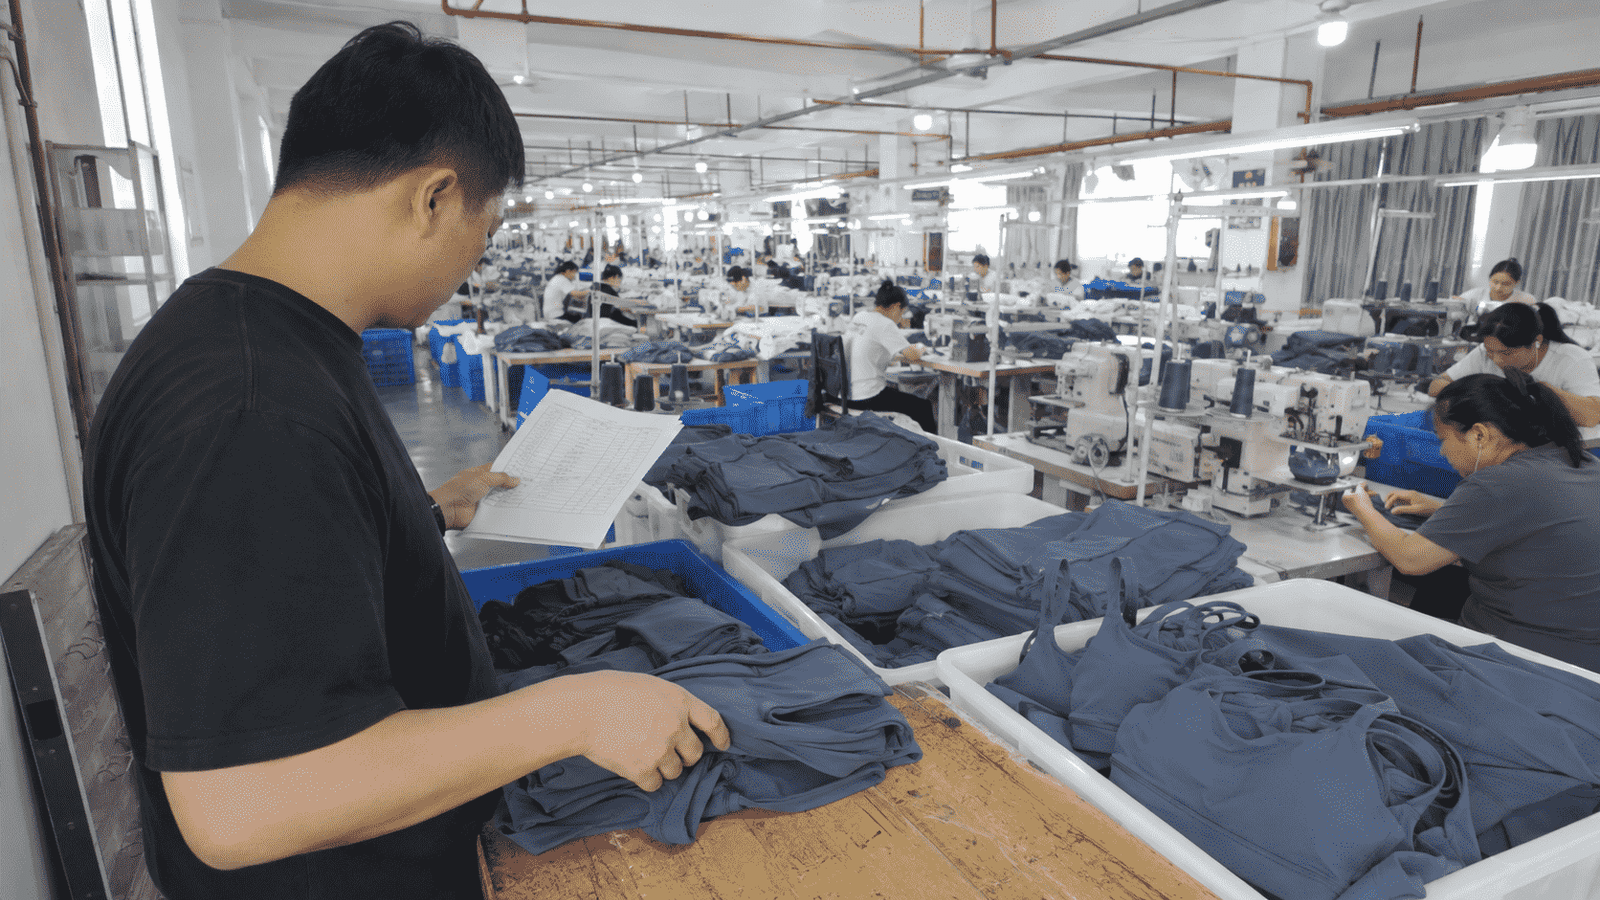

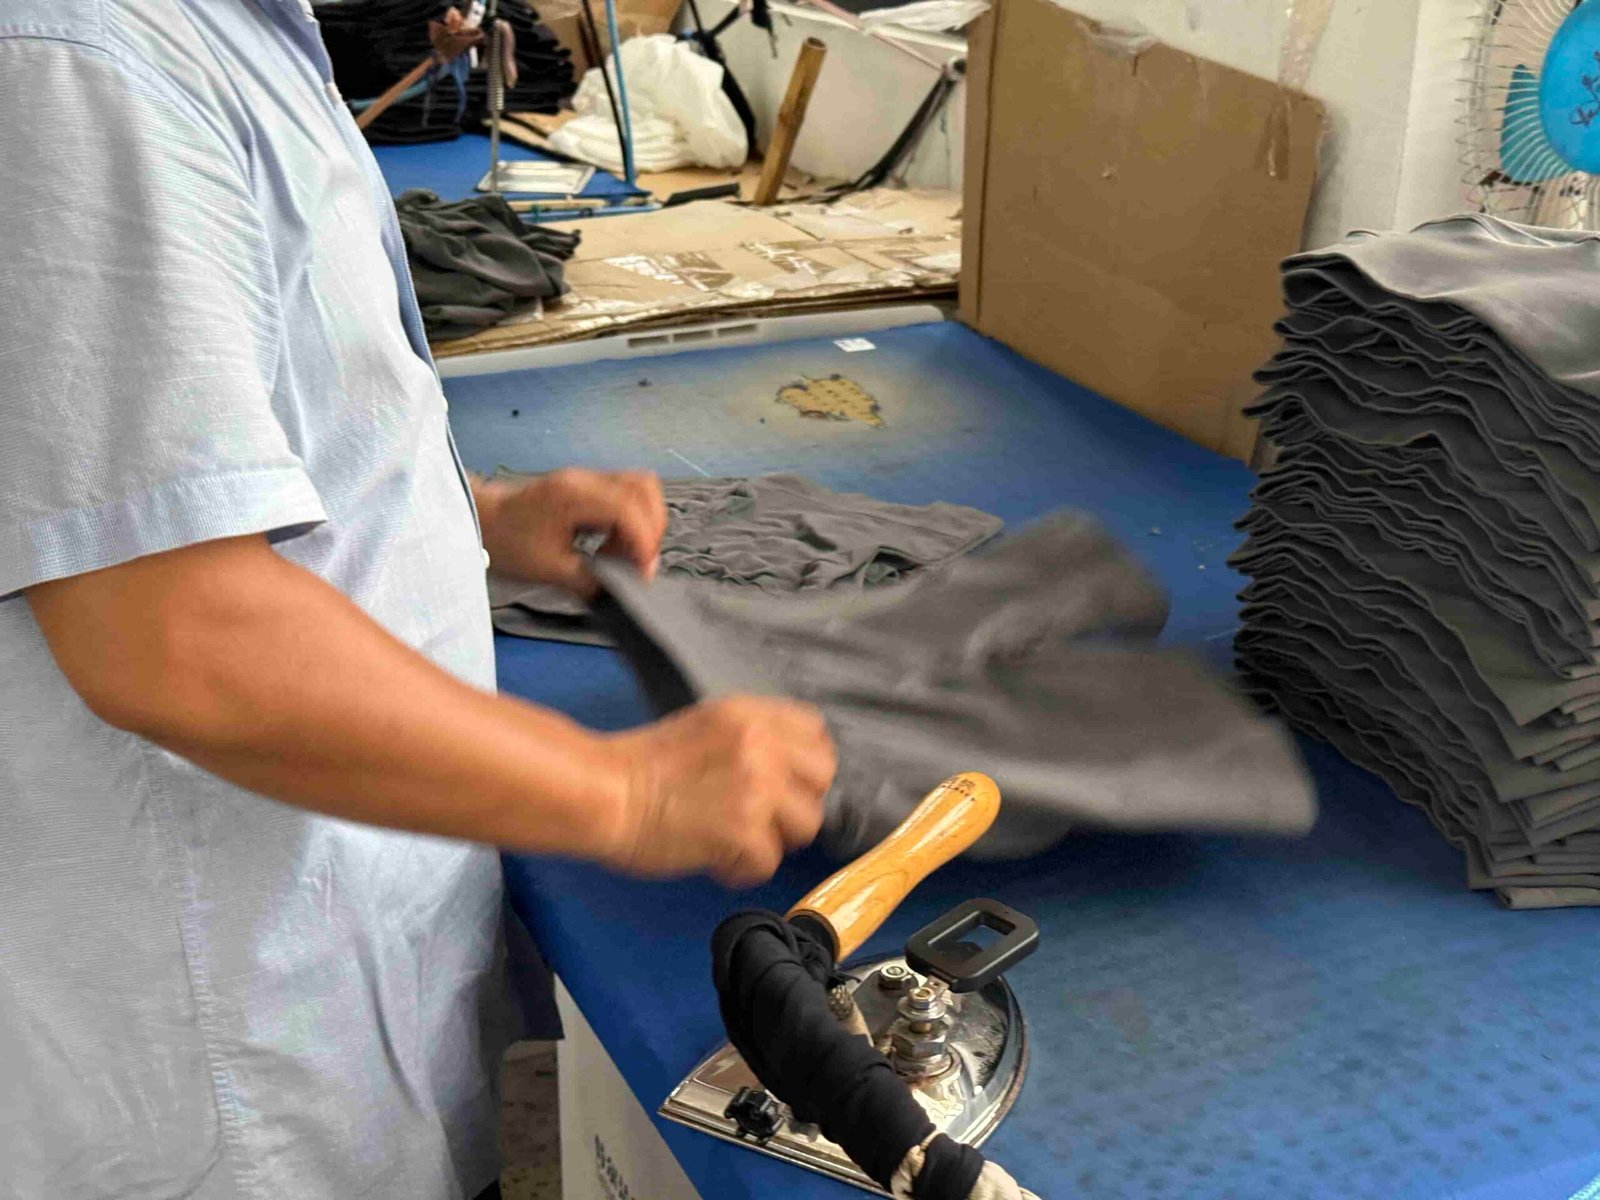
Verify the Manufacturing System Behind Racerback Production
MOVEVOX supports supplier verification through factory, technical and production review. Mature buyers should verify the real manufacturing system rather than relying only on website claims.
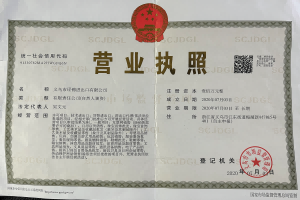
Legal Identity
MOVEVOX is operated by Yiwu Chenjin Import And Export Co., Ltd. Formal vendor review can verify the legal and commercial entity responsible for quotation, contract, payment and project execution. The legal entity was established in 2020, while MOVEVOX records activewear manufacturing and supply-chain activities as beginning in 2019.
Verify the actual contracting entity behind the MOVEVOX brand.
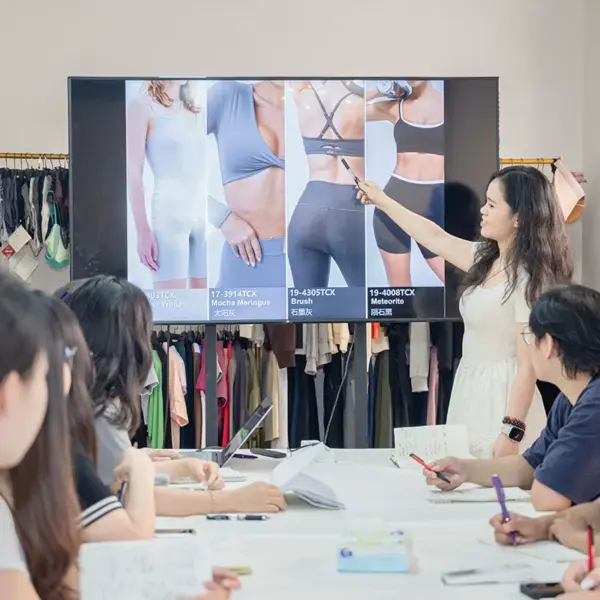
Development Area
The current development organization includes approximately eight people across design, pattern, sample-making and related functions. A technical review can examine how Racerback Tech Packs, references, POMs, Fit comments, sample versions and approvals move through development before bulk.
Racerback development should leave a controlled technical record.
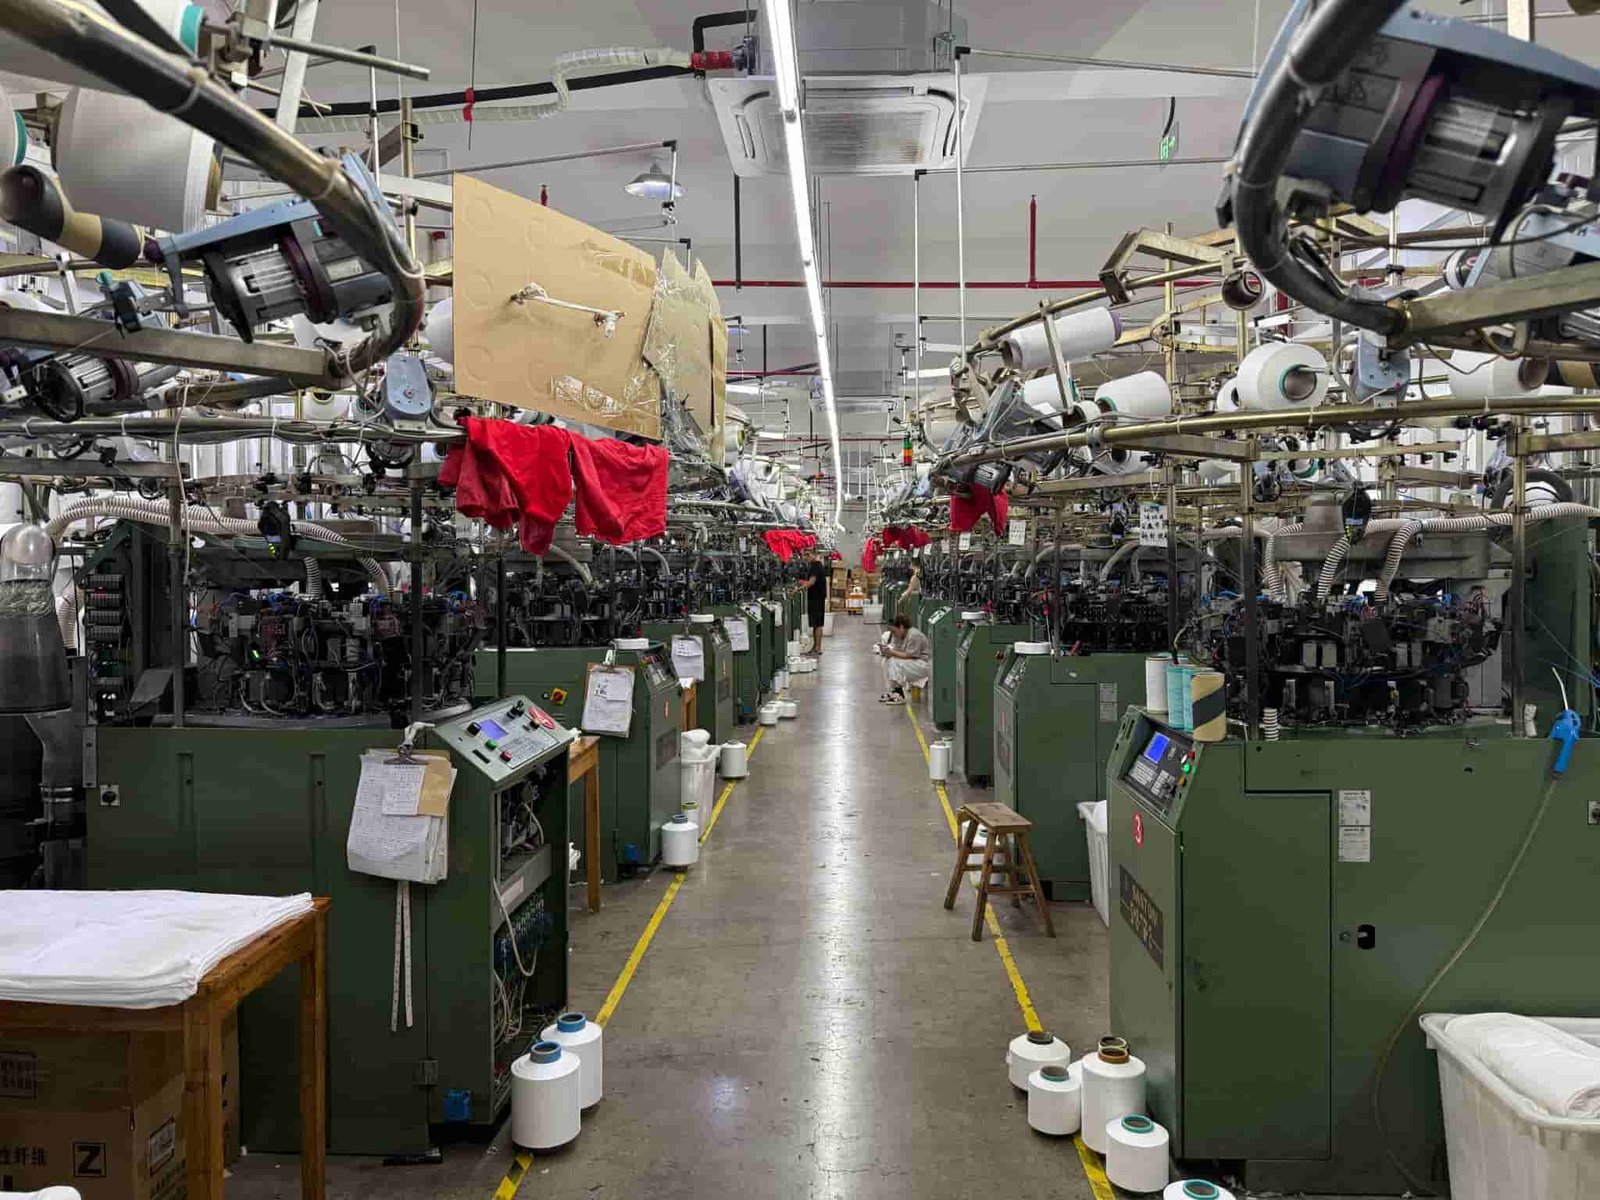
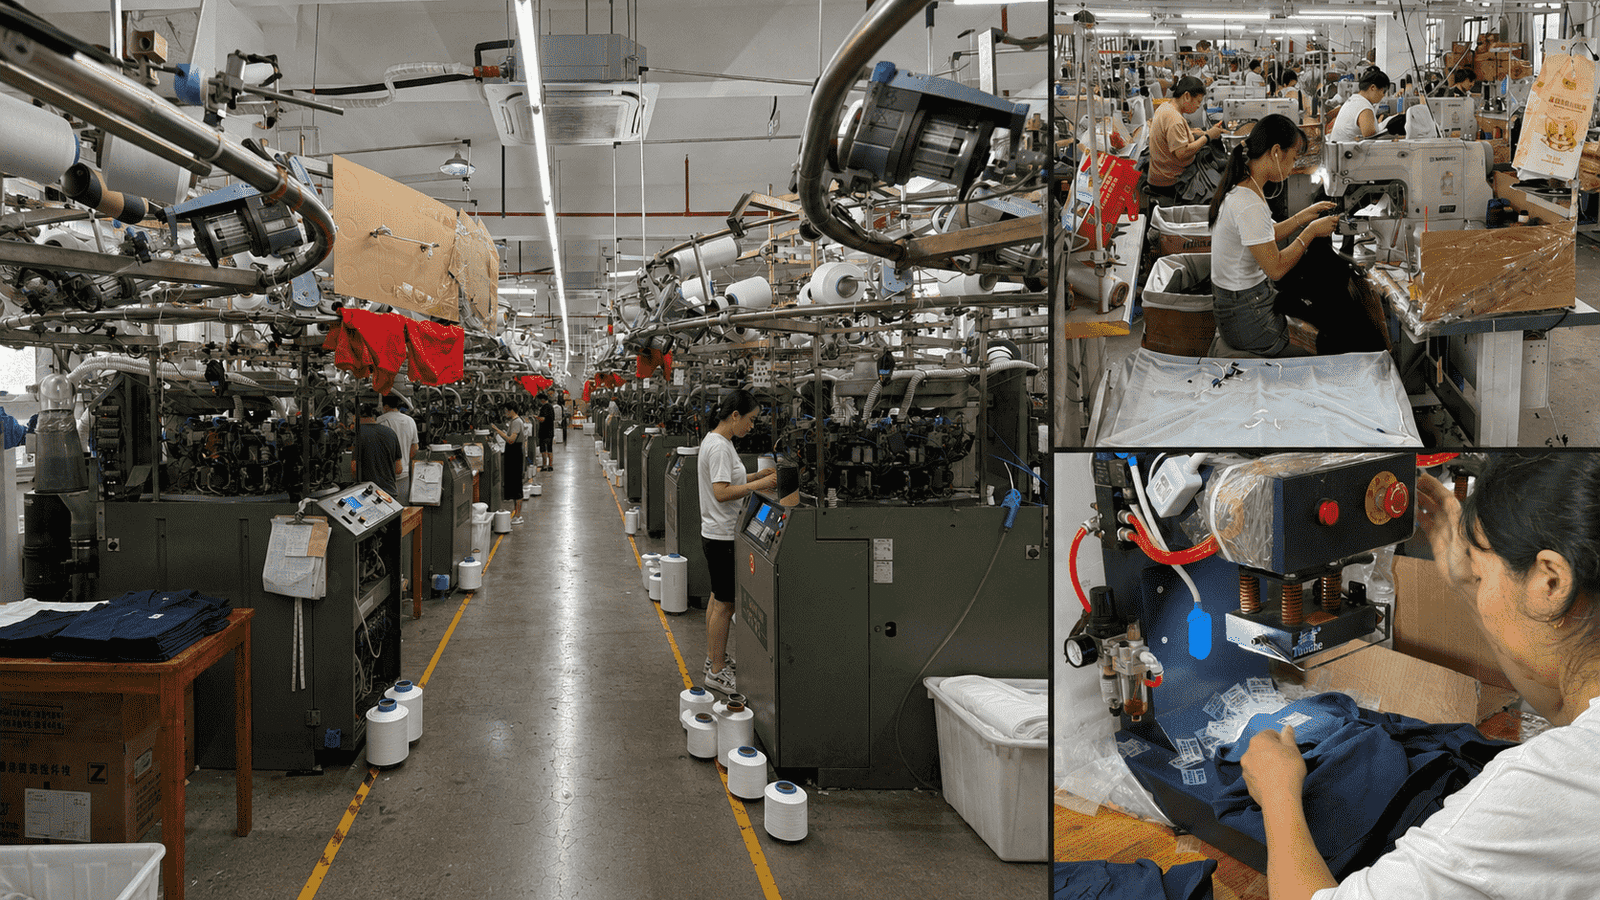
Seamless Area
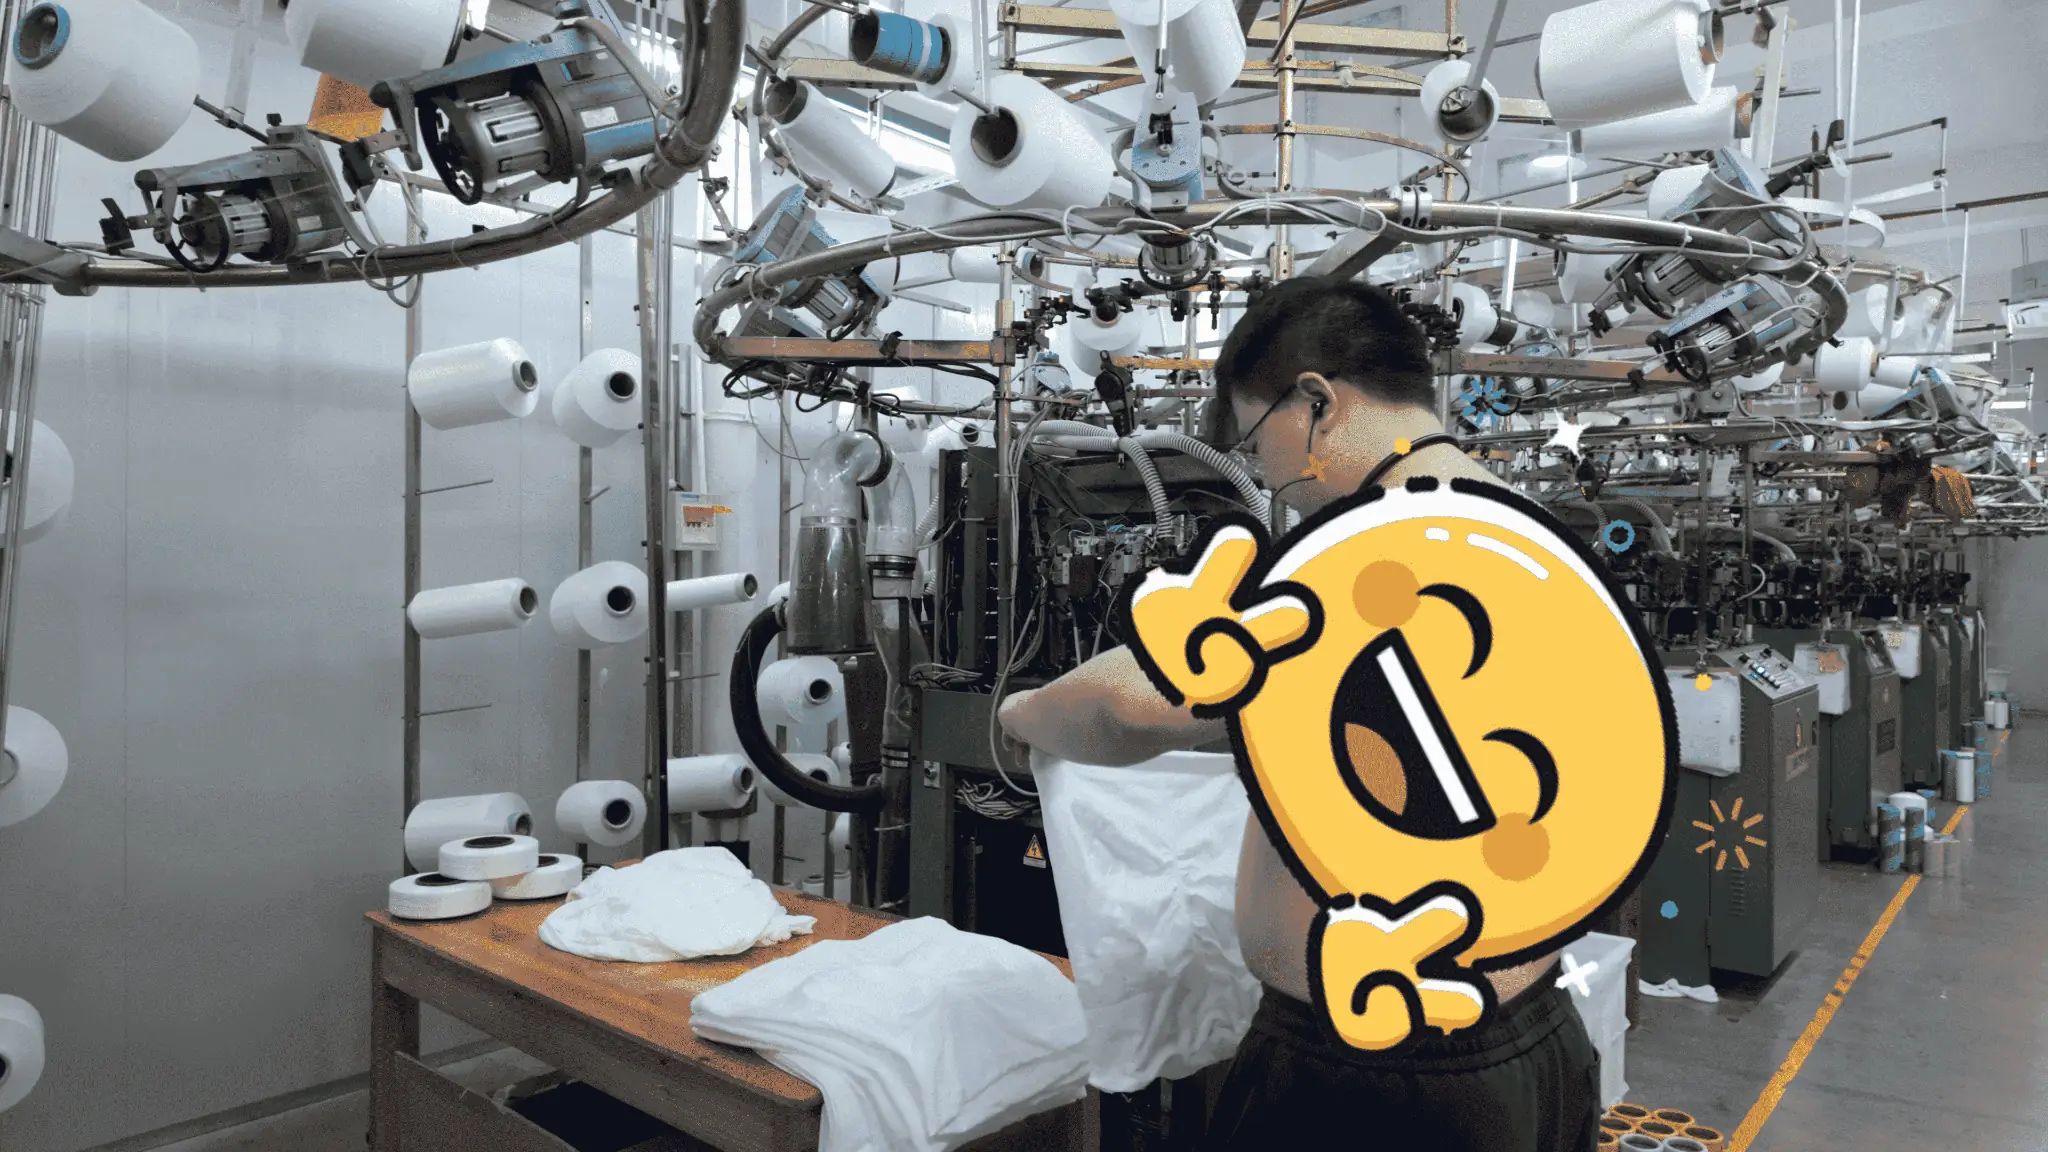
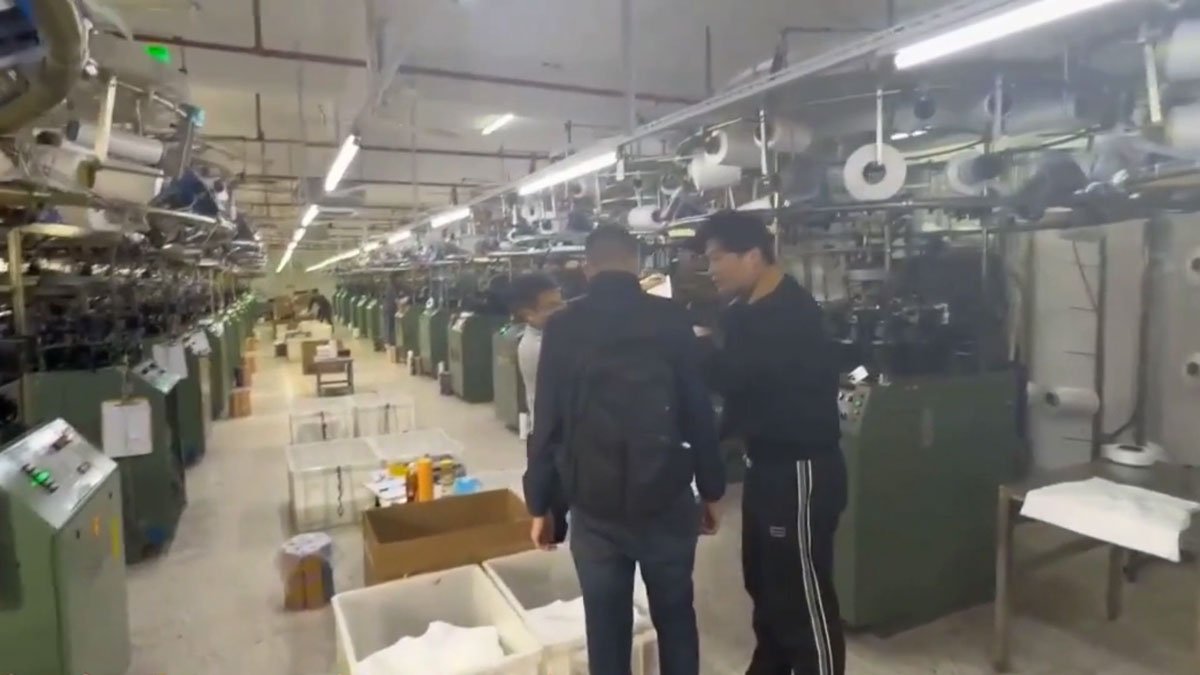
The core Seamless manufacturing system includes 28 Italian Santoni machines. Buyers can review equipment, yarn handling, program organization, trial production and the downstream steps required to convert a knitted Sports Bra body into the complete approved product.
MOVEVOX Santoni equipment within the Yiwu Seamless operation.
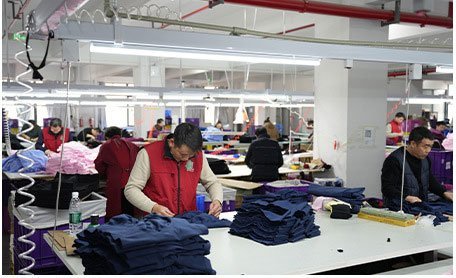
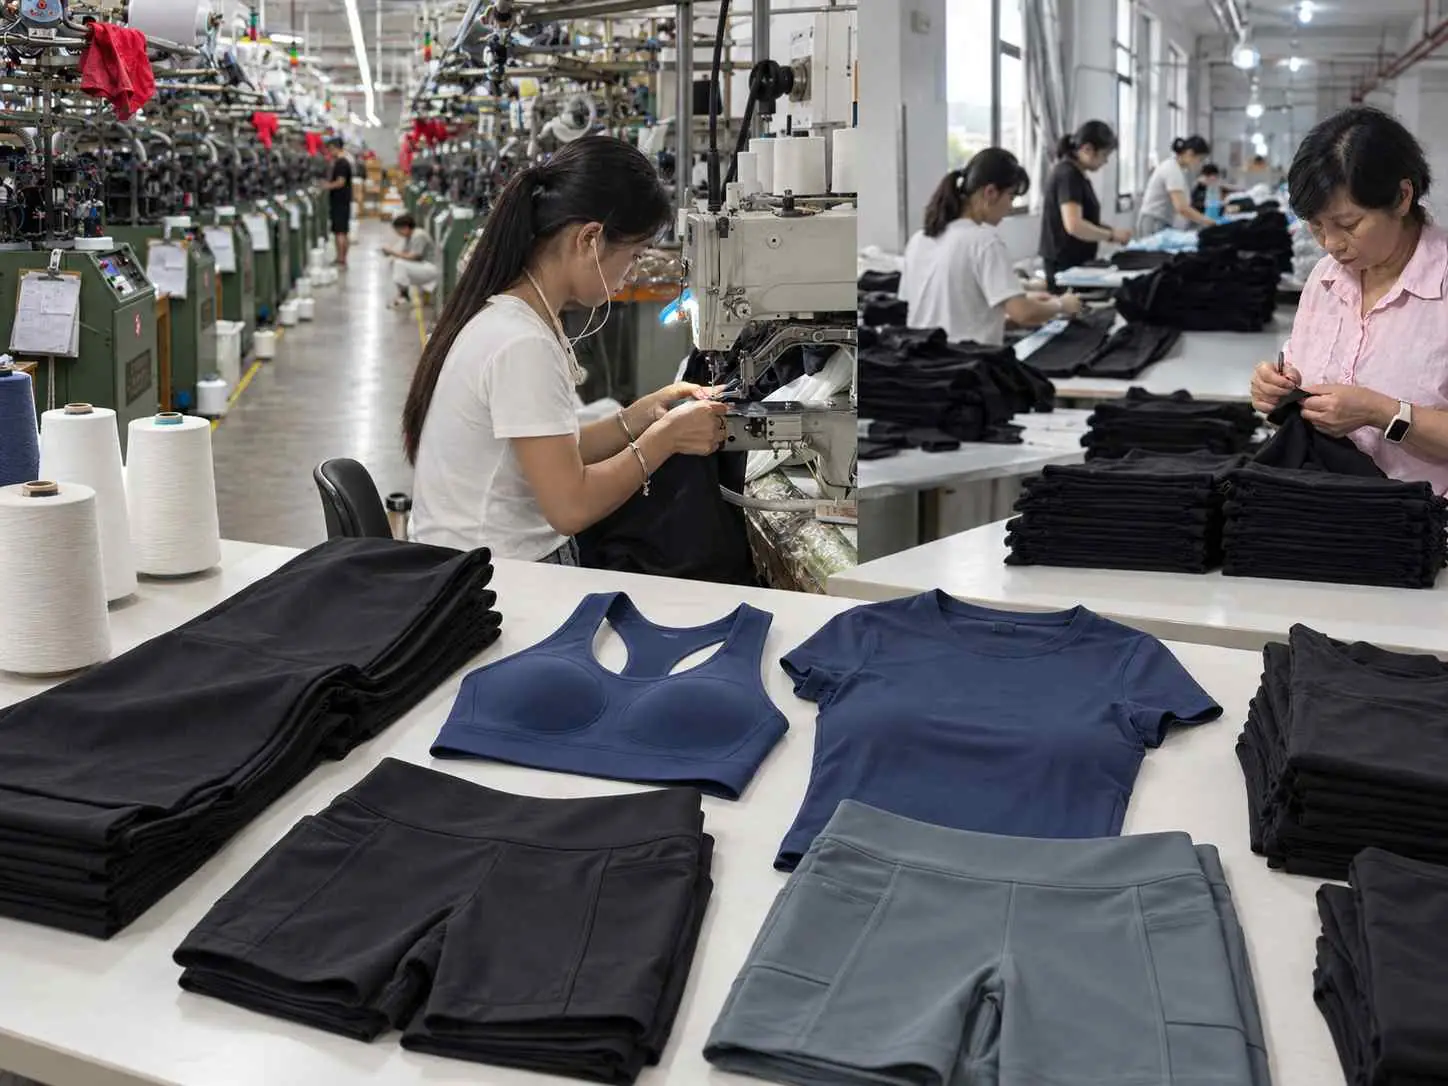
Cut & Sew
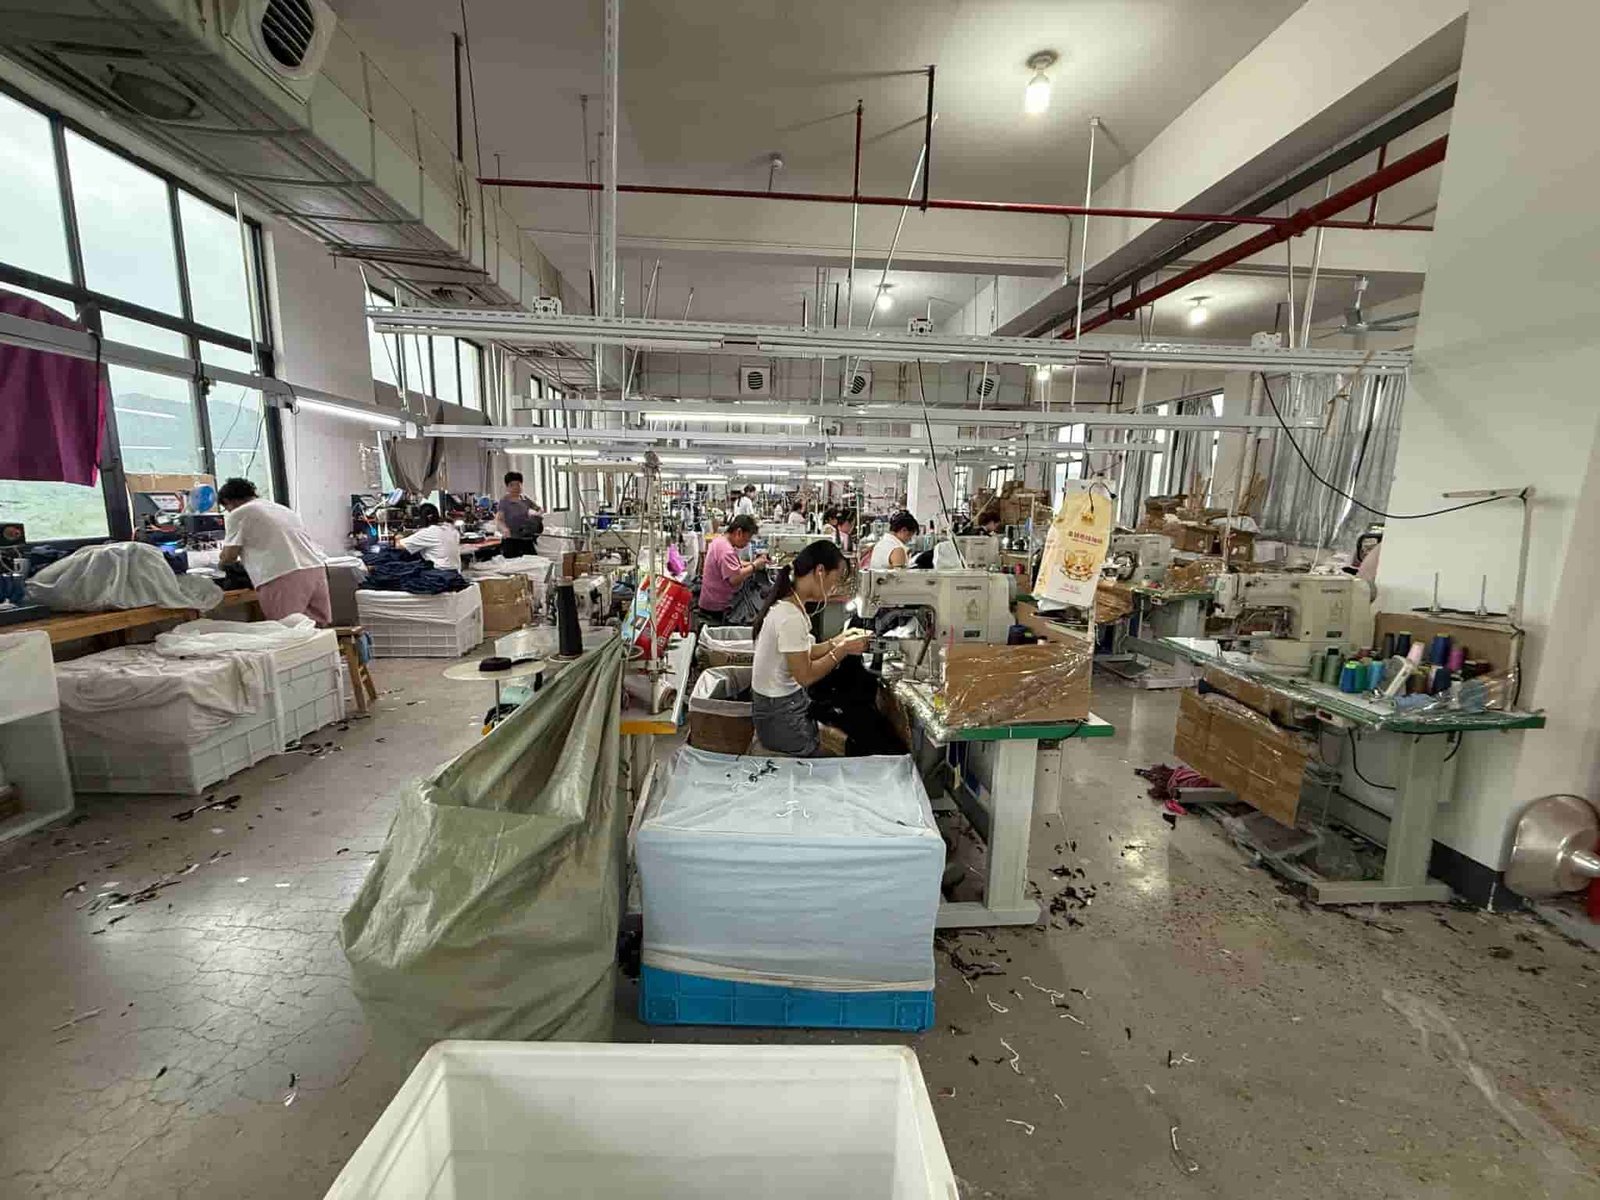
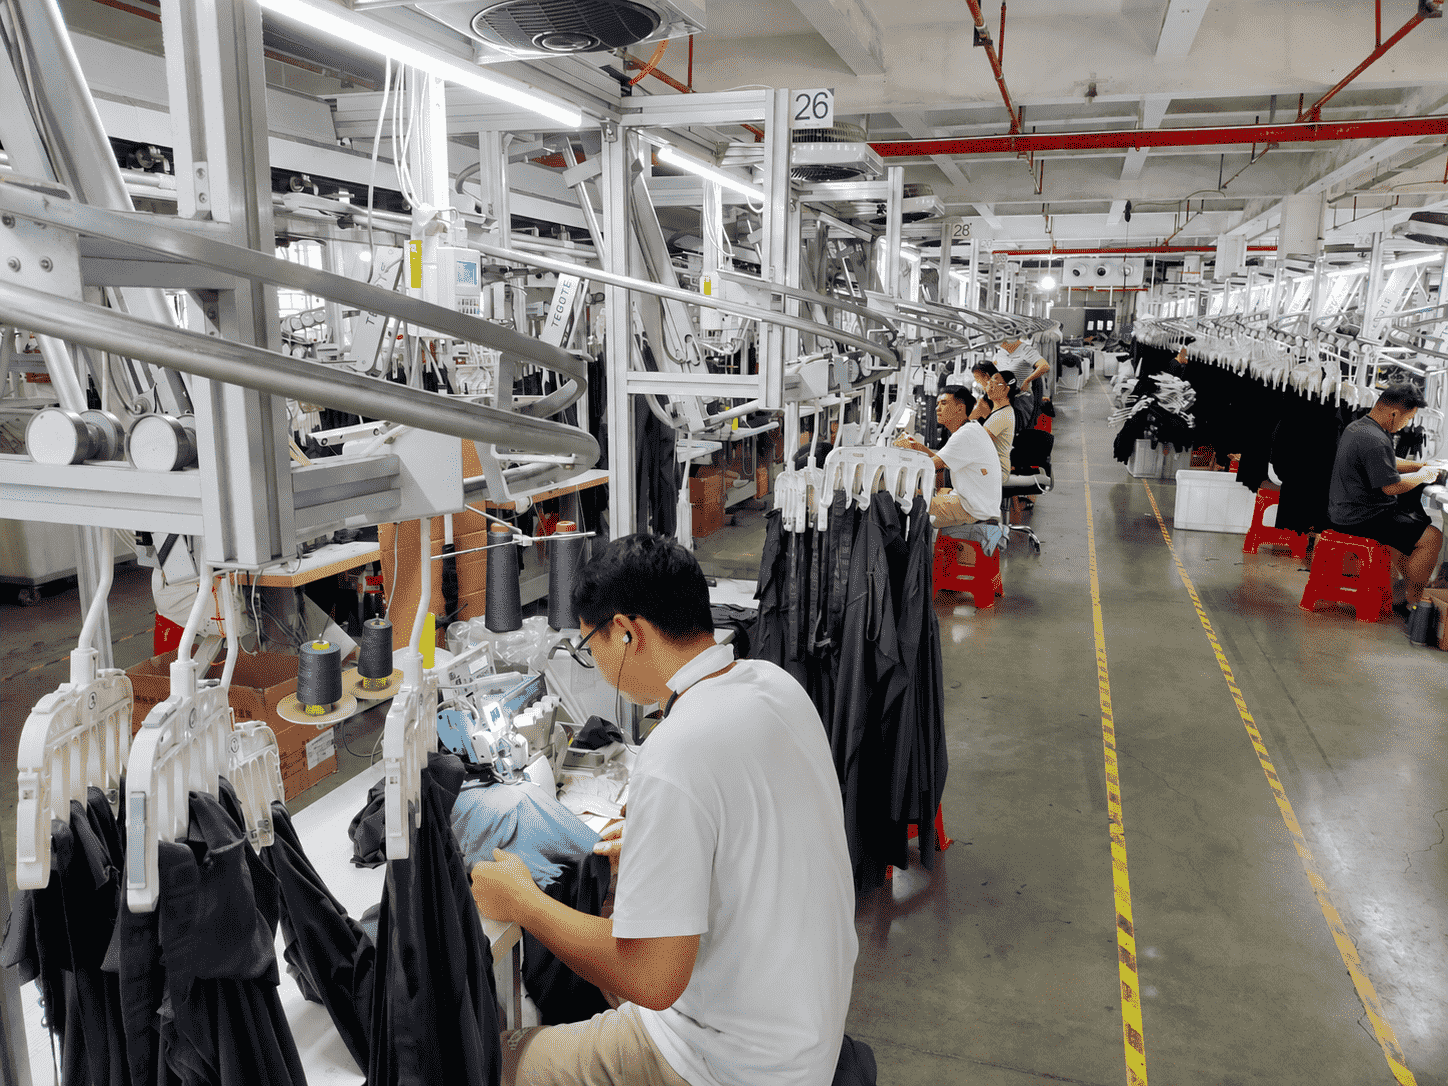
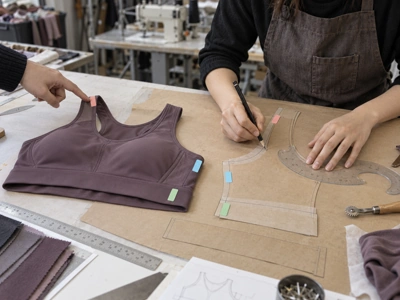
MOVEVOX's core self-operated Cut & Sew area includes approximately 24 principal sewing and garment machines. A technical visit can examine Racerback pattern execution, strap assembly, bindings, underband construction, lining, padding and other applicable operations.
Cut & Sew operations support structured Racerback assembly.
Quality Control
Five current QC personnel support relevant production inspection and quality execution. Buyers can review First Article, inline, measurement, workmanship, finished-product and packing control according to the actual product and order.
QC should verify Racerback geometry beyond exterior appearance alone.
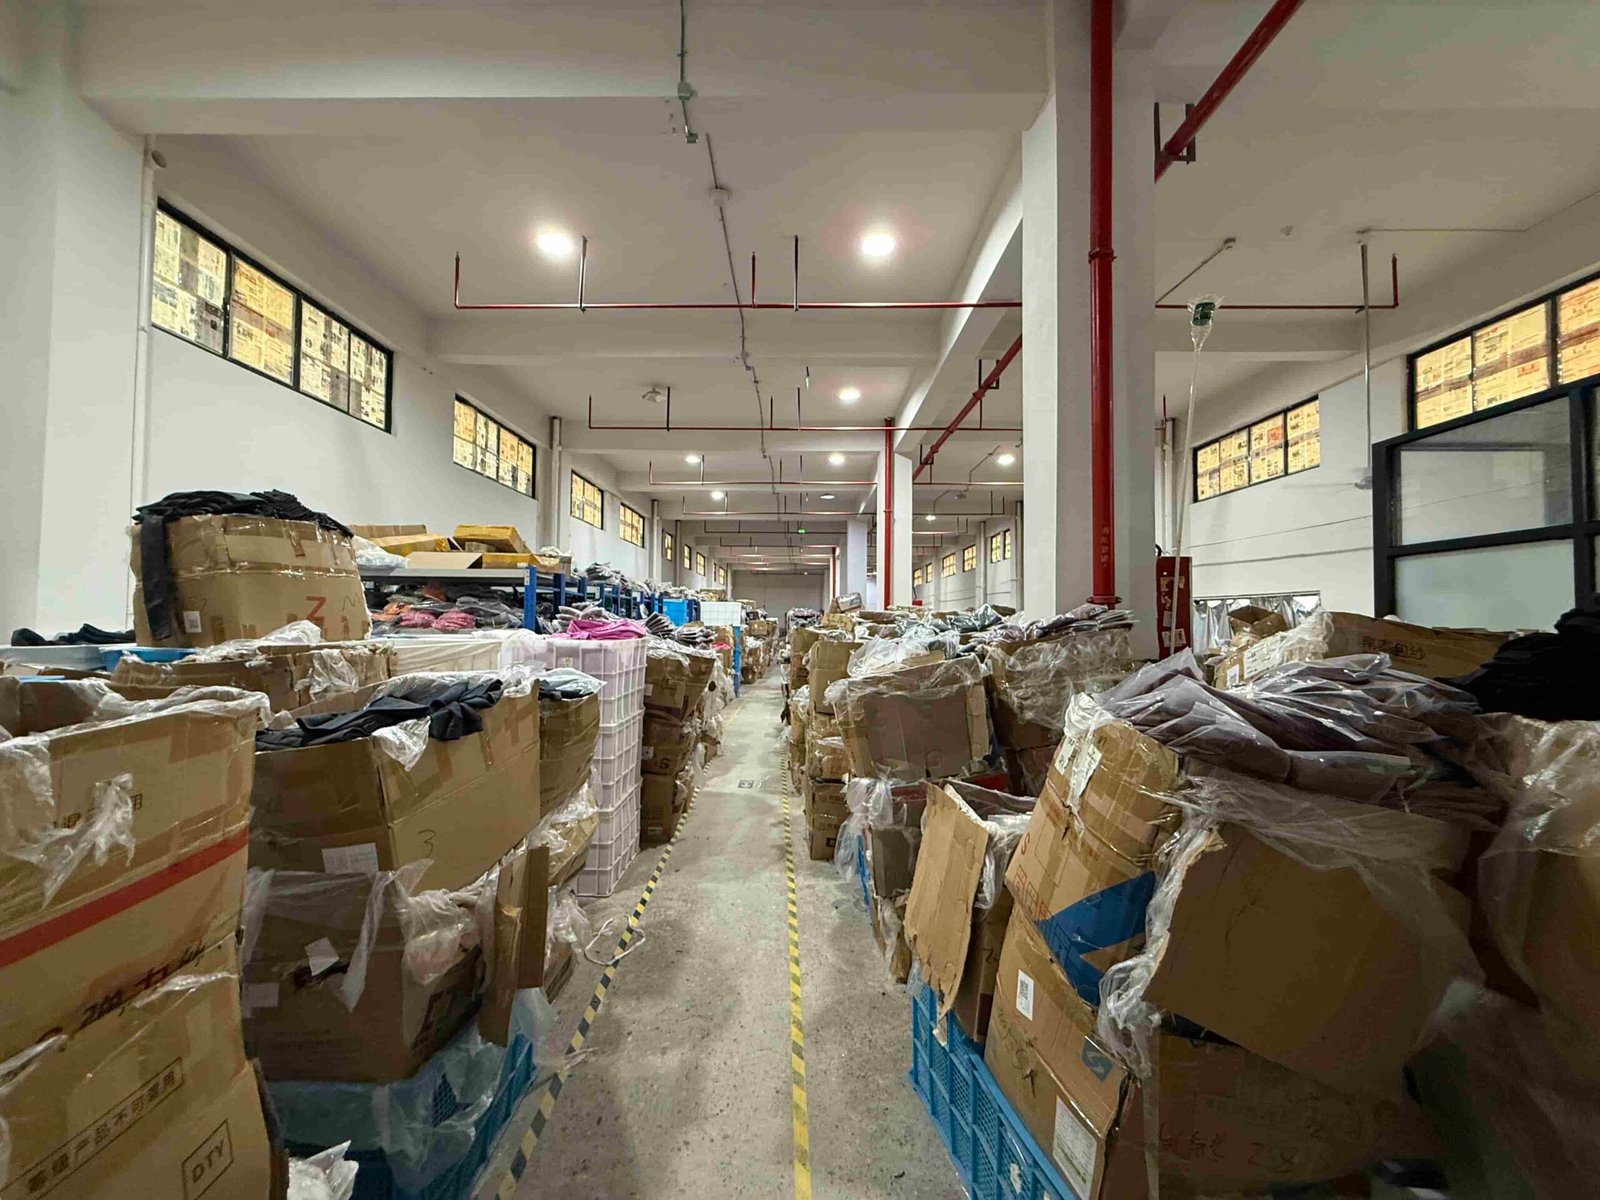
Packing
Packing connects style, color, size, barcode, SKU, labels and buyer-defined packaging to the correct finished garment. For larger Racerback programs, the audit can review how multi-color and multi-size products remain identified through packing.
Correct SKU identity should remain connected to the approved product.
Production Records
Relevant technical and quality records can connect the order with current product information, materials, production, inspection and shipment status. Records should be reviewed without exposing confidential information belonging to other customers.
Controlled records support auditability while protecting customer confidentiality.
Satellite Capacity
MOVEVOX uses eight long-term collaborative satellite facilities—six in Yiwu and two in Guangzhou—as part of its managed production network. Where buyer-approved-factory or site requirements apply, production allocation should remain transparent and subject to the applicable written requirement.
Collaborative capacity should not be presented as wholly owned production.
Trace Racerback Orders Across the Controlled Supply Chain
MOVEVOX combines self-operated manufacturing with controlled collaborative resources. Long-term brands need visibility into materials, production allocation, quality evidence and the commercial order they belong to.
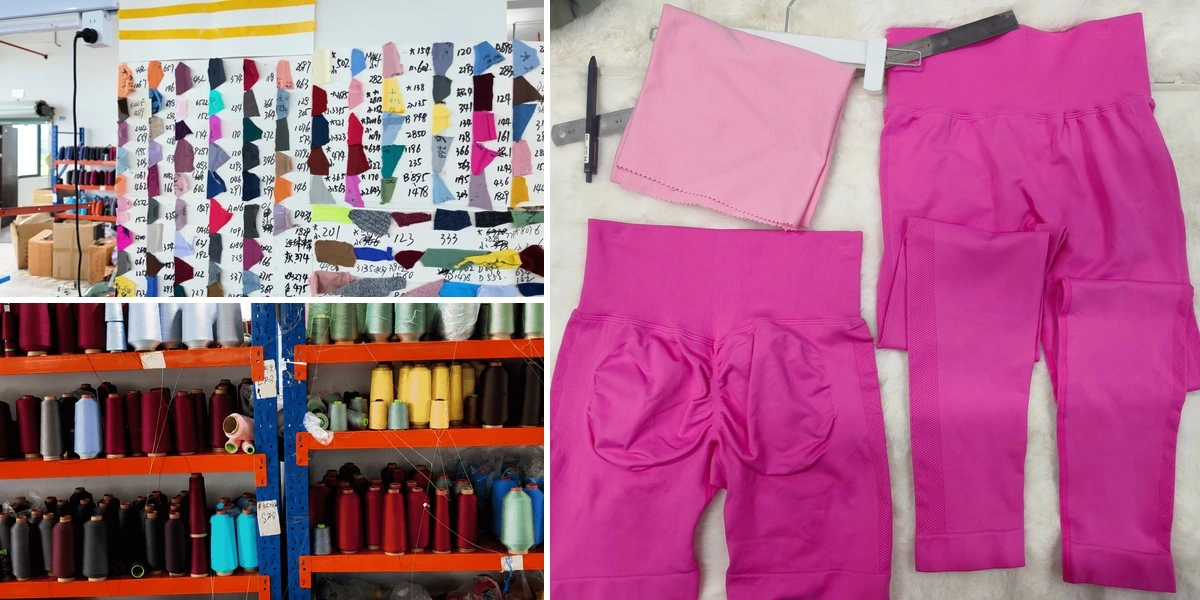
Yarn
Seamless yarn should remain connected to supplier, color or lot information and the applicable style or production requirement so a material issue can be investigated against the real order.
Fabric
Cut & Sew fabrics and lining should retain approved material references and relevant supplier or lot information before they enter cutting and assembly.
Components
Elastic, Bra Pads, labels and other critical externally sourced components can be mapped to the applicable project according to their supplier and receiving records.
Core Factory
The Yiwu core operation covers development, Seamless, Cut & Sew, QC, packing and management activities according to the actual production route.
Satellite Facility
Approved collaborative facilities can add production flexibility while remaining subject to centralized project standards, WIP control and quality requirements.
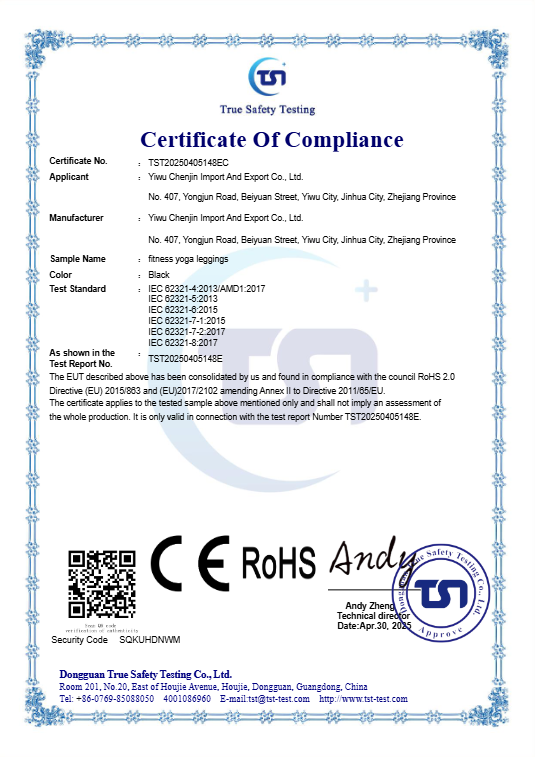
Inspection
First Article, inline, measurement, workmanship and final inspection records should remain connected to the correct PO, style, color and production scope.
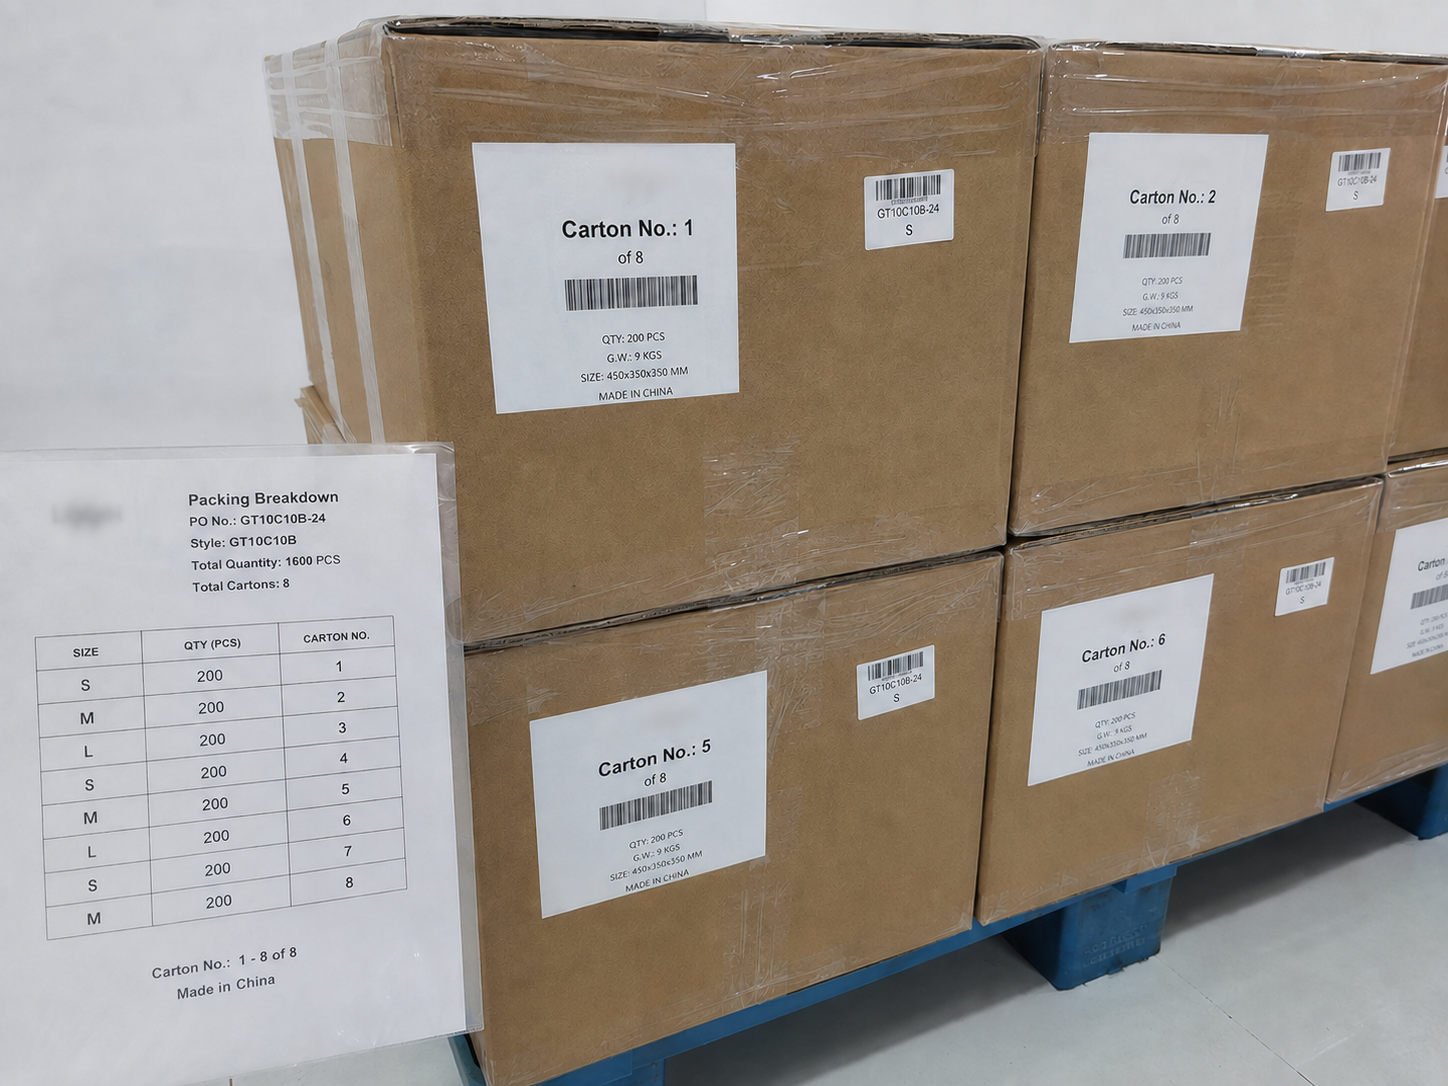
Packing
SKU, size, barcode, label and packaging information should remain connected to the correct finished garment and buyer order before shipment.
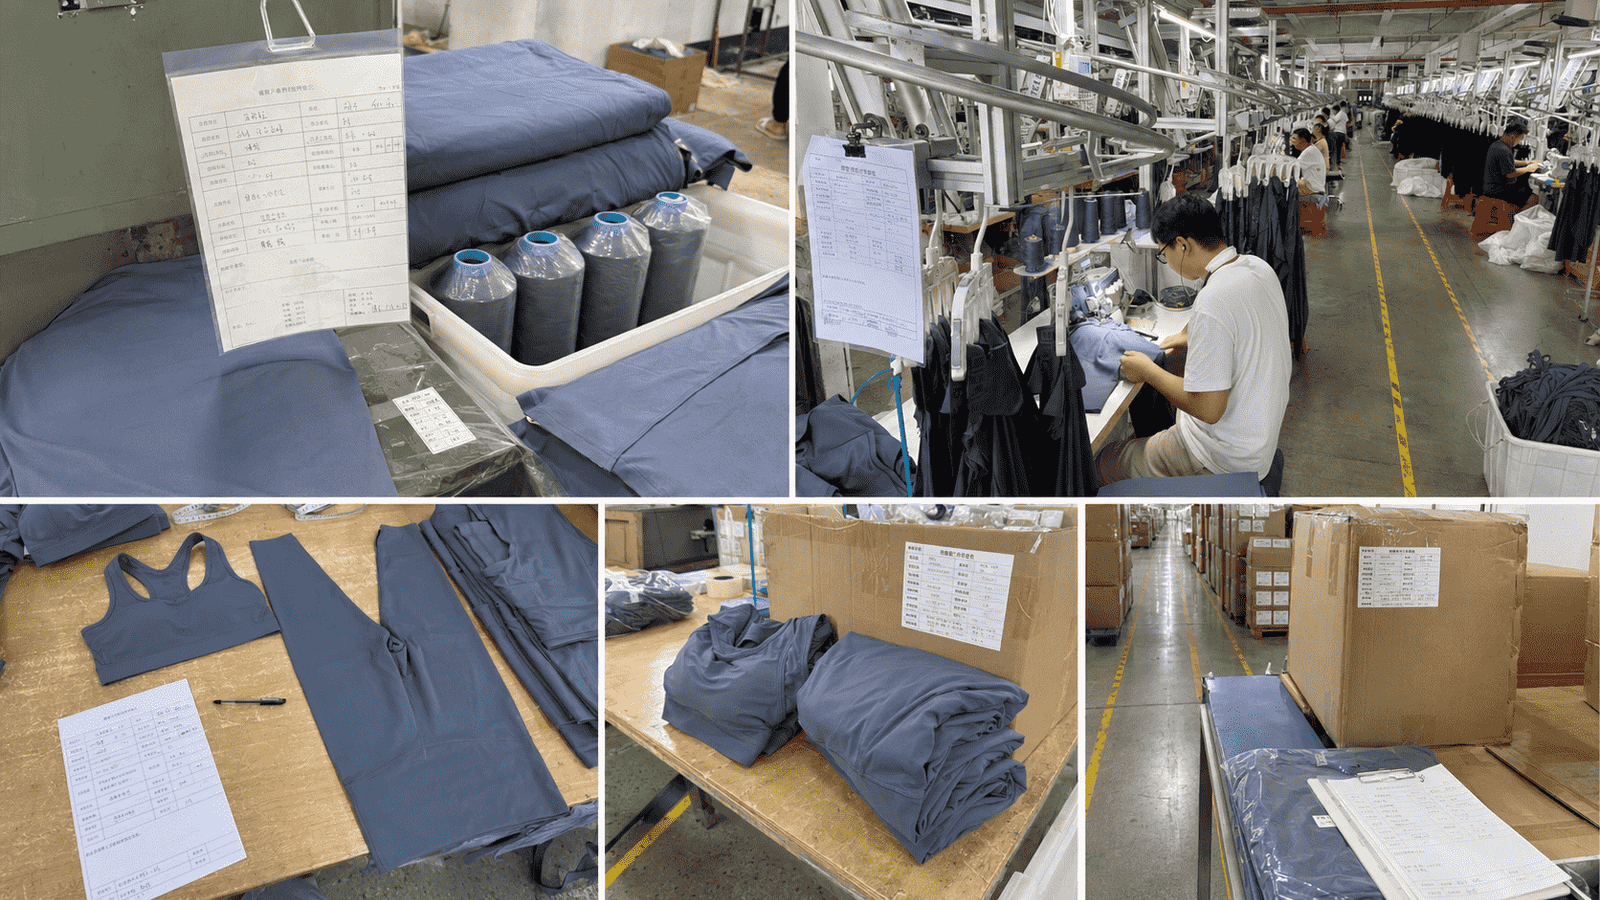
Shipment
Released production can be connected to commercial order, packing and shipment documentation so execution evidence remains traceable after the goods leave production.
From Sports Bra Development to Repeat Activewear Orders
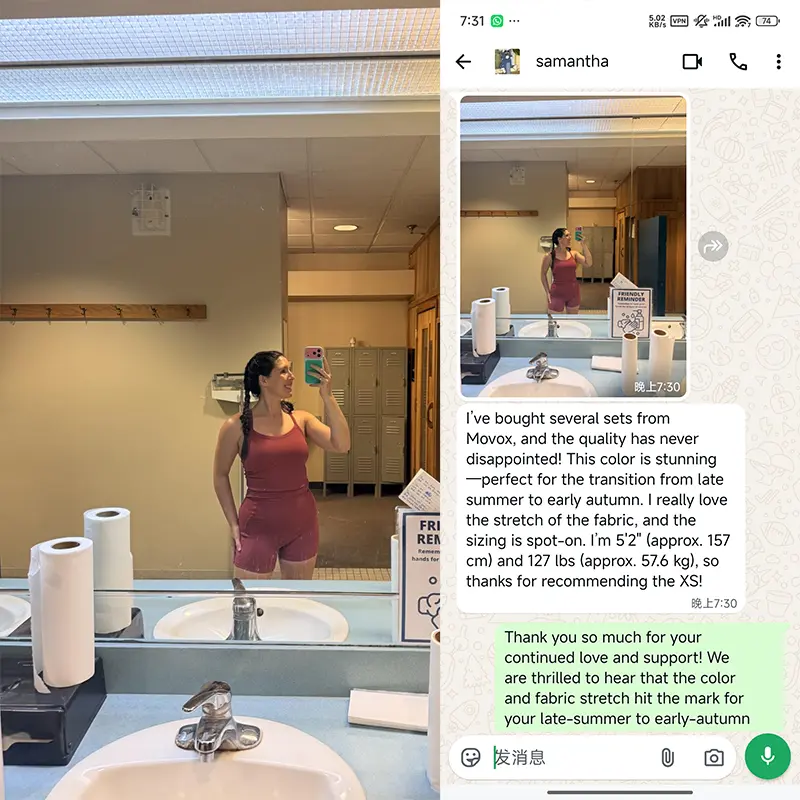
An anonymized U.S. activewear customer worked with MOVEVOX through Tech Pack development, sample revision, wearer-test sampling, branded bulk execution and repeat purchasing across a multi-SKU program that included Sports Bras. The case is not presented as Racerback-specific validation.
Customer Background
The customer operates in the U.S. fitness market and developed multiple activewear categories with MOVEVOX, including leggings, shorts, Sports Bras, tops, sets and bodysuits. The project required physical product development, multiple materials, private-label branding and structured SKU execution rather than a simple ready-made garment purchase.
Challenge
The buyer needed the product to move through real sample feedback before commercial production. A first physical version was not treated as automatically ready for bulk.
As the program expanded, commercial execution became more complex. Multiple products, sizes and colors had to remain aligned with branding, care information, custom packaging, printed materials and SKU-specific QR identification. This increased the need for technical version control, product identity and packing accuracy across the activewear program.
MOVEVOX Solution
MOVEVOX reviewed the customer's technical package and produced the first development sample. The customer used physical samples under its own fitness conditions and returned consolidated comments for revision.
MOVEVOX prepared the next version based on those comments. After the revised product direction was substantially accepted, approximately 5–10 additional samples were prepared so the customer and its audience could conduct practical wearer testing.
The approved activewear program then moved into branded commercial production. MOVEVOX coordinated garments, logo, labels, care information, customized packaging, printed materials and SKU-specific QR identification. For orders containing several colors and sizes, packing controls were organized to reduce the risk of a QR code or SKU being matched with the wrong garment.
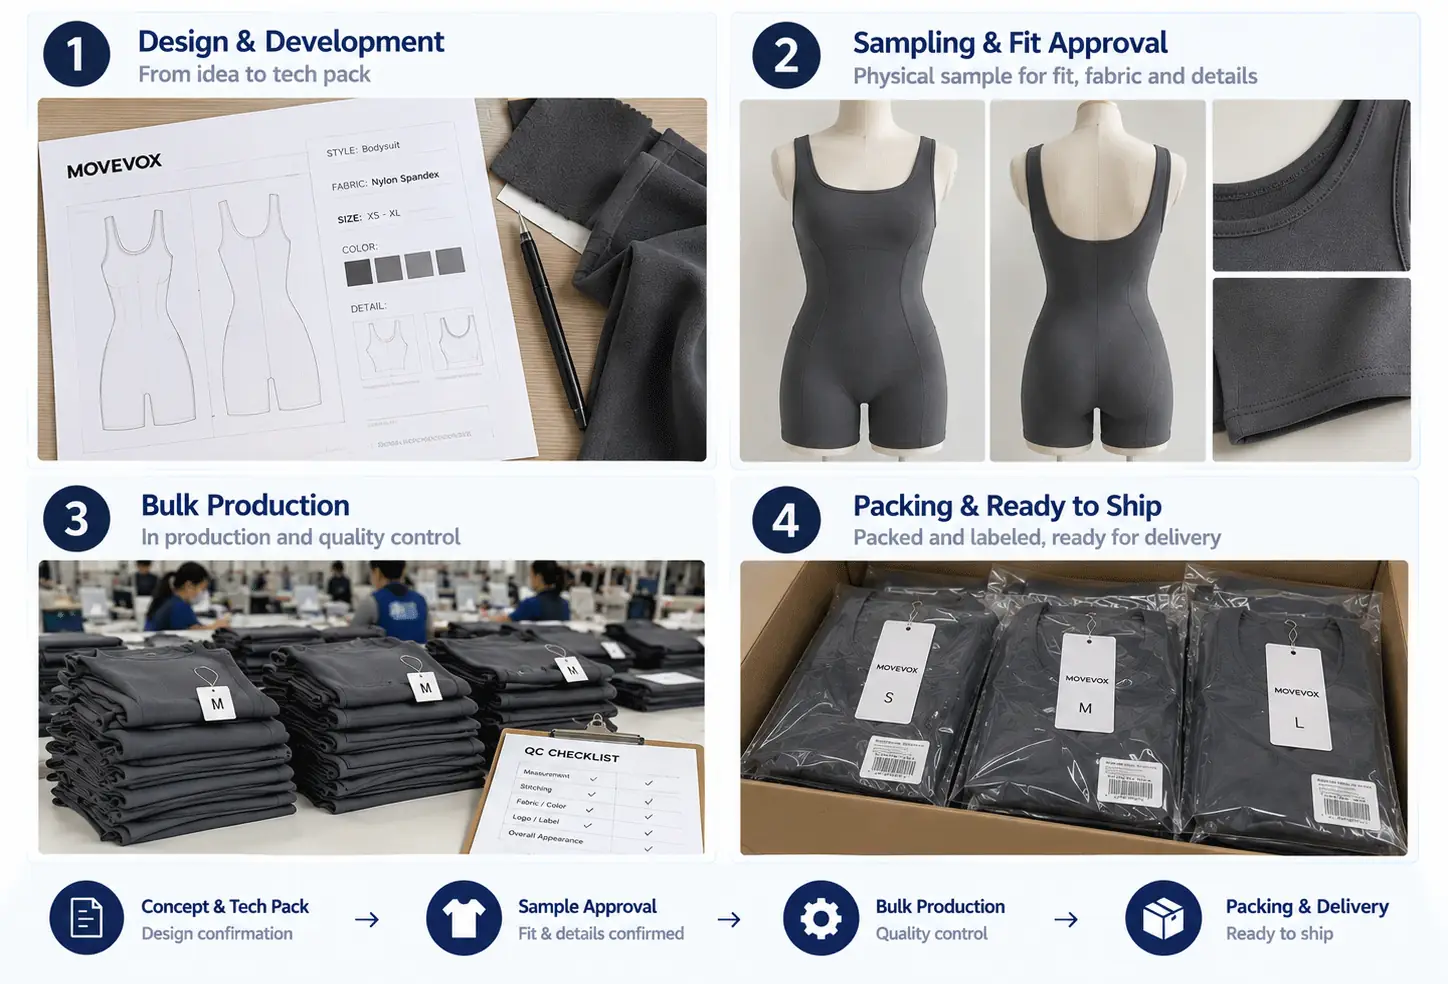
Tech Pack
The buyer supplied formal technical information that established the starting reference for product development and manufacturing feasibility.
First Sample
MOVEVOX produced the initial physical garment so actual Fit, material and construction could be evaluated beyond the flat technical file.
Revision
Customer comments were consolidated and converted into a revised physical version rather than passed to production as informal verbal instructions.
Wearer Samples
Approximately 5–10 additional samples were prepared after revision for practical wearer feedback before the commercial program advanced.
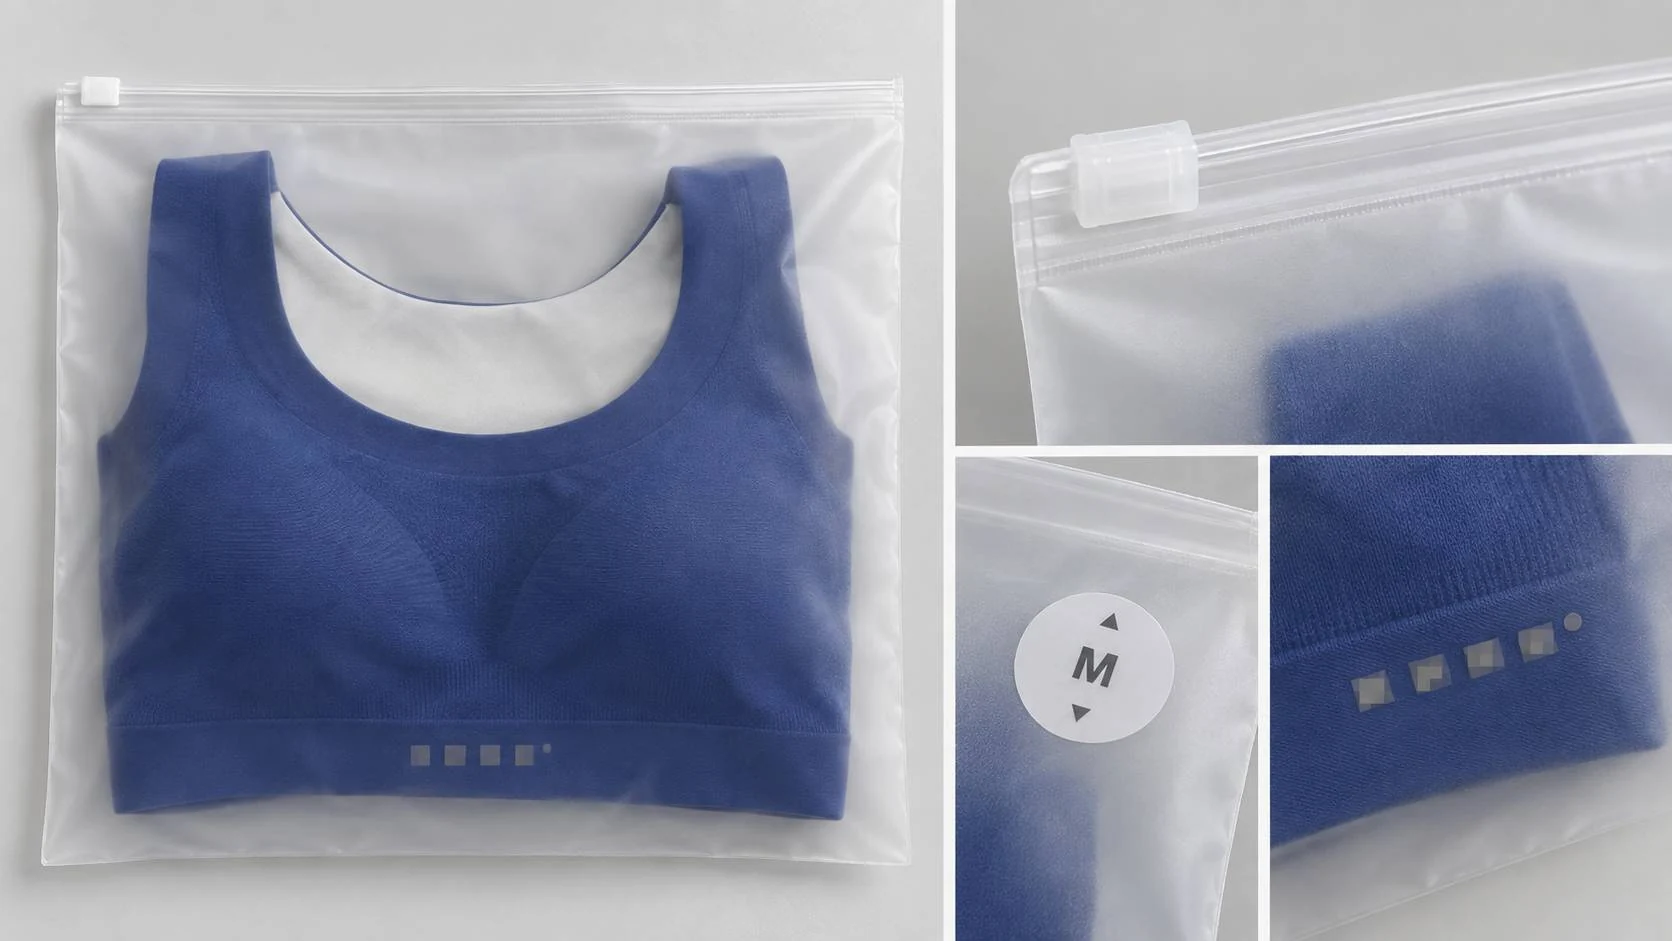
Branded Bulk
Approved products moved into bulk with logo, labels, care information, custom packaging, printed materials and QR / SKU identification.
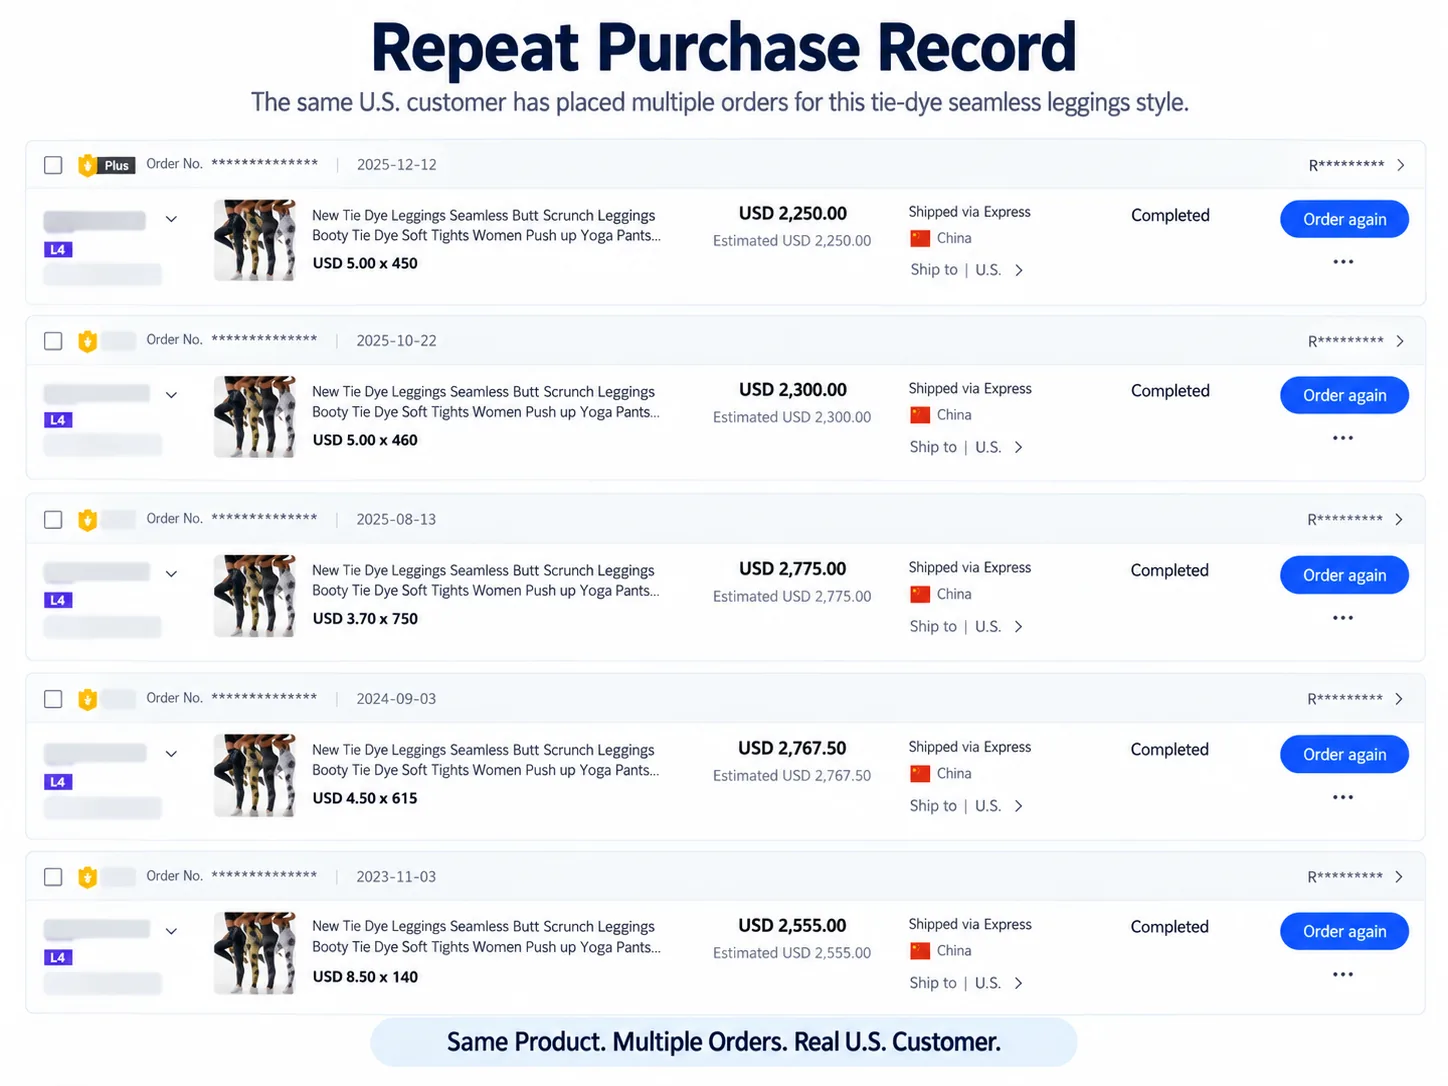
Repeat Orders
The documented cooperation continued into repeat purchasing, demonstrating a relationship that progressed beyond one isolated sample or trial order.
Test Samples
Additional wearer-test samples prepared after the main revision stage.
Pieces / Order
Historical example commercial orders were approximately 2,000 pieces per order.
Repeat Orders
The established cooperation record documents approximately two orders per month during a period of recurring business.
Cooperation
The documented customer relationship extended for approximately three years in the available case record.